Steam turbines in modern power plants routinely convert 38–46% of fuel energy into electricity, but every 1% drop in isentropic efficiency quietly costs a 500 MW unit upwards of $1.2 million per year in lost generation — which is why a disciplined steam turbine maintenance program, backed by a modern CMMS, is the single highest-leverage reliability investment a power generator can make. This guide breaks down HP, IP and LP blade inspection intervals, gland seal and thrust bearing procedures, valve overhaul cycles, and lube oil management for 2026, with field-tested PM templates and worked cost examples you can apply immediately. Whether you run a single extraction-condensing unit or a multi-shaft combined-cycle fleet, the checklists and KPIs below are designed to be imported directly into OxMaint so work orders, readings and failure codes flow without manual entry. Start Free Trial to deploy these PM templates in minutes, or read on for the full technical walkthrough.
Is your turbine losing 3% efficiency between overhauls — and you can't see it?
Undetected blade fouling, seal degradation and thrust bearing wear silently drain 1.5–3.0% of unit output within 18 months of a major inspection. A CMMS-driven preventive maintenance program catches the drift at 0.2% — before it becomes a $900K generation loss. This guide gives you the inspection intervals, PM task libraries and KPI thresholds to do exactly that.
The four-section turbine PM checklist most plants under-execute
A typical HP/IP/LP steam turbine demands 180–260 distinct preventive tasks per major overhaul cycle. The grid below condenses the high-criticality subset that directly protects availability and heat rate — organized by turbine section so crews can scope work orders without missing cross-section dependencies.
High-Pressure Section
- Borescope first-stage nozzle & blade leading edges after 8,000 operating hours
- Measure HP gland steam leakage flow; flag if >1.5% of main steam flow
- Record casing metal temperature differentials — alarm at >75°C top-to-bottom split
- Verify stop valve stroke time <0.5 s on monthly test
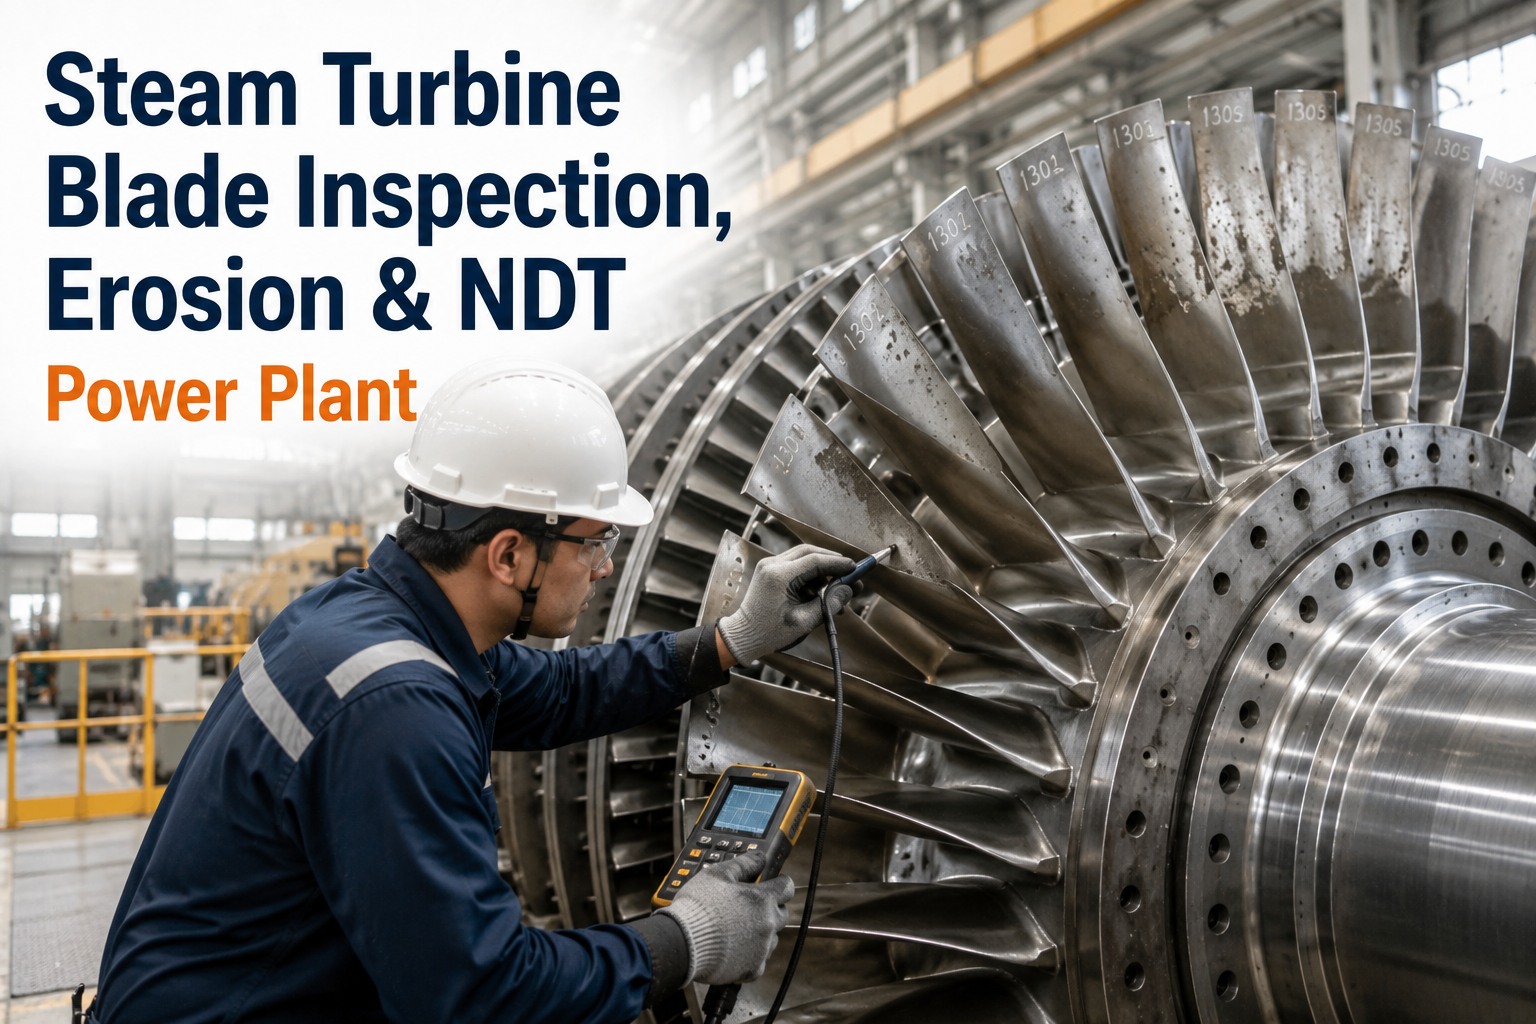
- Inspect blade root serrations via ultrasonic phased array at every major
Intermediate-Pressure Section
- Borescope reheat stage blades for erosion and copper deposition
- Check interstage labyrinth seal clearances against OEM chart ±0.05 mm
- Verify reheat stop & intercept valve exercise logic monthly
- Sample expansion joint bellows for creep at 60,000 hours
- Diagnose diaphragm casing split leaks with helium trace gas
Low-Pressure Section
- Inspect last-stage blade (LSB) for water erosion, stress-corrosion cracking
- Confirm condenser tube cleanliness factor >85% — back-pressure below 7 kPa
- Drain & inspect LP casing water extraction nozzles for blockage
- Verify moisture separator reheater (MSR) performance — superheat >28°C at outlet
- Test Stellite shields on LSB at every major; replace at >0.4 mm wear
Auxiliaries & Fluid Systems
- Sample lube oil every 30 days — ISO 4406 cleanliness 18/16/13 max
- Calibrate journal bearing drain temperature RTDs — alarm at 85°C
- Test thrust bearing shoe babbitt via eddy-current at major overhaul
- Verify turning gear engagement & 3–5 rpm roll rate after every trip
- Inspect gland steam condenser vacuum & seal water flow monthly
Steam turbine inspection cadence — what to do, when, and why
Interval drift is the most common root cause of unplanned turbine trips. The table below fuses OEM recommendations (GE, Siemens, Mitsubishi) with EPRI guideline 3002006395 into a single scannable schedule your CMMS can auto-trigger as PM work orders.
| Task | Frequency | Section | Acceptance Criterion | Risk if Skipped |
|---|---|---|---|---|
| Online vibration spectrum analysis | Continuous | All | ≤2.8 mm/s RMS at rated load | Bearing failure in 30–90 days |
| Lube oil particle & moisture test | 30 days | Aux | ISO 4406 18/16/13 · ≤30 ppm H₂O | Babbitt degradation, journal wipe |
| Stop / intercept valve stroking | Monthly | HP / IP | Full close ≤0.5 s, no sticking | Overspeed event on load rejection |
| Borescope internal inspection | 8,000 hrs or 12 mo | HP / IP / LP | No erosion >0.3 mm, no SCC | Forced outage, blade liberation |
| Gland seal clearance check | 18 mo | HP / IP | Within OEM ±0.05 mm | 1.5–3% heat rate penalty |
| Major turbine overhaul | 100,000 hrs / 8 yr | All | ASME PTC 6 acceptance test ±0.5% | Catastrophic failure, $4–9M loss |
The math behind a 1% efficiency loss — and how PM recovers it
Plant engineers routinely underestimate the dollar value of incremental turbine efficiency. Use the formula below to size the business case for a CMMS-driven PM upgrade before next budget cycle.
L = loss ($/yr) · P = rated MW · Δη = efficiency lost (fraction) · H = operating hours · Tariff = $/MWh
2% efficiency drift from seal + blade fouling on a base-load 500 MW unit at $42/MWh — recovered by a $48K/yr CMMS PM program.
Put this entire PM program on autopilot — inside OxMaint
Import the 180+ task library, set OEM trigger intervals, and auto-generate work orders the moment a bearing temperature or vibration threshold drifts. Most plants go live in under 14 days.
The five failure modes that drive 80% of unplanned turbine outages
EPRI failure data across 1,200+ steam turbines shows that just five mechanisms account for the bulk of forced outages. Coding every PM and corrective work order against this taxonomy in your CMMS turns tribal knowledge into a trending reliability database.
Blade Fatigue & SCC
High-cycle fatigue at blade root serrations and stress-corrosion cracking in LP last-stage blades account for ~28% of major steam turbine failures. Detect via borescope + phased-array UT at 8,000-hour intervals.
Gland Seal Degradation
Worn labyrinth seals leak 1.5–3% of main steam flow, directly inflating heat rate. Spring-backed segmented seals typically need replacement at 40,000–60,000 hours depending on duty cycle.
Thrust Bearing Failure
Babbitt fatigue from oil contamination or axial load excursions causes ~17% of bearing-class failures. Continuous axial-position monitoring plus 30-day oil sampling catches 90% of precursors.
Valve Stem Stiction
Stop, control and intercept valves develop stem friction from steam deposits. Monthly full-stroke testing and annual packing inspection prevent overspeed trip failures on load rejection.
Lube Oil Contamination
Water ingress >30 ppm or particles above ISO 18/16/13 degrade babbitt surfaces within months. A bypass polishing loop with automatic moisture removal is the single most cost-effective safeguard.
Five KPIs your CMMS should trend — and the alert thresholds
A steam turbine PM program without thresholds is just a calendar. Wire these five KPIs into OxMaint condition monitors so a deviation auto-opens a work order before operations ever notices.
ISO 10816 Zone B/C boundary for large flexible-rotor machines.
Journal bearing — verify flow and oil cooler ΔT on breach.
Trigger immediate load reduction; inspect thrust shoes at next outage.
Engage polishing loop; check gland steam condenser vacuum.
Open blade fouling & seal degradation investigation work order.
How a 1,200 MW coastal plant cut forced outages by 62% in 14 months
A two-unit coal-fired station on the U.S. Gulf Coast was losing 3.4 equivalent forced outage hours per month to steam turbine trips. After migrating 214 PM tasks and 11 condition monitors into OxMaint, the reliability team hit the milestones below.
Steam turbine maintenance — five questions plant engineers actually ask
How often should a steam turbine be borescope-inspected?
For base-loaded units, borescope the HP, IP and LP blade paths every 8,000 operating hours or 12 months — whichever comes first. Cycling units should halve that interval because thermal transients accelerate blade root fatigue and diaphragm distortion. OxMaint can auto-trigger the work order once the running-hour meter crosses the threshold, eliminating the calendar drift that causes most missed inspections.
What lube oil cleanliness target should we maintain?
Hold ISO 4406 cleanliness at 18/16/13 or better for turbine oil systems, with water content below 30 ppm. Particles above 14 µm are the leading cause of babbitt fatigue in journal and thrust bearings. A polishing loop sized for 10% of total oil volume per hour, combined with monthly CMMS-scheduled sampling, typically returns the cost of installation within one avoided bearing wipe — around $180K on a 500 MW unit.
When do gland steam seals need replacement versus re-tightening?
Spring-backed labyrinth seals generally need replacement at 40,000–60,000 operating hours, but the real decision criterion is leakage flow. If gland steam leakage exceeds 1.5% of main steam flow or the gland condenser vacuum drops more than 2 kPa below baseline, schedule seal replacement at the next planned outage — don't wait for the major overhaul interval. Book a Demo to see how OxMaint trends gland leakage data into a seal-replacement forecast.
Can a CMMS really prevent thrust bearing failures?
Yes — provided it ingests the right signals. Thrust bearing failures are almost always preceded by 30–90 days of rising axial displacement, oil temperature, and particle count. Wire those three signals into OxMaint as condition monitors with the alert thresholds listed above, and the system will auto-open an investigation work order at the first deviation — long before babbitt distress becomes measurable, let alone catastrophic.
What does a CMMS-driven turbine PM program cost versus save?
A mid-size fleet deploying OxMaint for steam turbine PM typically invests $36K–$60K per year in software plus 0.5 FTE of reliability engineering. Against that, a single avoided forced outage on a 500 MW unit returns $1.2M–$2.1M in margin, and a 1% efficiency recovery returns another $164K annually. Most plants see payback inside 14 months. You can Start Free Trial and import the task library in under a day.
Stop losing megawatts to drift your CMMS should have caught
Import the full steam turbine PM library, wire condition monitors to auto-work-orders, and watch your heat rate deviation trend flatten inside one outage cycle.
Free 14-day trial · No credit card