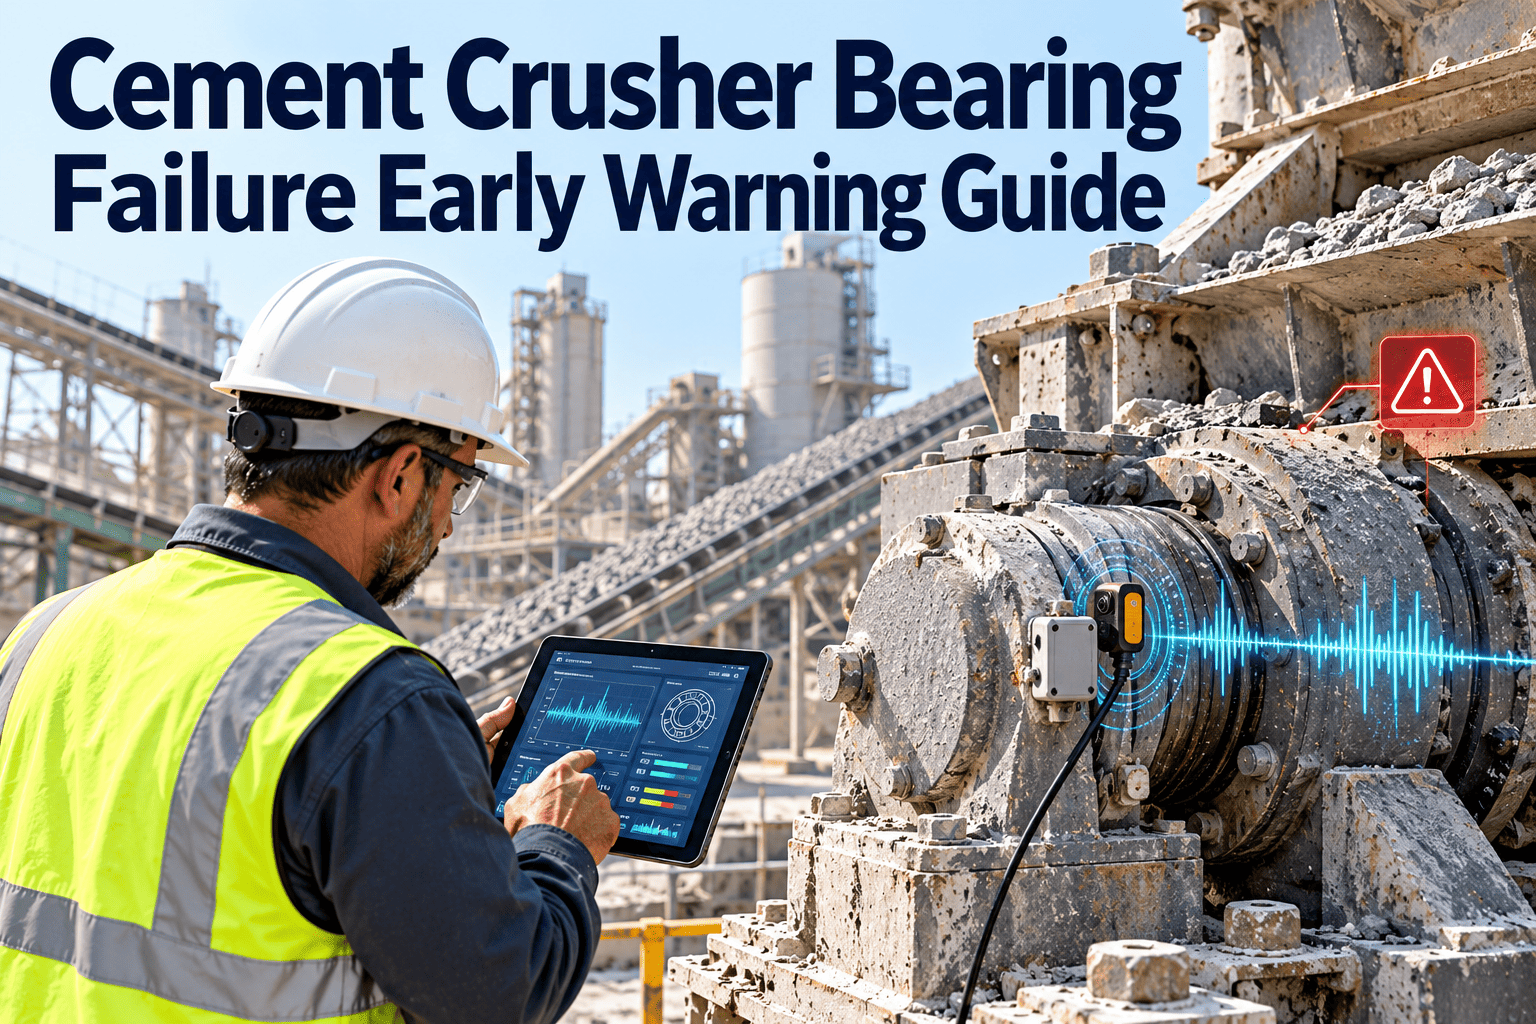
A crusher bearing rarely fails without warning, yet many plants only learn about it when the rotor stops and the primary crusher blocks the whole feed line. Heavy shock loads, dust, heat and irregular greasing wear bearings in ways that show up weeks earlier as small changes in vibration, temperature and sound. This guide explains the early warning signs, how to read them in order, and how to turn each signal into a planned job instead of an emergency stop. It also shows how a CMMS such as Oxmaint can keep readings, work orders and bearing history together.
Cement Crusher Bearing Failure Early Warning Guide
Primary and secondary crushers: catch bearing damage while it is still a planned job
Link vibration, ultrasound, temperature and lubrication signals into one warning ladder, with a clear action at every rung.
Ultrasound change
Vibration rise
Heat and grease condition
Noise and visible damage
Seizure and stoppage
Why crusher bearings are a special case
Harsh duty
- Impact loading from uncrushed material and tramp metal shortens bearing life.
- Limestone dust works past seals and mixes with grease.
- Slow rotor speeds on some designs weaken the signal that vibration tools rely on.
High consequence
- A crusher stoppage starves the kiln feed chain and forces a stockpile draw-down.
- Bearing seizure can damage shafts and housings, turning a short job into a long repair.
- Access and lifting needs make unplanned work slow and costly.
The warning ladder: what changes first, and what to do
| Stage | Signal | Typical tool | Response |
|---|---|---|---|
| Earliest | Rising high-frequency ultrasound energy, lubricant film breaking down | Ultrasound probe or sensor | Check grease quantity and type, then retest |
| Early | Bearing defect frequencies appear in the vibration spectrum | Portable analyzer or online sensor | Raise a planned work order and order the bearing |
| Developing | Temperature trend climbs against its own baseline | Infrared gun or fixed sensor | Increase inspection frequency, schedule the outage window |
| Late | Audible noise, grease discoloration, metal particles | Operator rounds, grease sampling | Plan replacement at the first safe stop |
| Critical | Sharp temperature rise and heavy vibration | Alarm and trip logic | Stop and isolate under lockout |
Common root causes behind bearing failure
A
Lubrication errors
Too little, too much, wrong grease or mixed grease types. Track quantity and interval per point rather than relying on memory.
B
Contamination
Damaged seals and dirty grease nipples let abrasive dust into the raceway.
C
Misalignment and looseness
Foundation movement or loose housings raise load on one side of the bearing.
D
Overload and tramp metal
Repeated shocks fatigue the bearing. Log events so patterns show up.
Set alert levels from your own baseline
1. Record a healthy baseline
Capture readings after a new bearing is fitted under normal load.
2. Define alert and alarm bands
Use manufacturer guidance and applicable vibration standards, and adjust after reviewing your history.
3. Trend, do not just compare to a limit
A steady upward slope at a modest level can be more urgent than one noisy spike.
4. Review after every event
Compare what the readings said with what the teardown found.
Turn bearing readings into scheduled work
Oxmaint links inspection rounds, condition findings, work orders and spare bearings so early warnings lead to a planned repair.
Operator round checklist for crusher bearings
Touch or scan housing temperature at the same points each shift
Listen for changes in tone near each bearing
Inspect seals and grease purge for dust or discoloration
Confirm greasing was done and logged for each point
Check guards, mounting bolts and visible housing cracks
Record anything unusual with a photo in the work order
Planned replacement versus emergency failure
Run to failure
- Stoppage at an unplanned time
- Collateral shaft and housing damage
- Expedited parts and overtime
- No evidence of root cause
Condition-triggered replacement
- Job fits a planned stop
- Parts and crew ready in advance
- Removed bearing inspected and documented
- Findings feed the next baseline
Oxmaint capabilities for crusher reliability
Asset records
Bearing model, location, installed date and failure history per crusher.
Preventive and condition tasks
Lubrication routes, temperature checks and vibration rounds with due dates.
Work orders
Corrective jobs raised from findings, with assignments and closure notes.
Inventory and reporting
Critical spare visibility and repeat-failure reports.
Reading each signal in more detail
Vibration
Overall vibration level tells you something is changing, but the spectrum tells you what. Bearing defects tend to appear at characteristic frequencies related to the rolling elements and races, and later spread into harmonics and sidebands. Slow-speed crusher shafts produce weak signals, so use sensors and settings suited to low speed, and trend envelope or acceleration measurements rather than relying only on velocity.
Ultrasound
Ultrasound picks up friction and impact at the bearing surface, often before vibration changes. It is also useful during greasing, because the signal falls as lubricant fills the contact and can warn of over-greasing. Compare readings to the same point and the same operating load each time.
Temperature
Housing temperature is a late indicator, but it is simple and valuable as a backstop. Trend it against ambient conditions and load, because a bearing near a hot process area or in summer will run warmer without being damaged. A sudden rise of a few degrees above its own recent trend deserves attention.
Lubricant condition
Grease that comes out dark, gritty or hard, or oil with metal particles, tells you the damage is already happening. Sample or inspect purged grease on a regular route and record what you see with a photo, so the next person can compare.
What a good early-warning routine looks like each week
Monday: review trends
The reliability engineer reviews the previous week's vibration, ultrasound and temperature trends for each crusher and flags any that moved away from baseline.
Midweek: confirm in the field
A technician takes confirming readings on flagged bearings, checks grease condition and records findings in the work order.
Thursday: plan the job
The planner books the next stop window, confirms the spare bearing, seals and tools, and assigns the crew.
Friday: close the loop
Results of the week are logged, open warnings are ranked by risk and the next week's rounds are adjusted.
Preparing for the replacement before the stop
1
Parts and tools
Confirm the bearing, seals, adapter sleeves, locking devices and the correct grease are in stock. Confirm heating or pulling tools are serviceable and that lifting equipment is available.
2
Safety and access
Prepare lockout points, confined space or work-at-height permits and the sequence for releasing stored energy in rotors and hydraulics.
3
Procedure and fit
Follow the supplier fitting procedure, check shaft and housing condition and record clearances and alignment values, so the next failure has a better data trail.
4
Teardown and findings
Photograph the removed bearing, note the wear pattern and compare it to the signal history. Update the baseline and failure code.
Matching bearing wear patterns to causes
| What you find on teardown | Likely cause | Corrective action |
|---|---|---|
| Dull, scratched raceways with abrasive marks | Dust contamination | Upgrade seals, clean grease nipples and protect transfer containers |
| Blue or brown discoloration and cracked cage | Overheating from poor lubrication or over-greasing | Review quantity and interval, check housing cooling |
| Flaking in a line on one side of the raceway | Misalignment or uneven load | Check foundation, alignment and housing fit |
| Dents spaced like the rolling elements | Shock or impact loading | Review feed control and tramp metal protection |
| Fretting marks on the shaft or bore | Loose fit | Repair or replace the shaft or housing, check tolerances |
KPIs for crusher bearing reliability
Planned versus unplanned replacement
Share of bearing changes that happened at a planned stop.
Mean time between failures
Average running time between bearing failures on each crusher.
Warning lead time
Days between the first confirmed warning and the replacement.
Round completion
Condition and lubrication rounds completed on time.
Reading the lead-time KPI
If warning lead time is too short to order parts and plan a crew, the plan is reactive in practice. Long lead times with frequent unplanned failures suggest warnings are being seen but not acted on. Review a few recent bearing failures with the team and ask when the first signal was visible, who saw it and what stopped the job from being planned.
Setting up the workflow in a CMMS
Register each crusher and every bearing as separate assets with model and installed date
Create recurring tasks for greasing, temperature checks, ultrasound and vibration rounds
Add required fields for readings, grease quantity and observations
Define a corrective work order template for suspected bearing damage
Link the bearing, seals and grease to the asset's parts list
Use failure codes that distinguish contamination, lubrication, overload and misalignment
Review repeat failures monthly and update tasks and baselines
Attach teardown photos to the work order for future reference
Why records matter more than memory
Crusher crews change, and the person who remembers last year's bearing problem may not be on shift when the next one starts. A maintenance system that keeps readings, photos, parts and findings against the asset gives every shift the same history, so warning signs are recognized faster and repeat failures are easier to prove and fix.
Typical mistakes that delay the warning
Habits that hide damage
- Taking readings at different points or loads each time, so trends cannot be trusted
- Relying on a single handheld temperature reading once a shift
- Adding grease whenever a bearing sounds noisy, which can mask the problem and cause overheating
- Leaving warnings in a spreadsheet that the planner never sees
- Ordering the spare only after the bearing fails
Habits that find it early
- Marking each measurement point on the housing and using the same instrument and settings
- Combining vibration, ultrasound, temperature and grease condition
- Using a defined greasing quantity and recording it
- Raising a work order the moment a warning is confirmed
- Keeping a critical spare bearing and seals in stores
Deciding how fast to respond
| Situation | Risk level | Suggested response |
|---|---|---|
| One early ultrasound change, no other signs | Low | Check grease, retest within days, keep the point on watch |
| Defect frequency visible in vibration and rising | Medium | Order parts, plan the job for the next suitable stop |
| Vibration and temperature both climbing | High | Increase checks to every shift and prepare for an early stop |
| Noise, smoke from the seal or sudden heat | Critical | Stop the crusher safely and isolate it |
Involve operations early
Operators know when the crusher sounds different and when feed conditions changed. Give them a simple way to report concerns, such as a quick mobile form, and make sure someone responds. When operations and maintenance agree on response levels beforehand, planned stops become easier to approve and the cost of a short outage is accepted as better than an unplanned failure.
Linking crusher health to the rest of the plant
Upstream effects
Feed size, oversized rock and tramp metal affect shock load. Quarry blasting and loader practice influence crusher wear, so share bearing findings with quarry and operations teams.
Downstream effects
A crusher stoppage reduces stockpile levels, which affects kiln feed and raw mill supply. Knowing stockpile cover helps decide how long a planned stop can be.
Closing the loop after each replacement
After a bearing is replaced, compare what the teardown showed with what the signals said. If the vibration spectrum pointed to an outer race defect and the removed bearing confirms it, trust that signal more. If the bearing was damaged but no signal moved, add a measurement. Update baselines for the new bearing, review the greasing quantity and note any change to seals or housings, so the next cycle starts with better information and a longer warning period.
Frequently asked questions
What is the earliest sign of crusher bearing failure?
Ultrasound and high-frequency vibration changes usually appear first. Temperature and noise tend to follow later.
Is temperature monitoring enough?
No. Heat often rises late in the failure process, so combine it with vibration, ultrasound and lubrication checks.
How often should bearings be inspected?
Match frequency to criticality and trend. A tool like Oxmaint can schedule rounds and tighten them when readings climb.
Does over-greasing cause failures?
Yes. Excess grease raises temperature and can damage seals, so define quantity and interval per point.
How can I see this in a CMMS?
You can book a demo to walk through a crusher bearing workflow.
Stop learning about bearing damage from the stoppage
Plan the repair while the crusher is still running with Oxmaint.