One jammed case erector can idle a whole shift of pickers. Cartons stop arriving at the sealer, the conveyor behind it fills, the labeler waits, and the dock doors sit with trailers that should have loaded an hour ago. Packaging lines look simple from the floor, but they are chains of small machines where any single stop spreads in both directions. This guide covers maintenance for case erectors, sealers, labelers, and wrappers, and how Oxmaint organizes preventive work so high-volume lines keep moving.
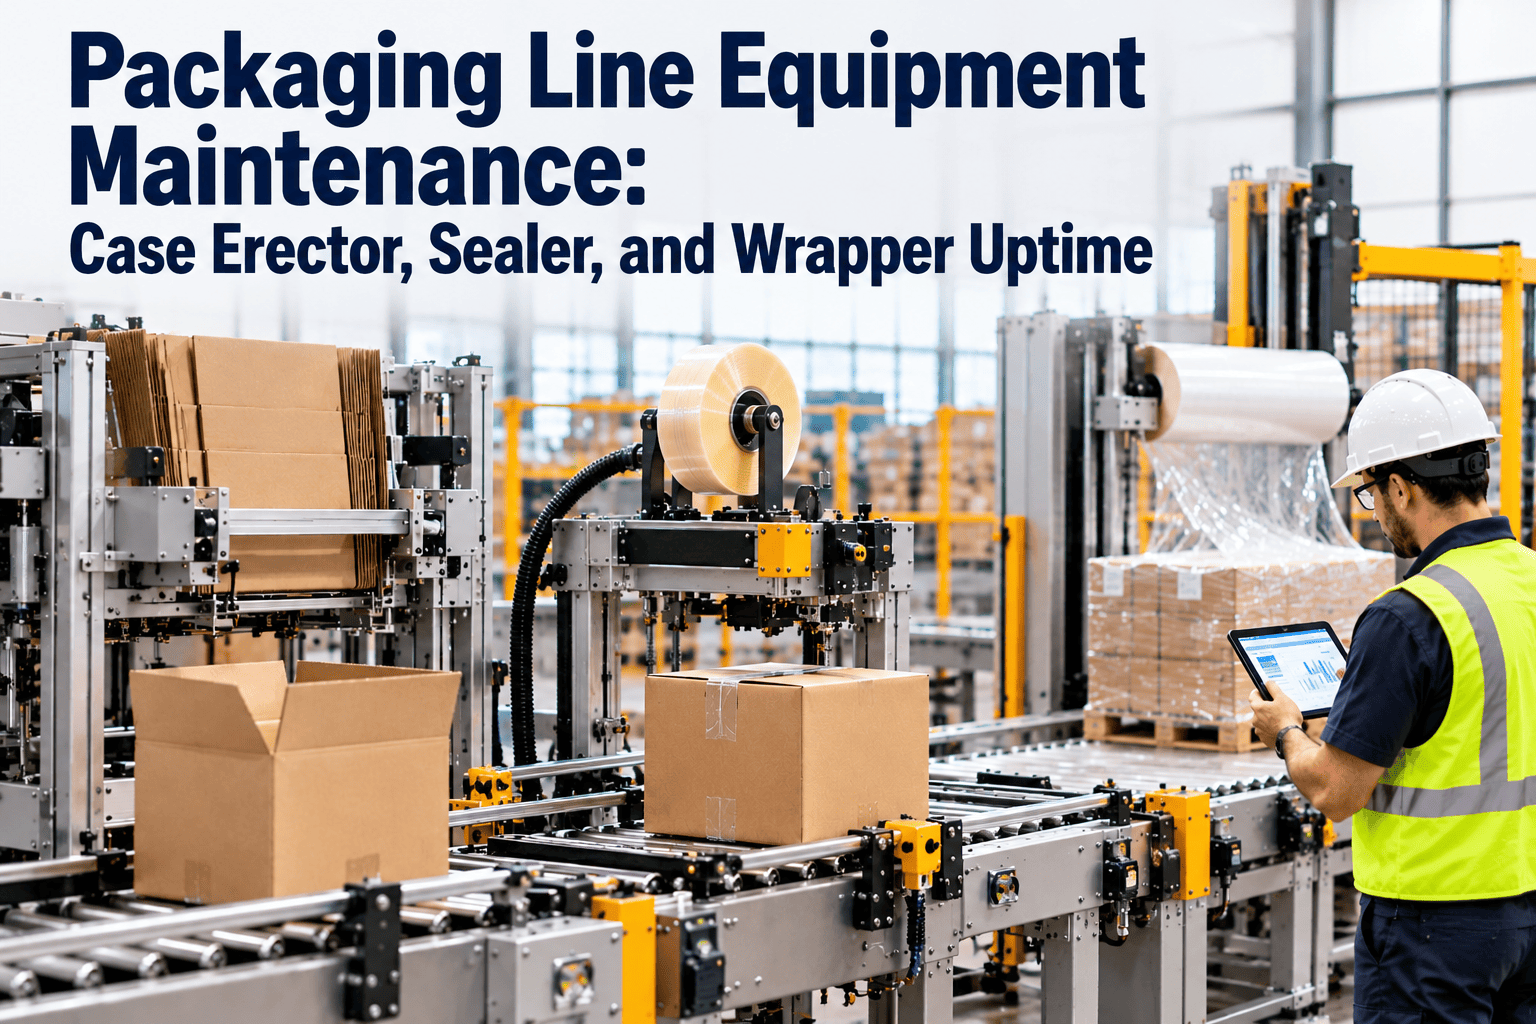
Packaging Line Equipment Maintenance: Case Erector, Sealer, and Wrapper Uptime
How One Stoppage Spreads Through a Packaging Line
- Conveyors back up and cartons accumulate.
- Pack stations wait for space to release product.
- Pick waves stall because totes cannot clear.
- Jam, sensor fault, glue failure, or tape problem.
- Operators clear and restart repeatedly.
- Small stops hide the real root cause.
- Sortation and shipping lanes run empty.
- Carrier cutoffs get missed.
- Overtime is used to catch up.
Because lines are tightly coupled, availability depends on the weakest machine rather than the average one.
Where Packaging Line Downtime Comes From
| Machine | Frequent problems | Typical root causes |
|---|---|---|
| Case erector | Misformed cases, jams, glue failures | Worn vacuum cups, dirty magazines, blocked glue nozzles, poor blank quality |
| Tape or glue sealer | Skipped seals, tape tails, jams | Dull blades, weak springs, worn drive belts, misadjusted case width |
| Print and apply labeler | Misprints, missed labels, no-read scans | Dirty print heads, worn rollers, sensor contamination, ribbon or label issues |
| Stretch wrapper | Film breaks, loose wraps, carriage faults | Film path wear, worn rollers, turntable issues, sensor faults |
| Conveyors and transfers | Stalls, noise, mistracking | Worn bearings, belt wear, chain stretch, lubrication gaps |
| Controls and sensors | Nuisance stops and false jams | Dust, loose wiring, misaligned photo eyes, damaged guards interlocks |
Micro-stops are the hidden loss
A line can look healthy in a daily downtime report while losing minutes to repeated brief stops. Capture them, even roughly, so patterns are visible.
Preventive Maintenance Plan by Machine
- Inspect vacuum cups and replace worn ones.
- Clean magazine, guides, and glue nozzles.
- Check pneumatic lines and fittings for leaks.
- Verify glue temperature, level, and filters.
- Confirm sensor alignment and guard interlocks.
- Check tape heads, blades, and springs.
- Inspect drive belts and rollers for wear.
- Verify side guides and case width adjustments.
- Clean adhesive and dust from the tape path.
- Test safety stops and covers.
- Clean print heads and platen rollers on schedule.
- Inspect applicator pads and tamp mechanism.
- Clean label and gap sensors.
- Check ribbon path, tension, and consumable stock.
- Verify barcode quality with a scan test.
- Inspect film rollers, carriage, and tension settings.
- Lubricate chains and bearings as specified.
- Check turntable or ring drive for smooth motion.
- Test photo eyes and load height detection.
- Confirm emergency stops and guarding.
Who Does What: A Layered Responsibility Model
Operator care prevents small problems
Operators see the machine all day. When they own simple cleaning and inspection tasks, technicians can focus on work that needs their skills.
Measuring Packaging Line Performance
Set availability targets for peak periods using your own baseline, because the right number depends on line design, shift pattern, and product mix.
From Stop Reasons to Root Causes
Consumables and Material Quality
- Inconsistent carton blanks cause misfeeds, so track supplier quality and complaints.
- Tape, hot melt adhesive, labels, and ribbons have shelf lives and storage requirements.
- Film quality affects breakage and load stability, so record film changes alongside wrapper faults.
- Changing a consumable brand without testing can create new failure modes.
- Store consumables to protect them from moisture, heat, and dust.
Condition-Based Maintenance Opportunities
| Signal | What it can indicate | Action |
|---|---|---|
| Rising motor temperature or current | Bearing wear, binding, or overload | Inspect drive train and lubrication |
| Increasing vibration or noise | Worn bearings or misalignment | Schedule inspection before failure |
| Longer cycle times | Sticking components or air supply issues | Check pneumatics and mechanical drag |
| Rising reject or misread rates | Dirty sensors or worn print components | Clean and recalibrate |
| More frequent micro-stops | Developing alignment or wear problem | Trend by machine and shift |
Spare Parts That Protect Uptime
- Stock fast-wearing parts such as vacuum cups, blades, belts, rollers, and sensors.
- Identify single-point-of-failure components with long lead times and hold critical spares.
- Record part usage against the machine, so reorder points follow real consumption.
- Agree response times with equipment vendors for major repairs.
- Review the parts list after every major failure.
Peak Season Readiness for Packaging Lines
Changeovers, Adjustments, and Setup Errors
| Changeover task | Failure it can cause | Control |
|---|---|---|
| Case size adjustment | Crushed cartons, skewed seals, jams | Marked settings and a sign-off checklist |
| Tape or glue settings | Open flaps or wasted material | Standard settings by case type |
| Label template change | Wrong or unreadable labels | Scan test before release |
| Wrap pattern selection | Unstable pallets or film breaks | Locked recipes by pallet type |
| Guard and sensor reset | Bypassed safety or nuisance stops | Verification step after every changeover |
Standard settings reduce guesswork
When every shift sets machines differently, maintenance chases faults that are really setup problems. Write down good settings, and train to them.
Packaging Line Safety and Lockout
- Use lockout and tagout for every adjustment or clearing task that exposes moving parts or stored energy.
- Check that guards, interlocks, and emergency stops are tested on a schedule and never bypassed.
- Pneumatic and spring-loaded mechanisms can move after power is removed, so release stored energy.
- Hot melt systems create burn risks, so use approved procedures for adhesive handling.
- Train temporary and seasonal staff on stop procedures before they touch the line.
Cleaning as a Maintenance Task
- Remove carton dust and debris from guides and sensors.
- Check consumables and loading paths.
- Look and listen for abnormal wear or noise.
- Clear adhesive and tape residue where it builds up.
- Note recurring stops for the next shift.
- Report damaged guards or loose fasteners.
Training and Knowledge Transfer
- Document troubleshooting steps for the five most common stops on each machine.
- Pair new technicians with experienced ones on the most failure-prone machines.
- Store manuals, wiring diagrams, and settings in the asset record, not in a drawer.
- Record lessons from each repair so the next technician starts with context.
- Cross-train operators on basic clearing and cleaning, with clear limits on what they should not touch.
Working With Equipment Vendors
When to Repair, Rebuild, or Replace Packaging Equipment
- Failures are isolated and parts are available.
- Repair cost is small against replacement.
- The machine still meets speed and quality needs.
- Wear is concentrated in a few major assemblies.
- The frame and controls are still sound.
- Downtime is rising but a full replacement is premature.
- Parts are obsolete or support has ended.
- Repeat failures cause line-wide stoppages.
- Volume or format changes exceed machine capability.
Cost history by asset makes this decision more objective, and it helps explain capital requests to finance.
How Oxmaint Supports Packaging Line Maintenance
Oxmaint is maintenance management software for plants, warehouses, and fleets. It organizes the work that keeps packaging equipment running.
- Asset hierarchy for the line, each machine, and key components, with history and documents.
- Preventive maintenance schedules by time or meter reading, with task lists for each machine.
- Work orders for corrective repairs, with priority, assignment, and parts used.
- Mobile checklists for operator care and technician inspections.
- Spare parts inventory with reorder points tied to usage.
- Reports on downtime, repeat failures, MTBF, MTTR, and PM completion.
Common Packaging Maintenance Mistakes
- Treating micro-stops as normal and never recording them.
- Relying on one technician's memory for machine knowledge.
- Skipping cleaning because it does not feel like maintenance.
- Replacing parts only after failure on machines that gate the whole line.
- Changing consumables without testing and without informing maintenance.
- Ignoring safety guards and interlocks that are bypassed during rushed shifts.
Weekly Packaging Maintenance Review Agenda
| Topic | Question to answer | Typical attendees |
|---|---|---|
| Top stop reasons | Which three causes cost the most time this week? | Line lead, maintenance lead |
| Open work orders | Which repairs block production or quality? | Maintenance supervisor |
| PM compliance | Which tasks were missed and what is the plan? | Maintenance planner |
| Parts and consumables | What ran short or arrived late? | Stores and purchasing |
| Upcoming volume | Which machines face the highest load next week? | Operations manager |
Linking Packaging Uptime to Dock and Delivery Performance
- Packaging output sets how quickly orders reach staging lanes and dock doors.
- Late packing compresses loading windows and increases pressure on drivers and dock crews.
- Label errors cause downstream sortation rejects and misrouted parcels.
- Reliable wrapping protects load integrity and reduces damage claims.
- Maintenance data shared with operations helps planners set realistic cutoffs.
Plan service windows around demand
Schedule planned downtime for the quietest windows in the day or week, and avoid starting major work before a known peak wave.
Checklist: Is Your Packaging Maintenance Program Ready?
- Every machine on the line is registered with a unique asset record.
- Preventive tasks exist for each machine, with clear intervals and instructions.
- Operators complete and record start-of-shift checks.
- Stop reasons are recorded, reviewed, and ranked weekly.
- Critical spares are identified, stocked, and reviewed after failures.
- Technicians can see history, manuals, and settings from a phone or tablet.
- Lockout procedures and guard checks are documented and audited.
Reading Downtime Data Without Fooling Yourself
- Separate planned stops, such as changeovers and breaks, from unplanned stops, so availability is not distorted.
- Count events as well as minutes, since many short stops can cost more than one long one.
- Compare machines on the same product mix and shift pattern before drawing conclusions.
- Check whether a machine is stopping because of its own fault or because the machine next to it is blocked.
- Review operator comments alongside codes, because the real cause is often in the note.
- Recheck results after each fix, since improving one weak point exposes the next.
Start simple, then refine
Five or six clear reason codes recorded consistently are better than fifty codes that operators ignore. Expand the list only when a category becomes too broad to act on.