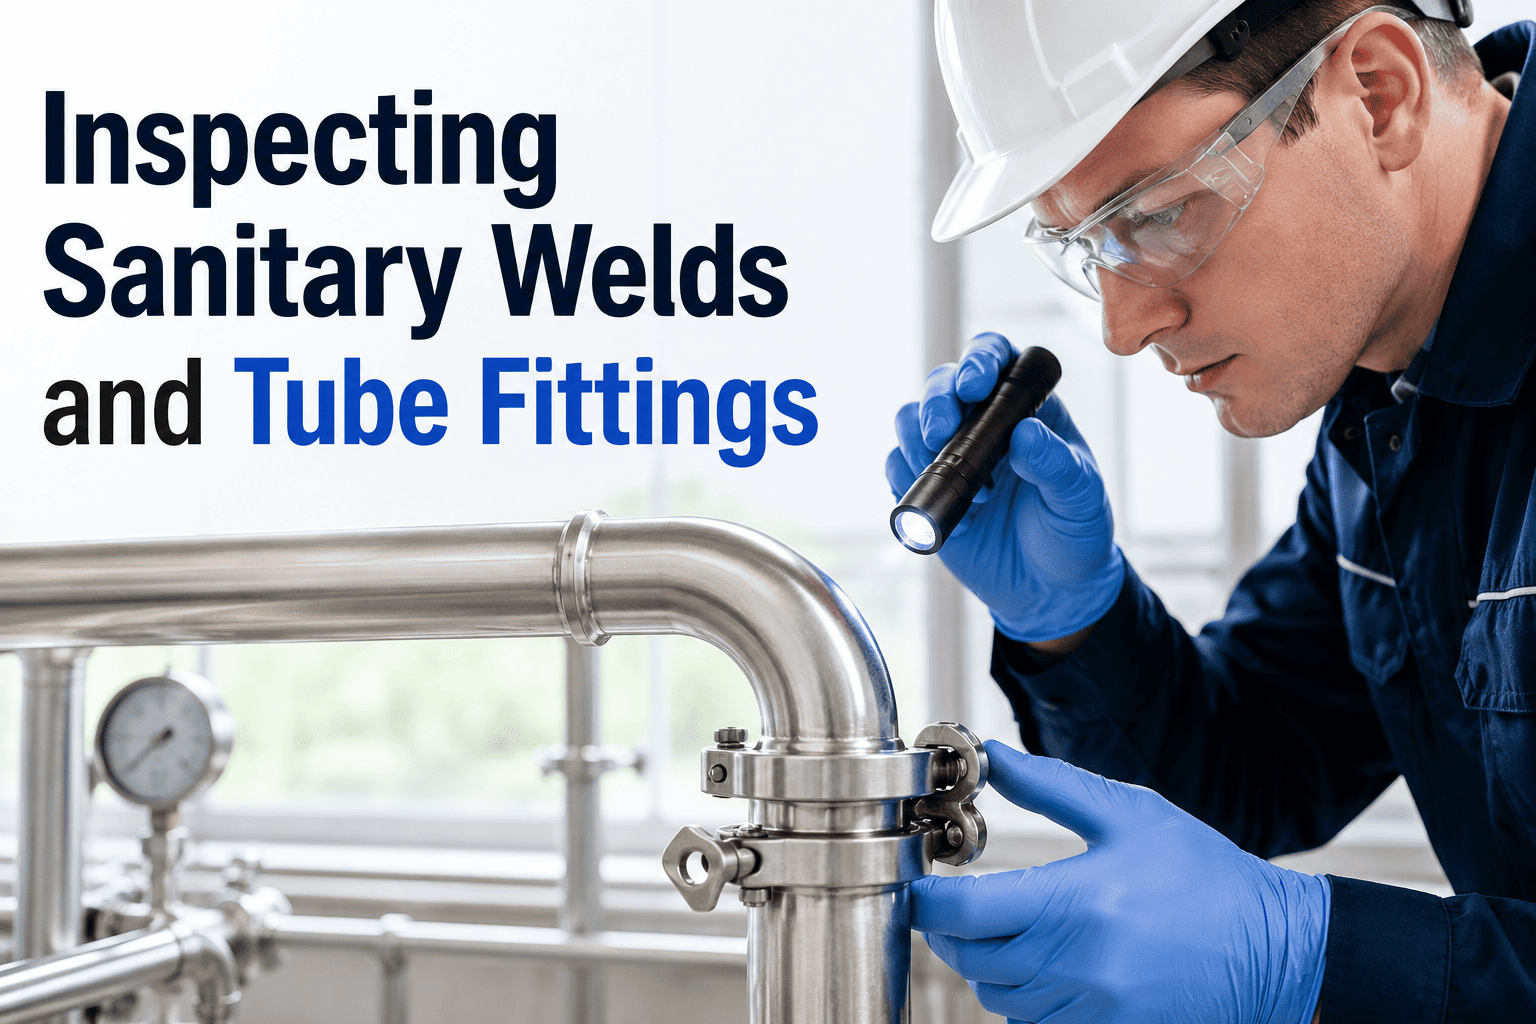
A sanitary weld looks fine from the outside and still fails an audit from the inside. Underneath a smooth cap, a single crevice, pit, or misaligned bore can trap product residue that no CIP cycle ever reaches, and that gap is invisible until a borescope, a swab test, or a recall finds it first. Tube fitting integrity is just as fragile — a ferrule torqued wrong or a gasket past its cycle count reopens the exact contamination path the weld was supposed to close. Plants that track weld maps, borescope results, and fitting inspection cycles on a structured schedule catch these failures before an auditor does, which is why sanitation-focused maintenance teams start a free trial on their sanitary piping network first.
Equipment Sanitation Field Guide
Inspecting Sanitary Welds and Tube Fittings Before They Fail an Audit
Cracked weld detection, borescope scheduling, tube fitting torque verification, and a CMMS-tracked inspection cadence built for 3-A and ASME BPE compliant piping.
0.8 µm
Maximum surface roughness (Ra) allowed on a sanitary weld under 3-A criteria
100%
Of critical product-contact welds recommended for borescope verification
60+
Orbital welds a single operator can complete in a day at sanitary quality
0.5 mm
Typical maximum step mismatch allowed inside a sanitary tube joint
Why a Weld That Passes Visually Can Still Fail Sanitation
A structural weld only has to hold pressure. A sanitary weld has to do that and stay clean under repeated CIP and SIP cycles, which means the inside of the joint matters more than the outside. Welds with crevices, pits, folds, or cracks have to be cut out and rewelded rather than patched, and a purge gas failure leaves the tube interior dark, crusty, and effectively impossible to sanitize. None of that shows up on a walk-by inspection.
Tube fittings carry the same risk from a different direction. Regulatory frameworks limit internal step mismatch to roughly half a millimeter and require full weld penetration with no concavity that can trap product, and a clamp fitting that skips its gasket replacement cycle reopens that same trap without a weld ever being touched. Teams ready to put both failure modes on one inspection record book a demo and walk through their own piping isometrics.
A weld can look perfect to the eye and still hold a crevice a borescope would catch in seconds.
Five Defects Inspectors Look For Inside the Joint
Sanitary weld failures repeat in a small, predictable set of patterns. Knowing what each one looks like on a borescope feed is what turns a routine inspection into an actual catch.
DEFECT 1
Crevices and Undercut
A narrow gap at the weld root where the two tube ends never fully fused. Product and cleaning solution both bypass it, leaving residue behind after every CIP cycle.
DEFECT 2
Pitting and Porosity
Small voids in the weld bead caused by contamination or gas entrapment during welding. Each pit is a microscopic harborage point invisible without magnification.
DEFECT 3
Internal Misalignment
A step or ledge where the tube ID does not line up across the joint. Flow catches on the ledge, product accumulates, and CIP flow can not clear it.
DEFECT 4
Heat Tint and Discoloration
A dark, crusty interior surface from an inadequate argon purge during welding. The oxidized layer corrodes faster and resists sanitation even when the geometry is sound.
DEFECT 5
Gasket and Ferrule Wear
A compressed, cracked, or under-torqued gasket at a clamp fitting reopens the same crevice risk as a bad weld, without any welding involved at all.
TOOL
Borescope as the Standard Check
A borescope run through the tube ID is the fastest way to confirm all five defect types at once, which is why it is the default verification step after every critical weld.
Where Sanitation Programs Actually Break Down
The weld quality is usually not the weak point. The record-keeping around it is. These four gaps show up again and again during audits and recall investigations.
Borescope Results Never Attached to the Weld
A borescope inspection happens, gets approved verbally, and the footage or photo never makes it into a searchable record. When an auditor asks for proof on weld 47, nobody can find it.
Weld Maps That Live Only on Paper
Fabrication drawings with numbered weld locations are common, but the inspection status per weld rarely gets tracked past the installation date. Nobody knows which welds are due for re-verification.
Gasket Replacement Running Past Cycle Count
Clamp fitting gaskets have a defined service life under repeated CIP exposure. Without a tracked cycle count, replacement becomes reactive, usually after a leak or a failed swab test.
Material Traceability Detached From the Asset
Heat lot numbers and material test reports get filed by the fabricator, not by the line. A recall investigation loses days reconstructing which tube run used which certified material.
Every one of these gaps has the same fix: attach the inspection record directly to the weld or fitting asset instead of a folder, so status and history are one lookup away. That is the discipline sanitation leads install when they start a free trial on a single piping run.
A gasket has a service life. Left untracked, it becomes the crevice the weld inspection was never checking for.
How OxMaint Puts Weld and Fitting Records on One Asset
OxMaint treats every tube run as a hierarchy: line, weld joint, and fitting, each carrying its own inspection history, calibration record, and replacement schedule under one searchable asset.
01
Weld Map Digitization
Every numbered weld from the fabrication isometric becomes its own asset record, so inspection status is visible weld by weld instead of buried in a drawing set.
02
Borescope Record Attachment
Photos and footage from each borescope pass attach directly to the weld asset with a pass or fail status, ready for an auditor to pull in seconds.
03
Gasket and Ferrule Cycle Tracking
Clamp fittings carry a CIP cycle counter that triggers a replacement work order automatically before the gasket exceeds its rated service life.
04
Material Traceability Linking
Heat lot numbers and material test reports attach to the tube run at fabrication, so a recall investigation traces the exact material in minutes, not days.
05
Re-Inspection Scheduling
High-risk welds and fittings get a recurring inspection interval based on CIP frequency, product type, and prior findings instead of a fixed calendar guess.
06
Audit-Ready Export
Every weld and fitting record for a line, a date range, or a full plant exports as one document, replacing the manual binder pull before an inspection.
Paper Weld Logs vs an Asset-Linked Inspection Record
The gap between a paper weld log and a CMMS-tracked record is not effort, it is recoverability. When an auditor or a recall investigator asks a question, the record either produces an answer in minutes or it does not exist at all.
What Plants See After Structuring This Inspection Program
Plants that move weld and fitting inspection onto a tracked asset record report a consistent pattern: fewer repeat findings, faster audits, and gasket failures caught before they become leaks.
70%
Fewer repeat weld findings
Scheduled re-inspection catches drift before the next audit cycle instead of after it.
90%
Faster audit document pull
Weld and fitting records export by date range instead of a manual binder search.
3x
More gaskets caught pre-failure
Cycle-count triggers replace gaskets ahead of the leak instead of reacting to it.
8 mo
Typical payback window
Driven by reduced rework, fewer corrective actions, and recovered engineering hours.
Frequently Asked Questions
How often should sanitary welds be re-inspected
High-risk welds on frequent CIP lines typically get re-checked on a shorter interval than low-traffic joints. The right cadence depends on product type, cleaning frequency, and prior findings, which a tracked schedule can adjust automatically.
Does OxMaint store borescope footage on the weld record
Yes. Photos or footage from each borescope pass attach directly to the weld asset alongside a pass or fail status, so the evidence is retrievable without searching separate files during an audit.
Can gasket replacement be triggered automatically
Yes. A CIP cycle counter on each clamp fitting generates a replacement work order once the gasket approaches its rated service life, avoiding the reactive replace-after-leak pattern most plants fall into.
What counts as a rejectable sanitary weld defect
Crevices, pits, folds, cracks, internal misalignment beyond tolerance, and heat tint from an inadequate purge all count as rejectable defects requiring the weld to be cut out and redone under standard sanitary criteria.
How does multi-site weld tracking work across plants
Each plant's weld and fitting records roll up into one portfolio view, so a corporate quality team can compare inspection status and open findings across every site without visiting each one.
Book a demo to see a live portfolio.
Decision Point
Stop Finding Out About Bad Welds During an Audit
Put every sanitary weld and tube fitting on one tracked asset record, with borescope evidence, gasket cycles, and material traceability attached from day one.
Weld-level inspection tracking
Live in days, not months
Multi-site portfolio view
Audit-ready exports
Borescope evidence attached per weld
Automated gasket cycle tracking
Full heat lot and material traceability