surface-grinder-maintenance-checklist-for-cnc-machine-shops

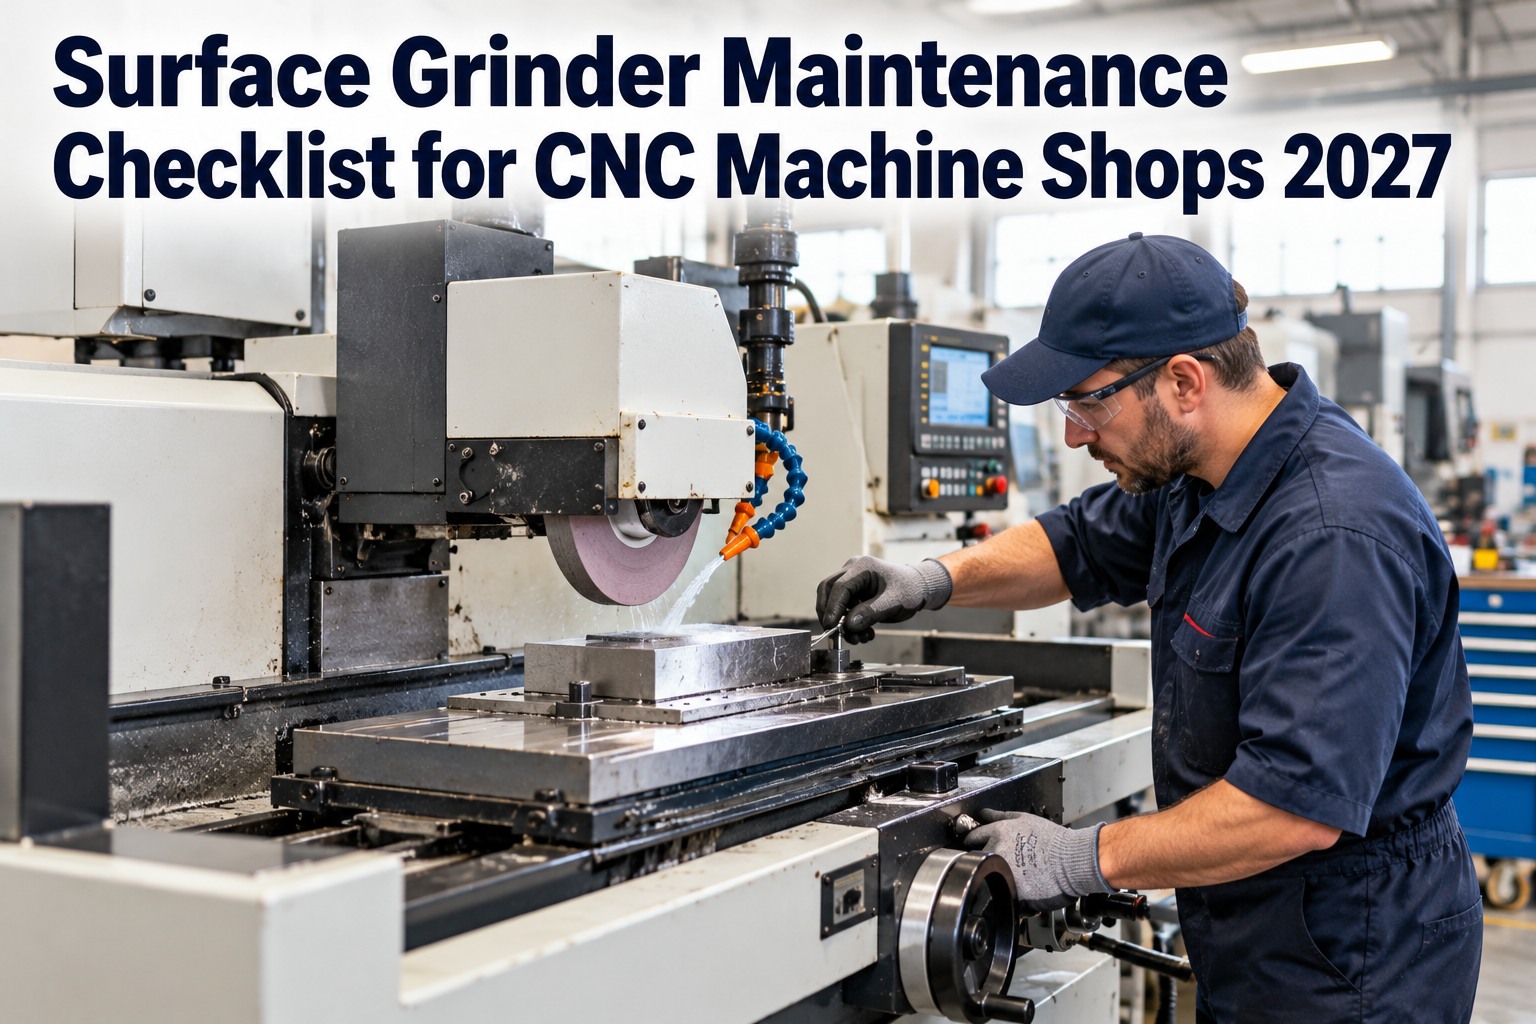
Surface Grinder Maintenance Checklist for CNC Machine Shops 2027


A surface grinder's whole job is finish and size held to tenths of a thousandth  so it doesn't fail loudly, it fails on the part. The first sign of trouble isn't a breakdown, it's chatter marks, taper, or a burned surface coming off the wheel. And nearly all of it traces to three things: a wheel that's out of balance or glazed, a spindle losing its precision, or coolant too dirty to do its job. This checklist keeps those in spec so the finish stays in spec — and OXMAINT AI, the AI-powered maintenance management software, schedules the PM, logs the surface-finish checks and raises a work order the moment quality drifts.

Production Equipment Maintenance · Surface Grinder Checklist · 2027

Surface Grinder Maintenance Checklist for CNC Machine Shops

A grinder tells you it needs attention through the part, not an alarm — chatter, taper, burn. This checklist keeps the wheel, spindle, ways and coolant in spec so the surface finish stays there, with OXMAINT AI tracking the PM and the quality readings that reveal a drift first.

IN SPEC
Smooth finish · size held
CHATTER
Vibration marks · scrap

The Part Is the Gauge — Read It First

On a grinder, the quality of the work is the condition monitor. A finish that drifts off, a size that wanders or a scorch mark is the machine telling you something's out of spec before any sensor would — which is why surface-finish and dimensional checks belong in the maintenance program, not just the QC booth. Catch the defect's signature and you know which part to service. Start free and log surface-finish and size checks against each grinder in OXMAINT AI.

Defect on the part
Usual cause
Where to look
Chatter marks
Wheel imbalance, worn spindle, loose setup, vibration
Balance & dress wheel; check spindle & mounting
Burn / discoloration
Glazed wheel, too little coolant, wrong wheel/feed
Dress the wheel; check coolant flow & concentration
Taper / out of flat
Way wear, misalignment, thermal drift, worn spindle
Check ways & geometry; warm up; inspect spindle
Poor finish / scratches
Dirty coolant, dull wheel, contamination in the loop
Service coolant filtration; dress or change wheel

Defect-to-cause links are a general troubleshooting guide; the real cause on any machine depends on the grinder, wheel, material and setup. Confirm before acting.

Three Systems Decide the Finish

Nearly every grinding defect comes back to one of three systems. Keep these in spec and the machine holds finish and size; let any one slip and it shows up on the part. The checklist below is built around them. Book a demo to map these systems to their PM in OXMAINT AI.

Wheel
Balance and dressing keep the cutting face true and open. An unbalanced or glazed wheel is the number-one source of chatter and burn.
Spindle & Ways
Spindle precision and clean, lubricated ways hold the geometry. Wear here shows as taper, out-of-flat and a creeping loss of size control.
Coolant
Clean, correctly mixed coolant cools the cut and flushes swarf. Dirty or weak coolant means burn, poor finish and scratches.

The Surface Grinder Maintenance Checklist

Work the groups by system, then the daily and periodic checks. Tick each item as it's done; in the OXMAINT AI software the same checklist runs on a handheld and files itself as a time-stamped record against the machine. Start free and run this checklist from any phone in OXMAINT AI.

01Grinding Wheel — Balance & Dress
02Spindle, Ways & Geometry
03Coolant & Filtration
04Daily, Safety & Quality Checks
Chatter DecoderWhen Chatter Appears, Work It in This Order

Chatter is the grinder's most common complaint — and it's almost always one of a few things. Work the cheap, likely causes first before chasing the spindle.

1
Re-balance and re-dress the wheel — the most common cause by far
2
Check the workpiece setup, magnet and fixturing for looseness
3
Look for external vibration and loose machine mounting
4
Only then inspect the spindle bearings for wear

A Grinder Doesn't Alarm — It Makes a Scrap Part Instead.

By the time a finish drifts off, the wheel's been glazing, the coolant's been loading or the spindle's been wearing for a while. The only way to stay ahead is to run the PM on schedule and watch the finish as a maintenance signal. The OXMAINT AI maintenance management software keeps the PM on track and turns a logged out-of-spec reading into a work order.

The PM Schedule by Interval

Grinder PM layers quick daily habits over periodic wheel, coolant and geometry work. Here's the core cadence — tighten it for high-precision or high-duty work, and follow the machine OEM's intervals. Start free and load this schedule onto each grinder in OXMAINT AI.

Daily
Check coolant level and flow, confirm way lube, dress the wheel as needed, wipe down and clear swarf, and spot-check a part's finish and size.
Weekly
Balance the wheel, test coolant concentration and pH, clean filters, and check spindle for heat, noise and vibration.
Monthly
Recharge or change coolant and clean the tank, inspect ways, wipers and lube system, and check worktable travel and backlash.
Annual
Full geometry check — flatness, squareness, parallelism — spindle inspection, and calibration of controls and gauging.

How OXMAINT AI Keeps a Grinder in Spec

A grinder rewards a program that runs the PM on time and treats the surface finish as a signal. The OXMAINT AI maintenance management software schedules the wheel, spindle and coolant work, logs the quality checks, and raises a work order the moment a reading drifts out of spec. Book a demo to see the full grinder workflow in OXMAINT AI.

PM SCHEDULE
Daily-to-annual wheel, spindle, ways and coolant tasks scheduled with overdue escalation, so nothing slips.
QUALITY LOG
Surface-finish and size checks logged against the machine, so a drift is visible as a trend, not a surprise.
DRIFT → WO
An out-of-spec reading or overdue dressing raises a work order automatically, with the machine attached.
DEFECT HISTORY
Chatter, burn and taper events logged with their cause, so recurring problems are traced to a root cause.
SPARES & WHEELS
Wheels, dressing diamonds, filters and coolant tracked in inventory, so a change isn't waiting on a part.
MACHINE RECORD
Every PM, reading and repair tied to the grinder — ready for capability review and audits.

Expert Review

This checklist is a general maintenance framework for surface and cylindrical grinders. The exact wheel, balancing, dressing, coolant, lubrication, geometry and calibration procedures, intervals and tolerances for any machine come from the grinder and wheel manufacturers and your quality system, which take precedence over anything here. Grinding-wheel handling and mounting, machine guarding and lockout follow the relevant safety standards and must be done by trained personnel. The defect-to-cause links are a troubleshooting guide, not a diagnosis — confirm the real cause on the machine before acting. OXMAINT AI schedules the PM, logs the quality checks, raises the work orders and keeps the machine history; it supports the maintenance and quality program your shop and reliability teams own, not OEM guidance, metrology or operator judgement.

Frequently Asked Questions

What causes chatter on a surface grinder?
Chatter — regular vibration marks on the finish — is most often an unbalanced or glazed grinding wheel, so re-balance and re-dress first. If it persists, check the workpiece setup and fixturing for looseness, look for external vibration and loose machine mounting, and only then inspect the spindle bearings. Working the cheap, likely causes first saves chasing the spindle unnecessarily. OXMAINT AI logs the defect and the fix so patterns surface. Book a demo to track chatter and its causes in OXMAINT AI.
How often should a grinding wheel be balanced and dressed?
Balance after every wheel mount and size change, and whenever chatter appears; dress whenever the wheel glazes, loads or loses its cutting edge — often daily in production, and always before precision work. The exact frequency depends on the wheel, material and finish required, following the wheel maker's guidance. Tracking dressing as a scheduled task keeps it from being skipped. Book a demo to schedule wheel dressing in OXMAINT AI.
Why does grinding coolant filtration matter so much?
Coolant cools the cut to prevent burn and flushes swarf out of the grinding zone. When it gets dirty, loaded with fines, or weak in concentration, you get burn, poor finish and scratches from recirculated debris — defects that look like a wheel or spindle problem but are really coolant. Clean filtration and correct mix are among the cheapest ways to protect finish. Book a demo to track coolant service in OXMAINT AI.
How do you know if a grinder spindle is worn?
A worn spindle shows up as play, unusual noise, heat or vibration, and on the part as persistent taper, out-of-flat or a loss of size control that balancing and dressing don't fix. Because spindle work is the most involved repair, it's worth ruling out wheel, setup and coolant causes first — then inspecting the spindle bearings. Trending the symptoms tells you when it's approaching a rebuild. Book a demo to trend spindle condition in OXMAINT AI.
How does a CMMS help maintain grinders in a machine shop?
It schedules the wheel, spindle, ways and coolant PM so nothing slips, logs surface-finish and size checks as a maintenance signal so a drift shows up early, and raises a work order automatically on an out-of-spec reading or overdue task. It also keeps defect history — chatter, burn, taper with their causes — tied to each machine for capability review and root-cause work. Book a demo to see the full grinder workflow in OXMAINT AI.

Keep the Wheel True, the Coolant Clean and the Finish in Spec.

Run surface grinder maintenance on the OXMAINT AI maintenance management software — scheduled wheel, spindle and coolant PM, surface-finish and size checks logged as a signal, a chatter and defect history traced to root cause, and a work order on every drift. Protect the finish, one tracked check at a time.
Share This Story, Choose Your Platform!