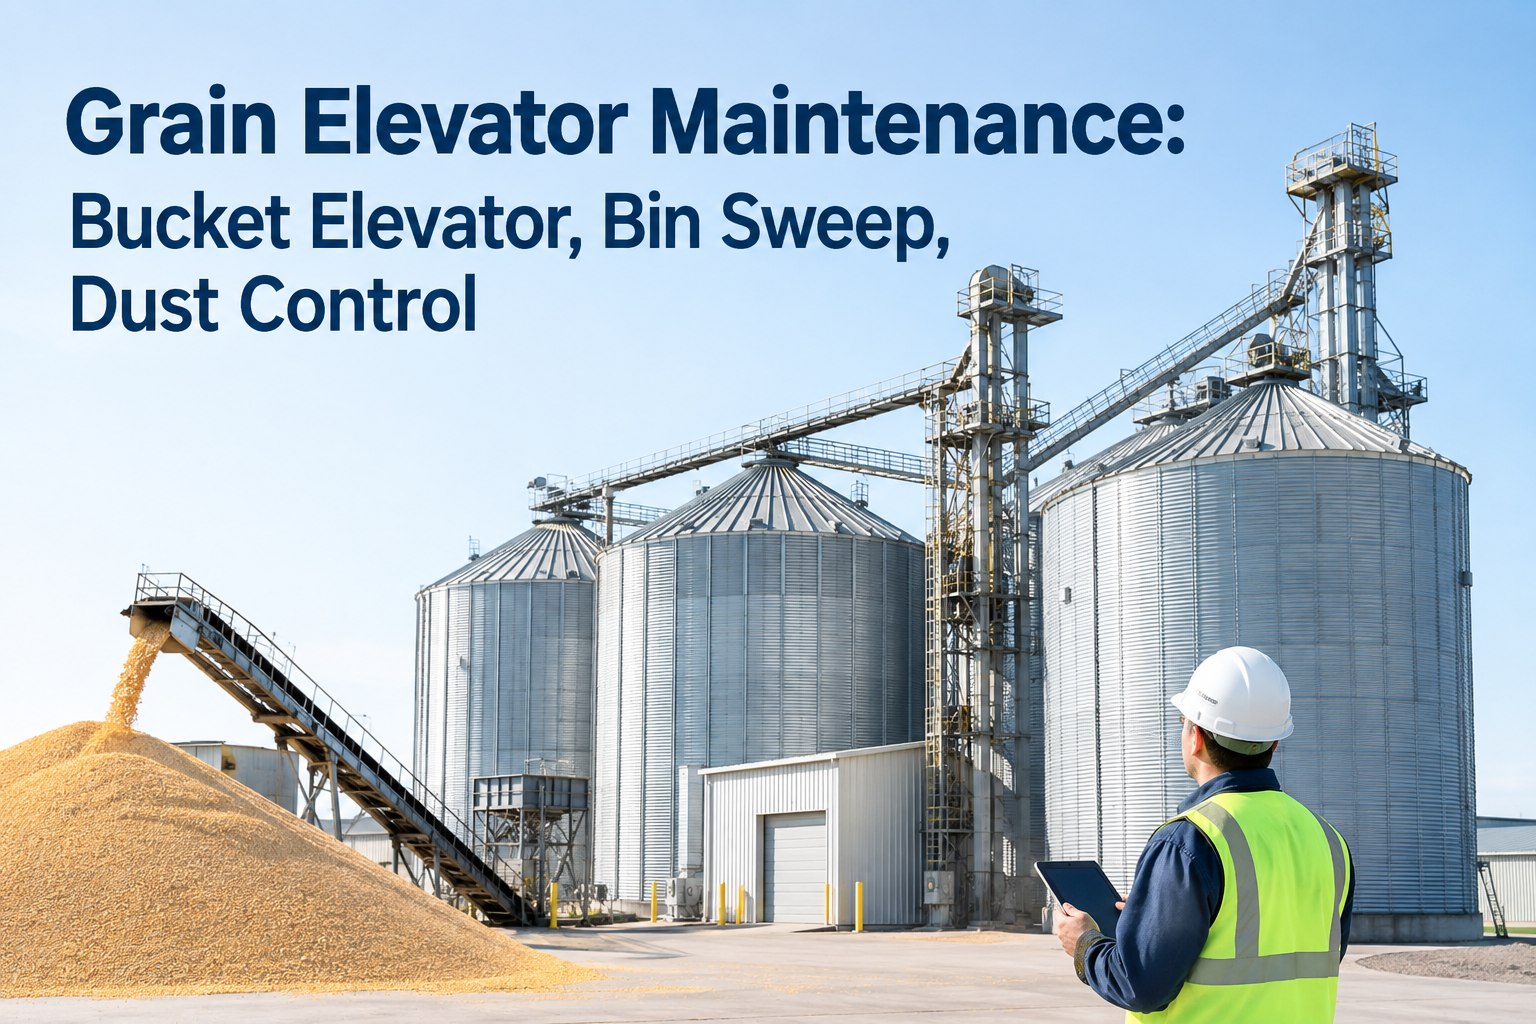
Grain Elevator Maintenance: Bucket Elevator, Bin Sweep, Dust Control

Connect with Industry Experts, Share Solutions, and Grow Together!

Join Discussion Forum
grain-elevator-maintenance-bucket-elevator-bin-sweep-dust-control

In a grain elevator, maintenance and safety aren't two programs — they're the same program. A misaligned belt rubbing its casing, an overheating bearing, a boot flooded with grain: these aren't just reliability problems, they're ignition sources in a building full of the most explosive fuel in food manufacturing. Grain dust ignites at concentrations you can't see, and it doesn't take much — NFPA has long held that dust just 1/32 inch deep over 5% of a surface presents a significant explosion hazard, and OSHA caps priority-area accumulation at 1/8 inch for exactly this reason. The U.S. still averages around eight grain-dust explosions a year, and the 1998 DeBruce elevator blast that killed six is the reminder of what's at stake. This guide covers the full maintenance program — bucket elevator alignment, bin sweeps, dust control and the NFPA 61 / OSHA 1910.272 discipline that ties them together — and how OxMaint's maintenance management software runs and documents it. Start free or book a demo.

Food Manufacturing · Grain Handling · Explosion Safety · CMMS 2026

Grain Elevator Maintenance: Bucket Elevator, Bin Sweep & Dust Control

Every maintenance task in a grain leg is also an ignition-control task. Align the belt, cool the bearing, clear the boot, hold the dust below the line — and document every one, because the inspection record is the compliance.

~8 / yr
grain-dust explosions in the U.S., per Purdue tracking
1/8 inch
OSHA dust-accumulation cap in priority housekeeping areas
≤300 MΩ
max surface resistance for conductive elevator belts (OSHA)
3 monitors
alignment, bearing temp & belt speed — the ignition-control trio

The Ignition Triangle Lives Inside the Bucket Elevator

The bucket elevator — the "leg" — is where primary explosions start, because it concentrates all three explosion ingredients in one enclosed housing: a cloud of grain dust (fuel), oxygen, and moving steel that can spark or overheat (ignition). Maintenance can't remove the fuel or the oxygen, so the entire discipline targets the third leg — every task below exists to keep an ignition source from ever forming. Sign up free and OxMaint schedules each of these as a documented, certifiable inspection.

Belt / Pulley Alignment
A belt tracking off-center rubs the casing and generates frictional heat fast. Monitor alignment at head and tail; a rub block or alignment sensor alerts or trips before it ignites. OSHA requires prompt correction of misaligned belts on inside legs.
Bearing Temperature
A failing or under-lubricated bearing overheats enough to ignite dust. Temperature (or vibration) monitoring on head, boot and inside-casing bearings is the early warning — and overheated bearings must be corrected or removed from service promptly.
Belt Speed / Slippage
A slipping belt on the drive pulley builds heat at the lagging and signals a flooded boot or drive fault. Speed monitoring catches slippage before friction becomes ignition.
Sensors give a false sense of security if they're never tested — like a smoke alarm with a dead battery, a bearing or alignment sensor can be silently nonfunctional. Testing the monitors is itself a scheduled PM task, not a set-and-forget install.

The Bucket Elevator PM Checklist

Beyond the three monitors, the leg needs a hands-on inspection rhythm. Note the flooded boot at the top of the list: feeding grain faster than the buckets can clear it is the single most common mechanical failure in a grain leg, straining the belt and drive. Book a demo to see these scheduled per leg.

Component
Watch-For
PM Task
Cadence
Boot
Flooding, grain buildup, take-up drift
Clear boot pool, verify choke-free feed, check take-up tension via access door
Daily→Weekly
Belt & Buckets
Cracked/missing buckets, loose bolts, belt wear
Inspect all buckets each season pre-harvest; check belt tension & conductive-belt integrity (≤300 MΩ)
Seasonal + Weekly
Head Pulley & Lagging
Lagging wear, pulley grooving, discharge throat wear
Inspect lagging condition (OSHA-named item), pulley face & throat via head access door
Scheduled reg.
Drive & Reducer
Coupling wear, reducer oil, motor heat
Gear-reducer oil check/sample, coupling & belt-drive inspection, motor current/temp
Monthly→6-mo
Casing & Spouting
Holes, leaks, dust escape at seams
Patch holes in casing/spouting promptly to stop dust leakage — a named OSHA item
Weekly
Bearings (all)
Heat, noise, lubrication state
Lubricate to spec; verify temp/vibration monitors are live and tested
Per mfr / Weekly

If It Isn't Documented, It Didn't Happen — and OSHA Agrees.

OSHA 1910.272 doesn't mandate a PM frequency — it mandates that you can demonstrate the program works, and that every inspection carries a certification record: the date, the name of the person who inspected it, and the equipment's serial or identifier. A verbal "we check it weekly" is not compliance. OxMaint produces that certification record automatically for every scheduled inspection, so the audit trail is a by-product of doing the work.

Bin Sweeps: The Confined-Space, Life-or-Death PM

Bin sweep augers finish emptying a bin the gravity flow leaves behind — and maintaining them means entering a grain bin, one of the most dangerous confined spaces in any industry. Here the PM procedure is inseparable from the entry procedure: no sweep maintenance happens without lockout/tagout and permit-required confined-space protocol first. Sign up free to attach LOTO and entry permits to every bin task.

1
LOTO & Entry Permit First
Zero-energy verified, permit-required confined-space entry authorized, atmosphere tested, attendant posted — before anyone steps in.
2
Auger Flighting & Wear
Inspect sweep flighting for wear (worse with abrasive grains), check for bent sections and worn wear-shoes.
3
Drive & Guards
Verify the sweep drive, backstops and all guarding — the moving parts that make bin entry lethal if energized.
4
Bin Floor & Cleanout
Clear residual grain, check aeration floor and sump, remove crusted/out-of-condition grain that fouls the sweep.

Dust Control: Attack the Fuel Before It Accumulates

If maintenance controls ignition, dust control removes the fuel — and the two together are what actually prevent an explosion. Housekeeping isn't cosmetic here; OSHA names floors within 35 feet of inside bucket elevators as priority areas where dust can't exceed 1/8 inch. A written, documented housekeeping schedule is itself a compliance requirement. Book a demo to schedule and log housekeeping as PM.

Keep Collection Working
Filter collectors, cyclones and aspiration keep airborne dust below the explosive limit. Monitor filter pressure-drop; correct any collector running below designed efficiency promptly.
Reduce Dust at the Source
Choke-feed transfer points, dust-tight enclosures, and minimized free-fall of grain cut emissions before they become accumulation.
Documented Housekeeping
Written cleaning schedule, priority areas held under 1/8 inch, explosion-proof vacuums and grain vacs — and every clean-down dated and logged.
Seal the Leaks
Patch holes in spouting, casings, augers and drag-conveyor casings so dust never escapes to settle on ledges and beams.

Know Your Standards: NFPA 61, 68 & 69

Grain-handling explosion protection sits on three NFPA standards plus the OSHA rule, and a Dust Hazard Analysis (DHA) is what determines which protections your specific equipment needs. Here's the shorthand. Sign up free and put your DHA recommendations on a tracked schedule.

NFPA 61
Prevention of fires & dust explosions in agricultural and food-processing facilities — the governing standard for raw grain, driving the DHA.
NFPA 68
Deflagration venting — sizing explosion-relief vents, generally applied to processed grains and indoor legs.
NFPA 69
Explosion prevention systems — suppression and isolation methods, applicable to both raw and processed grain.
OSHA 1910.272
The grain-handling standard — housekeeping limits, conductive belts, inspection access, and the certification-record requirement.

Paper / Reactive vs. OxMaint Grain-Handling Program

A binder of inspection sheets is the traditional approach — and it's exactly what fails an audit when a sheet is missing or a sensor test was skipped. Here's what changes when the program lives in a CMMS. Start free and put one leg on a documented program this week.

Element
Paper / Reactive
OxMaint Program
Ignition monitors
Installed, rarely tested
Sensor-test PM scheduled & logged
Certification record
Handwritten, easily lost
Auto-generated: date, name, equipment ID
Housekeeping
Done when someone remembers
Scheduled, dated, priority-area tracked
Bin entry
LOTO on a separate clipboard
Permit & LOTO attached to the work order
Overheated bearing
Noticed on the next round
Monitor alert opens an immediate work order
Audit readiness
Days assembling the binder
Full inspection history on demand

What OxMaint Gives the Grain Facility

OxMaint runs the whole grain-handling program — the three monitors, the leg PM, bin-sweep safety, dust housekeeping and the certification trail — as one documented system, so maintenance and explosion-safety compliance are the same effort. Here's the concrete mapping. Book a demo to see it on your facility.

Certification-Record Inspections
Every scheduled inspection captures date, inspector name and equipment ID automatically — the exact record OSHA 1910.272 requires.
Hazard-Monitor Testing
Alignment, bearing-temp and belt-speed sensors put on a test-and-verify schedule so a dead sensor is caught, not trusted.
Per-Leg PM Schedules
Boot, belt, buckets, head pulley, lagging, drive and casing each carry their own tasks at daily, weekly, seasonal and annual cadence.
LOTO & Confined-Space Permits
Bin-sweep and bin-entry work orders carry the lockout and permit-required entry steps, so the safety procedure runs before the maintenance.
Housekeeping as Scheduled PM
Priority-area cleaning dated and logged against the 1/8-inch limit — turning documented housekeeping from a binder into a workflow.
Alert-to-Work-Order
An overheated bearing or misaligned belt from the monitoring system opens an immediate corrective work order for prompt correction.

Use this program plus OxMaint to run bucket-elevator, bin-sweep and dust-control maintenance as one explosion-safety discipline — keeping ignition sources from forming, dust below the line, and a certification record for every inspection that stands up to OSHA and NFPA scrutiny. Try OxMaint free or book a demo to see it on your elevator.

"

We ran our legs off paper inspection sheets in a binder, and the problem wasn't that we didn't do the work — it was that we couldn't always prove it. A regulator asked for the certification records on our head-house bearings and it took us two days to assemble what should have been a two-minute pull. Worse, we found two bearing-temp sensors that had been dead for months — nobody was testing the testers. We moved the whole program into OxMaint: every inspection now auto-logs the date, the tech and the equipment ID, the sensor tests are scheduled like any other PM, and bin-sweep work orders won't proceed without the LOTO and entry permit attached. Our housekeeping is dated against the priority-area limit. When the next audit came, the records were one click. And we sleep better knowing the monitors are actually alive.

Facility Manager · Regional Grain Terminal

Frequently Asked Questions

Why is grain handling considered so explosion-prone?
Because the bucket elevator concentrates all three explosion ingredients — a grain-dust cloud (fuel), oxygen, and moving steel that can spark or overheat (ignition) — in one enclosed housing. The U.S. averages roughly eight grain-dust explosions a year, which is why maintenance targets ignition control so heavily.
What are the three monitors every bucket elevator needs?
Belt/pulley alignment, bearing temperature, and belt speed/slippage. Each catches a different developing ignition source — a rubbing belt, an overheating bearing, or a slipping drive — before friction becomes a spark. And the sensors themselves must be tested, or they can fail silently.
How much dust accumulation is too much?
OSHA caps priority housekeeping areas — including floors within 35 feet of inside bucket elevators — at 1/8 inch, and NFPA has held that just 1/32 inch over 5% of a surface is a significant hazard. A written, documented housekeeping schedule is required.
What makes bin-sweep maintenance so dangerous?
It requires entering a grain bin — a permit-required confined space — around a powered auger. No sweep maintenance should begin without verified lockout/tagout, an entry permit, atmospheric testing and an attendant. The safety procedure is part of the PM, not separate from it.
What records does OSHA require for grain inspections?
A certification record for each inspection containing the date, the name of the person who performed it, and the equipment's serial number or identifier. OxMaint generates this automatically for every scheduled inspection. Sign up free to start.

Maintenance Is Explosion Safety. Document Both at Once.

OxMaint runs bucket-elevator alignment, bin-sweep LOTO, bearing and belt monitoring, and dust housekeeping as one program — auto-generating the certification record OSHA requires for every inspection. Keep ignition sources from forming, and prove it. Start free — no credit card, unlimited users, forever. Or book a demo.
By William Jerry

✨

Experience
Oxmaint's
Power

Take a personalized tour with our product expert to see how OXmaint can help you streamline your maintenance operations and minimize downtime.

Book a Tour

Share This Story, Choose Your Platform!

Connect all your field staff and maintenance teams in real time.

Report, track and coordinate repairs. Awesome for asset, equipment & asset repair management.

Schedule a demo or start your free trial right away.

iphone

Get Oxmaint App
Most Affordable Maintenance Management Software

Download Our App