High-voltage cable failures in cement plants cause the longest electrical outages of any single asset class — re-termination and fault location in underground cable routes serving kiln drives and mill motors can take 3 to 7 days. Unlike transformer or switchgear failures where replacement equipment can often be sourced quickly, underground cable faults require locating the exact fault position, excavating the route, and completing a full splice or re-termination under controlled conditions. A structured CMMS-scheduled inspection program combining partial discharge testing, thermographic cable surveys, and aging asset flags is the most effective way to prevent the unplanned failures that strand production for days. For cement plants looking to implement this approach, Oxmaint's maintenance management platform provides the scheduling, record-keeping, and analytics to run a mature cable maintenance program — or book a 30-minute session with our team to discuss your plant's electrical reliability priorities.
High-Voltage Cable Inspection and Maintenance in Cement Plants
Underground HV cable failures cause 3–7 day outages. CMMS-driven PD testing, thermographic surveys, and aging asset flags stop them before they happen.
Why HV Cable Failures Are the Costliest Electrical Event
Unlike most electrical assets, underground HV cables combine long recovery times with difficult fault diagnosis. Understanding the failure chain helps prioritize inspection resources.
HV Cable Inspection Methods: What to Use and When
No single test method gives a complete picture of cable health. Best-practice cement plants use at least three complementary techniques on a rotating schedule.
PD testing identifies insulation voids, contamination, and treeing in XLPE and EPR cables before they cause failure. Online PD monitoring using high-frequency CT sensors can be performed without taking cables out of service — critical for kiln drive and primary mill motor feeders that cannot be de-energized for extended periods.
Trend PD magnitude (pC) and PD inception voltage (PDIV) over successive tests. A rising PD level or falling PDIV indicates accelerating insulation degradation and should trigger a condition-based replacement decision.
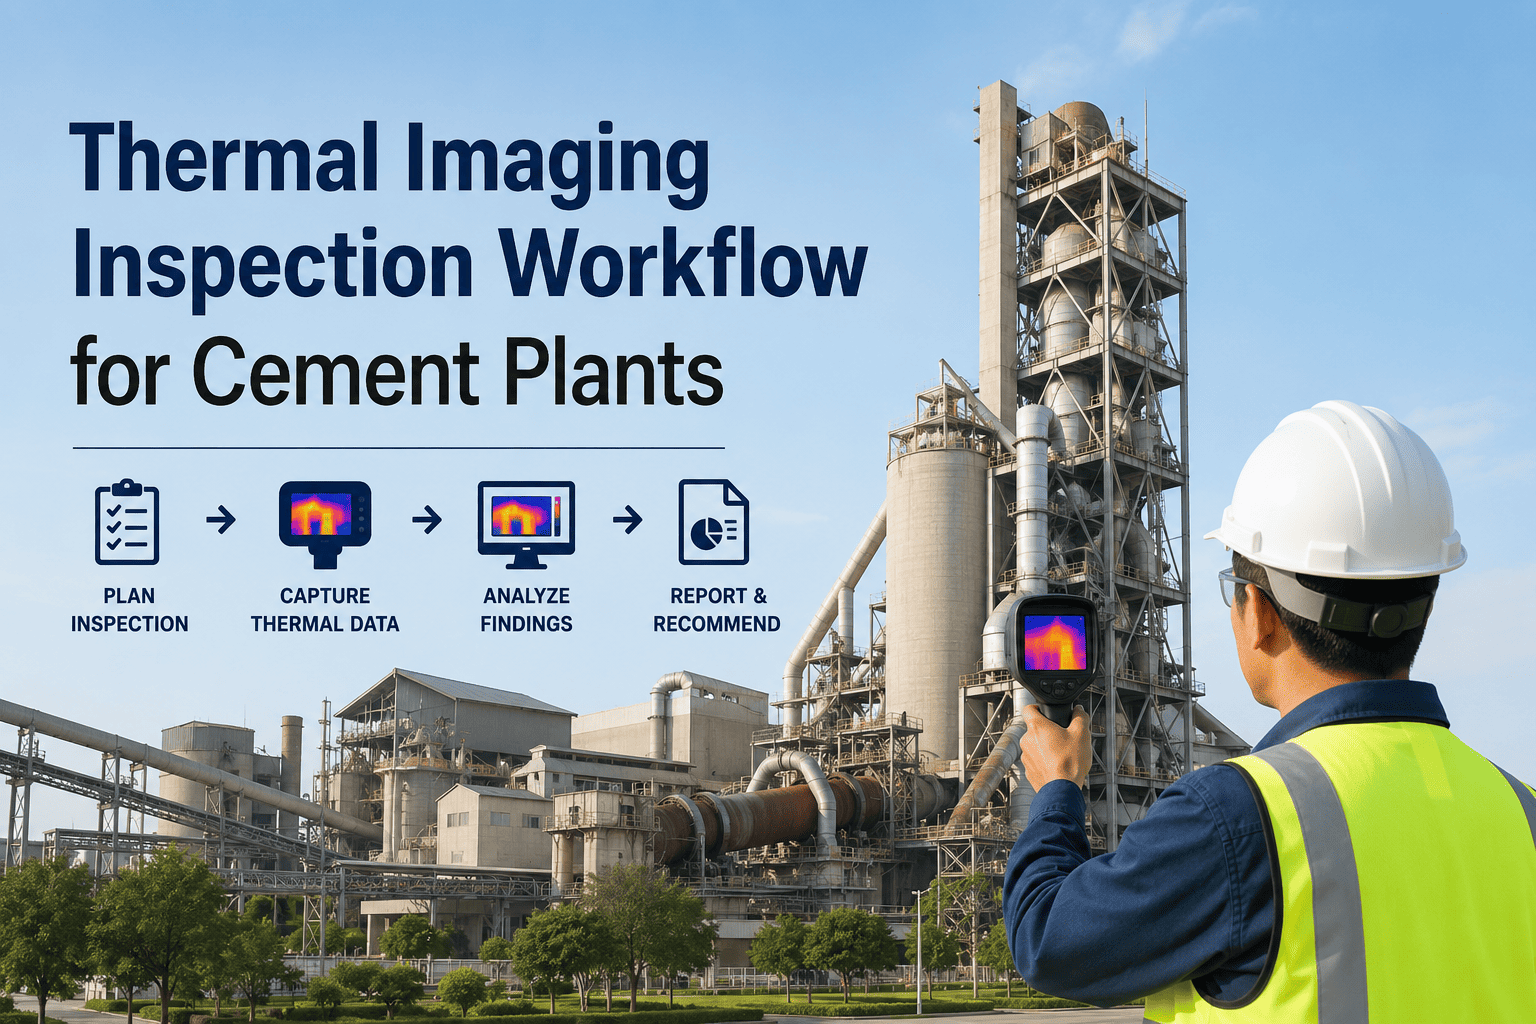
Infrared thermography detects resistive heating at cable joints, terminations, and areas of reduced insulation integrity. In cement plants, the most productive areas to survey are cable trays in the main electrical room, motor connection boxes, and cable terminations at transformer secondary bushings and switchgear busbars.
A temperature differential greater than 10°C above reference at a joint or termination warrants investigation and scheduled re-termination within 30 days.
Megger testing at 5kV or 10kV DC measures bulk insulation resistance and polarization index (PI). A PI below 2.0 or IR value below 1 GΩ per kV of rated voltage is a red flag. Trending IR over time is more valuable than any single reading — even a good absolute value that has halved since last test requires investigation.
Always perform IR testing before and after cable replacement, repair, or any civil work near the cable route to verify no installation damage occurred.
TDR precisely locates faults and impedance discontinuities (joints, water ingress) along a cable route without excavation. Modern TDR combined with GPS mapping produces a fault location accurate to within 0.5–2m — directly reducing excavation scope and repair time from days to hours in some cases.
Store baseline TDR traces in your CMMS when cables are new or after repairs. Future traces can be overlaid to identify new reflections that indicate developing faults.
CMMS Inspection Schedule: Recommended Framework
A structured inspection schedule for HV cables in cement plants must account for cable age, operating load, and criticality to production. This framework aligns with IEC 60364 and IEEE 400 recommendations.
| Cable Circuit | Voltage Level | PD Test Interval | Thermography Interval | IR Test Interval | Priority Flag Trigger |
|---|---|---|---|---|---|
| Kiln main drive feeder | 6.6kV / 11kV | Annual | Annual | Every 2 years | Age >15 years or PD rise |
| Raw mill motor feeder | 6.6kV / 11kV | Biennial | Annual | Every 3 years | Age >18 years |
| Coal mill feeder | 3.3kV / 6.6kV | Annual | Biennial | Every 3 years | Any IR trend decline |
| Cement mill feeder | 6.6kV / 11kV | Biennial | Annual | Every 3 years | Age >20 years |
| Compressor and blower circuits | 3.3kV / 6.6kV | Every 3 years | Biennial | Every 4 years | Thermographic alarm |
| Incomer and tie cables | 33kV / 66kV | Annual | Annual | Every 2 years | Age >12 years |
Cable Aging Management: When to Flag for Replacement
Age alone is not sufficient to trigger cable replacement — but age combined with test data, loading history, and route conditions defines a reliable replacement decision framework.
CMMS Work Order Structure for Cable Maintenance
Effective cable maintenance records in a CMMS must capture more than just inspection dates. Structured data enables trending and reduces troubleshooting time after faults.
- Cable type, voltage class, conductor cross-section
- Installation date and route drawing reference
- Number and location of joints and terminations
- Connected equipment (motor ID, transformer tag)
- Historical fault events with repair records
- PD magnitude (pC) at rated voltage, phase by phase
- Insulation resistance (GΩ) and polarization index
- Thermographic temperature differential at joints
- Visual inspection findings (physical damage, corrosion)
- Ambient temperature and humidity at test time
- PD level rising more than 20% since last test
- IR value below 1 GΩ per kV of rated voltage
- Thermographic delta-T exceeding 10°C at any joint
- Cable age passing 15-year and 20-year thresholds
- Next inspection overdue by more than 60 days
Case Study: 2,500 tpd Plant Eliminates Unplanned Cable Outages
A plant in North Africa with a single-string pyroprocessing line was experiencing two to three unplanned HV cable faults per year — each averaging 4.5 days of lost production at 2,500 tpd clinker output. Root cause analysis identified three systemic failures:
After commissioning a full PD survey, mapping all cable routes and joints into a CMMS, and proactively replacing the three highest-risk feeders during a planned kiln shutdown, the plant recorded zero unplanned HV cable outages over the following 24 months. Book a demo to discuss a similar cable audit for your plant.
Frequently Asked Questions
Turn Your Cable Inspection Data Into a Failure Prevention System
Oxmaint gives cement plant electrical teams structured asset records, automated inspection scheduling, trend-based aging alerts, and full audit trails — so HV cable faults become planned replacements, not production emergencies.