Every dollar invested in a food plant capital project is at risk until commissioning and validation are complete. FAT failures, IQ gaps, and missing OQ/PQ records have derailed FDA and USDA audits at facilities that spent millions on new lines — only to face production holds and re-validation costs because records were fragmented across binders and email threads. The stakes are not theoretical: FSMA 204 traceability requirements, allergen changeover protocols, and GFSI audit cycles all depend on a commissioning record trail that begins the day equipment is specified, not the week before startup. Facilities that onboard new assets directly into a CMMS at the commissioning stage — capturing IQ/OQ/PQ outcomes, calibration baselines, and PM schedules before first production run — avoid the costly retroactive documentation scramble that plagues most capital project handovers — start a free trial to see how Oxmaint structures commissioning records from day one, or book a demo and we will walk through your capital project workflow.
FOOD MANUFACTURING · CMMS · FSMA COMPLIANCE
Stop Losing Capital Project ROI to Incomplete Commissioning Records
See how Oxmaint structures FAT, SAT, IQ/OQ/PQ, and CMMS asset onboarding into one audit-ready workflow.
Real-time asset visibility from day one
Automated PM schedules post-commissioning
Audit-ready IQ/OQ/PQ records always accessible
No heavy implementation required · Live in days, not months · Works across multi-site portfolios
68%
of food plant capital projects experience commissioning delays due to documentation gaps
Source: PMMI Industry Survey
$2.4M
average cost of a production hold triggered by validation record failure during FDA audit
Source: FDA Enforcement Data
40%
of re-validation costs stem from missing baseline calibration records at commissioning
Source: ISPE Baseline Guide
3.2×
faster audit response when IQ/OQ/PQ records are CMMS-linked vs stored in paper binders
Source: GFSI Benchmarking Study
WHAT IS
Food Plant Capital Project Commissioning and Validation
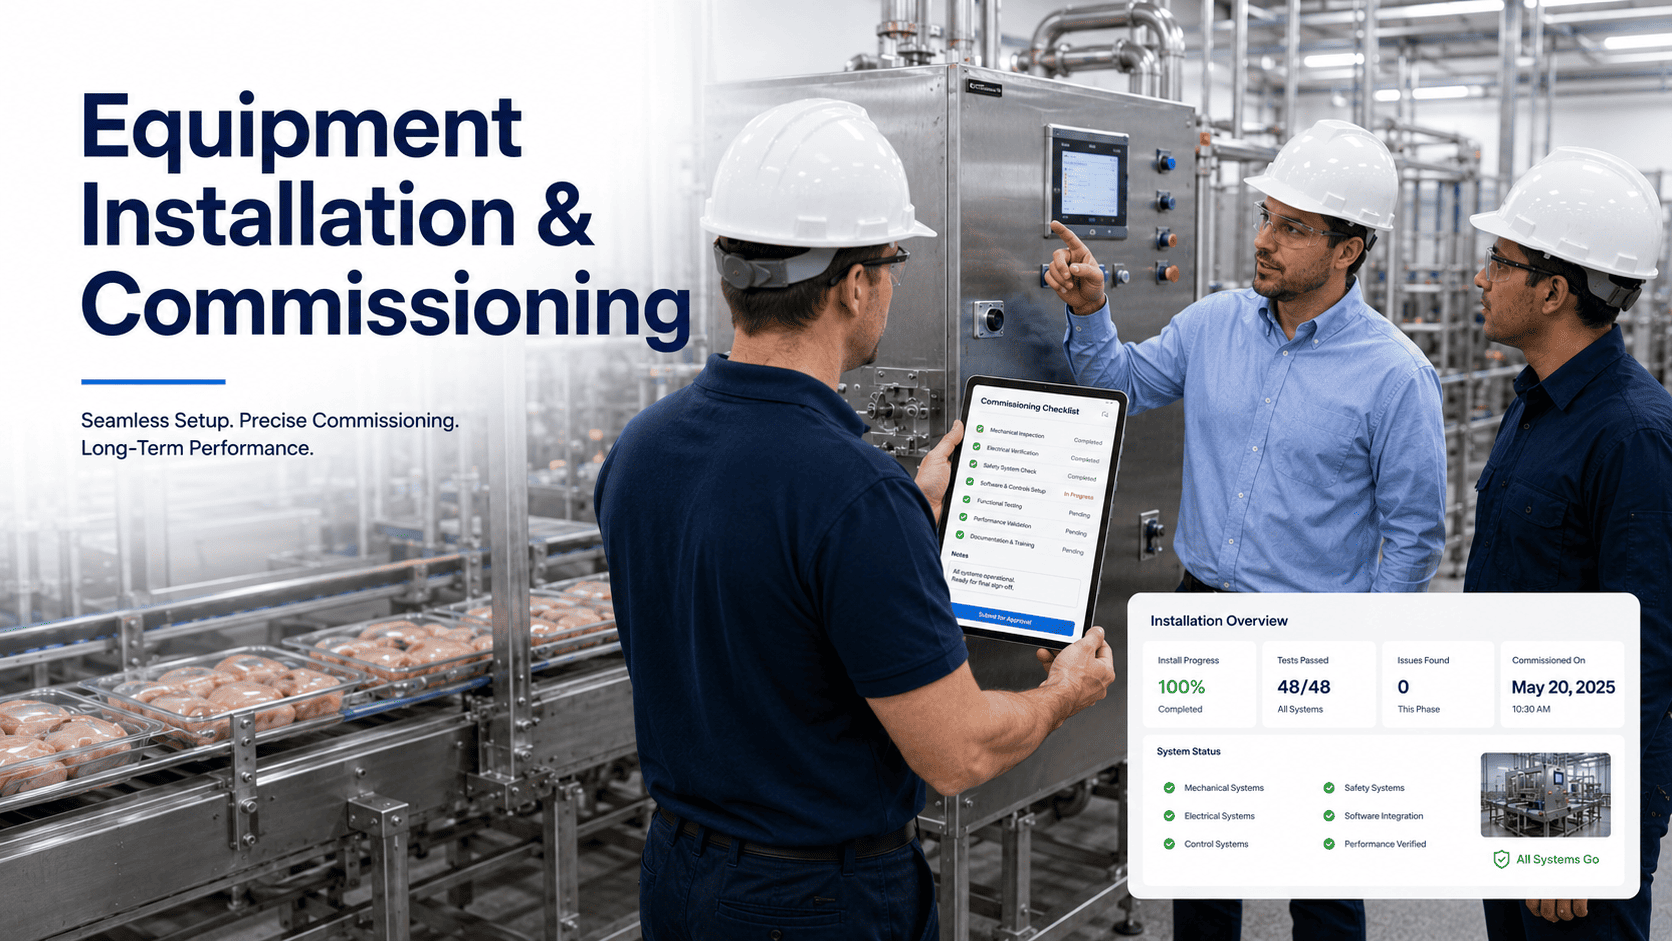
Food plant capital project commissioning is the structured process of verifying that newly installed or modified equipment meets design specifications before production begins. It encompasses Factory Acceptance Testing (FAT) at the OEM facility, Site Acceptance Testing (SAT) after installation, and the formal qualification sequence — Installation Qualification (IQ), Operational Qualification (OQ), and Performance Qualification (PQ) — required under FDA 21 CFR Part 11, USDA, and FSMA frameworks.
Validation goes one step further: it generates documented evidence that equipment consistently produces output meeting predetermined specifications under defined operating conditions. For food manufacturers, this means linking commissioning outcomes directly to HACCP control points, allergen changeover procedures, and CCP verification records — all of which are scrutinized in GFSI, SQF, and BRC audits.
The commissioning-to-production handover is the highest-risk moment in any capital project. Facilities that use a CMMS to onboard assets at the commissioning stage — capturing equipment data, calibration baselines, and PM schedules before first production run — carry that record trail forward through the entire asset lifecycle, dramatically reducing the cost of re-qualification, change control, and regulatory audit response — start a free trial to see how Oxmaint manages this handover.
KEY FRAMEWORK
The 8-Stage Commissioning and Validation Framework
01
Scope Definition and URS
User Requirement Specification locks design intent, regulatory requirements, and FSMA traceability data points before procurement. Scope gaps found here cost 10× less to fix than gaps found at SAT.
02
Factory Acceptance Testing (FAT)
Equipment tested at OEM facility against URS. FAT protocols cover mechanical function, controls logic, sanitary design compliance, and CIP/SIP cycle verification before shipment.
03
Site Acceptance Testing (SAT)
Post-installation testing confirms equipment performs as specified in the actual production environment, including utility connections, safety interlocks, and HMI integration.
04
Installation Qualification (IQ)
Documents that equipment is installed according to design specifications — correct utilities, correct location, correct materials of construction. Creates the as-built baseline for the CMMS asset record.
05
Operational Qualification (OQ)
Verifies equipment operates within specified limits across the full operating range — including worst-case conditions. OQ generates the parameter ranges that define acceptable PM and calibration windows.
06
Performance Qualification (PQ)
Demonstrates consistent output meeting product specifications under actual production conditions. PQ data becomes the benchmark for future deviation investigations and requalification triggers.
07
CMMS Asset Onboarding
All IQ/OQ/PQ records, calibration baselines, spare parts lists, and OEM manuals are loaded into the CMMS asset record at commissioning — not retroactively. This is the moment the asset lifecycle clock starts.
08
PM Schedule Activation
Preventive maintenance schedules derived from OQ parameters and OEM intervals are activated in CMMS before first production run — ensuring the asset never runs without a maintenance plan in place.
Most food plants spend 6–18 months on a capital project — then lose 30% of that investment to reactive failures in the first year because commissioning records were never connected to maintenance.
INDUSTRY PAIN POINTS
Where Food Plant Commissioning Projects Break Down
The majority of commissioning failures in food manufacturing are not technical — they are documentation and handover failures. Understanding where the record trail breaks is the first step to preventing it — start a free trial to see how Oxmaint closes these gaps from day one.
01
FAT and SAT Records Never Reach Maintenance
FAT and SAT documentation is completed by the project team and filed in project binders — then never transferred to the maintenance CMMS. When the equipment needs servicing 18 months later, the baseline data is lost or inaccessible, forcing expensive re-measurement and re-documentation.
02
IQ/OQ/PQ Gaps Fail FDA and USDA Audits
Incomplete qualification records are the single most cited cause of food plant warning letters and import alerts. Auditors specifically look for gaps between IQ and OQ completion dates — periods where equipment was operating without formal qualification evidence, exposing product and the facility to regulatory action.
03
Calibration Baselines Not Established at Commissioning
Without NIST-traceable calibration records created at commissioning, facilities cannot demonstrate that instruments were in calibration at the time of production. This is a critical gap in FSMA verification programs and GFSI audit requirements, often requiring costly retroactive calibration studies.
04
PM Schedules Created Months After Startup
Most facilities create preventive maintenance schedules weeks or months after equipment enters production — meaning the critical early-life period, when infant mortality failures are most likely, is covered only by reactive response. This pattern drives first-year failure rates 2–4× higher than facilities that activate PM schedules at commissioning.
05
Change Control Not Linked to Re-Qualification
Equipment modifications — new wear parts, upgraded controls, different cleaning agents — trigger re-qualification obligations that facilities routinely miss because change control and maintenance records are in separate systems. The result is undetected qualification gaps that grow with each modification cycle.
06
Handover Sign-Off Without Completeness Check
Capital project handovers to operations frequently occur under schedule pressure, with outstanding punch list items and missing documentation accepted as post-handover actions. These items are rarely closed in the compressed environment of production startup, creating permanent gaps in the asset record.
HOW OXMAINT SOLVES IT
Oxmaint Commissioning and Validation Workflow Features
CMMS Asset Onboarding at Commissioning
Create the asset record in Oxmaint at FAT stage — not after startup. Attach IQ/OQ/PQ documents, calibration certificates, OEM manuals, and spare parts lists directly to the asset before it enters production. The record is complete from day one.
Structured Qualification Checklists
IQ, OQ, and PQ protocols are built into mobile-accessible checklists with mandatory sign-off fields, date/time stamps, and photo evidence capture. Every qualification step creates a timestamped, tamper-evident record ready for FDA, USDA, or GFSI audit.
Calibration Baseline Integration
Link NIST-traceable calibration certificates to instrument asset records at commissioning. Oxmaint tracks calibration intervals, sends due-date alerts, and maintains a complete calibration history that satisfies FSMA verification and GFSI audit requirements.
PM Schedule Activation at Handover
OEM-recommended PM intervals and commissioning-derived maintenance requirements are loaded into Oxmaint during the commissioning phase. PM schedules activate automatically at the handover sign-off date — the asset enters production with a complete maintenance plan already running.
Change Control and Re-Qualification Triggers
Equipment modifications logged as work orders in Oxmaint can be flagged to trigger re-qualification workflows. Change control and maintenance records are in the same system — preventing the silent qualification gaps that accumulate when modifications are tracked separately.
Punch List and Handover Sign-Off Workflow
Commissioning punch list items are managed as work orders in Oxmaint with mandatory completion verification before handover sign-off is enabled. Operations cannot formally accept an asset until all outstanding items are resolved and documented.
BEFORE VS AFTER
Reactive Commissioning vs CMMS-Structured Commissioning
| Commissioning Area |
Without CMMS Integration |
With Oxmaint Commissioning Workflow |
| IQ/OQ/PQ Records |
Paper binders filed in project archive, inaccessible during audits |
Digital records linked to asset in CMMS, searchable in seconds during audit |
| Calibration Baselines |
Certificates in separate system, intervals tracked manually or not at all |
NIST-traceable certificates attached to asset record with automated renewal alerts |
| PM Schedule Start |
Created weeks or months after startup, critical early-life period unprotected |
Activated at handover sign-off — equipment enters production with full PM coverage |
| Change Control |
Modifications in maintenance system, re-qualification obligations missed |
Modification work orders trigger re-qualification workflow in the same system |
| Punch List Closure |
Items accepted as post-handover actions, rarely closed in production startup |
Mandatory completion required before handover sign-off is enabled in system |
| Audit Readiness |
3–5 days to compile records, gaps often discovered during audit preparation |
Continuous audit readiness — all records always current and accessible |
Food plants that onboard assets into CMMS at commissioning reduce first-year breakdown costs by up to 38% compared to facilities that build maintenance records retroactively.
ROI AND RESULTS
What Structured Commissioning Delivers
The ROI of CMMS-connected commissioning is realized across three time horizons: immediate audit readiness, first-year maintenance cost reduction, and long-term requalification savings — start a free trial to build your commissioning workflow today.
38%
Reduction in first-year breakdown costs
When PM schedules are activated at commissioning vs post-startup creation
3.2×
Faster audit response time
CMMS-linked qualification records vs paper binder retrieval during FDA/USDA audits
$180K
Average requalification cost avoided
Per capital project when change control triggers re-qualification automatically
92%
Punch list closure rate at handover
Facilities using mandatory CMMS handover sign-off vs 61% closure rate without structured workflow
FAQ
Commissioning and Validation Questions Answered
What is the difference between commissioning and validation in a food plant?
Commissioning verifies that equipment is installed correctly and operates as designed — it is primarily an engineering function. Validation generates documented evidence that equipment consistently produces output meeting predetermined specifications — it is a regulatory and quality function. In food manufacturing, commissioning (FAT, SAT) precedes and feeds into validation (IQ, OQ, PQ). Both must be complete before the asset is onboarded into the CMMS with its baseline records and PM schedules. Most audit failures occur because the two processes are managed by different teams using different documentation systems, creating gaps in the record trail.
When should assets be entered into the CMMS during a capital project?
The asset record should be created in the CMMS at the IQ stage — when the equipment is confirmed installed as specified. FAT and SAT documentation should be attached at that point, with OQ and PQ records added as they are completed. PM schedules should be built in the CMMS during the OQ phase and activated at the handover sign-off date. This approach ensures the CMMS record is complete before first production run and eliminates the retroactive documentation scramble that characterizes most post-startup CMMS onboarding projects.
How does Oxmaint support FSMA 204 traceability requirements for new equipment?
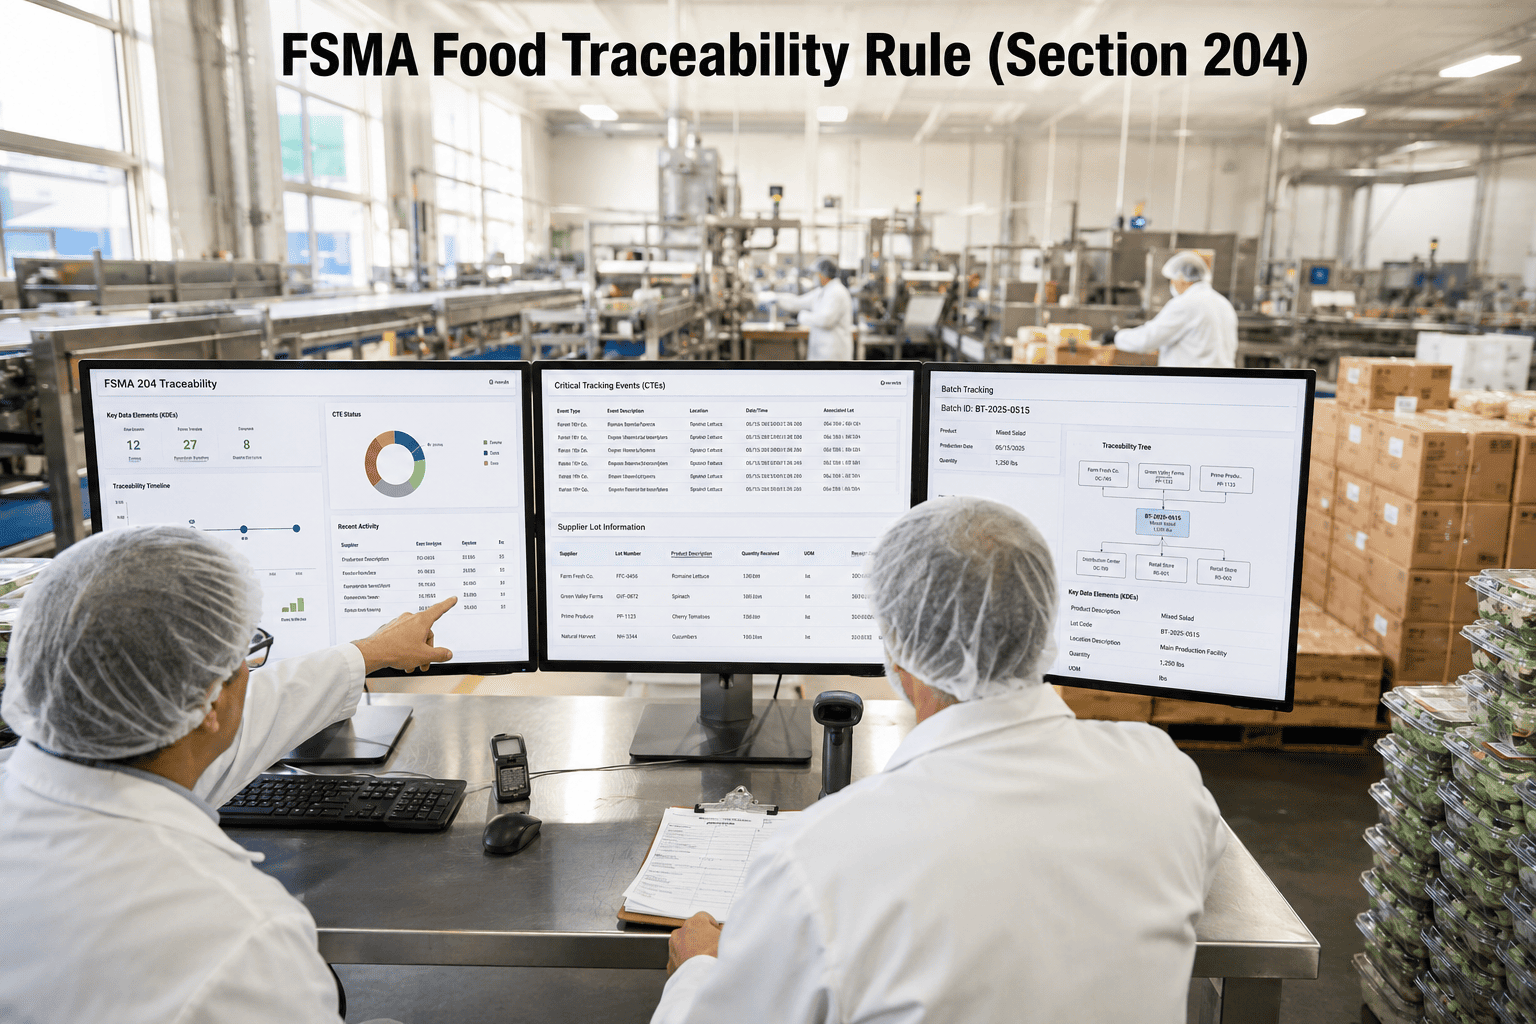
FSMA 204 requires traceability of Key Data Elements (KDEs) at Critical Tracking Events (CTEs) throughout the food supply chain. For new equipment, this means the asset record in the CMMS must capture equipment identifiers, commissioning dates, calibration status, and maintenance history in a format that can be linked to production batch records. Oxmaint's asset hierarchy — Portfolio, Property, System, Asset, Component — allows new equipment to be positioned within the facility structure at commissioning, with all qualification and maintenance records accessible by batch or production date for FSMA traceability queries.
How does Oxmaint handle re-qualification after equipment modifications?
In Oxmaint, equipment modifications are documented as work orders. Work orders can be configured to trigger a re-qualification checklist workflow when the modification type matches a defined re-qualification trigger — such as replacement of a critical component, change in cleaning agent, or controls upgrade. The re-qualification checklist follows the same IQ/OQ/PQ structure as the original commissioning, and the completed records are attached to the asset history alongside the modification work order. This closes the change control gap that allows qualification status to drift silently as equipment is modified over its lifecycle.
Book a demo to see this workflow configured for your equipment types.
FOOD PLANT COMMISSIONING · OXMAINT CMMS
Stop Losing Capital Project ROI to Incomplete Records
Turn every capital project into a permanent audit-ready asset record. Oxmaint connects FAT, SAT, IQ/OQ/PQ, calibration, and PM schedules into a single commissioning-to-production workflow.
Real-time asset visibility from commissioning day
Predictive maintenance from first production run
5–10 year CapEx forecasting from asset condition data
Used by operations teams managing 10,000+ assets · See measurable results in the first 30 days
No heavy implementation required · Live in days, not months · Works across multi-site portfolios