Electrical systems in cement plants consume 110–120 kWh per tonne of cement produced, representing 20–25% of total production costs. With hundreds of motors ranging from 400V low-voltage units to 11kV high-voltage drives powering kilns, mills, and conveyors, electrical infrastructure failures trigger cascading production shutdowns that cost $20,000+ per hour. A single VFD failure on a kiln induced draft fan halted one Mexican plant for 36 hours—costing over $700,000 in lost production before emergency repairs restored operations. Yet 60% of cement facilities still operate electrical maintenance programs based on time-based schedules rather than condition monitoring, missing early warning signs of insulation degradation, harmonic distortion, and thermal stress. This guide covers the complete spectrum of cement plant electrical maintenance—from daily inspection protocols to strategic upgrade decisions that extend equipment life by 30% while reducing energy consumption by 15–20%. Sign up for Oxmaint to digitize your electrical maintenance program and track motor health, transformer inspections, and VFD performance from a single dashboard.
110–120
kWh/tonne
Electrical Energy Consumption
20–25%
of costs
Production Cost Share
97%
reduction
Maintenance with VFDs
15–20%
savings
Energy with Upgrades
Cement Plant Electrical Infrastructure Overview
Understanding the electrical architecture of cement plants is essential before developing maintenance strategies. Power distribution begins at grid substations receiving 66kV–132kV supply and cascades through multiple transformation stages to reach individual motor control centers. Each voltage level presents unique maintenance challenges—from oil-immersed transformer inspections to MCC thermal imaging protocols.
132kV / 66kV
Grid Substation
Main Transformers
Circuit Breakers
Protection Relays
33kV / 11kV
HV Distribution
HV Switchgear
Power Factor Banks
HV Motors (Kiln/Mill)
6.6kV / 3.3kV
MV Distribution
MV Switchgear
VFDs
MV Motors
415V / 400V
LV Distribution
MCCs
LV Motors
Lighting/Auxiliaries
Critical Electrical Equipment in Cement Plants
Cement plants operate hundreds of electric motors across all production stages—from quarry crushers to cement packaging lines. Identifying the most failure-prone and production-critical equipment enables maintenance teams to prioritize inspection resources and spare parts inventory. Book a demo to see how Oxmaint tracks criticality ratings and generates condition-based work orders for your electrical assets.
Kiln Drive Motors
Voltage:6.6kV–11kV
Power:2,000–5,000 kW
Criticality:Critical
Common issues: Bearing wear, insulation breakdown, cooling system failures, gearbox coupling misalignment
Mill Drive Systems
Voltage:3.3kV–6.6kV
Power:3,000–8,000 kW
Criticality:Critical
Common issues: Synchronous motor excitation faults, ring gear alignment, VFD harmonics, power factor correction
ID/FD Fans
Voltage:6.6kV
Power:500–2,500 kW
Criticality:High
Common issues: VFD cooling failures, motor overheating in dusty environments, damper actuator faults
Power Transformers
Voltage:132kV/6.6kV
Capacity:20–50 MVA
Criticality:Critical
Common issues: Oil degradation, bushing failures, winding insulation aging, tap changer malfunctions
Variable Frequency Drives
Voltage:400V–6.6kV
Power:50–5,000 kW
Criticality:High
Common issues: Capacitor aging, IGBT failures, cooling fan blockage, harmonic filter degradation
Motor Control Centers
Voltage:415V
Feeders:50–200 per MCC
Criticality:Medium
Common issues: Contactor coil failures, thermal overload trips, loose terminations, arc flash hazards
Digitize Your Electrical Maintenance Program
Track motor health, transformer oil analysis, VFD performance trends, and thermographic inspections from one centralized platform. Automate PM schedules and generate compliance reports instantly.
Electrical Maintenance Inspection Protocols
Effective electrical maintenance in cement plants requires layered inspection protocols—daily visual checks, weekly functional tests, monthly condition assessments, and annual comprehensive audits. Each layer catches different failure modes at different stages of development, enabling intervention before catastrophic breakdown occurs.
Motor operating temperature via handheld IR or installed sensors
VFD display screens for fault codes, warnings, or abnormal readings
Transformer oil level gauges and temperature indicators
MCC panel temperatures and unusual sounds or smells
Cable tray integrity and visible damage to exposed conductors
Motor current readings compared against nameplate ratings
VFD cooling fan operation and air filter cleanliness
Power factor readings at main distribution boards
Emergency lighting and UPS battery status verification
Earthing system continuity spot checks
Thermographic survey of all switchgear, MCCs, and junction boxes
Motor vibration analysis on critical drives
VFD capacitor bank visual inspection for swelling or leakage
Transformer silica gel breather condition assessment
Cable termination torque verification on high-current feeders
Motor insulation resistance testing (megger) on all critical drives
Transformer oil dissolved gas analysis (DGA)
HV circuit breaker contact resistance and timing tests
Protection relay calibration and functional testing
Complete earthing system resistance measurement
Schedule a demo to see how Oxmaint automates inspection scheduling, captures thermographic images directly within work orders, and tracks trending data to predict failures before they occur.
Common Electrical Failure Modes and Prevention
Cement plant environments accelerate electrical equipment degradation through dust infiltration, thermal cycling, harmonic distortion, and continuous high-load operation. Understanding the root causes of common failures enables targeted preventive strategies that extend equipment life and reduce unplanned downtime. Book a demo to see how Oxmaint's failure mode tracking helps identify recurring electrical issues.
Root Causes: Thermal stress from overloading, VFD-induced voltage spikes, moisture ingress, cement dust contamination
Impact: Phase-to-ground faults, complete motor failure, production shutdown of 24–72 hours
Prevention: Quarterly insulation resistance testing, motor winding temperature monitoring, VFD output filters, IP65+ enclosures
Root Causes: Electrolytic capacitor aging (typical life 5–7 years), excessive ambient temperature, harmonic stress
Impact: DC bus voltage instability, drive trips, IGBT failures cascading from capacitor degradation
Prevention: Annual capacitor ESR testing, maintain ambient below 40°C, scheduled replacement at 5-year intervals
Root Causes: Moisture ingress through degraded seals, cellulose insulation breakdown, overheating, internal arcing
Impact: Reduced dielectric strength, accelerated aging, catastrophic failure with fire risk
Prevention: Annual DGA testing, moisture content monitoring, silica gel maintenance, IR thermography of bushings
Root Causes: Thermal cycling, vibration from rotating equipment, improper initial torque, corrosion
Impact: Hot spots leading to arc flash hazards, fire, equipment damage, personnel injury risk
Prevention: Monthly thermographic surveys, torque verification during shutdowns, anti-vibration mounting
Electrical System Upgrade Priorities
Modernizing electrical infrastructure in cement plants requires strategic prioritization—focusing investments where they deliver the highest ROI through energy savings, reliability improvements, and maintenance cost reduction. The upgrade pathway below sequences investments based on typical payback periods and operational impact.
Priority 1
VFD Installation on Major Fans
Typical Cost:
$150,000–$400,000 per drive
Energy Savings:
25–40% on fan power consumption
Payback Period:
12–24 months
Converting induced draft and forced draft fans from damper control to VFD control delivers the fastest payback of any electrical upgrade. One Mexican plant saved 5,300 MWh annually—€574,000 in revenue gains—after installing ABB drives on 735 kW ID fans.
Priority 2
Power Factor Correction Systems
Typical Cost:
$50,000–$200,000
Demand Reduction:
10–15% kVA demand savings
Payback Period:
18–36 months
Automatic power factor correction banks reduce maximum demand charges while improving voltage stability across the distribution network. Target PF of 0.95+ to avoid utility penalties and optimize transformer utilization.
Priority 3
IE3/IE4 High-Efficiency Motors
Premium Cost:
15–25% over standard motors
Efficiency Gain:
2–5% per motor
Payback Period:
24–48 months
Replace failed motors with IE3 or IE4 efficiency class units. For continuously running loads above 100 kW, the efficiency premium pays back within 2–4 years through reduced energy consumption.
Priority 4
Online Condition Monitoring Systems
Typical Cost:
$5,000–$15,000 per motor
Downtime Reduction:
30–50% unplanned stops
Payback Period:
12–24 months
Continuous vibration, temperature, and current monitoring on critical motors enables predictive maintenance—detecting bearing wear, insulation degradation, and alignment issues 4–6 weeks before failure.
Book a consultation to discuss upgrade prioritization based on your plant's specific energy costs, equipment age, and maintenance history.
VFD Applications in Cement Plants
Variable Frequency Drives have transformed cement plant operations by enabling precise speed control, soft starting, and dramatic energy savings across fan, pump, and conveyor applications. Beyond energy reduction, VFDs deliver 97% lower maintenance costs compared to mechanical flow control methods by eliminating dampers, valves, and fluid couplings.
Induced Draft Fans
30–40%
Energy Savings
Replaces inefficient damper control with precise airflow modulation. Fan power follows cubic law—reducing speed by 20% cuts power by 50%.
Raw Mill Separators
15–25%
Energy Savings
Optimizes separator speed for material fineness control, reducing over-grinding and improving specific energy consumption per tonne.
Kiln Feed Systems
20–30%
Energy Savings
Enables continuous feed rate adjustment matching kiln conditions, eliminating start-stop cycles and mechanical stress on conveyors.
Cooling Water Pumps
25–35%
Energy Savings
Matches pump output to actual cooling demand, eliminating throttling valve losses and reducing pump maintenance intervals.
Track Electrical Asset Performance in Real Time
Monitor motor health, VFD parameters, transformer conditions, and energy consumption from a unified CMMS dashboard. Generate automated work orders when thresholds are exceeded.
Safety and Compliance Requirements
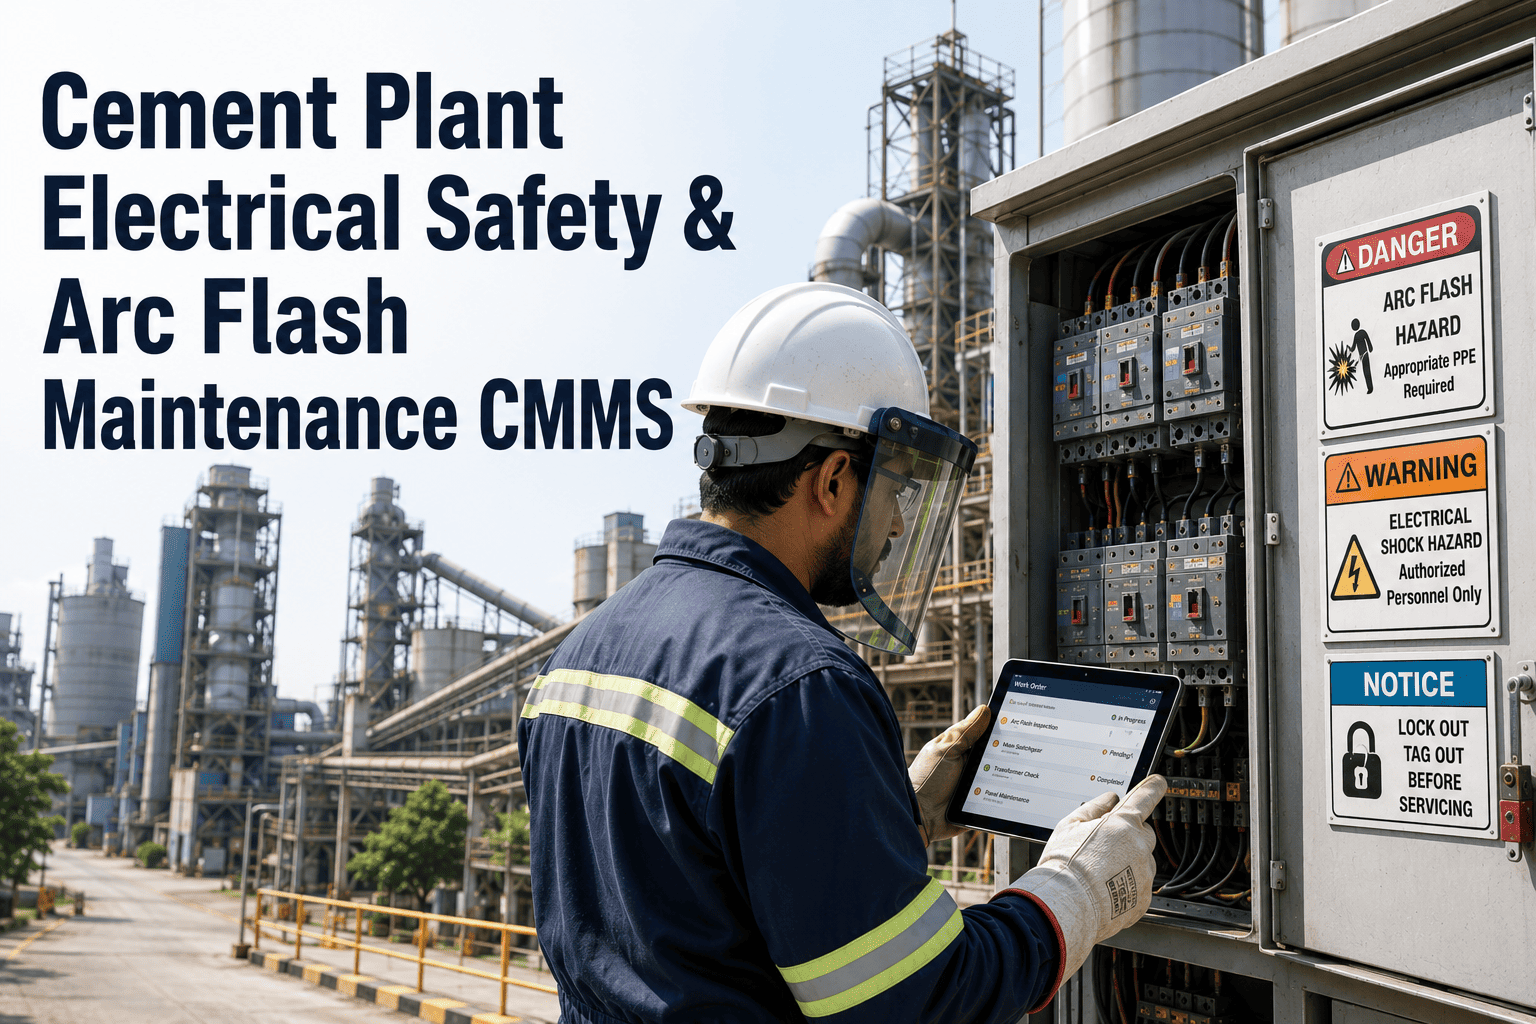
Electrical maintenance in cement plants involves significant hazards including arc flash, electrical shock, and stored energy in capacitors and transformers. Compliance with NFPA 70E, OSHA 1910.147 (lockout/tagout), and local electrical safety regulations is mandatory. Proper documentation through CMMS platforms ensures audit readiness and demonstrates due diligence.
01
Arc Flash Hazard Analysis
Conduct IEEE 1584 arc flash studies for all switchgear and MCCs. Label equipment with incident energy levels and required PPE. Update studies whenever system modifications alter fault current levels.
02
LOTO Procedures
Develop equipment-specific lockout/tagout procedures for every electrical isolation point. Verify zero energy state before work begins. Document all isolation and de-isolation steps in CMMS work orders.
03
Qualified Personnel Requirements
Only qualified electrical workers may perform live work or approach energized equipment within arc flash boundaries. Maintain training records and competency certifications for all electrical personnel.
04
Protective Equipment Testing
Test insulated gloves, hot sticks, and voltage detectors at required intervals. Document test dates and results. Remove defective equipment from service immediately.
Frequently Asked Questions
How often should transformer oil be tested in cement plants?
Transformer oil should undergo basic testing (breakdown voltage, moisture content, acidity) annually for units under 10 years old. Dissolved gas analysis (DGA) should be performed annually on critical transformers and every 2 years on non-critical units. High-stress environments may require more frequent testing. Results trending over time reveals developing faults before catastrophic failure.
What is the typical lifespan of VFD capacitors in cement environments?
Electrolytic capacitors in VFDs typically last 5–7 years under normal operating conditions. In cement plant environments with elevated ambient temperatures and dust infiltration, lifespan may be reduced to 4–5 years. Schedule capacitor replacement proactively at 5-year intervals for critical drives to avoid unexpected failures and cascading IGBT damage.
How do VFDs reduce maintenance costs beyond energy savings?
VFDs eliminate mechanical flow control components like dampers, louvers, and fluid couplings—removing their associated maintenance burden entirely. Soft start capability reduces motor starting current from 6–8x full load to 1.5x, dramatically extending motor and coupling life. One cement plant reported 97% reduction in ID fan maintenance costs after VFD installation by eliminating damper repairs and reducing motor rewinds.
What insulation resistance values indicate motor replacement is needed?
IEEE 43 recommends minimum insulation resistance of 1 megohm per kV of rated voltage plus 1 megohm. For a 6.6kV motor, minimum acceptable IR is 7.6 megohms at 40°C. Values below this threshold indicate deteriorated insulation requiring immediate investigation. Trending IR values over time is more valuable than single readings—a motor showing consistent decline should be scheduled for rewinding or replacement during the next planned shutdown.
How frequently should thermographic inspections be performed?
Monthly thermographic surveys are recommended for MCCs, switchgear, and high-current connections in cement plants. Critical equipment like kiln drive power electronics should be inspected weekly. During summer months with peak ambient temperatures, increase inspection frequency. All hot spots exceeding 10°C above ambient or showing abnormal thermal patterns compared to similar equipment should trigger immediate investigation and corrective work orders.
How can CMMS software improve electrical maintenance programs?
CMMS platforms centralize electrical asset records, automate PM scheduling, capture inspection data including thermographic images, and track trending parameters like insulation resistance and vibration levels over time. Condition-based triggers generate work orders automatically when thresholds are exceeded. Compliance documentation for arc flash studies, LOTO procedures, and equipment testing is maintained audit-ready. Plants using CMMS for electrical maintenance typically reduce emergency work orders by 40–50% within the first year.