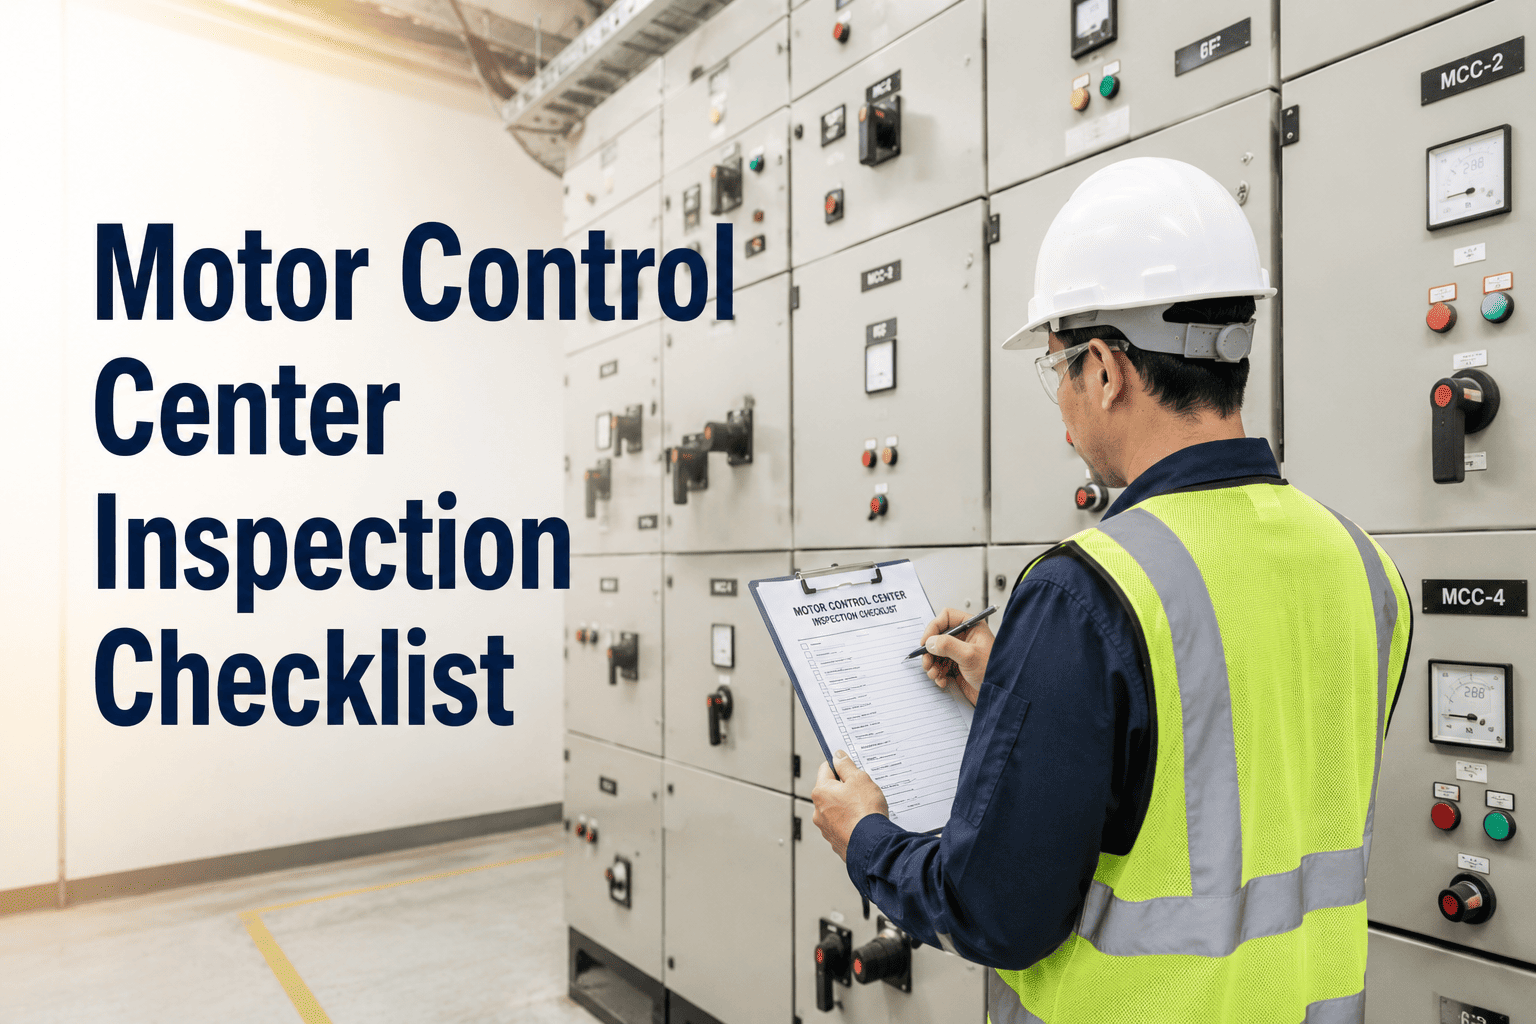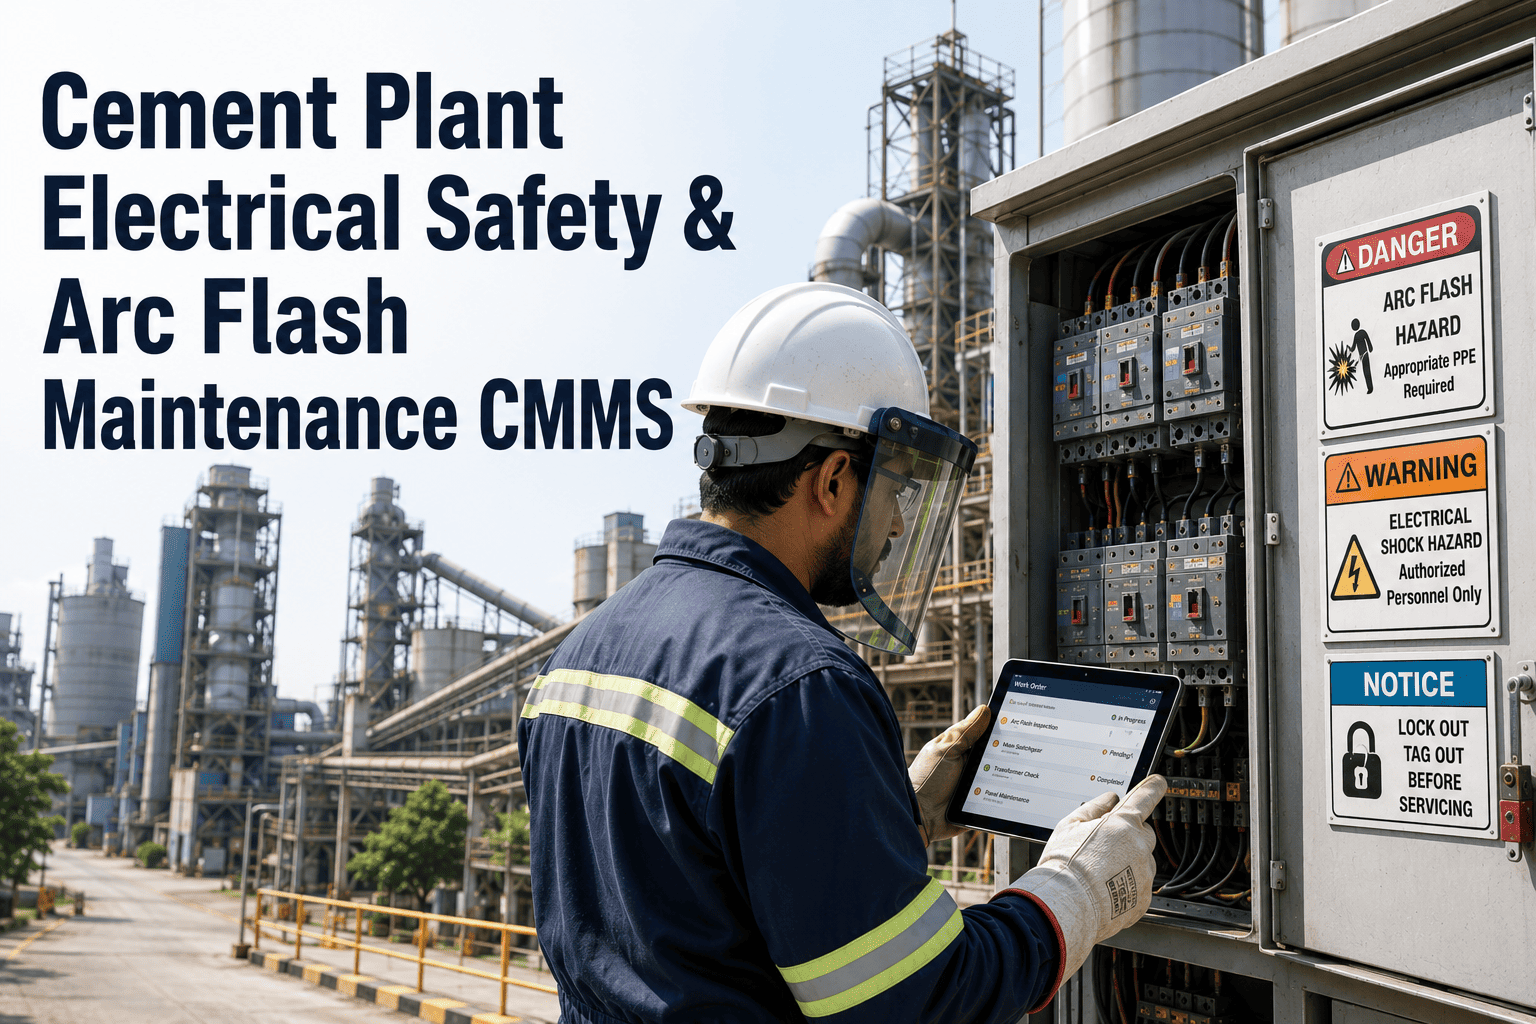
Cement plants run on massive electrical loads — 5,000+ HP kiln drives, 4,160 V switchgear, and hundreds of motor control centers powering mills, crushers, and conveyors around the clock. An arc flash event in that environment releases plasma hotter than 35,000°F in milliseconds, and NFPA 70E compliance enforced by OSHA is the only line between a routine maintenance task and a fatal incident. A CMMS-driven electrical safety program ties arc flash studies, energized work permits, PPE selection, and switchgear inspection cadences into one auditable system — closing the gaps that paper logs and spreadsheets leave open. You can Start Free Trial to stand that program up in days, not quarters.
Can your crew survive a 35,000°F arc flash at the MCC?
In a cement plant, one unlabeled motor control center can end a career in milliseconds. NFPA 70E demands engineered analysis, documented PPE, and verifiable maintenance — and OSHA enforces it with six-figure penalties. The CMMS-driven program below closes every gap, from switchgear labeling to energized-work permits.
Why cement arc flash incidents are 3× more expensive than average
Cement plants carry concentrated, high-voltage loads with little redundancy and 24/7 uptime pressure — meaning an arc flash event here is both more likely and more costly than in a typical plant. The numbers below define the stakes.
Medical, equipment damage, and cleanup — before OSHA fines or litigation.
A single arc flash can remove a skilled electrician from your crew for nearly three weeks.
Per violation — repeated citations climb higher and trigger unannounced follow-up inspections.
Molten metal and pressure waves cause burns, blunt trauma, and permanent hearing loss.
A 180-asset cement plant in Texas was spending $42,000/year on spreadsheets, paper energized-work permits, and ad-hoc PPE purchases. After a near-miss at a 480V kiln feeder MCC — an unlabeled bucket that should have been Category 4 — the plant deployed a CMMS-based arc flash program. Within 90 days, every switchgear cell and MCC bucket was relabeled, incident energy was recalculated, and PPE kits were matched to each work order. Compliance audit findings dropped to zero, insurance premiums fell 12%, and the plant recovered the full CMMS investment in 4.5 months.
NFPA 70E compliance requirements for cement operations
NFPA 70E is the consensus standard OSHA cites under the General Duty Clause. For a cement plant, every switchgear lineup, MCC, transformer, and VFD must be addressed by five interlocking elements — all of which the CMMS structures and timestamps.
Arc flash hazard analysis
Incident energy and arc flash boundary calculated at every bus, every feeder, every MCC bucket — using IEEE 1584 methods. Studies must be updated within 5 years or after any major one-line change.
Energized electrical work permits
Justification, risk assessment, PPE matrix, boundaries, and qualified-personnel sign-off — required whenever work is performed within the restricted approach boundary. The CMMS attaches the signed permit to the work order.
PPE selection & verification
Category-rated PPE (Cat 1–4) matched to incident energy at the specific device. The CMMS enforces PPE kit assignment per asset and logs inspection dates on every suit, glove, and face shield.
Switchgear & MCC inspection cadence
Infrared thermography quarterly, visual and cleaning PMs semi-annually, breaker calibration and contact-resistance testing annually — scheduled and routed through work orders with photo documentation.
Qualified-personnel documentation
Training records, task-qualification logs, and refresher cadences per employee. The CMMS flags expired qualifications and blocks assignment of energized work to unqualified techs.
Labeling & boundary marking
Arc flash warning labels with incident energy, working distance, boundary, and required PPE — printed and re-applied after every study revision. Audited annually through a CMMS rounding route.
Switchgear and MCC preventive maintenance checklist
Use this tiered checklist to structure CMMS work-order templates for every energized asset in the plant. Each item maps to an NFPA 70E article, an OSHA citation source, and a measurable acceptance criterion.
Switchgear thermography & visual
- Infrared scan of all bus connections, breaker stabs, and cable lugs — ΔT > 15°C above ambient flagged for corrective work order.
- Visual inspection of arc-flash labels for legibility, correct incident energy values, and intact boundary markings.
- Moisture & contamination check in switchgear rooms — cement dust accumulations cleaned from ventilation paths.
MCC bucket & starter maintenance
- De-energize and lockout each MCC bucket; verify zero voltage with a calibrated tester before any contact.
- Contact resistance & insulation resistance testing — megger at 1,000V, record values in CMMS for trend analysis.
- Overload relay calibration and heater-element verification against motor full-load amps stamped on the nameplate.
Breaker & relay calibration
- Primary injection testing of low-voltage power circuit breakers — long-time, short-time, and instantaneous pickups verified.
- Protective relay testing on medium-voltage feeders — coordination curves confirmed against the plant's short-circuit study.
- Arc flash study refresh if load additions, transformer changes, or utility source impedance have shifted since the last calculation.
| Asset class | Typical voltage | Arc flash category | Required PPE | PM frequency |
|---|---|---|---|---|
| Medium-voltage switchgear | 4,160 V – 13.8 kV | Category 3–4 | 40–100 cal/cm² suit | Quarterly IR · Annual cal |
| Low-voltage main switchgear | 480 V | Category 2–4 | 8–40 cal/cm² suit | Quarterly IR · Annual cal |
| Motor control centers | 480 V | Category 1–2 | 4–8 cal/cm² kit | Semi-annual PM |
| Kiln & mill VFDs | 480 V – 690 V | Category 2 | 8 cal/cm² kit | Semi-annual PM |
| Power transformers (dry) | 4,160 V primary | Category 3 | 25 cal/cm² suit | Annual IR · 3-yr oil/DGA |
| Lighting & distribution panels | 208/120 V | Category 1 | 4 cal/cm² kit | Annual visual |
Deploying a CMMS-driven arc flash program in 5 phases
A cement plant can move from paper permits to a fully auditable NFPA 70E program in one quarter. Each phase below produces a tangible artifact the next phase depends on — no step is optional.
Asset inventory & one-line import
Import every switchgear lineup, MCC section, transformer, and panel into the CMMS. Attach single-line drawings, equipment nameplates, and GPS coordinates. Most plants discover 8–15% more energized assets than their paper records show.
Arc flash study refresh
Re-run IEEE 1584 calculations using current utility fault data and any plant-side impedance changes. Import incident energy, boundary, and PPE category per asset directly into CMMS asset records.
Label & PPE deployment
Print and apply compliant arc flash labels at every device. Match PPE kits to the highest incident energy in each zone. CMMS prints labels from asset data — no manual transcription.
Work-order templates & permits
Build energized-work-permit templates with risk matrix, PPE checklist, and qualified-personnel requirements. Configure PM triggers for IR scans, breaker calibration, and relay testing — auto-generated from asset criticality.
Audit & continuous improvement
Run quarterly compliance reports: permit completion rate, PPE inspection compliance, overdue PMs, and incident-energy deviations. Export OSHA-ready documentation in one click. Most plants reach 98%+ audit pass rate within 90 days of go-live.
Turn arc flash compliance from a liability into a logged, audit-ready asset.
Deploy a CMMS that schedules every PM, attaches every permit, and labels every bucket — in one quarter, not one fiscal year.
Cement plant electrical safety & arc flash — answered
The five questions cement maintenance managers ask most before deploying a CMMS-driven arc flash program.
How often must a cement plant update its arc flash hazard analysis?
NFPA 70E requires a review every five years at minimum, and sooner whenever the electrical system changes — new transformers, added MCCs, utility source impedance updates, or large motor additions. In cement plants with continuous kiln and mill upgrades, an annual review of the one-line and a full recalculation every two to three years is the defensible standard. A CMMS flags the review date and auto-creates the work order.
What PPE category applies to a typical 480V cement plant MCC?
Most 480V MCC buckets fall into Category 1 (4 cal/cm²) or Category 2 (8 cal/cm²), depending on available fault current, clearing time of the upstream breaker, and working distance. Main switchgear lineups and transformer secondaries routinely reach Category 3 or 4 (25–100 cal/cm²), requiring full flash suits. Never assume — the incident energy label on each device is the only valid reference. You can Book a Demo to see how the CMMS enforces PPE-by-asset at the work-order level.
Can a CMMS actually prevent an arc flash incident, or just document it?
Both. The CMMS prevents incidents by enforcing de-energization verification before work, blocking energized tasks without a signed permit, matching PPE to the specific asset's incident energy, and flagging overdue thermography or breaker calibration that signals degrading equipment. Documentation is the audit trail — but the prevention is in the workflow gates the system enforces before any technician touches a live bus.
What does OSHA look for during a cement plant electrical inspection?
Inspectors ask for current arc flash labels, energized-work permits with justifications and signatures, PPE inspection records, qualified-personnel training documentation, lockout/tagout procedures, and PM records on switchgear and protective devices. Missing or outdated arc flash studies, unlabeled equipment, and PPE that does not match the hazard are the three most cited findings — each carrying penalties upward of $15,000 per violation. The CMMS produces all of these records in a single export.
How long does it take to deploy a CMMS arc flash program in a cement plant?
A mid-size cement plant with 150–250 energized assets can complete a full deployment in 12–14 weeks: three weeks for asset import, three for study refresh, three for labeling and PPE, three for work-order template and permit configuration, and one for team training and audit. Plants with existing CMMS data or a recent arc flash study compress this to 6–8 weeks. You can Start Free Trial and begin the asset import on day one.
One quarter to a fully auditable arc flash program.
Import assets, refresh the study, label every bucket, and route every permit through one CMMS — before the next inspection, not after.
Free 14-day trial · No credit card