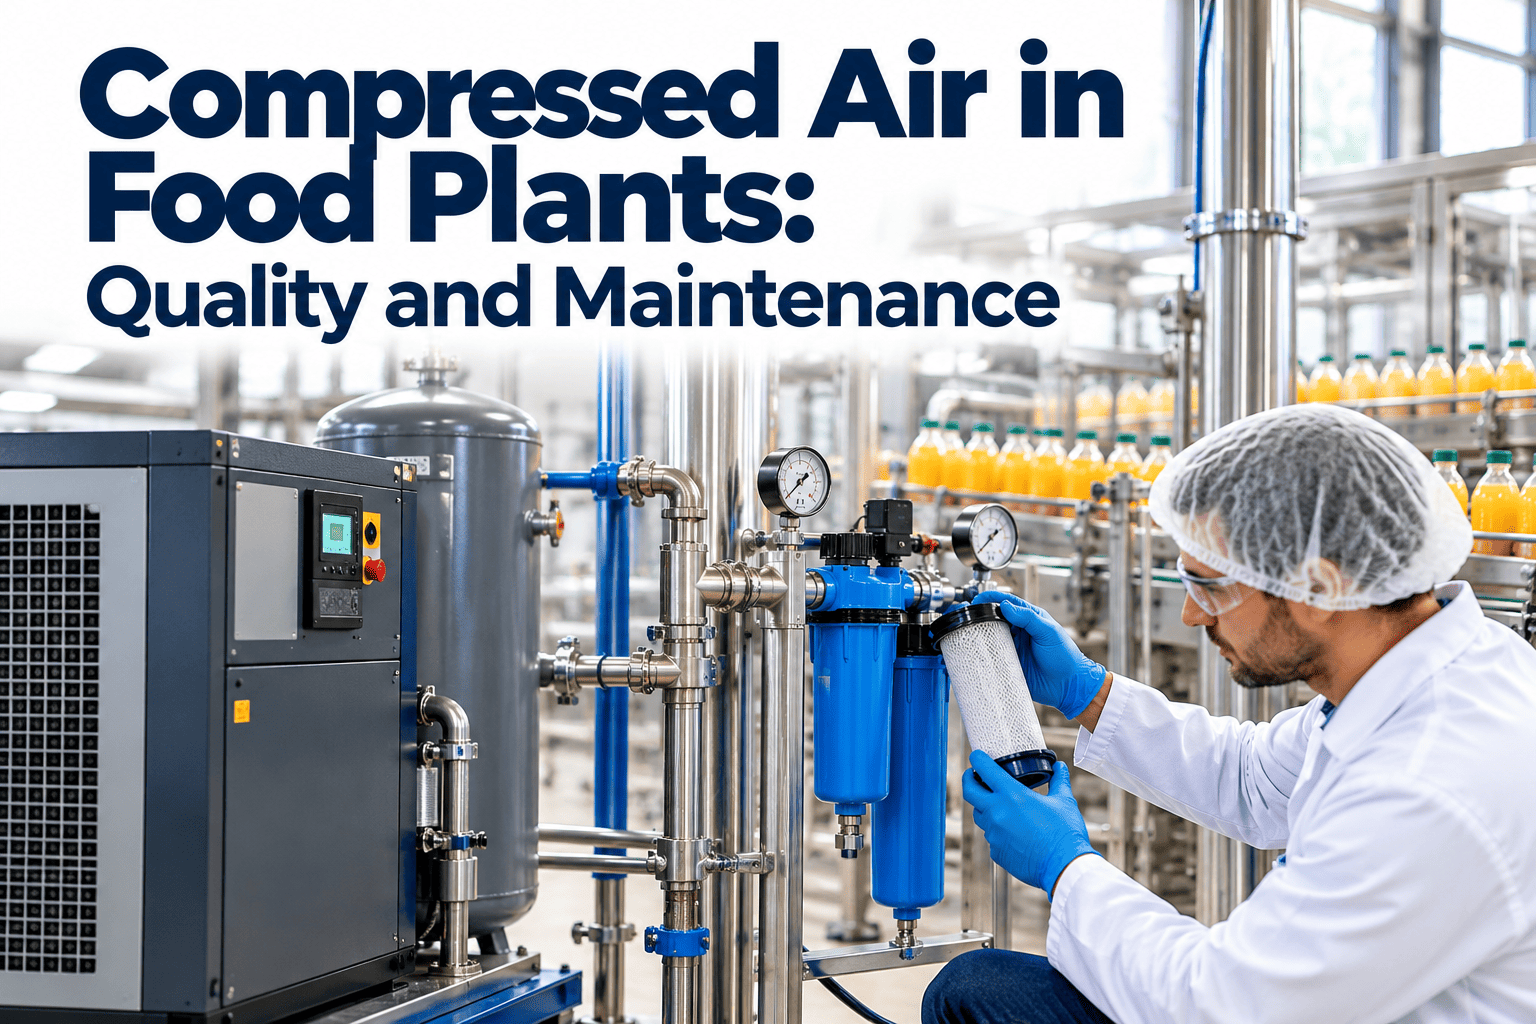
Compressed air is easy to overlook in a food plant because it is invisible and always there. It blows off packaging, drives actuators, agitates product, dries containers and sometimes meets food directly. If the air carries water, oil or particles, those contaminants travel with it to wherever the air goes. Keeping air clean is less about one clever filter and more about steady upkeep of compressors, dryers, filters and drains, backed by records that show it happened. That is where a maintenance management system can make utility work as visible as production work.
Compressed Air in Food Plants: Quality and Maintenance Tips That Work
Monitor filters, dryers and air quality, and maintain compressors where air touches product, with practical routines your maintenance and quality teams can run side by side.
- Intake and compressorMakes the air
- Aftercooler and separatorRemoves bulk water
- Receiver and drainsStores and sheds condensate
- DryerLowers moisture content
- FiltersRemove particles and oil
- Point of useFinal protection and sampling
Four Ideas to Carry Into Your Next Maintenance Meeting
- 1Decide purity by how air contacts product, not by habit or by what the compressor happens to deliver.
- 2Water is the root of most problems, because it carries oil and gives microorganisms a place to live.
- 3Change filters on condition and schedule, and record both, since a neglected element can pass contaminants.
- 4Test the air itself on a defined routine, because well-maintained equipment is a claim until results prove it.
Where Does the Air Actually Touch Your Product?
Before talking about filters, map where compressed air goes. Purity targets and inspection effort should follow the level of contact at each use.
The Four Contaminants to Control and How to Check Each One
Particles, water, oil and microorganisms enter the system from different places. Matching each to a control and a check keeps the program practical.
| Contaminant | Where it comes from | Why it matters | Primary controls | How to check |
|---|---|---|---|---|
| Solid particles | Ambient dust drawn in at the intake, pipe scale, worn components | Foreign material in or on product and packaging | Intake filtration, particulate filters, clean piping | Pressure drop across filters, particle testing |
| Water | Humidity in the intake air, condensation after compression | Corrodes piping, carries other contaminants, supports microbial growth | Aftercooler, separators, dryer, working drains | Dew point readings, condensate checks |
| Oil | Carryover from lubricated compressors, hydrocarbon vapor in intake air | Chemical contamination and off-flavors, packaging problems | Coalescing and oil vapor removal, compressor condition | Oil testing at defined points |
| Microorganisms | Intake air, wet piping and filters, dead legs | Biological contamination where air meets product | Dry air, sterile filtration at point of use where required | Microbiological sampling |
ISO 8573-1 Purity Classes Explained in Plain Terms
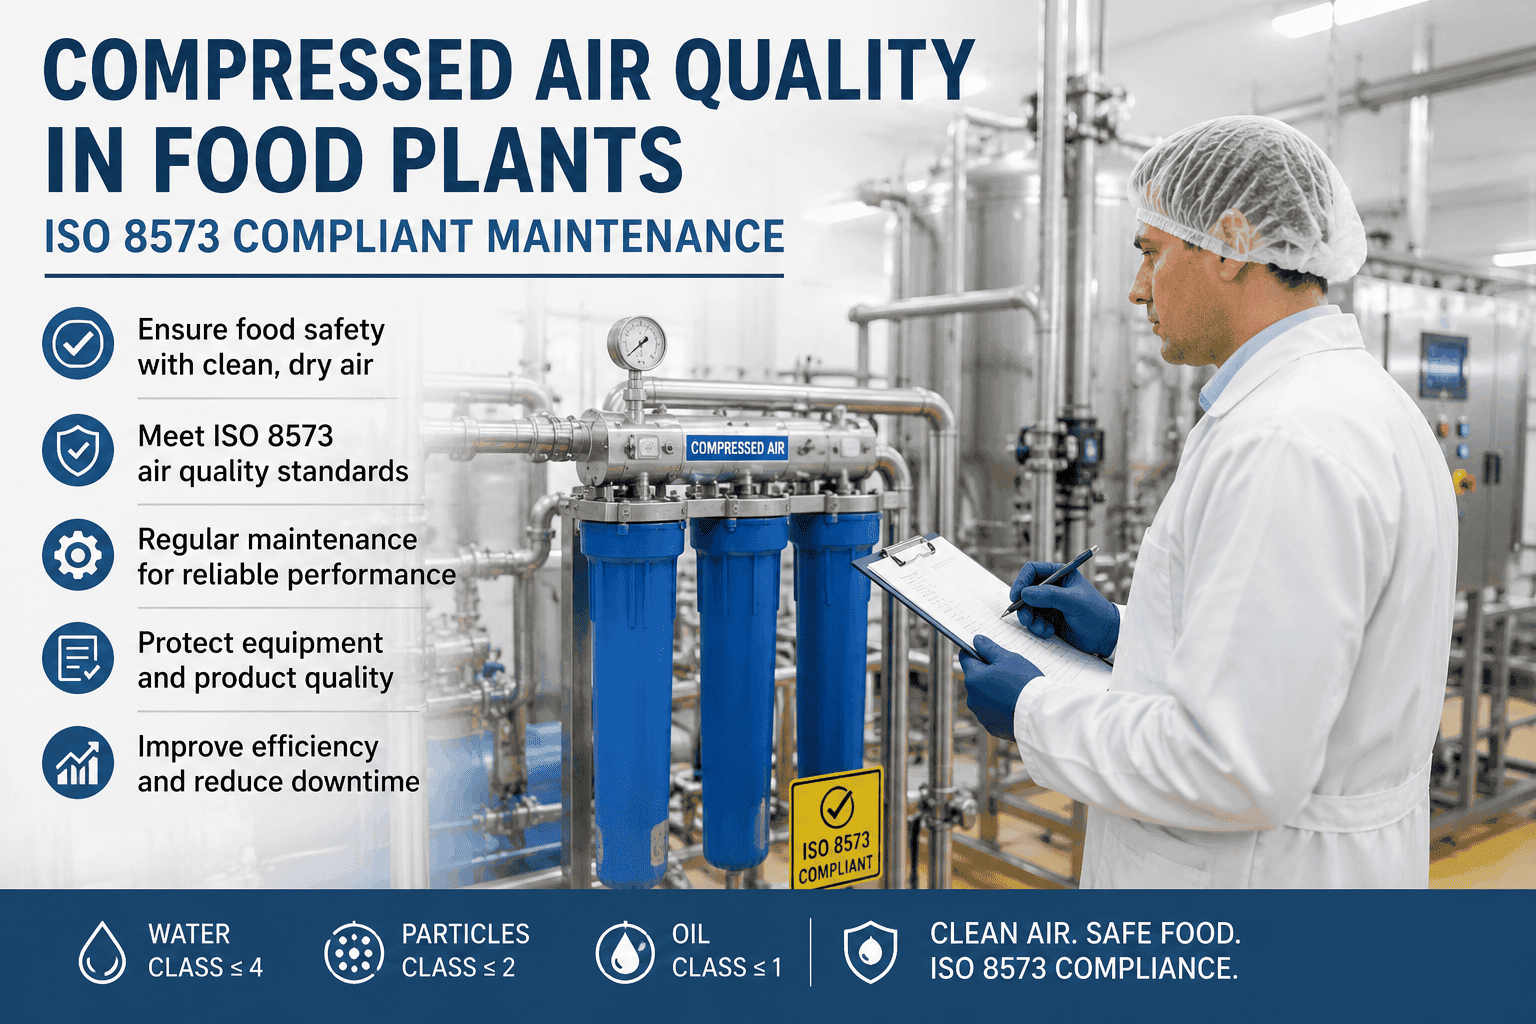
ISO 8573-1 describes air quality in three categories and assigns each a class number, where lower means purer and zero is the most stringent. Industry guidance for food and beverage uses these classes to set targets.
What published guidance adds
- The British Compressed Air Society Food Grade Compressed Air Best Practice Guideline was prepared with the British Retail Consortium and aligns with food safety schemes and ISO 22000-based requirements.
- It separates purity targets for direct contact and indirect contact with food or beverage.
- It recommends verifying air purity at least twice a year unless the HACCP process identifies a different frequency.
- It stresses qualified personnel and a maintenance regime that keeps purity at the level specified.
Give Compressors, Dryers and Filters the Same Schedule as Production Equipment
Oxmaint helps maintenance teams schedule filter changes, drain checks and compressor service, record readings on mobile devices, and keep results attached to each utility asset.
Maintaining Each Stage of the Treatment Train
Each stage protects the next. If one fails, the stages after it work harder or fail too, so walk the train in order when troubleshooting.
| Stage | What goes wrong | What to inspect | Maintenance action |
|---|---|---|---|
| Intake | Dust, humidity and nearby vapors drawn in | Intake location, intake filter condition | Replace filters, relocate intake if contaminated |
| Compressor | Oil carryover, overheating, worn seals and separators | Oil level and condition, temperatures, separator element | Service per manufacturer, replace separators and oil on schedule |
| Aftercooler and separator | Fouled coolers, failed drains | Discharge temperature, condensate removal | Clean coolers, service drains |
| Receiver | Accumulated condensate and corrosion | Drain function, external condition | Drain checks, vessel inspection as required |
| Dryer | Rising dew point, desiccant exhaustion, refrigerant or heat faults | Dew point reading, alarms, purge function | Service dryer, replace desiccant per manufacturer |
| Filters | Saturated elements, bypass, wrong grade for the duty | Differential pressure, element age, housing seals | Replace elements on condition and schedule |
| Distribution piping | Scale, leaks, wet low points, dead legs | Leak surveys, drain legs, condition of piping | Repair leaks, add drains, remove unused branches |
| Point of use | Missing final filters, damaged hoses, shared connections | Filter and hose condition, connection labeling | Replace worn parts, label food-contact outlets |
Six Filter and Dryer Habits That Prevent Most Problems
These routines are simple, and most plants can start them this month without new equipment.
- Tip 1Fit and read differential pressure gaugesRising pressure drop across a filter signals loading. Record readings on each round so the trend, not a single number, triggers action.
- Tip 2Change elements on the earlier of condition or scheduleFollow the manufacturer's time limit even when pressure drop looks fine, since elements can lose performance without a visible change.
- Tip 3Record element change dates and part numbersA filter housing with no history is hard to defend. Log the date, grade and who fitted it, for each housing.
- Tip 4Watch dryer dew point dailyA rising dew point means water is getting through. Catch it early, before wet air reaches filters and product areas.
- Tip 5Prove drains actually drainAutomatic drains fail closed or open. Check each one on a schedule and note any that need repair.
- Tip 6Keep spares for critical filtersMissing elements lead to delayed changes. Stock the grades used at food-contact points first.
Oil-Free or Oil-Lubricated: What Each Choice Means for Maintenance
Oil-free compressors reduce the chance of oil entering the air, but they still need drying, filtration and monitoring. Lubricated machines can serve food plants with the right treatment and discipline.
Oil-free compressors
- Remove the compressor as a source of oil carryover
- Still need intake care, drying and particulate filtration
- Maintenance focuses on seals, elements, cooling and condensate
- Oil vapor from the intake air still has to be considered
Oil-lubricated compressors
- Rely on separators and coalescing filters to control oil
- Separator and filter condition become central safety checks
- Where the compressor lubricant could reach product through air, use a food-grade lubricant as appropriate
- Oil testing at points of use confirms performance
Building a Purity Testing Routine Around Real Risk
Testing converts assumptions into evidence. Plan it with quality and food safety, and tie the frequency to your HACCP assessment.
- 1List every air use and its contact levelInclude hidden points such as air knives, container blow-off and pneumatic conveying.
- 2Set a purity target for each contact levelUse recognized guidance and your risk assessment to select classes for particles, water and oil.
- 3Choose sampling pointsSample at representative points of use, especially those at direct contact, and at the plant outlet for baseline.
- 4Set frequency and responsibilitiesGuidance commonly points to at least two checks a year unless your hazard analysis calls for different intervals.
- 5Record, review and act on resultsCompare results with targets, investigate failures and open corrective work on equipment found responsible.
Warning Signs Your Compressed Air Needs Attention
Operators and technicians often notice problems before any test does. Give them a simple way to report these signs.
Leaks, Pressure Drop and Energy: Why Quality and Cost Move Together
A well-maintained system is usually also an efficient one. The same inspections that protect quality tend to reveal wasted energy.
- Leak surveys reduce compressor run time and keep pressure steady at points of use.
- Clean filters limit pressure drop, so the compressor does not need a higher setpoint to compensate.
- Working drains and dryers stop moisture from adding load and corrosion downstream.
- Removing unused piping branches reduces leak points and dead legs where condensate collects.
- Trending compressor run hours and load against production helps spot gradual loss before a failure.
How Oxmaint Helps Run a Compressed Air Program
Oxmaint treats utility equipment as assets with schedules, readings and history, so air quality work is as visible as work on production lines.
- Compressor room assets organized by system and point of use
- Preventive schedules for filters, separators, desiccant and drains
- Inventory for elements and consumables
- Mobile checklists for rounds, with readings and photos
- Work orders that record element changes and repairs
- Corrective work raised from out-of-range readings
- Completion history by asset for audits and reviews
- Test results and certificates attached to records
- Dashboards showing overdue and upcoming tasks
Simple Measures to Track Compressed Air Health
Start with a handful and review them monthly alongside quality results.
A Thirty-Day Plan to Bring Compressed Air Under Control
You do not need a capital project to improve air quality control. A focused first month builds the register, the routines and the baseline that every later improvement depends on.
- W1Walk the system and build the registerList compressors, dryers, filters, receivers, drains and every point of use, with a note on contact level and who owns each item.
- W2Capture baseline readingsRecord dew point, filter differential pressure, compressor temperatures and run hours so future changes have something to compare against.
- W3Set up schedules and sparesCreate recurring tasks for rounds, drain checks and element changes, and stock the elements used at food-contact points.
- W4Plan the first purity testAgree targets and sampling points with quality, book the test and decide how results will trigger corrective work if they miss.
Common mistakes to avoid in the first month
- Buying filters before mapping where air touches product, which leads to over-treating some points and under-treating others.
- Changing elements without recording the date, grade and housing, which leaves no proof later.
- Relying on a single dew point alarm without checking that the sensor itself is calibrated.
- Leaving unused pipe branches connected, where condensate and microbial growth can accumulate.
- Treating compressed air as the maintenance team's concern alone, when quality and sanitation share the risk.
Compressed Air in Food Plants FAQs
What purity class does food-contact compressed air need?
It depends on whether air contacts product directly or indirectly and on your hazard analysis. Use recognized guidance such as ISO 8573-1 classes and confirm targets with your quality team.
How often should compressed air quality be tested?
Published guidance commonly suggests at least twice a year unless your HACCP process identifies another interval. Record results by sampling point in Oxmaint.
How often should compressed air filters be replaced?
Follow the manufacturer's time limit and the earlier of pressure drop or schedule. Log each change by housing so the history is clear.
Do oil-free compressors remove the need for filtration?
No. Intake contaminants, water and particles still need control, and oil vapor can enter from ambient air. Book a demo to see how utility checks are scheduled.
Can maintenance software prove compressed air quality?
It cannot test the air, but it records maintenance, readings and attached test results. A free trial shows how that evidence stays organized.
Keep Compressed Air Clean, Documented and Easy to Defend
Bring compressor service, filter changes, dryer readings and air quality results into one maintenance system, so utilities that touch product get the same discipline as the line itself.