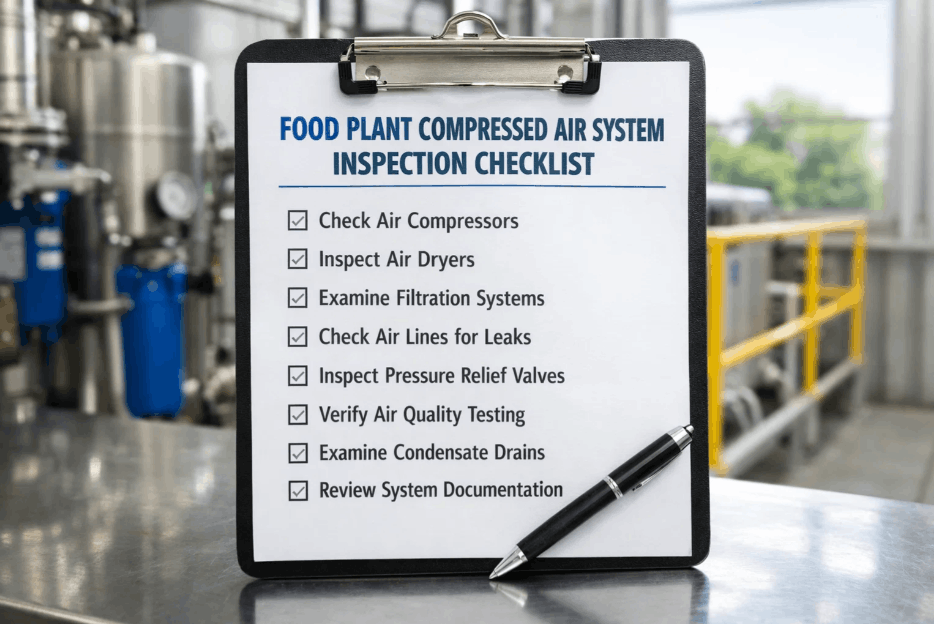
A snack food manufacturer in Texas avoided a $280,000 production disaster when a routine compressor inspection revealed metal particles in the oil sample—the first sign of bearing deterioration that would have caused catastrophic failure within weeks. The maintenance technician following their standardized compressor inspection usa protocol noticed the oil appeared slightly darker than normal, triggering an oil analysis that detected the contamination. Scheduled replacement during a planned shutdown cost $12,000; the unplanned failure would have destroyed the compressor, contaminated the air system with debris, and halted three packaging lines for an estimated four days. Systematic inspection doesn't just prevent failures—it transforms potential catastrophes into manageable maintenance events.
Compressor inspection requires more than checking gauges and listening for unusual sounds. Effective inspection follows a structured protocol that examines mechanical condition, electrical systems, lubrication, cooling, controls, and safety devices. Each inspection point correlates with specific failure modes, and documenting findings creates the trend data that enables predictive maintenance decisions.
Sign up for Oxmaint to access digital inspection templates with automated scheduling and trend analysis, or book a demo to see how digital inspections improve compressor reliability.
Inspection Guide
Compressor Inspection Guide & Report Template
Comprehensive inspection protocols for food manufacturing compressors with standardized documentation templates.
Of Failures Detectable Through Inspection
Maintenance Cost Reduction with Regular Inspection
Of Plants Lack Standardized Inspection Protocols
3-5x
ROI
Return on Inspection Program Investment
Why Structured Inspection Matters
Compressors in food and beverage facilities operate under demanding conditions—continuous duty cycles, temperature extremes, humid environments, and contamination from production processes. These conditions accelerate wear and create failure modes unique to food manufacturing. Without systematic inspection, problems develop undetected until they cause unplanned downtime, product contamination, or safety incidents.
Structured inspection protocols ensure consistency across technicians and shifts. When every inspector follows the same procedure and documents findings in standardized formats, trends become visible that would be missed with ad-hoc approaches. A gradual temperature increase, slowly rising vibration levels, or progressive oil consumption tells a story—but only if captured systematically over time.
78%
of compressor failures show detectable warning signs during routine inspection—elevated temperatures, abnormal sounds, oil condition changes, or pressure anomalies. Structured inspection protocols catch these indicators before they progress to failure.
Inspection Frequency Guidelines
Inspection frequency depends on compressor criticality, operating conditions, and failure history. These guidelines provide starting points—adjust based on your specific equipment and experience.
Operational Verification
Quick operational checks during production startup or shift changes to verify basic function and catch obvious problems.
Operating pressure verification
Temperature readings
Oil level check
Unusual sounds or vibration
Leak detection (audible)
Detailed Operational Review
More thorough examination of operating parameters, filtration, electrical, and safety systems during lower-demand periods.
Filter differential pressures
Oil color and condition
Electrical current draw
Condensate drain function
Control system operation
Comprehensive System Review
Complete inspection of all mechanical, electrical, and safety systems with documentation and trend analysis.
Belt tension and condition
Coupling alignment check
Safety valve verification
Electrical connection inspection
Vibration measurements
Major Inspection & Overhaul Assessment
Comprehensive internal inspection during planned shutdown to assess wear, plan rebuilds, and verify regulatory compliance.
Valve inspection and measurement
Bearing clearance checks
Motor insulation testing
Pressure vessel inspection
Complete oil system service
Access Digital Inspection Templates
Oxmaint provides mobile-ready inspection forms with automated scheduling, photo documentation, and trend tracking built in.
Compressor Inspection Report Template
Use this standardized format to document inspection findings. Consistent documentation enables trend analysis and supports maintenance planning decisions.
Equipment Identification
Asset ID / Tag Number
Equipment Make / Model
Serial Number
Location / Area
Inspection Details
Inspection Date / Time
Inspector Name / ID
Inspection Type (Daily/Weekly/Monthly/Annual)
Run Hours at Inspection
Discharge Pressure (PSI)
_______
100-125
OK / ALERT
Suction Pressure (PSI)
_______
Atmospheric
OK / ALERT
Discharge Temperature (°F)
_______
180-220
OK / ALERT
Oil Temperature (°F)
_______
160-200
OK / ALERT
Oil Pressure (PSI)
_______
Per spec +15
OK / ALERT
Motor Amps (Phase A/B/C)
___/___/___
< FLA
OK / ALERT
Belt Condition
Good / Worn / Cracked / Replace
Belt Tension
Correct / Too Loose / Too Tight
Coupling Condition
Good / Worn / Misaligned
Vibration Level
Normal / Elevated / Excessive
Unusual Sounds
None / Knocking / Hissing / Grinding
Mounting Bolts
Tight / Loose / Missing
Oil Level
Full / Low / Critical / Added ___qt
Oil Color
Clear / Amber / Dark / Milky
Oil Filter Differential
Normal / Elevated / Replace
Oil Leaks
None / Minor Seep / Active Leak
Crankcase Heater
Functional / Not Working / N/A
Oil Sample Taken
Yes / No / Sent to Lab
Voltage (L1-L2-L3)
___V / ___V / ___V
Phase Balance
< 2% / 2-5% / > 5%
Contactor Condition
Good / Pitted / Replace
Connection Tightness
All Tight / Retorqued / Corroded
Thermal Scan Results
Normal / Hot Spots Found / N/A
Ground Continuity
Good / Marginal / Failed
Relief Valve Condition
Sealed / Tested / Leaking
High Pressure Cutout
Setpoint Verified / Tested / Adjust
High Temperature Alarm
Functional / Tested / Not Working
Oil Pressure Safety
Functional / Tested / Not Working
Emergency Stop
Functional / Tested / Not Working
Guards in Place
All Present / Missing / Damaged
Corrective Actions Required:
Priority (Immediate/Scheduled/Monitor):
Digitize Your Inspection Process
Replace paper forms with mobile inspections that capture photos, track trends, and automatically generate work orders.
Common Inspection Findings and Their Significance
Understanding what inspection findings indicate helps prioritize corrective actions and predict developing problems.
Indicates
Inadequate cooling, low refrigerant (if applicable), worn valves, high compression ratio, or lubrication problems.
Action Required
Check condenser/cooler function, verify oil level and condition, inspect intake filtration, measure valve efficiency.
Indicates
Oil breakdown from overheating, contamination from worn components, moisture ingress, or extended service beyond change interval.
Action Required
Send sample for analysis, change oil and filter, investigate root cause before resuming operation.
Indicates
Bearing wear, coupling misalignment, belt problems, loose mounting, or internal component wear.
Action Required
Perform vibration analysis to identify source, check alignment and mounting, inspect bearings and belts.
Indicates
Mechanical binding, bearing failure developing, electrical problems, high discharge pressure, or restricted intake.
Action Required
Compare to historical baseline, check voltage and phase balance, verify operating pressures, inspect for mechanical binding.
Indicates
Control system issues, unloader valve problems, check valve failure, leaks in system, or capacity mismatch with demand.
Action Required
Verify control settings, test unloader and check valve function, perform leak detection, evaluate system capacity.
Indicates
Worn piston rings or valve seals, oil separator failure, external leaks, or operating temperature causing oil carry-over.
Action Required
Track consumption rate, check oil separator, inspect for leaks, verify operating temperature, plan internal inspection.
Inspection Best Practices
1
Establish Baseline Readings
Document normal operating parameters for each compressor when newly installed or after major service. Without baselines, you can't identify gradual degradation trends.
2
Inspect at Consistent Conditions
Take readings under similar operating conditions each time—same load state, ambient temperature range, and runtime. This enables meaningful trend comparison.
3
Include all senses in inspection—not just gauges. Listen for unusual sounds, feel for abnormal vibration or heat, look for oil stains and discoloration, even smell for burning or overheating.
Use All Your Senses
4
Document with Photos
Photograph findings to create visual records. Images of oil color, belt condition, or leak locations communicate more than text descriptions and enable comparison over time.
5
Review Trends Regularly
Monthly review of inspection data reveals gradual changes invisible in single inspections. Plot key parameters over time to identify developing problems early.
6
Close the Loop on Findings
Ensure every deficiency identified generates a work order and gets resolved. Inspections that identify problems but don't drive corrective action waste effort.
Frequently Asked Questions
How do I determine the right inspection frequency for our compressors?
Start with manufacturer recommendations adjusted for your operating conditions. Critical compressors supporting food safety requirements warrant more frequent inspection. Track findings over time—if inspections consistently find no issues, frequency may be excessive; if problems are discovered too late, increase frequency.
What qualifications do inspectors need?
Daily operational checks can be performed by trained operators. Weekly and monthly inspections require maintenance technicians familiar with compressor systems. Annual comprehensive inspections may require specialized technicians or manufacturer service for internal assessments and regulatory compliance verification.
How do we transition from paper to digital inspection forms?
Start by digitizing your existing forms to maintain familiarity while gaining digital benefits. Train inspectors on mobile devices and verify connectivity in compressor areas.
Sign up for Oxmaint to access mobile inspection templates designed for industrial environments.
What regulatory requirements apply to compressor inspection?
Requirements vary by jurisdiction and application. OSHA requires pressure vessel inspection. State boiler codes may apply to receivers. Food safety programs (SQF, BRC, FSSC 22000) require documented preventive maintenance. Consult local authorities and your food safety team for specific requirements.
How long should we retain inspection records?
Retain inspection records for the life of the equipment plus any regulatory retention requirements. Food safety programs typically require 2-3 years minimum. Digital records with unlimited retention enable long-term trend analysis that reveals gradual degradation patterns.
Standardize Your Compressor Inspections
Oxmaint provides digital inspection templates with automated scheduling, photo documentation, trend tracking, and automatic work order generation for identified deficiencies.