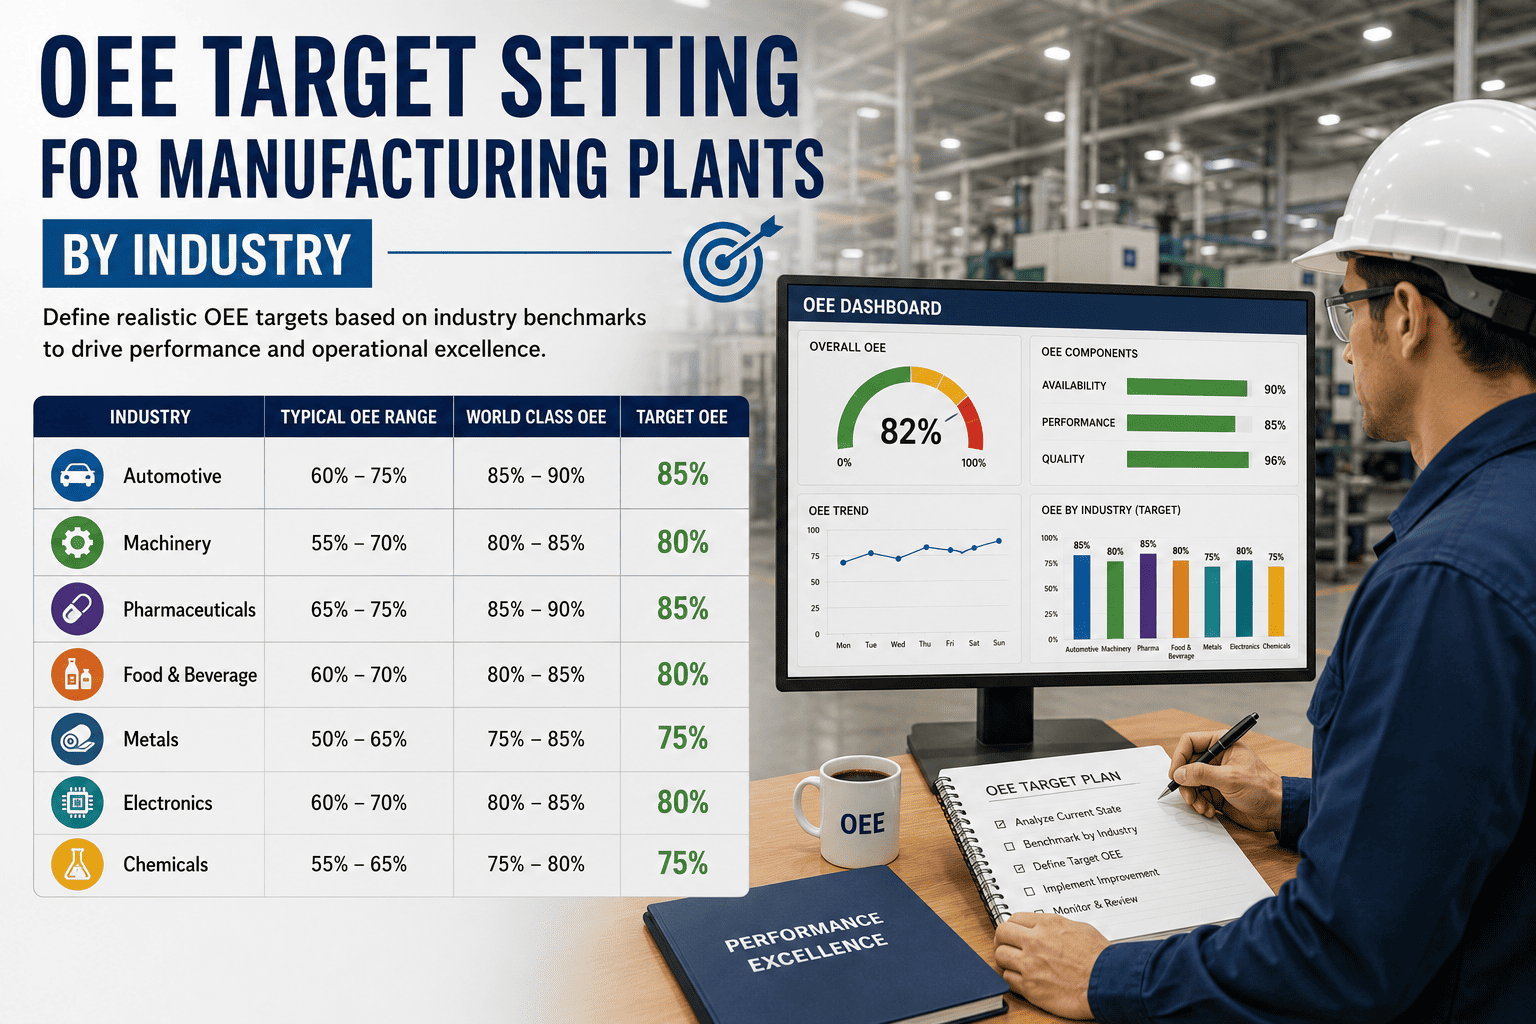
Overall Equipment Effectiveness is the one number most plants track religiously and set carelessly — managers copy the famous 85% "world-class" benchmark onto every line regardless of industry, asset age, or product mix, then wonder why operators either coast or burn out. Realistic OEE targets must be calibrated to your sector's typical performance, your current baseline, and the realistic improvement runway your maintenance program can sustain over twelve months. This guide breaks down defensible OEE targets for automotive, food, pharma, plastics, and metals plants, plus a month-by-month roadmap for closing the gap using CMMS-driven reliability practices. Ready to turn targets into a plan? Start Free Trial and baseline your assets in under a week.
OEE TARGET SETTING GUIDE
Is your OEE target quietly sabotaging your plant?
A target 8 points too low breeds complacency. A target 12 points too high burns out crews inside a quarter. The right number is sector-specific, baseline-anchored, and sequenced over a 12-month runway — not pulled from a benchmark poster on the breakroom wall.
THE TARGET-SETTING EQUATION
Why one OEE number never fits every plant
World-class OEE is widely cited at 85%, but that figure originated from Nakajima's TPM work in Japanese automotive tier-1 plants in the late 1980s — and it assumes mature autonomous maintenance, operator-owned reliability, and AM/FM schedules running above 90% adherence.
THE CORE FORMULA
Availability = run time ÷ planned production time. Performance = ideal cycle time ÷ actual cycle time. Quality = good units ÷ total units. Each component must be tracked separately — a single blended number hides where the loss actually lives.
REALISTIC TARGET FORMULA
Year-one target captures roughly 40% of the gap between your current OEE and your sector's realistic ceiling. A plant at 58% with a 78% ceiling targets 66% — ambitious enough to stretch, grounded enough to sustain without heroics.
A 180-asset automotive components plant running three shifts measures baseline OEE at 61% across its CNC machining cells. Its sector ceiling sits near 82%. Applying the formula: 61 + (82 − 61) × 0.40 = 69.4% for year one. Pushing for 78% in twelve months would require cutting unplanned downtime by 45% — physically possible only with a CMMS-driven PM program that doesn't yet exist. Sequencing matters more than ambition.
OEE TARGETS BY MANUFACTURING INDUSTRY
Benchmark targets for five core sectors
These ranges blend published industry data with field observation from hundreds of CMMS deployments. "Typical" reflects the median plant; "achievable ceiling" reflects what a disciplined 12-month reliability program reaches without capital overhauls.
| Industry | Typical OEE | Achievable Ceiling | Year-1 Target | Biggest Loss Driver |
|---|---|---|---|---|
| Automotive (Tier 1) | 65–72% | 82% | 70–76% | Changeover duration |
| Food & Beverage | 55–68% | 76% | 64–71% | Sanitation changeover |
| Pharmaceuticals | 58–66% | 74% | 64–69% | Validation batches |
| Plastics & Rubber | 52–64% | 72% | 60–67% | Scrap & startup yield |
| Metals & Fabrication | 50–62% | 70% | 58–66% | Tool wear & setup |
Average SMED-able changeover in automotive tier-1 — cutting it to 9 minutes recovers 6 OEE points without touching availability.
Share of food-plant OEE loss traceable to sanitation changeovers — schedulable, measurable, and CMMS-controllable.
Pharma batch rejection rate at plants without electronic batch records — drops below 3% once CMMS-captured deviations replace paper logs.
WORLD-CLASS VS TYPICAL — CALIBRATING EXPECTATIONS
The 85% myth and what to aim for instead
Most plants chasing 85% OEE fail not because the number is impossible, but because they treat it as a year-one destination rather than a 5-year maturity outcome. Here is how the two standards actually compare — and where your plant should position itself.
- Availability 72% — unplanned downtime dominates
- Performance 89% — minor stops and speed loss
- Quality 96% — rework visible but not systematically tracked
- PM adherence below 70%, mostly reactive dispatch
- Availability 90%+ — predictive maintenance at scale
- Performance 95% — speed losses engineered out
- Quality 99%+ — SPC and autonomous maintenance embedded
- PM adherence above 95%, condition-based triggers active
"Plants that reach 85% OEE didn't set 85% as their year-one target. They set 68%, hit it, reset to 74%, hit it, and compounded. The target is a stepping stone — not a billboard."
— Reliability engineering consensus across 400+ CMMS deployments
THE 12-MONTH IMPROVEMENT ROADMAP
How to sequence OEE gains without breaking the team
A defensible OEE roadmap moves through four phases — baseline, stabilize, accelerate, sustain — each tied to a specific CMMS capability coming online. Skipping phases is the single most common reason improvement programs collapse in month seven.
Instrument and measure honestly
Deploy CMMS asset registry, wire up downtime reason codes (top 10 only — Pareto discipline), and capture 90 days of clean data. Expect measured OEE to drop 4–8 points as hidden losses surface. Target shift: no OEE change yet, but data integrity above 95%.
Kill the top-3 downtime causes
RCA on the three largest loss codes, rebuild PM checklists inside CMMS, launch lubrication and inspection routes. Availability typically climbs 4–6 points. OEE movement: +3 to +5 points — the first number that sticks because it is earned, not willed.
Attack speed loss and changeover
SMED events on bottleneck assets, ideal cycle-time recalibration, minor-stop tracking via CMMS sensors. Performance climbs 3–5 points as true bottlenecks surface. OEE movement: another +2 to +4 points. This is where most plants plateau without sustained discipline.
Lock in quality and condition-based triggers
Vibration and thermal sensors on critical assets, SPC integration, autonomous maintenance routines owned by operators. Quality rises 1–2 points and availability holds. OEE movement: +1 to +2 points — smaller increments, but the baseline no longer erodes.
GAP ANALYSIS — FINDING YOUR REAL CEILING
Where your OEE is actually leaking
Before setting a target, you need a gap analysis that isolates the six standard big losses. The pattern of loss — not the total — determines what your ceiling actually is and which phase of the roadmap will move the needle first.
Equipment failure
Unplanned breakdowns. Target below 5% of scheduled time. CMMS predictive triggers and PM adherence above 90% are the primary levers.
Setup & adjustment
Changeover time. SMED methodology can cut this 50–70%. Schedulable, so it inflates planned downtime rather than availability — but still erodes OEE.
Idling & minor stops
Under-five-minute stoppages — jams, sensor faults, misfeeds. Hardest loss to track without IoT sensors feeding CMMS. Often 8–12% of available time.
Reduced speed
Running below nameplate cycle time. Operators slow lines deliberately to mask quality issues — the loss hides in performance and compounds silently.
Process defects
Scrap and rework during steady-state running. SPC and tightened PM tolerances reduce this; CMMS deviation logs make it visible per shift.
Startup yield
Scrap produced from machine startup to first good part. Standardized warm-up procedures and CMMS startup checklists cut this 30–50%.
CMMS-DRIVEN OEE PLANNING
Set targets your team can actually hit — and beat
OxMaint's CMMS baselines your real OEE in under a week, isolates the six big losses by asset, and builds a 12-month improvement roadmap calibrated to your industry ceiling.
FREQUENTLY ASKED
OEE target setting, answered
Is 85% OEE a realistic target for most plants?
No — 85% is a 3-to-5-year maturity outcome, not a year-one target. Most plants sit between 55% and 70% OEE. A realistic 12-month target captures roughly 40% of the gap between your current baseline and your industry's achievable ceiling, which lands most plants in the 66–72% range. Chasing 85% before the CMMS, PM, and condition-monitoring infrastructure exists will demoralize crews and erode data trust. Start Free Trial to baseline your true number first.
How do I know if my OEE target is too high?
If your team needs a 30%+ reduction in unplanned downtime in a single year to hit it, the target is too high without a greenfield reliability program. A second signal: if your OEE movement requires performance above 97% or quality above 99% on aging assets, you are asking the equipment to outperform its design condition. Recalibrate using the baseline-plus-40%-gap formula.
Should OEE targets differ by line or be plant-wide?
They should differ by line — ideally by bottleneck asset. A plant-wide OEE number averages away the losses that matter and lets strong lines mask weak ones. Set targets at the constraint-asset level, roll up to the line, then to the plant. This is why a CMMS with asset-level downtime tracking is non-negotiable for credible OEE target setting.
How often should OEE targets be revisited?
Quarterly for operational targets, annually for strategic targets. If you hit your year-one target in month nine, do not auto-bump it — investigate whether the gain is structural (PM adherence, SMED) or situational (a favorable product mix). Structural gains justify a reset; situational gains do not. Book a Demo to see how OxMaint automates that structural-vs-situational split.
What OEE target should a food and beverage plant set?
Most F&B plants run between 55% and 68% OEE, dragged down by sanitation changeovers and CIP cycles that can consume 35–40% of available time. A realistic year-one target is 64–71%, achieved by scheduling and optimizing sanitation windows through CMMS rather than treating them as fixed. The sector ceiling without major capex sits near 76%.
READY TO CLOSE THE GAP?
Turn your OEE target into a 12-month execution plan
Baseline your assets, isolate the six big losses, and build a sector-calibrated roadmap your operators will actually buy into — all inside OxMaint's CMMS.
Free 14-day trial · No credit card