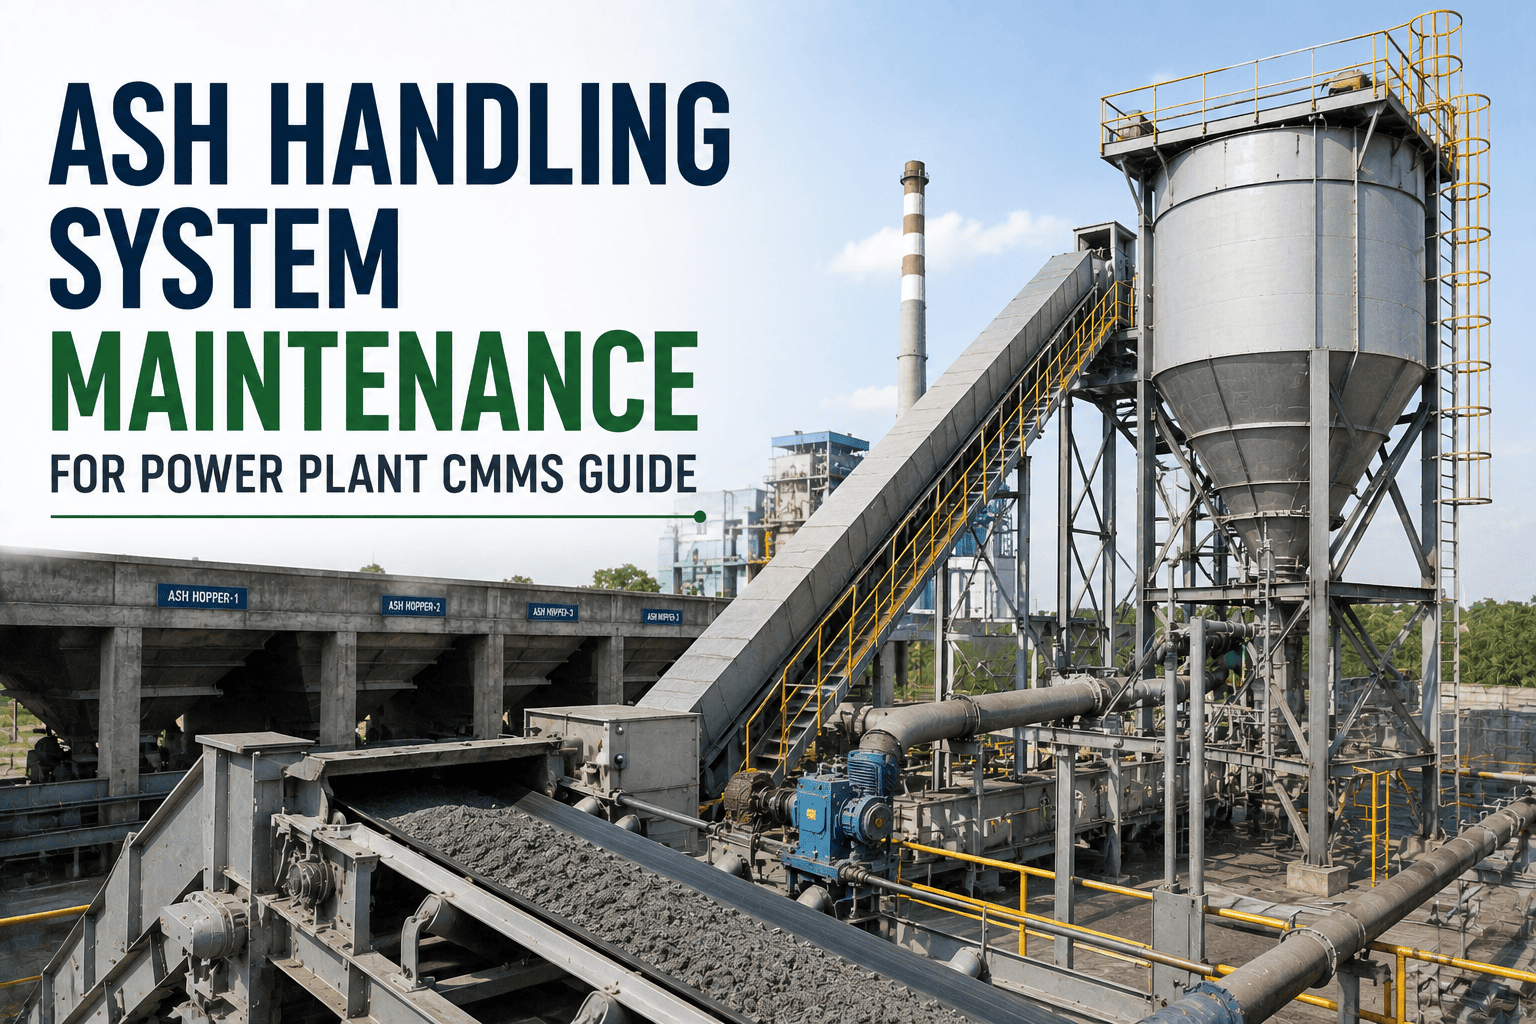
Ash handling systems are the least glamorous — and most frequently neglected — asset group in a thermal power plant. Bottom ash falls continuously from the boiler into the submerged scraper conveyor trough below. Fly ash loads the ESP hoppers field by field, extracted in pulses by vacuum pumps and pushed pneumatically to silos hundreds of meters away. Every component in this chain — SSC chains, drag flights, dome valves, pneumatic conveying lines, clinker grinders, and slurry pumps — operates in conditions that destroy unprotected metals: abrasive ash, high temperatures, corrosive slurry, and continuous duty cycles. When one component fails, it does not fail alone. An SSC chain snap at 2 AM forces an emergency boiler load reduction. A blocked ESP hopper backs up fly ash into the electrostatic field and degrades precipitator performance. A seized clinker grinder holds up the entire bottom ash extraction sequence. The common thread in all of these events is the same: no structured, CMMS-tracked maintenance program that caught the warning before the failure. This guide covers the complete maintenance framework for ash handling systems in thermal power plants, with a specific focus on submerged scraper conveyor PM programs, fly ash system inspection schedules, and the CMMS records that make the difference between a planned overhaul and an emergency shutdown. Connect your ash handling assets to Oxmaint free and run your first PM campaign today, or book a 30-minute demo to see ash handling maintenance workflows live.
Ash Handling System Maintenance and Submerged Scraper Conveyor Programs
Bottom ash, fly ash, SSC chains, ESP hoppers, clinker grinders, and pneumatic conveying lines — the complete maintenance and CMMS program for every component in the ash handling chain.
How a Thermal Power Plant Ash Handling System Actually Works
Ash is produced in two forms during coal combustion: bottom ash (approximately 20% of total ash), which collects in the boiler hopper beneath the furnace, and fly ash (approximately 80%), which is carried upward in flue gases and captured by electrostatic precipitators, economizer hoppers, and air preheater hoppers. Each form requires a completely separate handling chain, and each chain has its own critical maintenance requirements. A maintenance failure anywhere in either chain creates a disposal bottleneck that threatens continuous boiler operation.
Submerged Scraper Conveyor Maintenance: The Highest-Consequence Asset in Ash Handling
The SSC operates continuously, submerged in a water trough directly beneath the boiler, removing hot bottom ash while simultaneously cooling it and maintaining the airtight seal between the boiler and the ash handling system. A breach in that seal means uncontrolled air ingress into the furnace — an immediate boiler control emergency. The SSC's chain, drag flights, sprockets, trough liner, and sealing system each have distinct failure modes and maintenance intervals. All findings must be logged in a CMMS asset record that shows trend, not just snapshot.
Ash Handling PM Schedule: Interval-by-Interval Reference
The PM intervals below are derived from manufacturer specifications and operating experience at coal-fired thermal plants. Every task must be scheduled as a work order in a CMMS — not a paper calendar. Condition readings captured during PM tasks should be stored against the asset record and trended, not just checked against pass/fail thresholds. It is the trend, not the single reading, that predicts the next failure window.
Run your first ash handling PM campaign in Oxmaint — this week
Oxmaint pre-loads ash handling PM templates for SSC, ESP hoppers, vacuum pumps, pneumatic conveying, and fly ash silos. Work orders route automatically to the right technician, condition data is trended per asset, and audit-ready reports generate without manual prep.
Ash Handling Asset Maintenance Quick Reference
| Asset | Critical Failure Mode | Warning Signs | PM Interval | CMMS Trigger |
|---|---|---|---|---|
| SSC Chain | Chain snap — boiler load reduction forced | Elongation increase, link pitting, skip sounds | Weekly elongation check | Elongation exceeds 2% of nominal pitch |
| Drag Flights | Trough floor erosion, extraction inefficiency | Scraping noise, reduced ash throughput | Monthly wear plate thickness | Plate below 60% original thickness |
| Clinker Grinder | Oversized clinker passes, downstream blockage | Motor current rise, noise on large clinker | Monthly roll gap measurement | Roll gap above OEM maximum setting |
| Dome Valve (Fly Ash) | Seal failure — ash backflow into ESP hopper | Partial-close, sticky actuator, air leak at seat | Weekly cycle test | Actuator stroke time exceeds 5 seconds |
| Vacuum Pump | Loss of extraction vacuum — ESP hoppers fill | Amperage rise, bearing noise, vacuum pressure drop | Daily operating check | Vacuum below required extraction level |
| Pneumatic Conveying Line | Line blockage — fly ash system shutdown | Pressure differential above design, elbow wear-through | Weekly pressure differential | Differential exceeds design range |
| Fly Ash Silo | Bridging / rat-holing — ash not discharging | High-level alarm with no extraction, arch formation | Monthly fluidization pad check | Silo level not dropping on extraction demand |
| Slurry Pump | Impeller wear — disposal capacity drops | Discharge pressure falling, amperage trending down | Monthly performance check | Discharge pressure drop greater than 15% |
Scroll right to view all columns on mobile
What CMMS-Tracked Ash Handling Records Actually Change
The difference between an ash handling system that runs reliably and one that generates a crisis every quarter is almost never the equipment — it is the maintenance program behind it. A CMMS does not replace technical skill. It ensures that the right task gets done at the right interval, that every condition reading is stored and trended, and that when an auditor, insurer, or regulator asks for documentation, the answer is a report — not a search through paper files.
Condition Trending vs Snapshot Checks
SSC chain elongation at 1.4% today means nothing in isolation. The same reading trended over 6 months tells you the rate of wear, when the 2% threshold will be reached, and whether the last operational change accelerated wear. A CMMS stores every reading against time — a paper log does not. Start free on Oxmaint to begin trending your SSC chain data immediately.
Planned Outage Coordination
SSC chain replacement, trough liner overlay, and clinker grinder tooth replacement all require a boiler-coordinated outage. A CMMS that tracks each component's condition against its replacement threshold lets maintenance managers plan a single combined outage window instead of three reactive shutdowns. The cost difference is substantial. Book a demo to see how Oxmaint coordinates ash handling outage planning.
Environmental and Regulatory Compliance
Ash handling systems are subject to environmental permit conditions covering dust emissions, ash disposal records, and operating log requirements. A CMMS generates the PM completion records, corrective work order history, and equipment calibration logs that auditors require — without manual report assembly that consumes maintenance manager time for days before an inspection.
Spare Parts Demand Planning
SSC chain, dome valve diaphragms, pneumatic conveying elbow liners, and vacuum pump wear kits all have known consumption rates under condition-based replacement. A CMMS that tracks part consumption against asset condition history generates accurate reorder triggers — eliminating both the emergency procurement surcharge and the carrying cost of excessive safety stock.
Frequently Asked Questions: Ash Handling Maintenance
What is the most critical maintenance task on a submerged scraper conveyor?
Chain elongation monitoring is the single highest-value task. An SSC chain that snaps during boiler operation forces an emergency load reduction — and the warning is always there weeks ahead in the elongation trend data. Weekly measurement stored in a CMMS with rate-of-wear tracking gives you the planned replacement window instead of a 2 AM emergency. Start free on Oxmaint to set up SSC chain elongation trending on your asset record today.
Why do fly ash pneumatic conveying lines fail so frequently?
The primary cause is elbow liner wear at high-velocity bends, followed by pipeline blockage from insufficient conveying velocity or moisture ingress into dry ash. Ceramic and silicon carbide elbow liners need thickness inspection every 6–8 weeks in high-throughput lines. A CMMS that tracks elbow liner age and pipeline pressure differential trends will predict both failure types ahead of time. Book a demo to see pneumatic line PM workflows in Oxmaint.
How often should ESP hopper heaters be inspected?
Hopper heaters should be verified as energized and operating every shift, and physically inspected for element condition every 3 months. Failed heaters allow ash to cool and cement in the hopper, creating blockages that are extremely difficult to clear without damaging the hopper structure. CMMS-scheduled PM on hopper heaters is one of the lowest-cost, highest-payoff tasks in a fly ash maintenance program. Sign up for Oxmaint to add hopper heater PMs to your ESP asset record.
What records does a coal ash handling program need to maintain for compliance?
Environmental compliance for ash handling typically requires: PM completion records with sign-off dates, corrective work order history for all disposal equipment, ash disposal volume logs, dust suppression system operational records, and water trough quality data for wet systems. Oxmaint generates all of these automatically in exportable formats for environmental audits. Book a demo to see compliance reporting in action.
Can Oxmaint handle both SSC maintenance and fly ash system PMs in the same platform?
Yes. Oxmaint manages the entire ash handling asset tree in a single platform — SSC components, ESP hopper systems, pneumatic conveying lines, vacuum pumps, clinker grinders, and fly ash silos — with separate PM schedules, condition trending, and work order histories per asset. Start free to register your first ash handling assets and run your first PM campaign.
Build a reliable, documented ash handling maintenance program — starting today
Oxmaint connects to your existing sensor infrastructure, runs structured PM schedules for SSC systems, ESP hoppers, pneumatic conveying lines, and fly ash silos, and generates the compliance-ready records your audit team needs — all without paper logs or spreadsheet tracking. Start free with your first ash handling assets, or see a live ash handling PM workflow in a 30-minute demo.