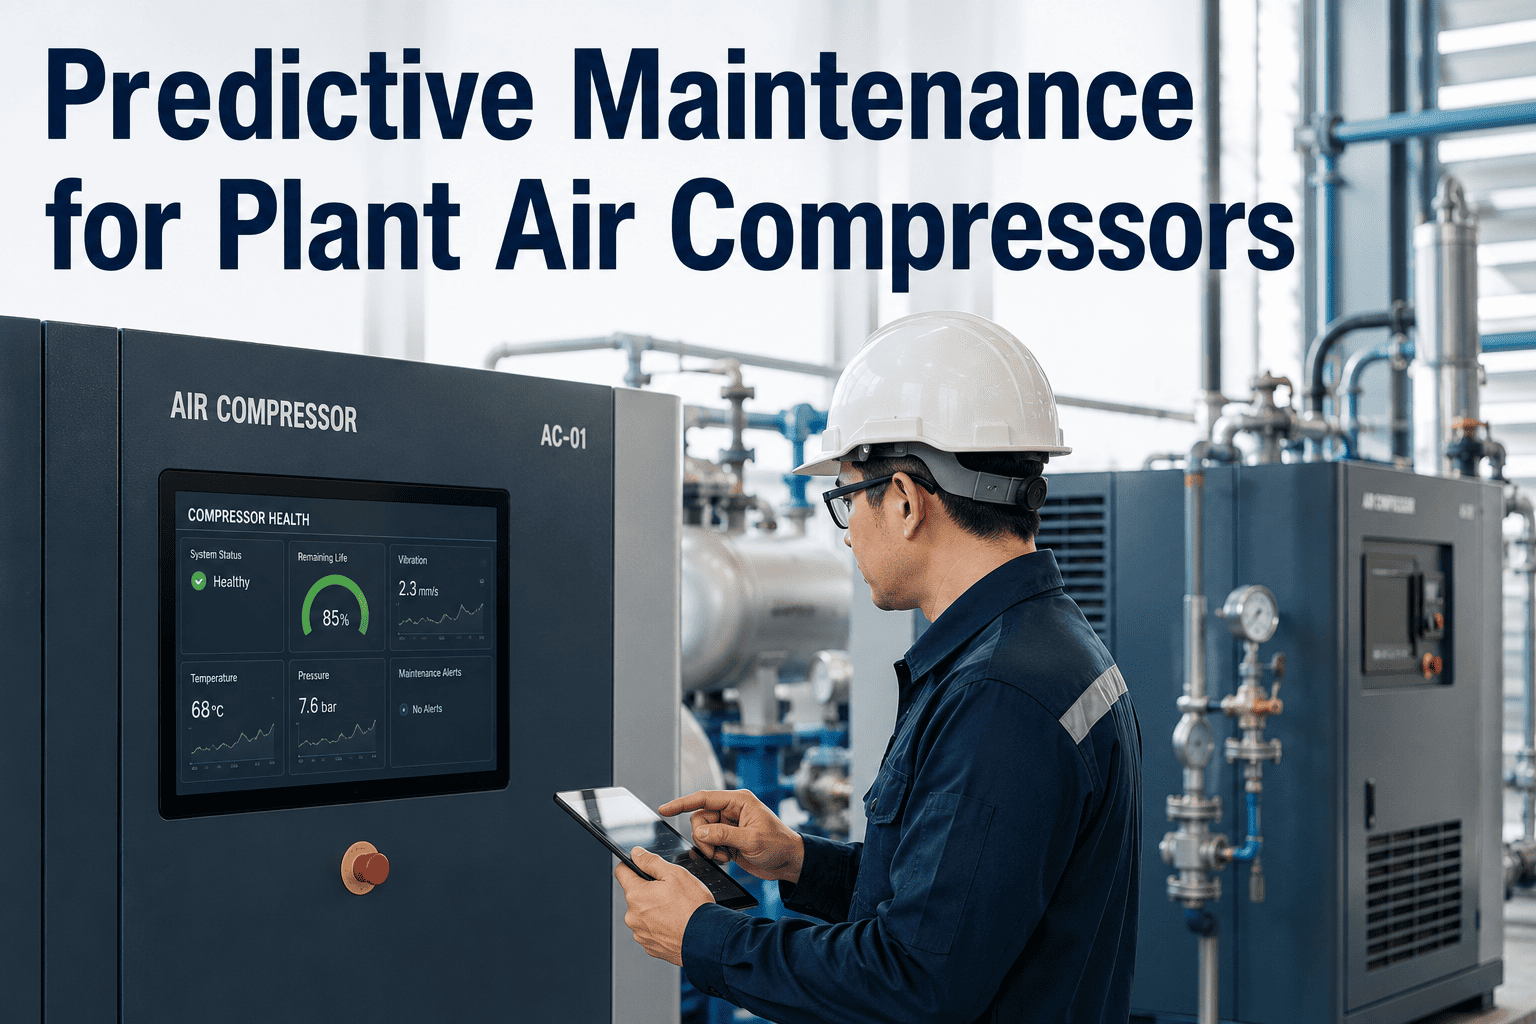
Compressed air is often called the fourth utility, and yet it is usually the least monitored system in the entire plant — pneumatic actuators, instrument air, and control systems all depend on it, but the compressors producing it typically run on a fixed service interval with no visibility into bearing wear, valve condition, or motor health between scheduled shutdowns. When a plant air compressor fails unexpectedly, the ripple effect reaches every pneumatic valve and instrument that depends on stable air pressure, not just the compressor room itself. Sign in to OxMaint to see how predictive monitoring on your compressed air system prevents that ripple effect before it starts.
OxMaint · Auxiliary Equipment · Predictive Maintenance
Your plant runs on compressed air. Your compressors are running on guesswork.
Predictive maintenance on plant air compressors catches bearing wear, valve degradation, and motor issues weeks before they turn into an unplanned air system outage.
The Failure Modes That Take Down a Plant Air Compressor
Compressor failures rarely come out of nowhere. Each major failure mode develops through a detectable degradation pattern well before the unit actually stops producing air.
Mechanical
Bearing Wear
Rising vibration amplitude and characteristic frequency signatures appear well before a bearing seizes, giving weeks of advance warning if vibration is actually being tracked.
Mechanical
Valve Plate Fatigue
Reciprocating compressor valve plates fatigue from repeated impact loading, showing up first as a subtle drop in volumetric efficiency and discharge pressure stability.
Thermal
Cooling System Degradation
Fouled intercoolers and aftercoolers raise discharge temperature gradually, increasing thermal stress on downstream components long before a high-temperature trip occurs.
Electrical
Motor Winding Insulation Aging
Insulation resistance decline and rising motor current imbalance are measurable months before a winding fault takes the motor offline entirely.
Contamination
Lubricant Degradation
Oil analysis reveals viscosity breakdown and wear metal accumulation that precede accelerated component wear, especially in screw compressors running continuous duty.
Control
Sensor and Control Drift
Pressure and temperature sensors drift out of calibration over time, causing the control system to make decisions based on inaccurate readings long before anyone notices the discrepancy.
What an Unplanned Compressor Outage Actually Costs
The direct repair cost of a compressor failure is usually the smallest part of the total impact. Most of the cost comes from what stops moving elsewhere in the plant while compressed air is unavailable.
15%
Direct repair — parts and labour for the compressor itself
35%
Production impact from pneumatic valves and actuators losing control air
25%
Instrument air loss affecting process control accuracy and safety systems
25%
Restart and stabilization time across every dependent pneumatic system
A compressor failure is rarely just a compressor problem — it is a plant-wide pneumatic system interruption. Predictive monitoring is what keeps that interruption from happening in the first place.
The Monitoring Parameters That Predict Compressor Failure
A practical predictive program does not require monitoring everything — it requires tracking the right parameters against the right baseline for each compressor type.
| Parameter |
What It Reveals |
Recommended Monitoring Frequency |
| Vibration spectrum |
Bearing wear, imbalance, misalignment on rotating elements |
Continuous on critical units, monthly on standby units |
| Discharge temperature trend |
Cooling system fouling, internal wear increasing friction |
Continuous via installed sensors |
| Volumetric efficiency |
Valve wear, ring wear, internal leakage in reciprocating units |
Weekly calculation from flow and pressure data |
| Oil analysis |
Lubricant breakdown, wear metal presence, contamination ingress |
Quarterly, or monthly for continuous-duty units |
| Motor current and insulation resistance |
Winding insulation aging, phase imbalance, bearing drag |
Continuous current monitoring, annual insulation test |
Scroll right to view full table on mobile
Predictive Priorities by Compressor Type
Reciprocating, rotary screw, and centrifugal compressors fail in different ways, so a predictive program has to weight its monitoring priorities differently depending on which type is running in your compressor room.
Reciprocating Compressors
Valve plate condition and volumetric efficiency are the top priority, since valve fatigue from repeated impact loading is the dominant failure mode. Vibration monitoring should focus on crankshaft and piston rod frequencies.
Rotary Screw Compressors
Oil analysis and bearing vibration take priority, since rotor and bearing wear combined with lubricant breakdown are the primary degradation paths in continuous-duty screw units.
Centrifugal Compressors
Surge detection and impeller vibration monitoring are critical, since surge events cause rapid mechanical damage that develops far faster than the gradual wear patterns typical of positive-displacement units.
Frequently Asked Questions — Predictive Maintenance for Plant Air Compressors
OxMaint · Predictive Maintenance · Auxiliary Equipment
Compressed air runs your whole plant. It deserves more than a fixed service interval.
Vibration trending. Discharge temperature monitoring. Volumetric efficiency tracking. Oil analysis and motor health — the predictive layer your compressed air system has been missing.