The control-room console shows a Stage-3 vibration event and an upward trend in inlet differential pressure. The night lead walks the plant floor list in their head: recent filter access work, a late preventive task, a weather report that mentioned high winds, previous pulse-cleaner chatter. Trip the machine and lose generation, or keep running and risk a blade hit that forces an emergency inspection? That decision is the one operators dread — made under time pressure, incomplete context, and with a decade of disconnected historian points and CMMS notes just out of reach. This article shows how long-range historian and CMMS context shapes the operational decision, and how Oxmaint AI converts findings into defensible, auditable maintenance actions — bring your own tags to a 30-minute technical review and see the panes on your records.
Siemens SGT-400 · Inlet Filter House · FOD & Hidden Functions · 2026
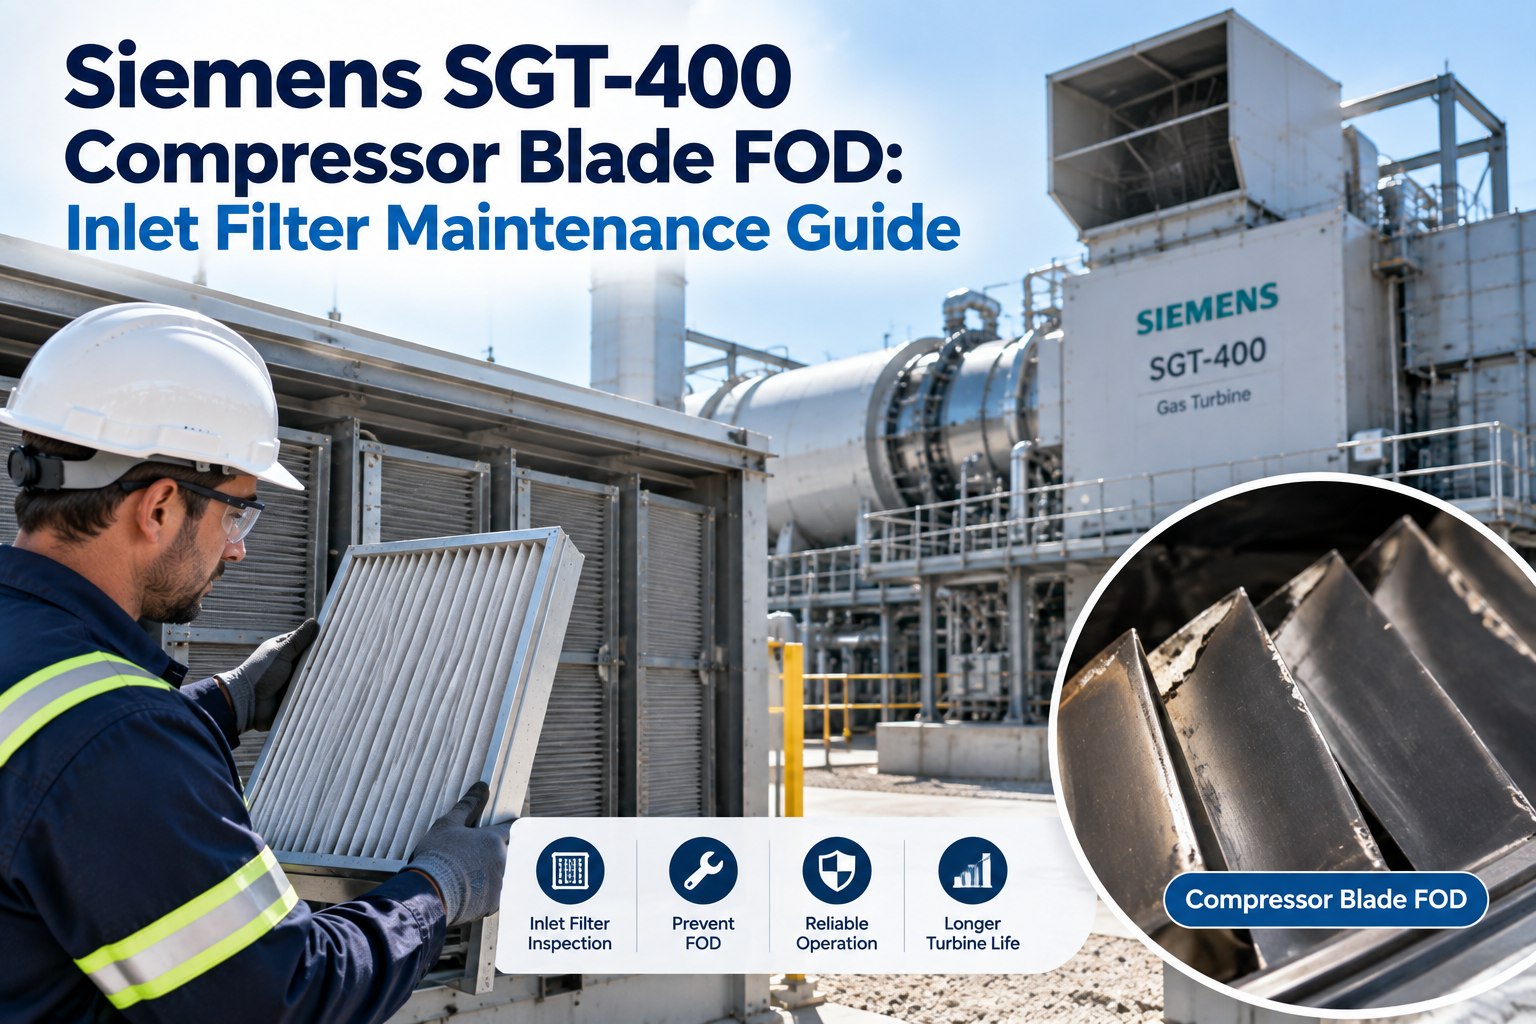
Siemens SGT-400 Compressor Blade Foreign Object Damage: Inlet Filter House Failure Modes and Hidden-Function Testing
Long-range historian + CMMS stitched into three panes — Failure Mode Timeline, Signal → Confidence, Suggested WO → Maximo/SAP — grounded in SAE JA1011 RCM logic. An evidence pipeline that sits on top of your historian and EAM, not a replacement.
02:17
Stage-3 vibration + rising inlet dP event
5–15 yrs
historian + CMMS context stitched per unit
3-Pane
Timeline · Signal → Confidence · Suggested WO
JA1011
SAE-grounded RCM decision logic
What This Guide Covers
Five things a night lead can operationalize today — from long-range context to a closed-loop workflow. Start a free trial to bring your own inlet-filter history.
01
How 5–15 years of historian + CMMS context changes the decision pathway for inlet-filter FOD risk
02
A grouped, in-product pane walkthrough: Failure Mode Timeline · Signal → Confidence · Suggested WO → Maximo/SAP
03
RCM decision logic grounded in SAE JA1011 (functions → functional failures → failure modes → effects)
04
A closed-loop Detect → Diagnose → Prioritize → Dispatch workflow you can operationalize today
05
Practical FAQs and next steps to see your own data
06
Written for the operator moment — trip or keep running, without a decade of disconnected notes out of reach
What the Inlet Filter House Must Do
For the SGT-400, the inlet filter house has two indispensable roles: keep FOD-sized material out of the compressor, and provide early warning of filtration degradation via differential pressure, pulse-jet control feedback, and access/interlock states. Failures in those roles can be immediate and obvious, or slow and hidden — leading to progressive blade damage that only becomes apparent after a costly outage. Book a technical review to walk the two roles on your unit.
Two Indispensable Roles
What the Filter House Does
! Keep FOD-sized material out of the compressor
! Provide early warning of filtration degradation via differential pressure, pulse-jet control feedback and access/interlock states
! Failures can be immediate and obvious — or slow and hidden
! Slow, hidden failures lead to progressive blade damage that only becomes apparent after a costly outage
Typical Hardware On Site
Site Variations Apply
• Cartridge or bag media with pulse-jet cleaning
• Weather hoods and anti-ingestion screens
• Access panels, gaskets and interlocks
• Differential-pressure transmitters and pulse-control valves
A 5–15 Year Historian + CMMS View: What Operators Need to See
Bring together, for a single unit, long-range time series and CMMS records. Correlating those items — timeline stitching and cross-signal correlation — turns scattered facts into an operable "story" about how often pulse cycles stall, when dP has risen persistently after work, or whether vibration spikes preceded maintenance entries. That story is the raw input for targeted verification and intervention. Start a free trial to stitch your own unit's story.
Long-Range View · SGT-400 Inlet Filter House · Single Unit
Time Series
INLET_DP · FLOW_ACTUAL · PULSE_CYCLE_CNT · VIB_AXIAL_1X · AMBIENT_WIND · tag names illustrative
CMMS
Media replacements · pulse-system repairs · late PMs · borescope findings · incident reports
Events
Borescope inspections noting nicks · weather events · access panel work · missed replacements
PATTERN Repeated media changes with later vibration anomalies → candidate hidden failure
PATTERN Periods where pulse cycles stopped updating → chronic pulse-system issue
PATTERN Inspection notes mention minor blade nicks following a weather incident
STORY Scattered facts stitched into a raw input for targeted verification and intervention
In-Product Pane Walkthrough
Three grouped panes take the stitched story from pattern to auditable work order. Book a technical review to see the panes populated with your records.
Pane 1
Failure Mode Timeline
A stitched timeline of key maintenance activities, historian anomalies and inspection outcomes for the inlet filter house. Scan long-range patterns (repeated access work followed by later vibration anomalies) to identify candidate hidden failures such as degraded gaskets or chronic pulse-system issues.
Pane 2
Signal → Confidence
Which signals drive the correlation for a hypothesized failure mode and where gaps exist in instrumentation or records. Confidence is qualitative (strong, medium, weak) and the pane flags contributing signals and absent context — planners know whether to rely on a trending alarm or require hands-on verification.
Pane 3
Suggested WO → Maximo/SAP
A draft, auditable work order with diagnostic and corrective steps aligned to the identified failure mode. Example scope: visual gasket check, bypass-leak smoke test, pulse-valve functional test under simulated conditions, then borescope if tests indicate elevated risk. Push into your EAM with timeline snippets and signal excerpts attached.
Evidence
Auditable Attachments
Illustrative timeline items are qualitative: repeated media changes, periods where pulse cycles stopped updating, inspection notes that mention minor blade nicks following a weather incident. The CMMS record contains the evidence that justified the task.
Evidence Pipeline — Not a Replacement for Maximo, SAP or Other EAM Governance.
The workflow is designed to sit on top of your historian and EAM: it reads tags and CMMS entries, generates suggested WOs with attachments, and records the outcome for auditability. The system surfaces correlations and suggested tasks; it does not replace OEM procedures or site permits. Use the evidence to justify decisions and follow established operational controls for trip/derate actions.
RCM Decision Logic (SAE JA1011 Grounded)
Standard RCM mapping — Functions → Functional Failures → Failure Modes → Effects — applied to inlet filtration. Start a free trial to run the mapping on your unit.
Function
Prevent FOD ingress and provide early warning.
Functional Failures
Loss of filtration efficiency, unintended bypass, failure of pulse-jet cleaning.
Failure Modes
Torn or displaced media, gasket/access-panel failures, pulse control malfunctions, discrete ingestion events.
Effects
Progressive blade nicking, sudden FOD impact, efficiency loss, forced derate or trip.
JA1011 Hidden-Function Principle
If the failure is not readily detected during normal operations and can lead to significant adverse effect (operational, safety, environmental), a task that exercises the hidden function is justified.
Discriminating Tests First
Prefer tasks that discriminate among look-alike causes — those that separate sensor faults from real filtration breaches — before high-invasion corrective actions.
Selecting Verification Tasks
Three rules for choosing what to do first, keeping intrusion low and audit trails intact. Book a review to walk task selection on your last inlet event.
Low-Intrusion First
Prioritize low-intrusion, high-discriminative tasks first — e.g., confirm pulse actuator feedback and compare differential pressures across filter stages.
Escalate on Evidence
Escalate to borescope or media replacement only if diagnostic checks indicate increased risk or confirm infiltration.
Record Evidentiary Signals
Ensure tasks are recorded with their evidentiary signals so post-work analysis is auditable.
Operational Guardrails
System surfaces correlations and suggested tasks; it does not replace OEM procedures or site permits. Use evidence to justify decisions and follow established controls for trip/derate.
Closed Loop: Detect → Diagnose → Prioritize → Dispatch
The four-step loop that turns a rising dP trend into an auditable, dispatched work order with the outcome recorded back into the historian/CMMS for future correlations. Start a free trial to close the loop on your next inlet event.
Step 1
Detect
Continuous monitoring of differential pressure, pulse counts and vibration channels generates alerts when patterns deviate from historical behavior.
Step 2
Diagnose
Cross-correlate the detected signals with 5–15 years of historian events and CMMS records to identify likely failure modes — timeline stitching and correlation, not opaque scoring.
Step 3
Prioritize
Use RCM consequence categories (safety/environmental, operational, maintenance/process) and detectability to set a conditional priority. Hidden failures with high consequence and poor detectability get elevated priority.
Step 4
Dispatch
Produce a contextual, evidence-backed suggested work order for your EAM (Maximo/SAP/Infor), attach the relevant timeline and tag excerpts, and dispatch. Record the outcome and outcome evidence back into the historian/CMMS so future correlations reference the actual results.
Disclaimer
The honesty note that governs every illustration on this page. Book a technical review to discuss OEM guidance for your unit.
"
All timeline descriptions and pane examples in this article are illustrative and qualitative. No OEM intervals, setpoints or financial ROI figures are supplied here. Final operational and maintenance actions must follow OEM guidance, site procedures and permit controls.
Oxmaint AI Reliability Desk
Practical FAQs
Can all inlet bypasses be detected from dP and vibration alone?
No. Some edge leaks or small bypass paths are only found through hands-on hidden-function checks. Correlated signals reduce unnecessary interventions but cannot eliminate the need for occasional physical verification.
Will this create nuisance work orders?
The approach prioritizes tasks by consequence and detectability and flags missing instrumentation. The goal is fewer, more defensible interventions — not more noise.
Are hidden-function tests the same as standard PMs?
Not always. Hidden-function checks are targeted to verify a function that would otherwise be invisible under normal monitoring (for example, a pulse-cleaner actuation under simulated load or a smoke bypass test), and are selected based on RCM logic.
Bring Your Tags. See the Panes on Your Records.
If you want your own SGT-400 inlet-filter history and CMMS stitched into these panes for an operational review, book a technical session or start a trial and bring the relevant tags (for example: INLET_DP, PULSE_CYCLE_CNT, VIB_AXIAL_1X). We'll show the timeline, signal correlations and a suggested WO draft tied to your actual records. Start a free trial to bring your own data.