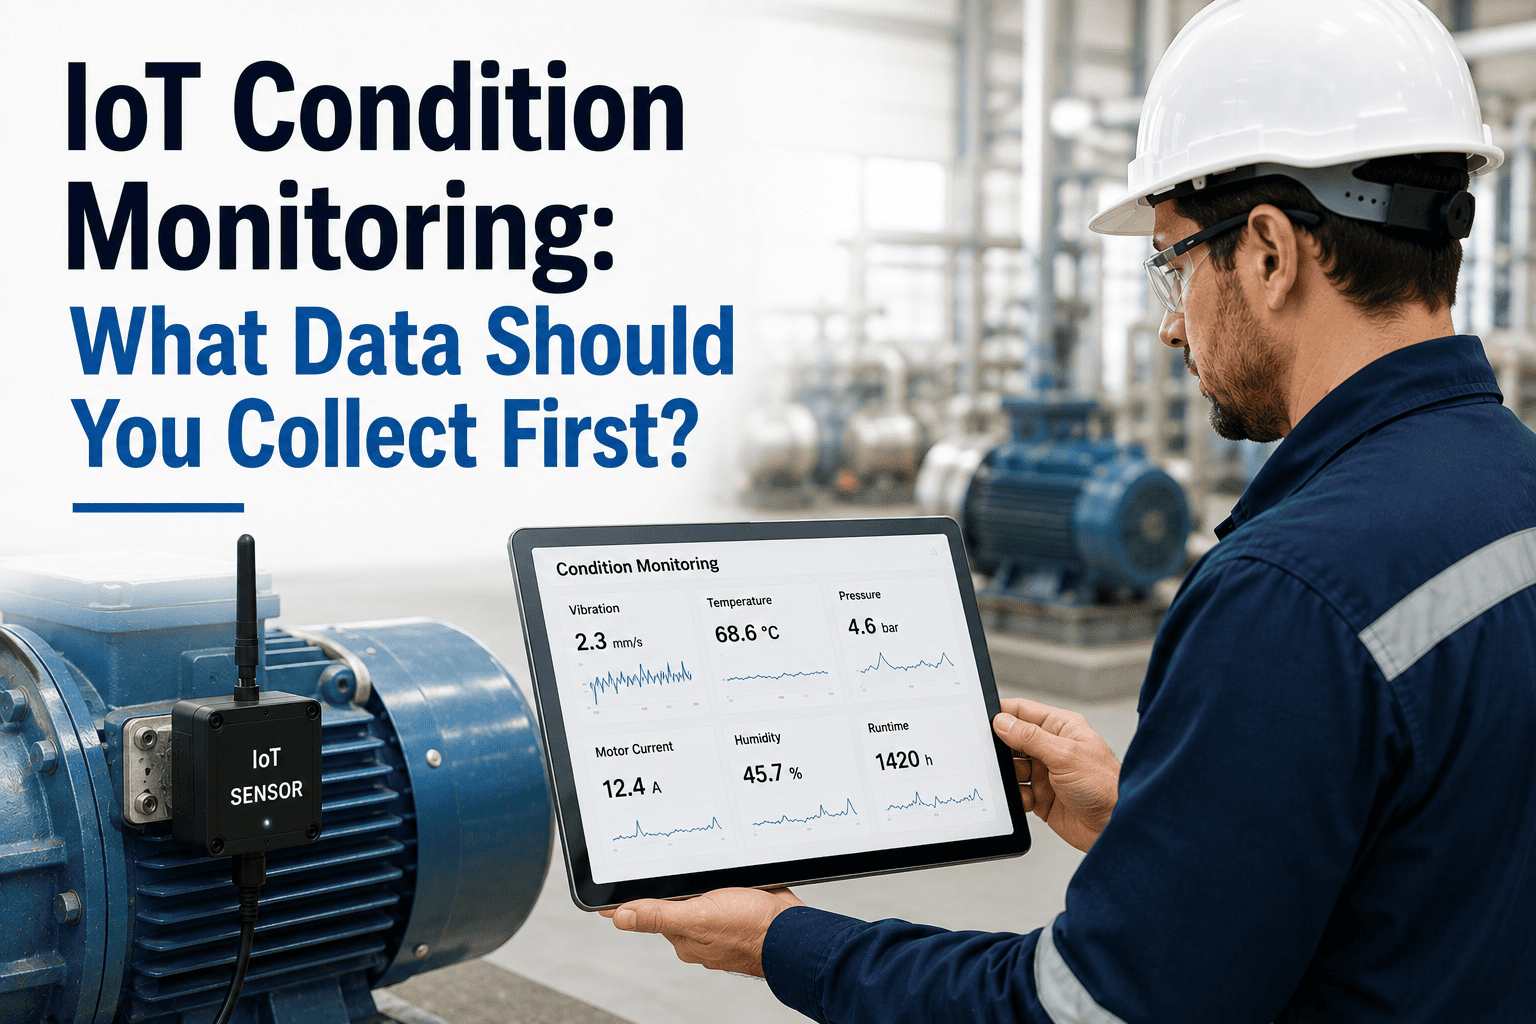
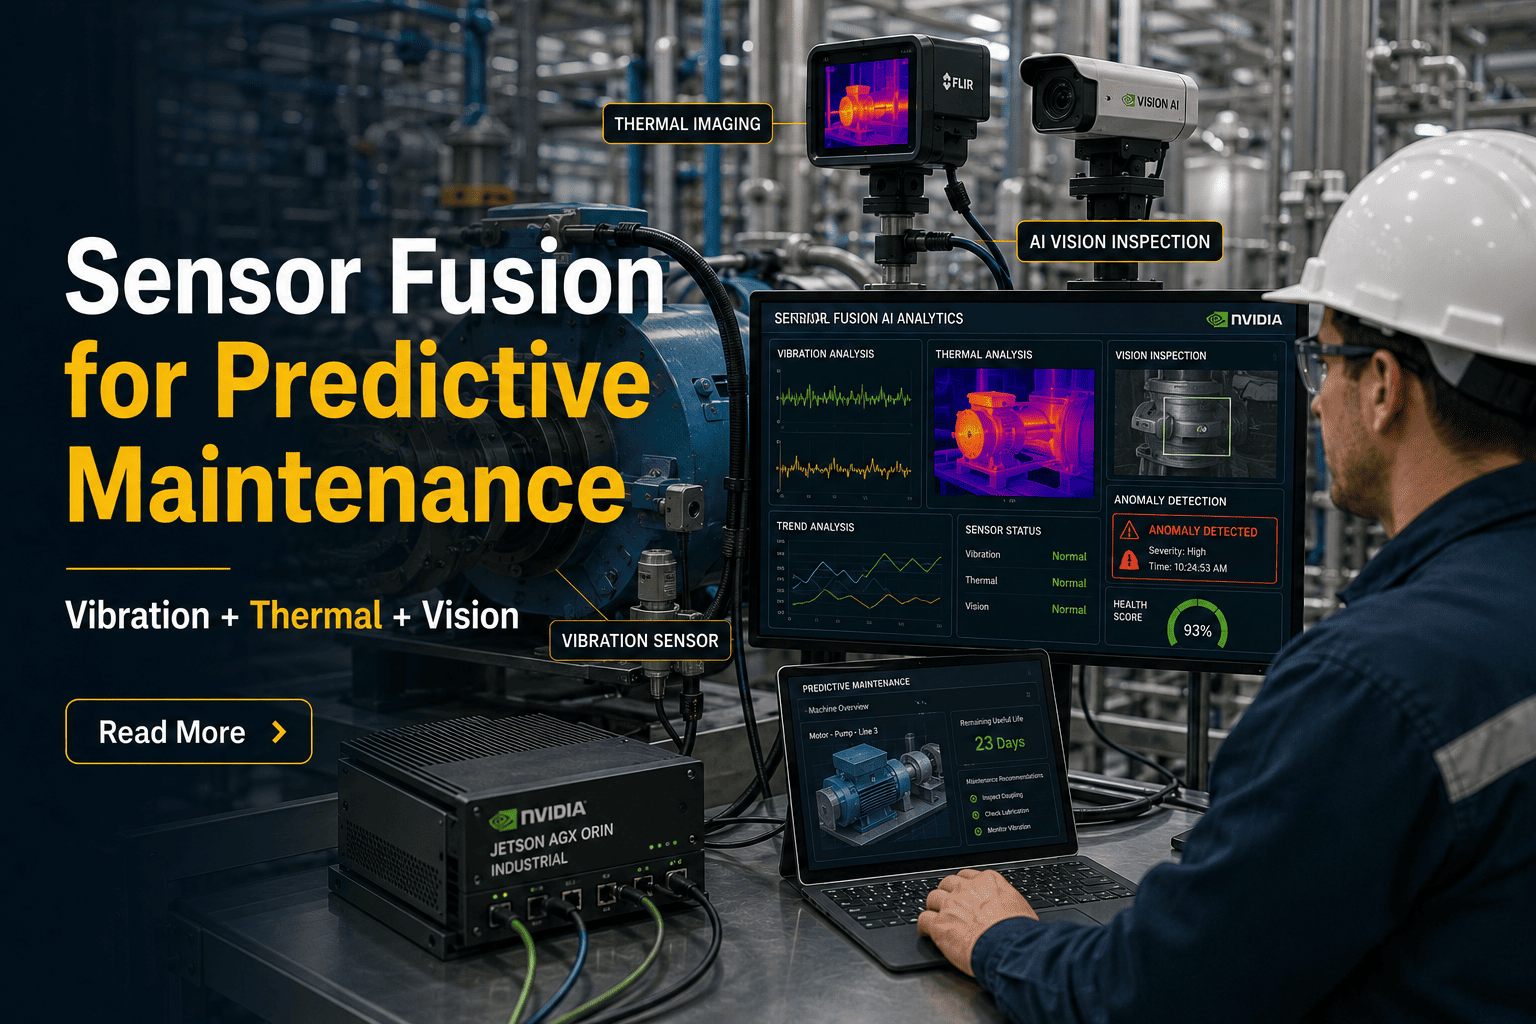
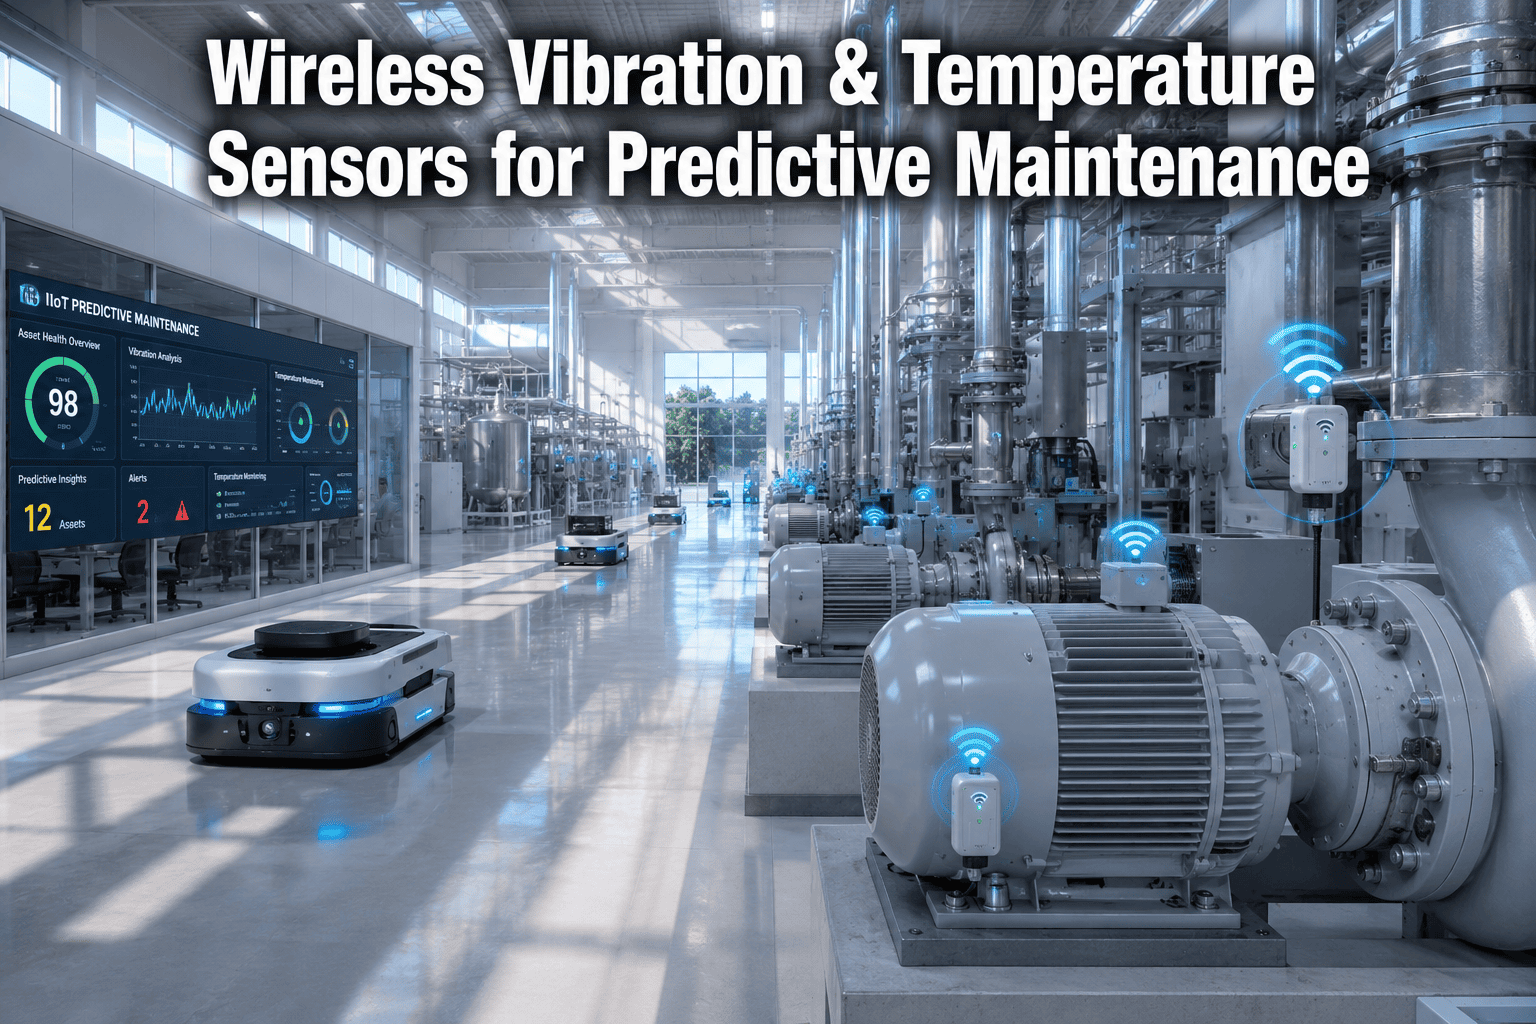
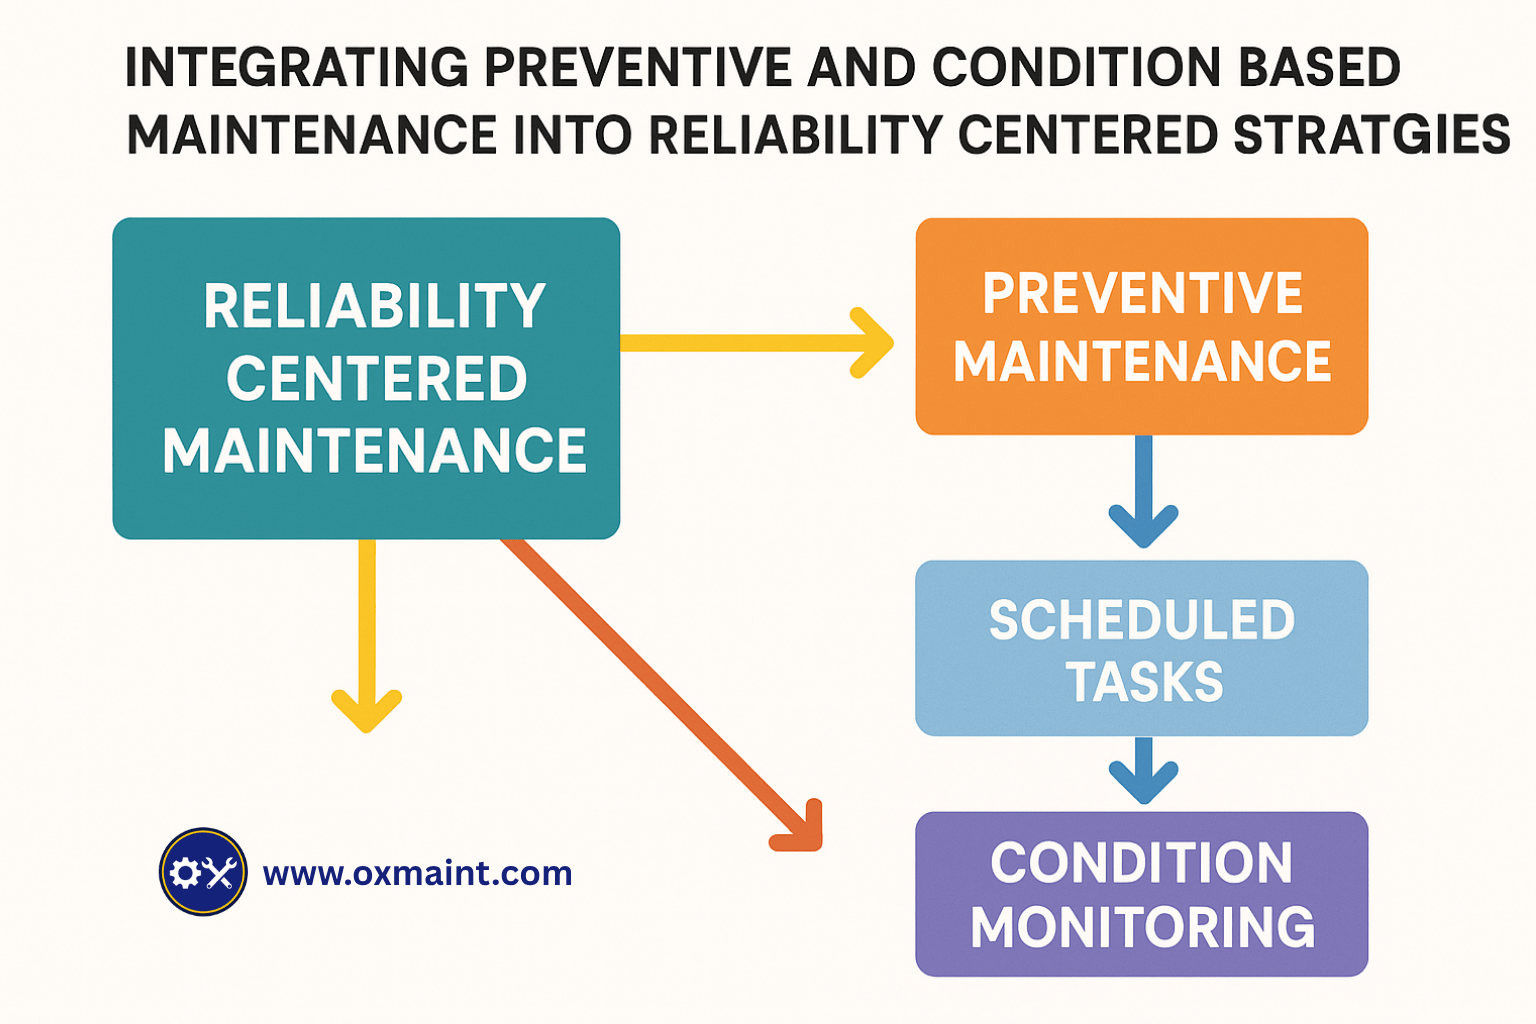
Gas turbines health monitoring through vibration, temperature, and oil analysis is the backbone of modern maintenance and reliability programs for power generation and oil-and-gas operators. Condition monitoring for gas turbines shifts teams from reactive firefighting to predictive control by catching early warning signals like compressor fouling and hot gas path (HGP) degradation before they escalate into forced outages that cost $50K–$500K per day. By integrating gas turbines vibration monitoring, gas turbines temperature monitoring, and routine oil analysis into a single CMMS workflow, plants routinely cut unplanned downtime 30–50% and extend mean time between overhauls by thousands of operating hours. This guide breaks down the most effective gas turbines monitoring techniques, sensor placement strategies, and fault detection methods—and shows how OxMaint turns that sensor data into automated work orders and reliability decisions. Ready to modernize your maintenance program? Start Free Trial with OxMaint today.
Gas Turbines Health Monitoring
Are you catching turbine faults 30 days before failure — or 30 minutes after?
Over 70% of gas turbine unplanned outages are traceable to detectable early warning signals in vibration, temperature, and oil data. The difference between a $4K bearing swap and a $400K rotor rebuild is how fast your team acts on that data.
Three Pillars of Fault Detection
Gas turbines monitoring techniques that catch failures early
Effective gas turbines condition monitoring rests on three complementary data streams. No single technique detects every failure mode — reliability programs that deploy all three typically identify 85–95% of incipient faults before secondary damage occurs.
Vibration Monitoring
Detects: bearing wear, rotor unbalance, blade rub, misalignment
Accelerometers and proximity probes on gas turbines vibration monitoring systems track amplitude, frequency, and phase. A sudden rise in 1× component typically signals rotor unbalance, while 2× indicates misalignment. High-frequency envelope readings catch bearing defect frequencies 4–8 weeks before spalling becomes audible.
Temperature Monitoring
Detects: HGP degradation, combustion hot spots, fouling, cooling-air failure
Exhaust gas temperature (EGT) thermocouple arrays and thermal imaging map combustion uniformity. A 15°C spread between thermocouples often precedes combustor can or fuel nozzle issues. Trending exhaust temperature against compressor discharge temperature reveals compressor fouling and turbine efficiency loss early.
Oil & Debris Analysis
Detects: gear wear, bearing fatigue, lubricant degradation, contamination
Spectrometric and ferrographic oil analysis identify wear-metal particles (Fe, Cu, Pb, Sn) in the lubrication system. Online magnetic chip detectors and particle counters provide real-time debris alerts. Rising iron content above 10–15 ppm in a 500-hour sample window frequently precedes journal-bearing failure.
Worked Example
From early warning signal to avoided outage: a real-world scenario
Baseline anomaly detected
A Frame 7FA gas turbine's gas turbines online monitoring system flags a 0.18 in/s rise in overall vibration on the compressor drive-end bearing — a 35% jump over the 90-day rolling baseline. Simultaneously, envelope-detected high-frequency energy at a bearing outer-race defect frequency confirms an incipient spall.
Automated work order generated
OxMaint receives the condition-monitoring alert via API and auto-generates a corrective work order tagged to the specific asset hierarchy node. The reliability engineer reviews severity, schedules a borescope inspection during the next planned slow-down, and orders the replacement bearing kit — all inside one platform.
Controlled intervention executed
During a scheduled 3-day outage, technicians swap the degraded bearing — a $4,200 parts-and-labor fix. Had the fault progressed to secondary rotor damage, the repair would have required a $340K rotor pull and 21 days of forced downtime. Net avoided cost: approximately $336K plus $2.1M in lost generation revenue.
Post-repair trend confirmed
Vibration returns to 0.07 in/s baseline. OxMaint logs the failure mode, repair cost, and MTBF data against the asset record, automatically updating the next PM interval and feeding predictive analytics so the reliability team can refine alarm thresholds across the fleet.
Degradation Patterns
Compressor fouling vs HGP degradation: what your data reveals
Gas turbines lose 2–5% in thermal efficiency within the first 1,000 operating hours due to compressor fouling, while hot gas path degradation accumulates more slowly but costs 10× more to correct. Distinguishing the two through condition data determines whether you schedule an offline wash or plan a 4-week major inspection.
| Indicator | Compressor Fouling | HGP Degradation | Typical Action |
|---|---|---|---|
| Compressor discharge pressure | Drops 3–8% | Slight gradual decline | Online or offline compressor wash |
| Exhaust gas temperature (EGT) | Rises 5–15°C above baseline | Rises 10–25°C; spread widens | Fouling: wash; HGP: borescope + hardware inspection |
| Heat rate deviation | +1 to +3% | +2 to +5% | Recoverable via wash (fouling); non-recoverable until HGPI (HGP) |
| Vibration signature | Usually unchanged | May show blade-pass or rub harmonics | Vibration route analysis; confirm with borescope |
| Recovery after maintenance | 90–100% recoverable after wash | Only recoverable at combustion inspection / HGPI | Schedule wash cycle; plan HGPI per equivalent operating hours |
A 200-MW combined-cycle plant losing 3% output to undetected fouling forgoes roughly $1,800 per operating day in marginal revenue — making frequent, data-triggered wash cycles one of the highest-ROI preventive actions available.
Sensor Strategy
Gas turbines sensor placement for maximum fault coverage
Optimal gas turbines sensor placement ensures that every high-risk failure mode has at least one dedicated detection point. The matrix below maps standard sensor types to their mounting locations and the specific faults they capture — a reference reliability engineers use when auditing monitoring coverage on a unit.
Bearing housing vibration
Captures unbalance, misalignment, looseness, and bearing defect frequencies. Mount radially at 45° on both ends for full coverage.
Shaft relative displacement
Measures shaft orbit, eccentricity, and thrust position — critical for detecting rub, oil whirl, and thrust-bearing overload on large rotors.
EGT distribution mapping
Multiple thermocouples around the exhaust annulus detect combustion-can imbalance, nozzle bowing, and burner fouling via temperature-spread alarms.
Ferrous debris in oil
Online detectors count and size magnetic particles, giving instant alerts when bearing or gear spalling accelerates — complementing lab oil samples.
Compressor pressure ratio
Trending inlet-to-discharge pressure ratio at corrected flow reveals compressor fouling and stage surge margin — a direct indicator of wash timing.
Phase reference & speed
Provides the timing reference for order-tracking and phase analysis — essential for balancing, rub detection, and transient start-up vibration analysis.
Turn Sensor Data Into Action
See OxMaint close the loop from alarm to work order — book a 30-min demo
Discover how maintenance teams use OxMaint to auto-trigger work orders from vibration and temperature thresholds, track asset health, and eliminate spreadsheet-based condition monitoring for good.
How OxMaint Helps
From condition data to controlled reliability with OxMaint
OxMaint's AI-powered CMMS and EAM platform bridges the gap between gas turbines online monitoring sensors and the maintenance actions that prevent failure. Instead of alarms sitting in a historian waiting for someone to notice, OxMaint automates the full reliability workflow — from threshold breach to verified repair.
Automated alarm-to-work-order dispatch
Connect vibration, temperature, and oil-debris thresholds directly to OxMaint work-order workflows. When a gas turbines early warning signal breaches a configured limit, a corrective work order is auto-created, assigned to the right technician, and prioritized — cutting response time from hours to minutes.
Predictive analytics on asset health trends
OxMaint's AI engine trends vibration amplitude, EGT spread, and wear-metal ppm across every gas turbine in your asset hierarchy, predicting remaining useful life and surfacing the units most likely to fail in the next 30, 60, or 90 days — so you plan interventions before they become forced outages.
Full asset hierarchy & PM automation
Model every gas turbine from skid to sub-component. OxMaint auto-schedules preventive maintenance — compressor washes, borescope inspections, filter changes, oil sampling — based on equivalent operating hours, calendar intervals, or condition triggers, ensuring no PM slips through the cracks.
Reliability analytics & audit-ready reporting
Every work order, sensor alert, and repair cost is logged against the asset record automatically. OxMaint dashboards surface MTBF, MTTR, availability, and OEE in real time, while one-click audit reports keep you compliant with ISO 55000, OEM warranty, and regulatory requirements without manual data compilation.
FAQ
Gas turbines health monitoring: frequently asked questions
What is condition monitoring for gas turbines?
Condition monitoring for gas turbines is the continuous or periodic collection and analysis of vibration, temperature, oil, and performance data to detect incipient faults before they cause failure. It uses gas turbines monitoring sensors — accelerometers, thermocouples, proximity probes, and oil debris detectors — to trend asset health and trigger maintenance only when the data indicates degradation, rather than on a fixed time schedule alone.
How does gas turbines vibration monitoring detect bearing faults?
Gas turbines vibration monitoring detects bearing faults by analyzing characteristic defect frequencies in the vibration spectrum. Outer-race, inner-race, and rolling-element defects each produce distinct frequency signatures calculable from bearing geometry and shaft speed. Envelope detection and high-frequency resonance techniques amplify these early-stage signals, often revealing spalling 4–8 weeks before vibration amplitude reaches alarm thresholds. OxMaint can auto-create a work order the moment these signatures cross a configurable limit — Start Free Trial to see it on your assets.
What are the most important gas turbines early warning signals?
The highest-value early warning signals are rising overall vibration amplitude and the emergence of bearing defect frequencies, a widening EGT spread between thermocouples (indicating combustion imbalance or HGP degradation), increasing wear-metal concentration in oil samples, and a gradual drop in compressor discharge pressure relative to inlet conditions (indicating fouling). Trending these parameters against a rolling baseline — rather than relying on absolute alarm limits — catches the subtle shifts that precede 70–90% of gas turbine failures.
How often should oil analysis be performed on a gas turbine?
Most OEMs and reliability standards recommend laboratory oil analysis every 500–1,000 operating hours or monthly, whichever comes first, for frame-type gas turbines in continuous duty. Aeroderivative units in peaking service may follow a different interval based on starts and stops. Online magnetic chip detectors and particle counters supplement lab samples with real-time debris alerts between sampling windows. OxMaint auto-schedules oil sampling PMs and logs lab results against the asset — book a demo at Calendly to automate your sampling program.
Can a CMMS improve gas turbines reliability and reduce downtime?
Yes. A modern CMMS like OxMaint improves gas turbines reliability by automating PM scheduling, linking condition-monitoring alarms directly to work-order creation, and centralizing asset history so failure patterns are visible across the fleet. Plants that replace spreadsheets and reactive processes with a CMMS typically cut unplanned downtime 30–50%, raise PM compliance above 95%, and reduce maintenance labor costs 15–25% through better planning and fewer emergency callouts.
Start Your Reliability Transformation
Stop firefighting gas turbine failures — start predicting them
Join the maintenance and reliability teams using OxMaint to turn vibration, temperature, and oil data into automated work orders, higher availability, and lower lifecycle cost. See the platform on your assets in a 30-minute personalized demo.
Free 14-day trial · No credit card