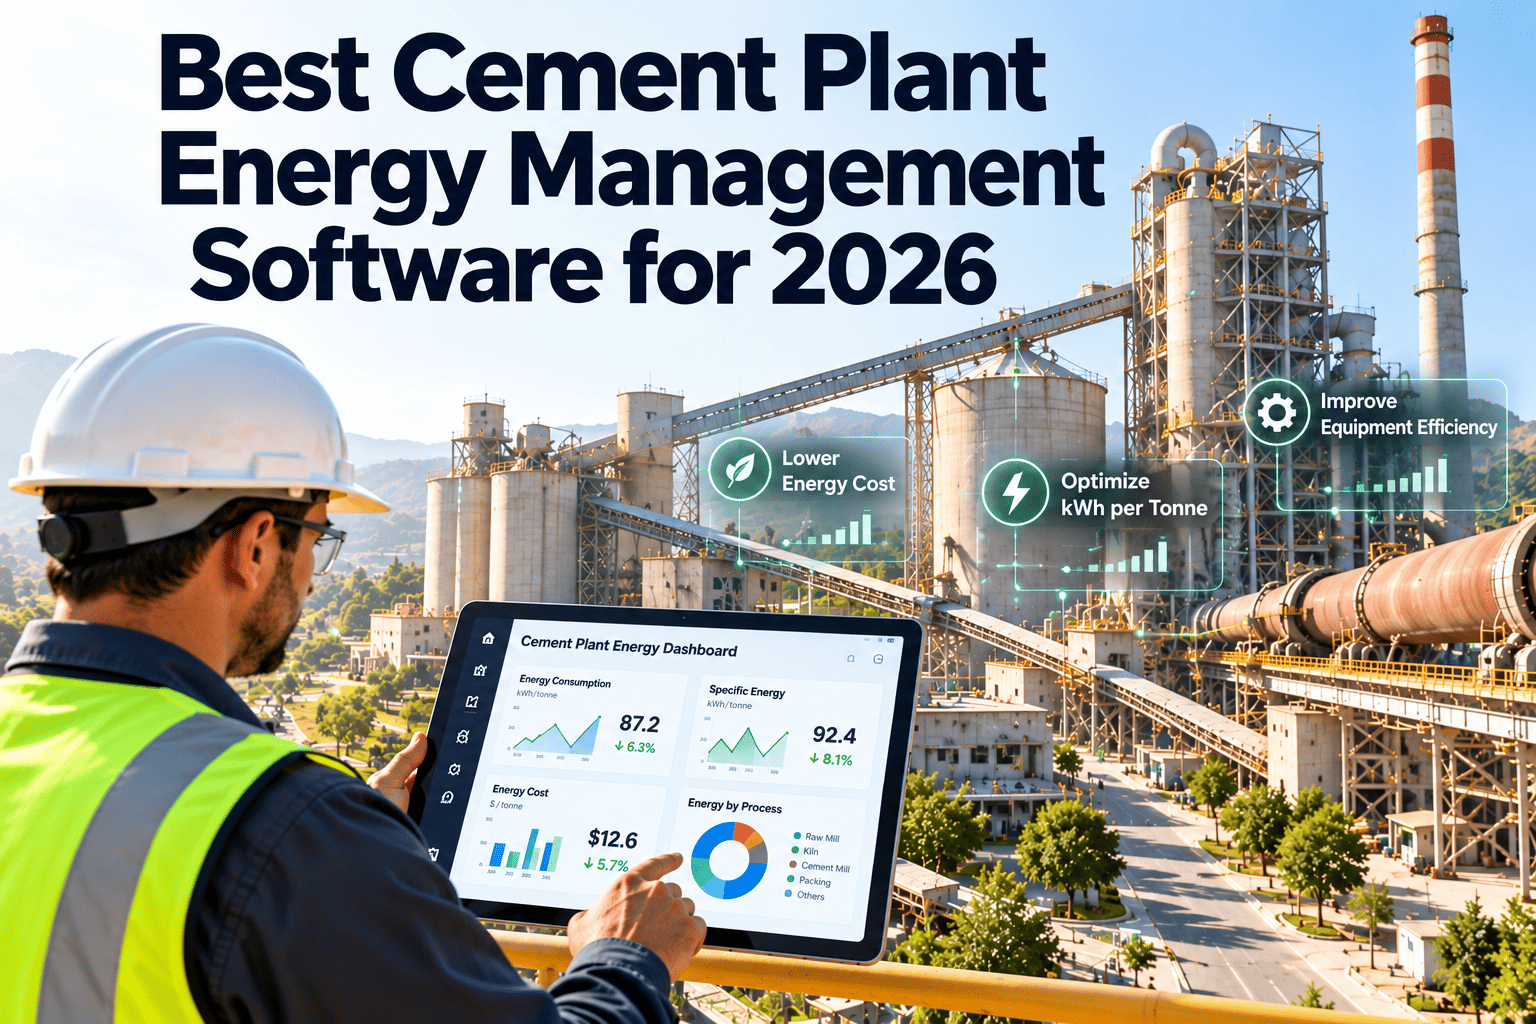
Choosing energy management software for a cement plant is harder than it looks, because the energy story is spread across kilns, mills, fans, compressors and utilities, with data in meters, historians, SCADA and spreadsheets. In 2026 the useful question is less about which dashboard looks best and more about which tool turns energy data into action on the plant floor. This guide gives you a vendor-neutral way to compare options, with attention to integrations, analytics and the maintenance link. If you want to see how a maintenance platform fits into that picture, you can open an Oxmaint account and explore the workflow.
Best Cement Plant Energy Management Software for 2026
A practical comparison framework for cement teams: what to demand from energy software, how categories differ, and how maintenance workflows turn insight into savings.
Layer 4Action: work orders, inspections, preventive tasks
Layer 3Analytics: normalised kWh per tonne, anomalies, benchmarks
Layer 2Integration: historian, SCADA, meters, ERP, quality data
Layer 1Measurement: sub-meters, drives, process sensors
What cement plants need from energy software in 2026
Cement is energy and emissions intensive, and thermal and electrical efficiency affect cost, product quality and carbon reporting. Software has to reflect how a plant actually runs.
A
Production-normalised metrics
Energy only means something per tonne of clinker or cement, by product type and operating mode.
B
Process-aware context
Fuel mix, alternative fuels, kiln stops, mill grades and ambient conditions change the baseline.
C
Equipment context
Energy drift needs to be explained by condition, so asset and maintenance data must be reachable.
D
Reporting and standards support
Support for energy management systems such as ISO 50001 and internal carbon or cost reporting.
Software categories compared
No single product covers everything well. Most plants combine two or three categories, so compare what each is genuinely strong at.
| Category | Strength | Typical limitation | Best fit |
|---|---|---|---|
| Energy monitoring and analytics platforms | Metering, dashboards, normalisation, benchmarking | Weaker at assigning and tracking maintenance actions | Plants with strong sub-metering and an energy team |
| Process optimisation and advanced control | Improves kiln and mill operation in real time | Needs good instrumentation and tuning effort | Plants chasing process stability gains |
| Historian and plant data platforms | Reliable time-series storage and trending | Analytics and workflows depend on add-ons | Plants building their own reporting |
| Maintenance management software (CMMS) | Inspections, work orders, assets, preventive tasks, spares | Not a metering or process control tool | Turning energy findings into repairs and routines |
| Spreadsheets and custom reports | Flexible and cheap to start | Manual, error-prone and hard to scale | Early-stage tracking only |
Evaluation scorecard
Score each shortlisted product from 1 to 5 against these criteria, weighted by your plant priorities. Ask for a demonstration with your own data.
CriterionQuestion to ask
Data integrationWhich historians, SCADA, meters and ERP systems connect, and how long does it take?
NormalisationCan it normalise by product, load and operating mode?
Anomaly detectionHow are deviations flagged, and who is notified?
Maintenance linkCan a finding become a work order or inspection task?
Usability on siteDo operators and technicians use it on mobile devices?
ReportingDoes it support management and compliance reporting needs?
Security and deploymentHow are access, data ownership and network security handled?
Total cost and supportWhat are licences, integration work, training and ongoing support?
See the action layer of your energy programme
Energy insight pays off when someone is assigned to fix the cause. Explore how inspections and work orders close that loop.
Capabilities worth testing in a pilot
Energy and process side
- Specific energy by kiln, raw mill, cement mill and fans
- Thermal energy per tonne of clinker with fuel mix
- Peak demand and tariff period tracking
- Compressed air and utility monitoring
- Alerts on deviation from a normalised baseline
Maintenance side
- Inspection rounds that capture energy-related findings
- Work orders linked to the asset causing the loss
- Preventive tasks for filters, leaks, lubrication and alignment
- Spare parts planning for wear components
- History to verify results after repairs
Common energy losses that maintenance can address
Where Oxmaint fits
Oxmaint is maintenance management software, not a metering or process control platform. Its role is to make sure energy findings lead to assigned, tracked and verified maintenance work.
Detect
Your energy platform or historian shows a drift in normalised consumption.
Inspect
An inspection task is raised and technicians record findings on mobile.
Correct
A work order is assigned with parts, priority and planned window.
Prevent
A preventive schedule stops the same loss from returning.
Verify
Asset history and reports show whether energy improved after the repair.
Mistakes to avoid when selecting software
Buying dashboards without actions
Define who acts on each alert and in which system.
Ignoring data quality
Calibrate meters and map tags before blaming the tool.
Skipping the operators
Involve shift crews early so the tool matches real routines.
Choosing on features alone
Weigh integration effort, support and adoption cost.
No baseline
Record pre-project consumption so savings can be proven.
Thermal and electrical energy: two different problems
Cement energy splits into fuel burned in the kiln and electricity consumed across the plant. Software should handle both, because the levers and data sources differ.
Thermal energy
- Fuel consumption per tonne of clinker
- Fuel mix including alternative fuels and biomass
- Preheater and cooler heat recovery performance
- Kiln stability, stops and restart losses
- Insulation, refractory and false air effects
Electrical energy
- Raw mill, cement mill and coal mill specific power
- Kiln, ID fan and cooler fan consumption
- Compressed air and utility systems
- Crushers, conveyors, packing and dispatch
- Peak demand, tariffs and power factor
Plants exporting to markets with carbon border rules, such as the EU Carbon Border Adjustment Mechanism that covers cement, also need credible emissions and energy records. Confirm current requirements with your compliance team.
Integration checklist: where the data comes from
SourceWhat it provides and what to verify
Electricity metersConsumption by feeder or unit. Verify metering coverage, calibration and time stamps.
Historian or SCADAProcess variables such as feed rate, temperatures and fuel flow. Verify tag naming and data gaps.
Laboratory and quality systemsFineness, clinker and cement quality. Verify how sample results map to production periods.
ERP and production reportsTonnage, grades and costs. Verify consistency with plant measurements.
Maintenance systemAssets, inspections, work orders and downtime. Verify asset naming matches the energy structure.
Fuel and utility invoicesPurchased energy cost and quantity. Verify reconciliation with site meters.
Testing analytics and AI claims in vendor demos
Many 2026 products advertise machine learning and automated insights. Ask vendors to demonstrate, with your own data, rather than describe.
Claim: automatic anomaly detection
Test: replay a past incident and see whether and when it would have been flagged.
Claim: optimised setpoints
Test: ask who approves changes, how they are limited and how results are verified.
Claim: easy integration
Test: request the list of connectors used at comparable cement sites and effort required.
Claim: proven savings
Test: ask how savings were measured, against which baseline and over what period.
Claim: explains root cause
Test: check whether explanations link to equipment condition or only to correlations.
A phased implementation roadmap
Phase 1
Define energy boundaries, baselines and normalisation rules with process and finance.
Phase 2
Close metering and data gaps on the largest consumers first.
Phase 3
Launch dashboards and alerts for a few agreed indicators.
Phase 4
Connect findings to inspections, work orders and preventive tasks.
Phase 5
Review verified savings and extend to further areas.
Building the business case
| Benefit area | Where it appears | How to measure it |
|---|---|---|
| Lower specific energy | Mills, fans, kiln fuel use | Normalised consumption against a documented baseline |
| Avoided breakdowns | Kiln line and grinding circuits | Unplanned downtime hours before and after |
| Reduced peak demand charges | Electricity tariff | Billed demand compared with the prior year |
| Reporting effort | Energy and sustainability teams | Hours spent preparing reports |
| Better maintenance targeting | Planned and reactive work ratio | Share of work triggered by condition findings |
Be cautious with savings claims in vendor material. Use your own baseline and count only savings you can verify.
Governance that keeps the programme alive
1
Named owners
Each indicator has an owner who answers for it in the review meeting.
2
Regular review
A weekly operational review and a monthly management review with the same indicators.
3
Action tracking
Every alert or finding produces a tracked action with a due date.
4
Baseline control
Baselines change only with documented reasons such as new products or equipment.
Use cases by plant area
| Area | Energy question | Data needed | Maintenance link |
|---|---|---|---|
| Kiln and preheater | Why is fuel use per tonne of clinker rising? | Fuel flow, clinker output, stops, shell and gas temperatures | False air, refractory, cooler and seal inspections |
| Raw mill | Is specific power drifting for the same raw mix? | Mill power, feed, product fineness, fan power | Wear parts, hydraulics, filters and ducts |
| Cement mill | Does energy match the grade being ground? | Mill and separator power, grade, fineness | Liners, media, separator and ventilation |
| Fans and filters | Are dampers throttled or filters restricting flow? | Fan power, pressure drop, damper position | Filter media, impeller, leaks and actuators |
| Compressed air | How much air is lost to leaks? | Compressor power, pressure, runtime | Leak surveys, dryers, filters and valves |
| Packing and dispatch | Which loads run when idle? | Feeder, conveyor and dust collector runtime | Worn spouts, conveyor alignment and dust systems |
Security, data ownership and support questions
Energy platforms touch operational data, so involve IT and operations security teams early.
1
Where does the data live?
Ask about hosting location, backups, retention and what happens to your data if you leave.
2
How is plant connectivity secured?
Clarify one-way data flows, network segmentation and how remote access is controlled.
3
Who gets access?
Check role-based permissions, audit trails and single sign-on support.
4
What does support include?
Confirm response times, training, onboarding help and cement industry experience.
Pilot success criteria worth agreeing in advance
Technical criteria
- Data from the chosen units flows reliably for the whole pilot
- Normalised energy matches figures your engineers trust
- Alerts fire on known past events and avoid constant false alarms
- Reports can be produced without manual rework
Operational criteria
- Operators and planners use the tool during normal shifts
- At least some findings lead to completed corrective work
- Energy actions have owners and due dates
- Results are reviewed in a regular meeting
If a pilot cannot meet these tests on a small scope, scaling it to the whole plant will not fix the problem.
Total cost of ownership: beyond the licence
| Cost element | What to ask |
|---|---|
| Licences or subscriptions | How is pricing structured: per site, per asset, per user or per data point? |
| Integration work | Who builds and maintains connectors, and what happens when systems change? |
| Metering and instrumentation | Which new meters or sensors are needed to get useful data? |
| Training and change management | How many people need training and how long will adoption take? |
| Internal effort | How many hours per week will engineers spend maintaining the system? |
| Upgrades and support | Are updates and support included, and for how long? |
Maintenance-linked energy losses to look for first
- Compressed air leaks at valves, fittings and hoses that run around the clock
- False air entering through kiln seals, preheater doors and duct joints
- Fouled or blocked filter media raising fan power
- Worn separator parts forcing mills to grind material again
- Misaligned couplings and poorly lubricated gearboxes adding mechanical losses
- Failing insulation and refractory allowing heat loss from kilns and ducts
- Motors and drives running idle or oversized for their duty
These are inspection and repair problems as much as monitoring problems, which is why the energy platform and the maintenance system should share a common asset structure.
Frequently asked questions
What is the best energy management software for a cement plant?
It depends on your data, goals and team. Score options against your own criteria using a pilot.
Is a CMMS a replacement for energy software?
No. It complements it by turning findings into maintenance work. You can book a demo to see how.
What should I normalise energy by?
Tonnes of clinker or cement, product type, load and operating mode, plus fuel mix for thermal energy.
How long should a pilot run?
Long enough to cover several operating conditions, often a few weeks to a few months, on a limited scope.
Where do I start with maintenance?
Begin with the biggest energy users and set up inspections in Oxmaint.
Turn energy insight into maintenance action
Pair your energy analytics with a maintenance workflow that assigns, tracks and verifies every fix.