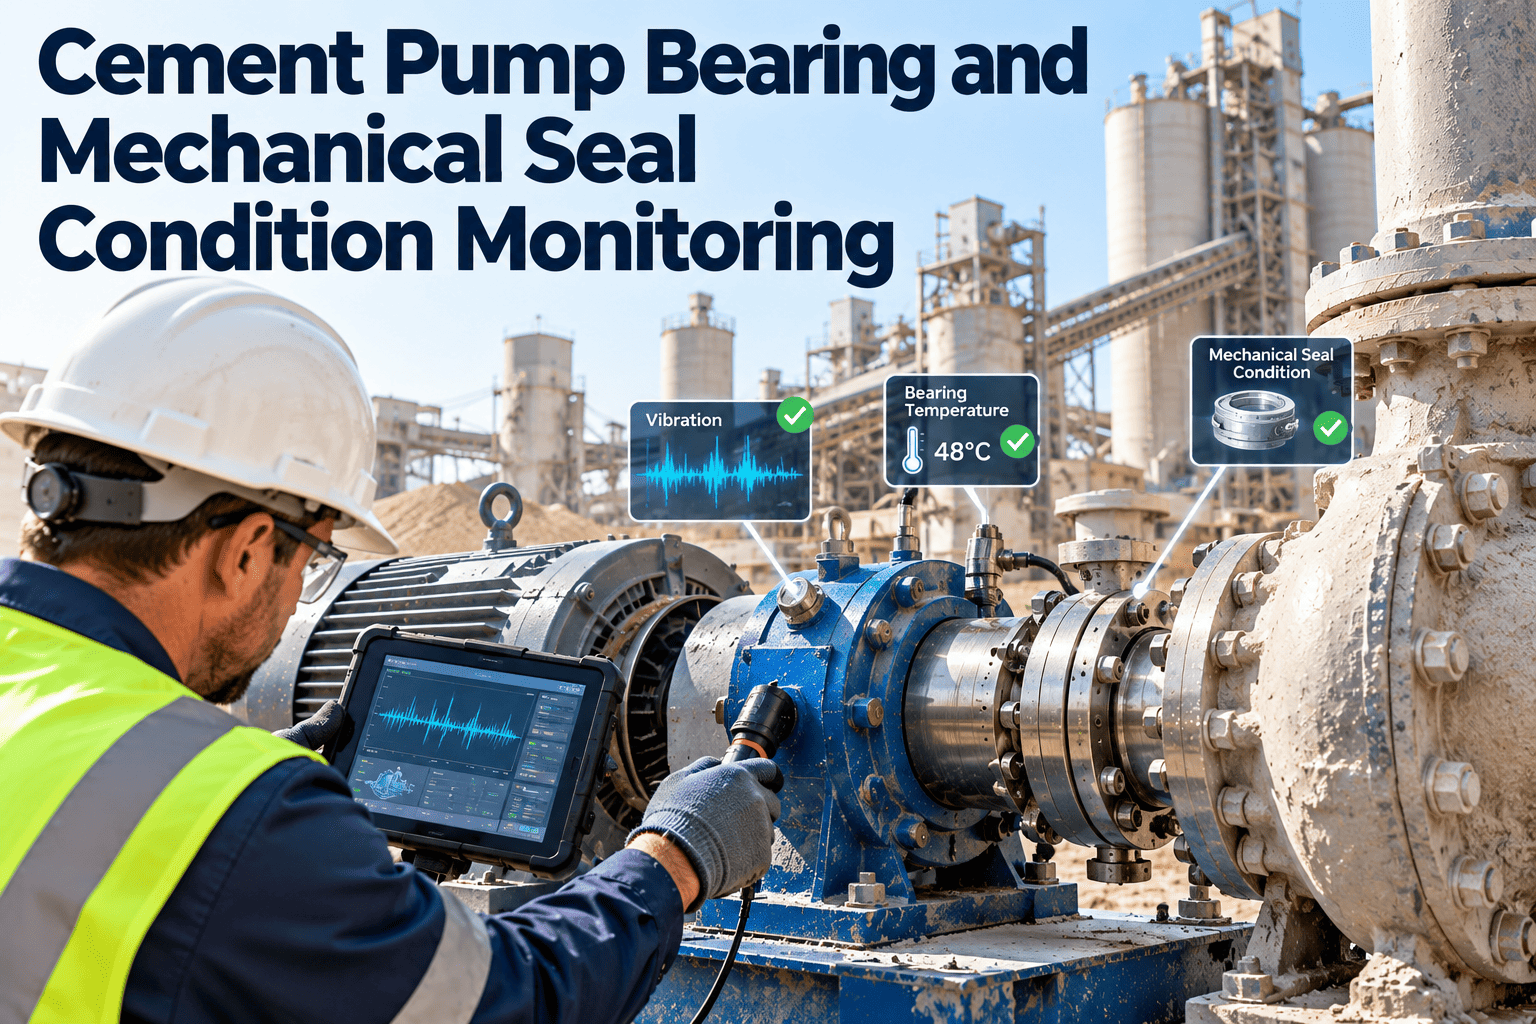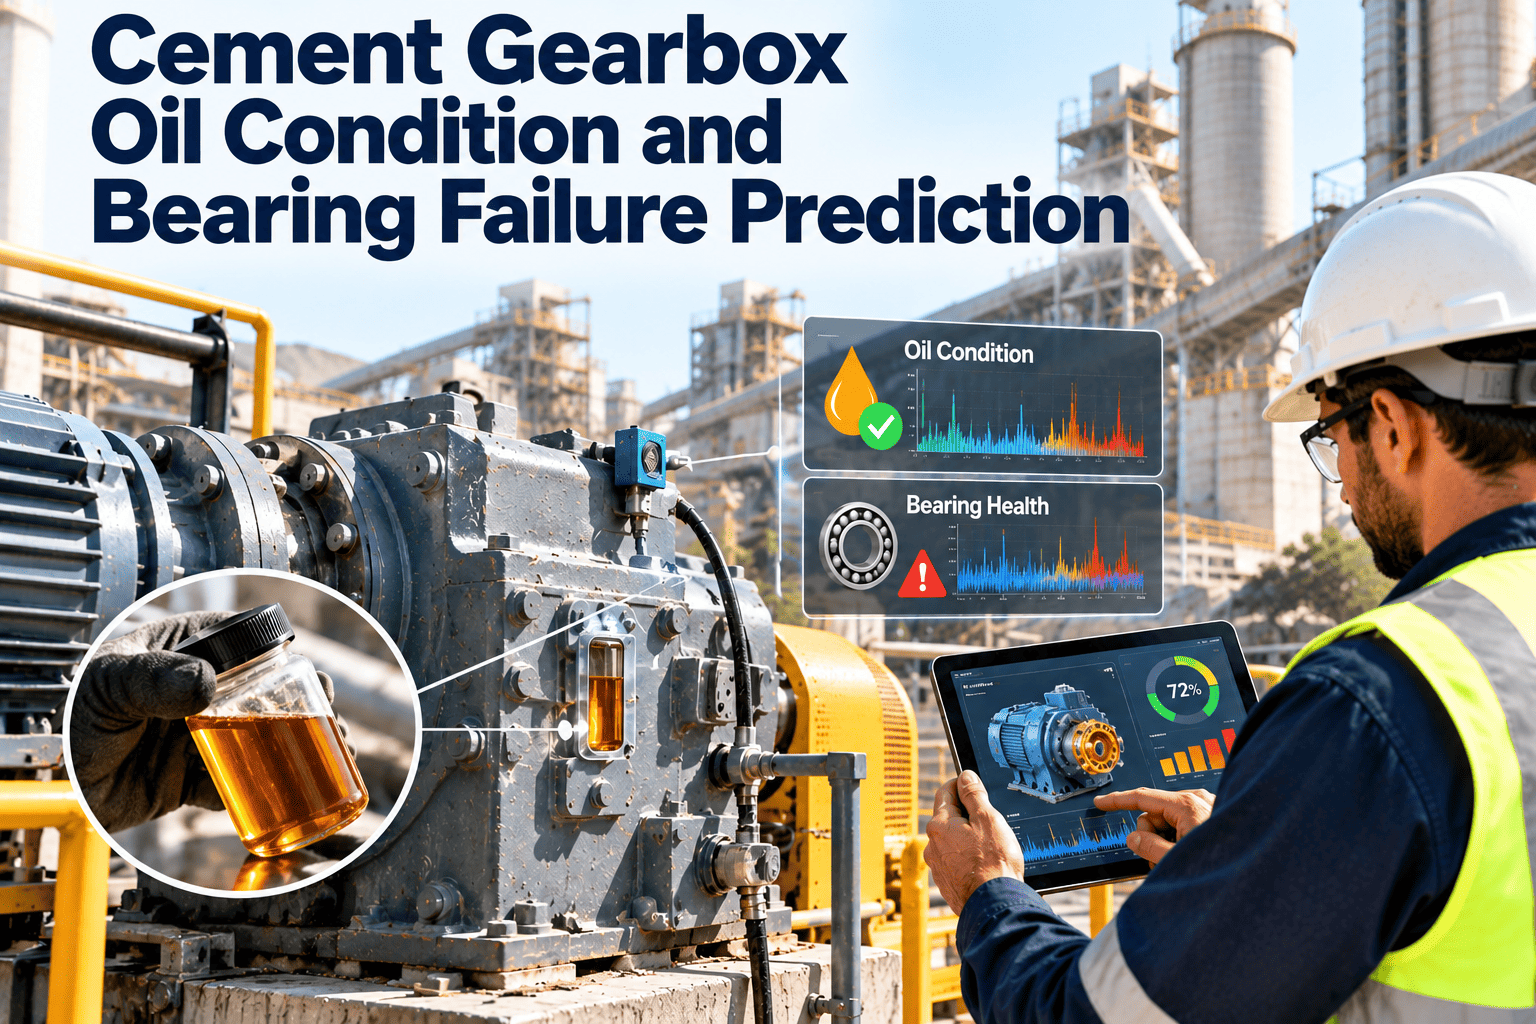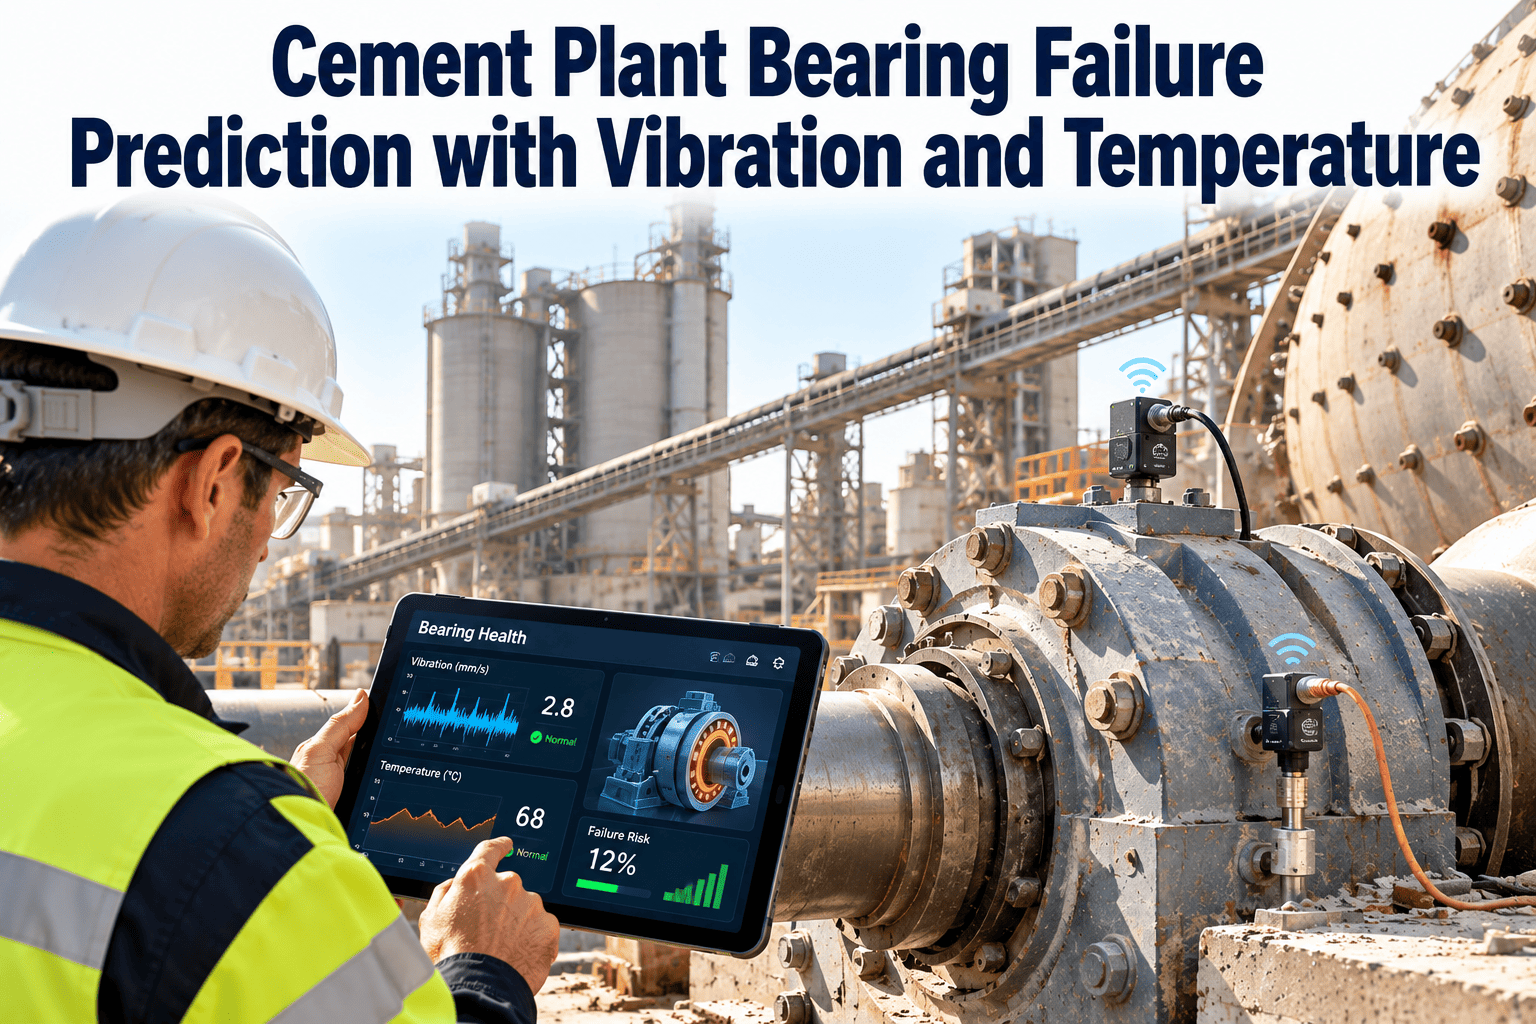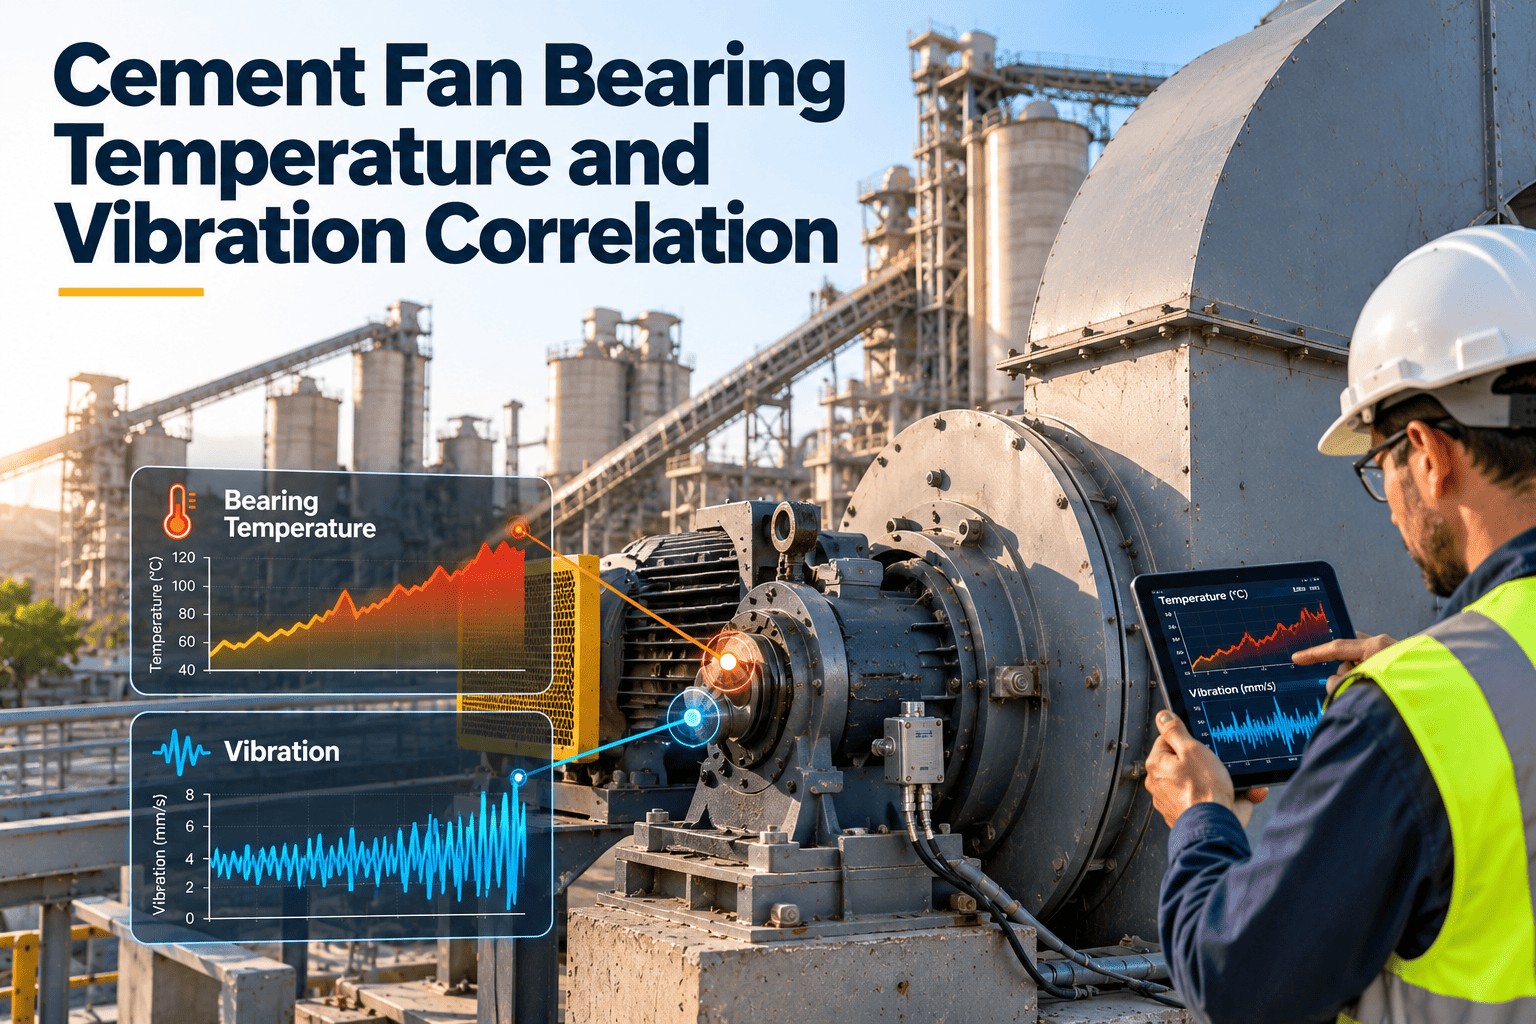
Large fans keep a cement line breathing: the kiln ID fan, preheater fan, cooler fans, raw mill fan and separator fans all run long hours in dusty, hot conditions. Bearing temperature and vibration are the two signals most plants already measure, yet they are often judged separately against fixed alarm limits. Read together, they tell a much clearer story about whether a fan has an imbalance, a lubrication problem, buildup or a bearing that is genuinely failing. This guide explains how to correlate both signals, which patterns to act on, and how Oxmaint preventive maintenance can turn each finding into a tracked task.
Cement Fan Bearing Temperature and Vibration Correlation
One signal can mislead. Two signals read together point to the cause, and to the right action before a fan trips the kiln.
Why Correlation Beats Single Alarms
- Fixed limits are late: a fan can degrade for weeks before it crosses a generic alarm value.
- Load and temperature interact: ambient heat, hot gas and fan speed change both signals without a fault.
- Causes differ: the right fix for imbalance is different from the right fix for a lubrication fault.
- False alarms cost trust: pairing signals filters out spikes from sensors and process changes.
Pattern Guide: What the Combination Suggests
| Pattern | Likely causes to check | First actions |
|---|---|---|
| Vibration rising at running speed, temperature steady | Dust buildup on impeller, blade wear, imbalance, loose mounting | Inspect impeller, review trend after cleaning, check bolts and base |
| Vibration at twice running speed | Misalignment between motor and fan, coupling wear | Alignment check, coupling inspection |
| Bearing temperature rising, vibration steady | Low or excess lubricant, wrong grease, cooling fault, blocked airflow, sensor error | Check lube quantity and type, cooling, sensor reading |
| Both rising with high-frequency content | Bearing surface damage, contamination, lubricant breakdown | Increase monitoring, plan bearing inspection and spares |
| Sudden step change in both | Impeller damage, foreign object, loose component | Assess immediately and consider controlled shutdown |
| Temperature spike after greasing | Over-greasing or mixed lubricants | Review grease procedure and allow settling before judging |
Escalation Ladder for Fan Alerts
Cement Fans and Their Typical Problems
Turn Fan Readings into Assigned Work
Schedule inspection rounds, record readings and raise work orders for each confirmed fan fault.
Measurement Practices That Protect the Data
- Record fan speed, damper position and load with each reading
- Measure at the same points and direction every time
- Establish a baseline after bearing replacement or rebalancing
- Note ambient conditions and recent lubrication
- Check sensor mounting and cable condition
- Comparing readings at very different loads
- Judging a trend straight after greasing
- Relying on one global alarm limit for all fans
- Ignoring sensor drift or frozen values
- Closing alerts without recording the cause
Lubrication and Its Effect on Both Signals
- Too little lubricant raises friction, temperature and often vibration at higher frequencies.
- Too much grease can raise temperature without a mechanical fault.
- Mixing incompatible greases can break down lubrication and shorten bearing life.
- Contamination from dust or moisture damages rolling surfaces and shows up as rising high-frequency vibration.
Fan Maintenance Workflow in Oxmaint
Fan Reliability KPIs
Fan Bearing Basics for Maintenance Teams
Knowing how fan bearings behave makes the data easier to interpret.
Rolling and sleeve bearings
Many smaller fans use rolling element bearings, while large process fans often use sleeve bearings with oil systems. Failure signs and monitoring points differ between them.
Where the heat comes from
Bearing temperature rises from friction, load, lubricant condition and heat conducted from hot gas or shaft. Cooling and seals therefore affect the reading as much as the bearing itself.
Why vibration frequency matters
Imbalance, misalignment, looseness and bearing defects show up at different frequencies. Overall level alone shows that something changed, but not what.
Loads change the picture
Fan speed, damper position and gas density change forces on the rotor. Always record operating conditions with readings.
Reading Vibration Frequency Patterns
Use these patterns as a starting guide and confirm with a qualified analyst and manufacturer data.
| Pattern | What it may indicate | Typical next step |
|---|---|---|
| Once per revolution | Imbalance from buildup, wear or damage | Inspect impeller and clean or rebalance |
| Twice per revolution | Misalignment or coupling problems | Check alignment and coupling |
| Multiple harmonics | Looseness or a cracked or soft foundation | Inspect bolts, base and supports |
| Non-synchronous peaks | Developing bearing defects | Increase monitoring and plan bearing work |
| Broadband high-frequency noise | Late-stage bearing damage or poor lubrication | Urgent inspection and risk assessment |
Interpreting Temperature Correctly
Temperature moves slowly and depends heavily on conditions, so context matters.
Absolute vs change
A bearing can run hot but stable for years. A change from its own baseline is often more telling than a single alarm value.
Ambient and process heat
Hot gas, sun and seasons change readings. Compare with similar conditions and note any cooling water or airflow changes.
Lubricant and cooling system
Check oil level, flow, filters and coolers. Poor cooling can raise temperature while vibration remains normal.
Sensor health
Loose probes, damaged wiring and bad contact create false trends. Verify with a handheld measurement when a reading looks unusual.
Planning the Repair Once a Fault Is Confirmed
A planned repair is shorter and safer than an emergency stop.
- Confirm the fault and the extent: Use inspection, frequency analysis and lubrication checks before ordering parts.
- Prepare spares and tools: Bearings, seals, couplings and alignment tools should be ready before the window.
- Plan balancing and alignment: Rotor balancing, alignment and clearance checks should follow bearing work.
- Record a new baseline: Take readings after restart and store them as the new reference.
Mistakes That Hide Fan Faults
These habits cause late detection and repeat failures.
- Using one limit for all fans: Different fans and loads need their own normal ranges.
- Skipping load data: Readings without speed or damper position are hard to compare.
- Ignoring slow drift: Small changes over weeks can precede serious damage.
- Over-greasing after an alert: Excess grease may raise temperature and hide the real cause.
- Closing the alert without cause: If the cause is not recorded, the same failure repeats.
Building an Inspection Route for Fans
Routes keep readings consistent between people and shifts.
Define measurement points
Mark and photograph each point and direction, so every reading is taken in the same place.
Set normal ranges
Use baseline data by fan and operating condition, not only generic limits.
Record context
Include speed, damper position, ambient conditions and recent maintenance.
Add sensory checks
Note unusual noise, smell, leaks, guard condition and visible buildup.
Close the loop
If a reading looks wrong, create a work order and track the result.
Online Monitoring or Portable Readings?
The right mix depends on fan criticality, cost and failure history.
| Fan group | Typical approach | Reason |
|---|---|---|
| Critical large fans | Continuous vibration and temperature monitoring with alarms | Detects fast changes between rounds |
| Medium importance fans | Frequent route-based readings, with online sensors where justified | Balances cost and coverage |
| Smaller auxiliary fans | Routine inspection rounds and basic temperature checks | Keeps effort proportional |
Reliability Improvements Beyond Monitoring
Detection is only part of the job. Reducing the root causes lowers repeat faults.
- Reduce buildup: Improve cleaning, sealing and process control where deposits unbalance impellers.
- Improve lubrication practice: Use correct grease, quantities and tools, and keep lubricants clean.
- Address foundations: Soft feet, cracked bases and loose anchor bolts amplify vibration.
- Review design: Repeat failures may justify upgraded bearings, seals or protective coatings.
Spare Parts and Planning for Fan Repairs
The parts you hold determine how fast you can respond when data points to a fault.
Critical bearings and seals
Hold or reserve the bearings, seals and couplings for fans that can stop the kiln.
Rotor and impeller options
Large rotors have long lead times, so consider spare rotors or agreed repair services.
Tools and instruments
Keep alignment tools, balancing equipment and portable analyzers calibrated and available.
Supplier agreements
Agree response times and technical support for specialist repairs.
How Oxmaint Supports Fan Reliability
Oxmaint organizes the maintenance side of fan monitoring and does not replace sensors or analysis software.
- Asset records: Fans, motors, bearings and couplings are linked with their maintenance history.
- Route-based inspections: Mobile checklists capture readings, notes and photos at set intervals.
- Work orders: Confirmed faults become assigned tasks with parts and deadlines.
- Reporting: Dashboards show repeat failures, overdue tasks and time between repairs.
Case Study Style Walkthrough: A Developing Fan Fault
This is an illustrative scenario, not a real plant record. It shows how correlation guides a decision.
Week one
Route readings show slightly higher vibration at running speed, while bearing temperature is unchanged. The technician records load and notes visible dust on the impeller.
Week two
Vibration climbs again and temperature begins to rise. A work order is raised for inspection and a lubrication check, and spares are confirmed.
Week three
Inspection finds buildup on blades and a dry bearing. The team plans cleaning, rebalancing and lubrication in the next window.
After the repair
New baseline readings are stored, the cause is coded and the inspection interval is reviewed.
Signals Worth Adding Over Time
Start with temperature and vibration, then add more only when they answer a specific question.
- Motor current: Helps separate mechanical load changes from fan airflow changes.
- Oil pressure and flow: Important for sleeve bearings and oil-cooled systems.
- Shaft position: Can show wear or thrust changes on larger machines.
- Damper and speed data: Gives the context needed for fair comparison between readings.
Questions to Review at the Monthly Reliability Meeting
Short regular reviews keep fan data in use.
Which fans changed trend?
List fans with new drift in vibration or temperature since last month.
Which alerts were confirmed?
Check how many led to findings and how many were false.
Which repairs are overdue?
Review open work orders on critical fans and clear blockers.
What did we learn?
Record causes and adjust inspection or lubrication routines.
Frequently Asked Questions
Catch Fan Faults Before They Stop the Kiln
Organize readings, inspections and bearing work in one maintenance system.