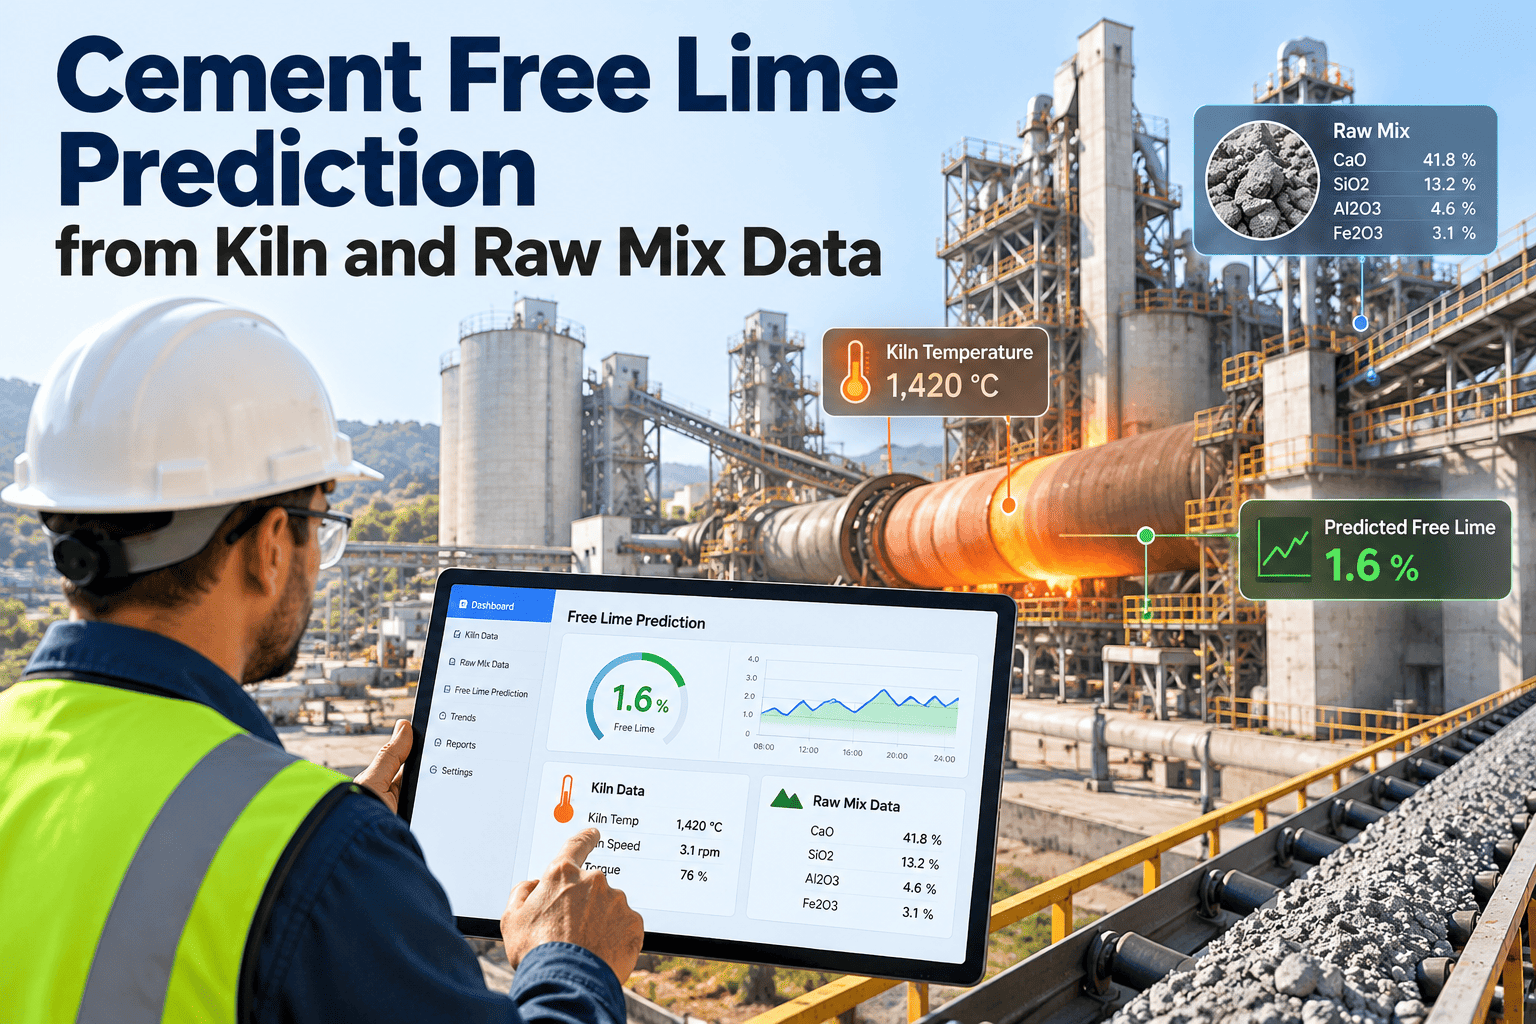
Free lime is the number a kiln crew waits on, and it arrives late. By the time a lab result confirms under-burnt clinker, the kiln has produced hours of material under the same conditions. Prediction closes that gap by estimating free lime from raw mix chemistry and kiln process data the plant already records. It only works when the instruments feeding it are healthy and the response is organised, which is why plants pair it with a cement maintenance management platform that keeps the data trustworthy.
Cement Free Lime Prediction from Kiln and Raw Mix Data
Predict clinker free lime before the lab result arrives, and keep the sensors, samplers and kiln equipment behind the prediction maintained, evidenced and acted on through one maintenance workflow.
Why Free Lime Is the Most Watched Clinker Number
What free lime actually tells you
- Free lime is uncombined calcium oxide left in clinker when the burning zone has not fully converted the raw mix into calcium silicate phases.
- It is a readout of everything upstream: raw mix chemistry, burning zone stability, feed homogeneity, fuel quality and kiln speed.
- Published plant targets commonly sit around 0.5 to 1.5 percent, although each plant sets its own band.
- Values drifting well above the plant limit point to under-burning and risk soundness problems in the cement.
Cost sits on both sides of the target
- Higher fuel consumption per tonne of clinker
- Harder clinker that costs more to grind
- More refractory stress and ring formation risk
- Unconverted lime reaching the cement mill
- Strength variability and soundness concerns
- Rework, blending or downgraded product
The Lab Delay Problem: Before and After Prediction
- Sample taken from the clinker cooler discharge
- Preparation and analysis in the lab
- Result entered and sent to the control room
- Operator adjusts hours after conditions changed
- Model estimates free lime continuously from process data
- Alert fires when the estimate trends toward the limit
- Operator corrects early; lab samples validate the model
- Instrument faults found by the model become work orders
Input Data: Which Signals Drive the Prediction
| Signal group | Typical variables | Why it matters for free lime | Maintenance dependency |
|---|---|---|---|
| Raw mix chemistry | LSF, silica modulus, alumina modulus, kiln feed fineness | Chemistry drift changes how much heat the mix needs to burn clean | Sampler, XRF and raw mill condition |
| Burning zone | Zone temperature, kiln torque or amps, flame condition | Direct indicator of burning intensity | Thermocouple and pyrometer calibration |
| Gas analysis | O2, CO, NOx at kiln inlet | NOx often tracks burning intensity | Gas analyser sampling lines and filters |
| Fuel system | Fuel flow, calorific value, ash and moisture | Ash infiltration shifts mix chemistry without warning | Feeder, weigh belt and flow meter accuracy |
| Feed and speed | Kiln feed rate, kiln speed, secondary air temperature | Sets residence time and heat balance | Feed weigh-feeder, kiln drive, cooler fans |
From Data to Decision: The Prediction Workflow
Choosing a Modelling Approach
| Approach | Best used for | Strength | Watch out for |
|---|---|---|---|
| Neural network soft sensor | Estimating the free lime value from many correlated variables | Handles non-linear kiln behaviour; academic work has reported satisfactory free lime and phase prediction | Needs well-cleaned data and retraining after process changes |
| Classification (good or under-burnt) | Giving operators a practical yes or no signal | Research suggests experts often prefer quality class over absolute value because of process complexity | Coarse; less detail near the limit |
| Statistical process control | Spotting drift in raw mix and burn zone stability | Simple, transparent, familiar to quality teams | Does not itself estimate the value |
| Hybrid | Model estimate plus SPC alarms plus lab validation | Balanced and easy to audit | Needs clear ownership across process and maintenance |
Root Causes Behind Free Lime Excursions
Why this matters to the maintenance team
- Many of these causes are equipment conditions: feeders, burners, cyclones, fans, seals and refractory.
- When prediction flags a trend, the first question is whether the process moved or the equipment degraded.
- A shared record of past interventions lets the team answer that question quickly instead of guessing.
Where Predictions Go Wrong: A Maintenance Risk Matrix
A Good Model on Bad Instruments Is Still a Bad Number
Keep every kiln and raw mix sensor on a schedule, with calibration and repair history in one place.
Reading the estimate alongside process context
- A rising estimate with stable raw mix chemistry usually points toward burning zone, fuel or feed behaviour.
- A rising estimate after an LSF shift points toward the raw mill and proportioning system.
- An estimate that moves while every other signal stays flat deserves an instrument check before any process change.
- An estimate that disagrees with consecutive lab results suggests retraining or a data alignment problem.
Turning Prediction Alerts into Maintenance Action
How Oxmaint supports this workflow
- Asset management keeps the kiln, raw mill, samplers, analysers and feeders in one register with their history.
- Preventive maintenance schedules calibration and cleaning for the instruments that feed the model.
- Work orders capture each sensor fault or drift investigation, from alert to closeout.
- Mobile inspections let technicians record checks at the kiln and sampling points on the spot.
- Dashboards and reports show repeat instrument problems and downtime, supporting decisions on spares and upgrades.
- Inventory tracks critical spares such as thermocouples, sampling filters and analyser consumables.
A Practical Rollout Timeline
Common Mistakes to Avoid
What a good response record looks like
- The prediction alert, its time and the estimated value at that moment.
- The operator and process engineer actions taken, with the lab result that followed.
- Any instrument or equipment fault found, with the work order that corrected it.
- The outcome: whether free lime returned to the target band, and how long it took.
KPIs to Track the Programme
Reviewing the KPIs together
- Hold a short monthly review with process, quality and maintenance in the same room.
- Compare prediction error trends with the calibration and repair history of the model inputs.
- Decide whether each repeat deviation needs a process change, a maintenance task or a model update.
- Record decisions so the next review starts from evidence rather than memory.
Readiness Checklist Before You Deploy
- Lab free lime results timestamped accurately
- Kiln signals logged at consistent intervals
- Raw mix results linked to production time
- Known sensor faults documented
- Calibration schedule for each input instrument
- Owner assigned for each sampler and analyser
- Critical spares identified and stocked
- Work order route defined for model-driven alerts
- Alert limits agreed by process and quality
- Operator response steps written down
- Retraining triggers defined after major changes
- Review cadence set for model performance
Frequently Asked Questions
Keep the Data Behind Your Free Lime Prediction Trustworthy
Organise kiln and raw mix instrument maintenance, calibration and corrective work in Oxmaint so predictions stay accurate and operators can rely on them.