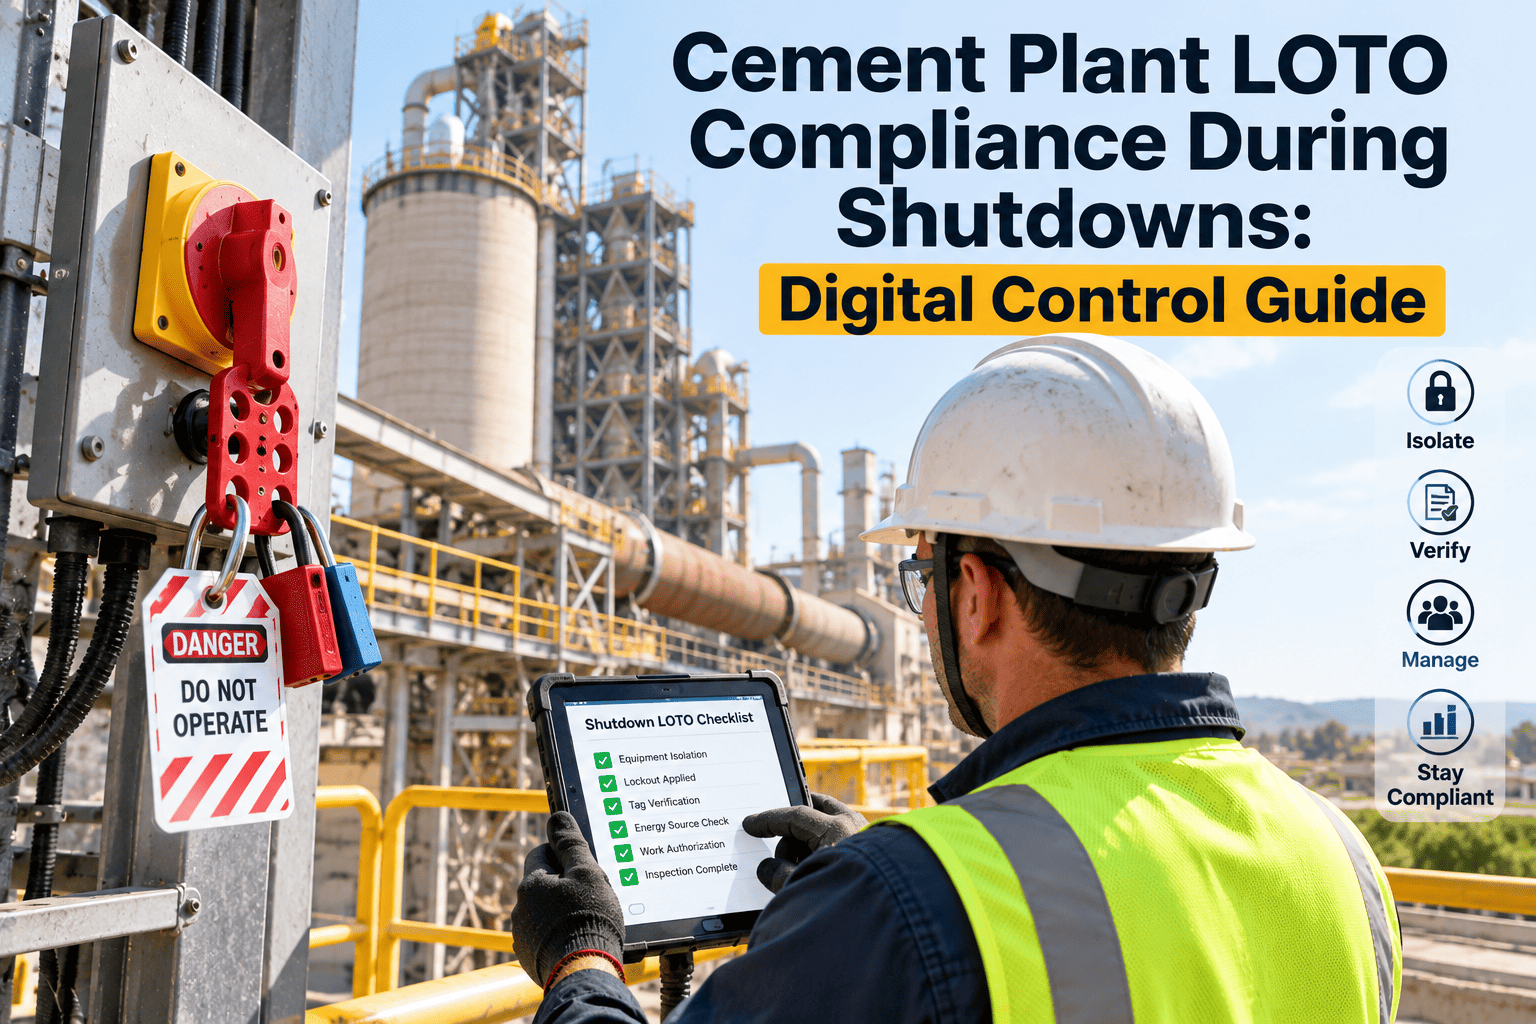
A cement plant shutdown puts more people on more equipment in less time than any other event on the calendar. Contractors, riggers, refractory crews and in-house technicians all need safe access to the kiln, preheater, mills, fans and conveyors at once. Lockout/tagout is what keeps that access survivable, yet paper tags and whiteboards struggle at this scale. This guide shows how to control isolations digitally, with maintenance management software as the backbone.
Cement Plant LOTO Compliance During Shutdowns: Digital Control Guide
Link every isolation to a work order, every lock to a named person and every verification to a record, so a shutdown stays controlled when hundreds of tasks run in parallel.
Why Shutdowns Stress Every Energy Control Program
During normal operation, a lockout involves one crew and one machine. During a shutdown the same procedures are repeated hundreds of times, often by people who do not know the plant.
- Contractor crews arrive in large numbers with different safety cultures and different lock hardware.
- Work runs around the clock, so shift handovers happen with locks still applied.
- Multiple trades work on the same equipment, such as mechanical, electrical, refractory and scaffolding crews.
- Schedule pressure pushes people toward shortcuts, such as skipping verification or sharing a lock.
- Isolation points are numerous and spread across motor control centers, valves, dampers and field panels.
In the United States, general industry lockout requirements sit in OSHA 29 CFR 1910.147, while quarry and mining operations fall under MSHA rules. Other countries and corporate standards add their own layers, so confirm which apply to each area of your site.
Cement-Specific Stored Energy You Must Plan For
Opening a breaker is rarely enough in a cement plant. Many hazards remain after power is isolated.
| Area | Hazardous Energy | Isolation Consideration |
|---|---|---|
| Preheater cyclones | Hung-up material, blockage, hot gas, compressed air from air cannons | Lock out air supply, depressurize cannons, plan safe clearing methods |
| Kiln | Rotation, residual heat, falling coating or refractory | Lock main and auxiliary drives, control turning, confirm cooling and support |
| Raw and cement mills | Rotating shell, girth gear, grinding media, hydraulic systems | Lock drives and auxiliary drives, release hydraulic pressure, block rotation |
| Silos and hoppers | Engulfment, bridged material, aeration and extraction systems | Isolate feeders and aeration, combine with confined space permit |
| Bucket elevators and conveyors | Back-driving, gravity, belt tension | Lock drives, fit backstops or pins, release tension |
| Fans and dampers | Windmilling, pneumatic and hydraulic actuators | Lock motors, secure impellers, isolate actuator energy |
| Coal and alternative fuel systems | Dust, ignition sources, feeders, pressurized lines | Isolate feed, purge lines, control ignition sources |
Where Paper-Based LOTO Breaks Down
- Isolation points copied by hand from outdated drawings
- No live view of which locks are on which equipment
- Contractor lock lists kept in separate files
- Verification signatures easy to skip or backfill
- Restart readiness depends on someone walking the plant
- Audit evidence scattered across binders
- Standard procedures attached to each asset
- Live status of every isolation tied to a work order
- One register for employees and contractors
- Required verification steps before work can start
- Restart checks that confirm all locks are cleared
- Time-stamped history ready for audits
The Digital Lockout Lifecycle, Step by Step
Put Every Isolation on the Work Order
See how procedures, checklists and completion records can live beside each shutdown task.
What a Compliant Shutdown LOTO Record Contains
Inspectors and internal auditors look for evidence that the program works in practice, not only that it exists on paper.
Managing Contractors Without Losing Control
Shutdown contractors often carry the highest exposure and the least familiarity. Digital control gives you a consistent method for all of them.
- Require induction and LOTO competence checks before issuing any plant access.
- Use a single lock and tag standard so devices are recognizable and traceable.
- Assign a plant owner to each contractor task, responsible for the isolation boundary.
- Record contractor crew changes so the lock register stays accurate day and night.
- Prohibit shared or borrowed locks, and review lock removal exceptions daily.
- Run a short daily safety review of open isolations and near misses.
Risk Matrix: Common Failure Points
| Failure Point | Typical Cause | Digital Control |
|---|---|---|
| Missed isolation point | Outdated drawing or incomplete scope | Standard procedure on the asset, reviewed before the stop |
| Skipped verification | Schedule pressure | Mandatory verification step before task start |
| Residual stored energy | Focus on electrical isolation only | Energy source checklist covering hydraulic, pneumatic, gravity, thermal |
| Lock removed by wrong person | Handover confusion | Lock register with named owners and exceptions log |
| Premature restart | Poor communication between trades | Clearance check across all tasks on the asset |
KPIs for a Controlled Shutdown
Add leading indicators such as observation counts, near-miss reports and audit findings closed on time. Trends here tell you more than injury rates alone.
Pre-Shutdown LOTO Readiness Checklist
- Equipment hierarchy and isolation procedures reviewed and updated
- Stored energy sources identified for kiln, preheater, mills and silos
- Lock, tag and group lockout box inventory confirmed
- Contractor induction and competence verified
- Confined space and hot work permits aligned with isolations
- Shift handover method agreed and tested
- Restart and clearance process defined
- Emergency and rescue arrangements confirmed
How OXMAINT Supports the Workflow
OXMAINT organizes the maintenance side of energy control so that safety steps travel with the work.
Confirm with your safety team how digital records fit your formal permit-to-work and lockout policies. Software supports the procedure, it does not replace it.
Group Lockout and Shift Handover Rules
Large shutdown tasks often use group lockout, where many people work under one isolation. This works only with strict key control.
High-Risk Situations to Treat Separately
Some cement tasks need more than a standard lockout. Combine isolations with permits and specific controls.
- Preheater cyclone clearing: handle hung-up material with planned methods, correct PPE, controlled access and isolation of air cannons and feeders.
- Kiln entry: confirm cooling, lock main and auxiliary drives, control kiln rotation, check for loose coating and brick, and use a confined space permit.
- Mill entry: lock the main motor and auxiliary drive, secure the shell against rotation and control access during liner work.
- Silo and hopper work: isolate extraction and aeration, address engulfment risk and use rescue arrangements.
- Electrical work: separate lockout from live work rules, verify absence of voltage and ground where required.
- Work at height: lock out equipment below and protect against dropped objects.
A short reference table for each area helps contractors who work in your plant for only a few days.
Training and Competence Requirements
Typical Audit Findings and How to Avoid Them
| Finding | Root Cause | Preventive Action |
|---|---|---|
| Generic procedures that do not match the equipment | Copied templates, no field review | Equipment-specific procedures reviewed with operators and electricians |
| Missing evidence of annual inspection | No owner or schedule | Recurring inspection tasks with assigned owners |
| Contractor locks not traceable | Separate paper registers | One lock register for all crews |
| Procedures not updated after modifications | No link between change management and LOTO | Equipment change triggers a procedure review |
| Stored energy not addressed | Focus on electrical isolation | Mandatory energy source checklist |
| Verification not recorded | Informal practice | Verification as a required completion step |
Treat each audit finding as a work order with an owner and a due date, and record the closure evidence.
After the Shutdown: Learning From the Records
- Count how many isolations were planned in advance, and how many were improvised.
- Review near misses and stop-work events to find recurring weak points.
- Identify equipment that lacked clear isolation points and update drawings or labels.
- Check whether contractor induction was completed before arrival or after delays.
- Update procedures with feedback from the technicians who used them.
- Feed lessons into the next shutdown scope and permit planning.
The same records help show regulators and corporate auditors that your program improves over time.
Quick Reference: Stop-Work Triggers
- A lock, tag or isolation point cannot be found or does not match the procedure.
- Equipment moves, makes noise or shows pressure after isolation is verified.
- Scope changes and new energy sources appear that the procedure did not cover.
- A crew member is unsure about their role or cannot show a valid lock.
- Weather, access or lighting conditions change the safety of the task.
Frequently Asked Questions
Run Your Next Shutdown With Verified Energy Control
Give planners, supervisors and contractors one clear record of what is isolated, who is exposed and when equipment is safe to restart.