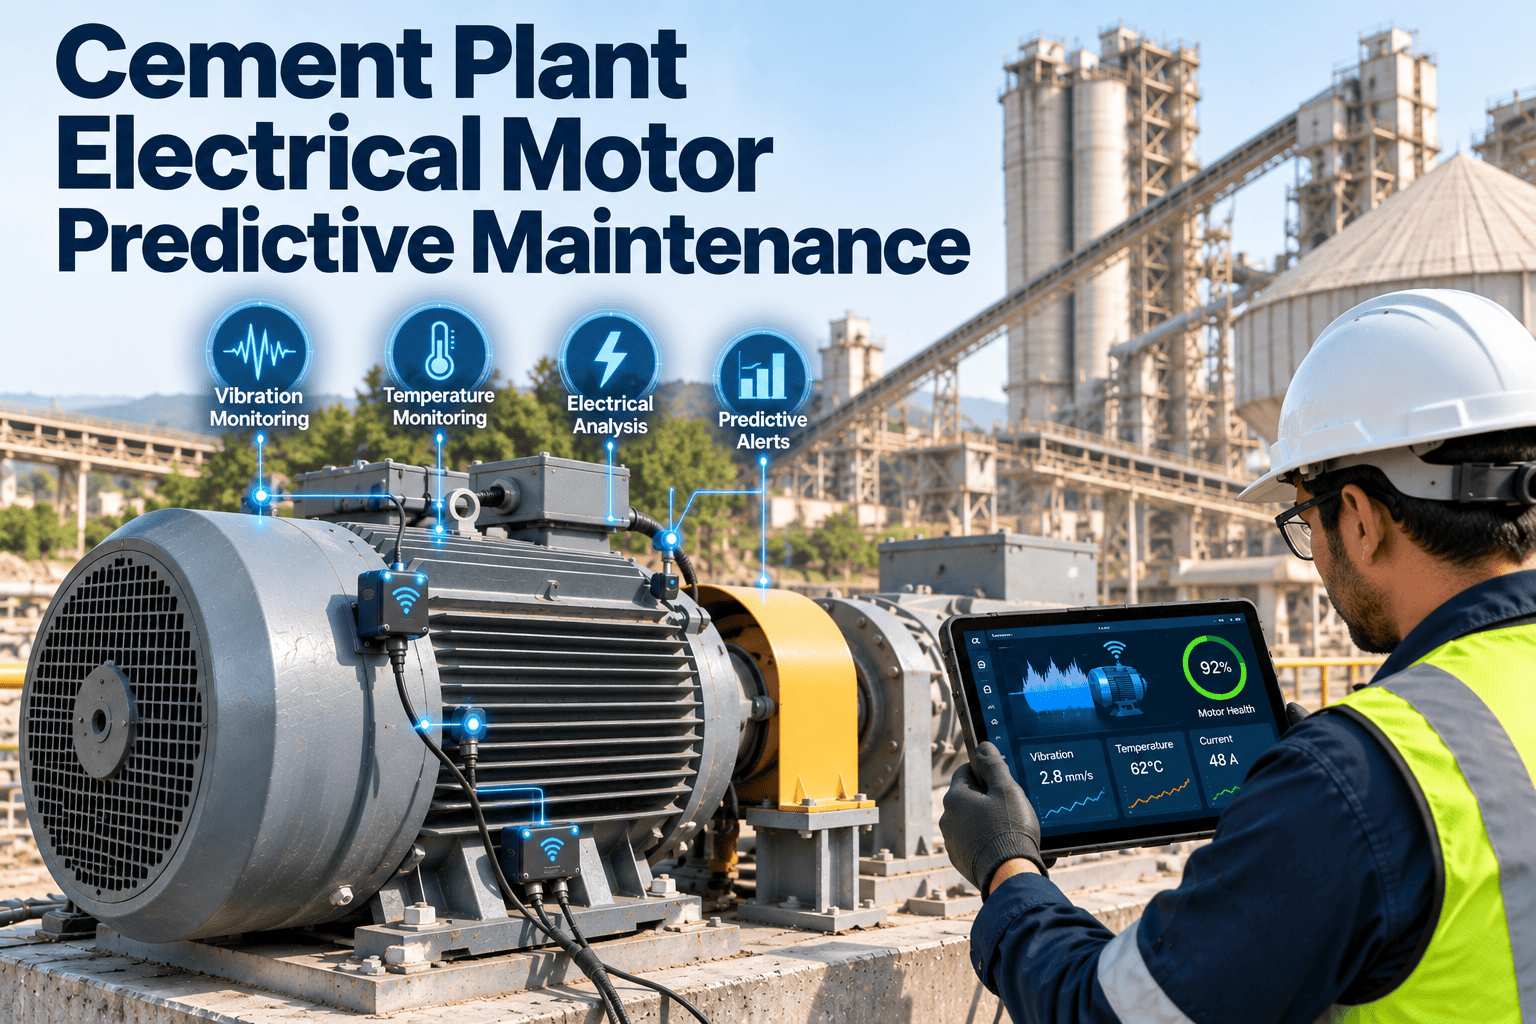
Electric motors drive almost every critical process in a cement plant, from the kiln and raw mill to fans, crushers, elevators and the cement mill itself. A single motor failure can stop a whole process section, and the repair is rarely quick when the motor is large or custom wound. Most failures give warning weeks or months ahead through vibration, heat, current or insulation changes. This guide explains how cement plants turn those signals into planned work, and how a cement plant maintenance platform keeps the follow-up organized.
Cement Plant Electrical Motor Predictive Maintenance
Detect bearing, winding and rotor faults early, rank motors by process risk, and convert every warning into a scheduled work order before the motor trips.
- HealthyBaseline readings recorded
- Early signalUltrasound and vibration trend up
- Confirmed faultCurrent, heat and insulation data agree
- Planned repairWork order scheduled in a stop
- Functional failureTrip, process stop, emergency repair
Why Cement Plant Motors Fail Early
Cement plants are hard on electrical machines. The environment, the duty cycle and the way power is supplied all shorten motor life when they are not managed.
Dust and heat
Fine dust blocks cooling paths and enters bearings and terminal boxes. Hot zones near kilns and coolers raise winding temperature and age insulation faster.
Heavy starting and load swings
Mills, crushers and conveyors start under load and see sudden changes. Repeated starts stress rotor bars, couplings and windings.
Power quality
Voltage imbalance, harmonics from drives and poor grounding cause overheating and can damage bearings through circulating currents.
Lubrication errors
Too little or too much grease, or the wrong type, is a very common root cause of bearing damage in dusty plants.
Misalignment and looseness
Thermal growth, worn foundations and loose bolts create vibration that slowly destroys bearings and couplings.
Moisture and contamination
Washdown, rain and condensation lower insulation resistance, especially in motors that sit idle during stops.
Which Technique Finds Which Fault
No single test catches everything. Combine methods according to motor size, speed and criticality.
| Technique | Faults it can reveal | Typical use in a cement plant |
|---|---|---|
| Vibration analysis | Bearing wear, imbalance, misalignment, looseness, rotor problems | Routes on fans, mills, elevators, pumps and gearbox-driven motors |
| Infrared thermography | Hot bearings, loose connections, overloaded windings, blocked cooling | Motor bodies, terminals, starters and switchgear |
| Motor current signature analysis | Broken rotor bars, eccentricity, supply imbalance, load problems | Large motors that are hard to access while running |
| Insulation resistance and polarization index | Moisture, contamination, insulation ageing | Offline tests during stops and after long idle periods |
| Ultrasound | Early bearing friction, lubrication problems, partial discharge activity | Grease optimization and early screening of bearings |
| Winding resistance and surge tests | Turn-to-turn faults, phase imbalance | Acceptance of rewound motors and suspect machines |
| Power quality measurement | Harmonics, voltage imbalance, sags | Drive-fed motors and feeders with repeated trips |
Rank Motors by Process Risk First
Start with the motors whose failure hurts most. Score each one on consequence and on how likely it is to fail.
Typical high-consequence motors
- Kiln main drive and auxiliary drive
- Kiln ID fan and cooler fans
- Raw mill, coal mill and cement mill main drives
- Separator and mill fan motors
- Preheater and kiln feed elevators with no standby
- Large crusher motors and apron or belt drives
Smaller motors with standby units or short lead times can follow a simpler plan. The goal is to apply the most effort where an outage costs the most.
Put Every Motor on a Condition Plan
Register motors, assign inspection routes, record readings and raise work orders from one system your whole team can use.
From Reading to Repair: The Predictive Workflow
- 1
Build the motor register
Record nameplate data, drive type, bearing sizes, location, criticality, spares and test history for each motor.
- 2
Set baselines
Capture vibration, temperature, current and insulation values when the motor is healthy so later changes are meaningful.
- 3
Collect on a schedule
Run routes at intervals that match criticality. Use online sensors where access is difficult or the risk is high.
- 4
Set alert limits
Use standards such as ISO 20816 for vibration severity and manufacturer limits for temperature and insulation as starting points.
- 5
Diagnose and confirm
Compare two or more methods before ordering a repair, so false alarms do not erode trust in the program.
- 6
Plan the job
Create a work order with parts, tools, permits and a target stop window. Reserve the spare motor if one exists.
- 7
Verify and learn
Retest after repair, record the cause found, and adjust intervals or limits using what the failure taught you.
Time-Based Versus Predictive Motor Care
Calendar-only maintenance
- Greases and inspects on fixed dates regardless of condition
- Misses faults that develop between visits
- Replaces healthy bearings and still suffers surprise trips
- Leaves little evidence for deciding rewind or replace
Predictive and condition-based care
- Uses trends to decide when work is truly needed
- Finds faults early enough to book a stop window
- Reduces emergency call-outs and spare-part rush costs
- Builds a failure history that guides purchasing
Most plants need both
Basic preventive tasks such as cleaning, greasing, tightening and visual checks still matter. Predictive methods add the evidence that tells you when to act and when to leave a healthy motor alone.
Motor Inspection Checklist for Stops and Rounds
While running
- Listen for unusual bearing or electrical noise
- Record bearing and frame temperature
- Check cooling fan, guards and air inlets for dust
- Review vibration readings against the last trend
- Check load current against nameplate and normal range
- Look for grease leakage and oil stains
During a planned stop
- Measure insulation resistance and polarization index
- Check terminal box for moisture, heat marks and loose lugs
- Confirm alignment and soft foot condition
- Inspect couplings, bolts and base frame
- Clean cooling passages and replace worn filters
- Test space heaters on motors that sit idle
Special Cases in Cement Plants
Large mill and kiln drives
Repair lead times are long. Keep detailed test records, agree rewind or exchange options with a service provider, and plan spare strategy early.
Variable frequency drives
Check filters, cooling and cable condition. Watch for bearing currents and consider shaft grounding where drive-fed motors show repeated bearing failures.
Motors in classified areas
Coal handling areas may be classified. Any repair must preserve the protection concept, and records should show who did the work and which parts were used.
KPIs That Show the Program Is Working
Motor-related downtime
Hours lost to motor trips and repairs, tracked by area.
Planned versus emergency repairs
The share of motor jobs scheduled ahead of failure.
Route completion
Inspection and test routes finished on time.
Mean time between failures
Trend per motor family, especially fans and mill drives.
Repeat failure rate
Motors failing again for the same cause.
Review these monthly with operations. A rising planned share and falling repeat failures indicate that warnings are being acted on. Share the results with operations and finance so the value of early detection, such as avoided emergency repairs and shorter stops, is visible beyond the maintenance team and supports continued investment in the program.
How Oxmaint Supports Motor Reliability
Oxmaint organizes motor data and follow-up work. It does not replace diagnostic instruments, but it keeps their findings from getting lost.
Asset management
Store each motor with nameplate data, location, drive details, documents and complete repair history.
Preventive and inspection tasks
Schedule greasing, cleaning, thermography and insulation tests with checklists on mobile devices.
Condition-based work orders
Create corrective work when a reading crosses a limit and track it through approval, planning and completion.
Spare motors and parts
Track bearings, couplings and spare motors so a diagnosed fault can be fixed in the next available window.
Scheduling
Group motor jobs with kiln, mill or fan stops to use the downtime well.
Reports and dashboards
See failure patterns, backlog, repeat issues and compliance with planned routes in one view.
Bearings and Lubrication: The Biggest Everyday Lever
Bearings are among the most common motor failure points, and grease practice often decides how long they last.
Right grease
Mixing incompatible greases can break down the lubricant. Record the approved grease for every motor and label the grease point.
Right quantity
Over-greasing raises temperature and can push grease into windings. Use a defined shot count or ultrasound guidance instead of guessing.
Right interval
Speed, size, temperature and dust all change the interval. Start from the manufacturer and refine with condition data.
Signs that lubrication is the real problem
- Temperature rises shortly after every greasing event
- Repeated bearing failures on motors with the same duty
- Dark, dry or contaminated grease at the drain
- High-frequency vibration or ultrasound levels before any mechanical fault
Rewind, Repair or Replace?
When a motor is diagnosed with a serious fault, the decision should rest on data, not habit.
| Question | What to check | Why it matters |
|---|---|---|
| How many times has it been rewound? | Service history and repair records | Repeated rewinds can reduce efficiency and reliability |
| What caused the failure? | Root cause findings, not just the damaged part | Repairing without fixing the cause invites a repeat |
| Is a spare available? | Spare register and lead time for exchange | A swap may restore production faster than a repair |
| What is the energy impact? | Efficiency class and operating hours | Long-running motors may justify a higher-efficiency replacement |
| Is the repair quality proven? | Test reports before and after the work | Documented results show whether the repair met requirements |
Records, Standards and Safety
Good records support audits, insurance reviews and internal learning.
- A
Electrical safety
Lockout and permit procedures must be followed for every motor task. Store the permit and isolation reference with the work order.
- B
Test documentation
Insulation, resistance and vibration results should be saved with date, instrument, operator and motor identity.
- C
Standards references
Motor design and testing commonly follow IEC 60034 and IEEE guidance, while vibration is often judged against ISO 20816. Use the versions your plant has adopted.
- D
Competency
Record who is qualified for thermography, vibration analysis and high-voltage work, and assign tasks accordingly.
Reading the Warning Signs
Mechanical signals
- Rising vibration at bearing frequencies
- Growing looseness or misalignment signatures
- Hot spots on bearing housings
- Noise that changes with load or speed
Electrical signals
- Current imbalance between phases
- Falling insulation resistance after similar conditions
- Sidebands in current signature near line frequency
- Repeated overload or earth fault trips
Trend beats single readings
One high number may be noise. A steady climb across several readings, confirmed by a second method, is the stronger case for planned action.
Planning Motor Work Into Stops
A diagnosed fault only pays off if the repair lands in a suitable window.
- Keep a live backlog of confirmed motor defects ranked by risk
- Match each job to kiln, mill or fan stop calendars
- Stage spare motors, bearings and couplings before the stop starts
- Assign qualified crews and confirm lifting and access needs
- Retest and record results before returning the motor to service
Why backlog visibility matters
When defects sit in notebooks, they miss the stop window and become emergencies. A shared backlog lets maintenance and operations agree early on what must be fixed and what can wait.
Mistakes That Weaken Motor Programs
- Collecting data without a clear owner for acting on alarms
- Skipping baselines, which makes later trends hard to judge
- Greasing by habit instead of measured quantity and interval
- Ignoring power quality when bearings keep failing
- Rewinding motors without recording test results before and after
- Treating every motor the same regardless of process impact
Questions for your next reliability review
- Which motors caused the most lost production hours last year?
- How many alarms were acted on within the planned time?
- Which failures had a warning that nobody recorded?
- Do critical motors have a tested spare or a confirmed exchange option?
- Are baselines current after rewinds, replacements or process changes?
Answering these honestly shows where the program is strong and where signals are being lost between inspection, diagnosis and repair. Fix the weakest link first, then repeat the review every quarter.
A realistic first step
Choose the ten motors whose loss would stop the plant, set baselines and start a trend. Use the first quarter to prove value before extending to the rest.
Frequently Asked Questions
What is predictive maintenance for electric motors?
It uses vibration, temperature, current and insulation data to find faults early and schedule repairs before failure.
Which cement plant motors should come first?
Start with kiln, mill and fan drives and any motor without a standby. Book a demo to see how to rank them.
Do we need online sensors on every motor?
No. Use online monitoring on critical or hard-to-reach motors and walk-around routes for the rest.
How often should motors be tested?
Intervals depend on criticality, duty and history. Begin with OEM guidance and adjust using trend data.
Can a CMMS manage predictive findings?
Yes, it tracks readings, work orders and history. Sign up for Oxmaint to organize them.
Catch Motor Faults Before They Stop the Kiln
Bring motor registers, routes, work orders and spares into one maintenance system and act on warnings in time.