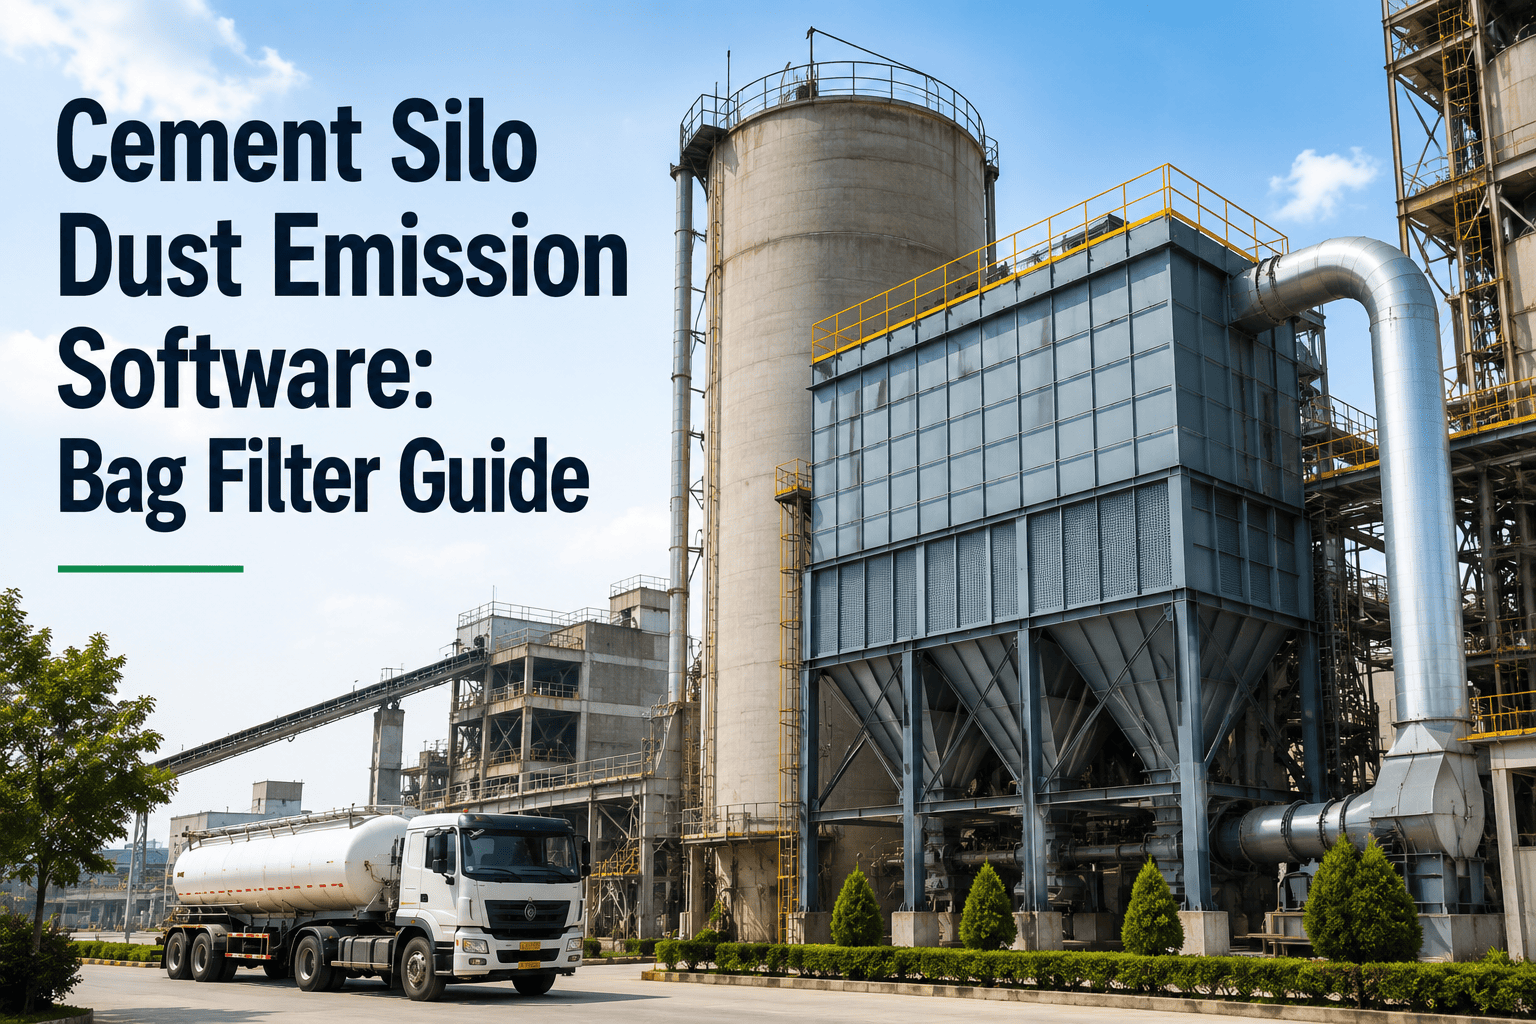
A cement silo does not fail loudly. Differential pressure across the bin-vent filter drifts up a few millimeters of water column at a time, a pulse valve solenoid starts firing late, dust cakes onto the filter media, and weeks later the plant has a visible dust plume rolling off the top of the silo during a routine tanker fill. By the time anyone sees it from the ground, the filter bags are already compromised and a compliance report is overdue. Cement silo dust emission software closes that gap by turning differential pressure, high-level probe, and pulse-jet data into scheduled work orders long before a top-of-silo release becomes a reportable event. This guide covers exactly how that monitoring should work, and you can book a 30-minute walkthrough to see it running against your own silo fleet.
Silo Dust & Emissions
Cement Silo Dust Emission Software: The Bag Filter Guide
Top-of-silo dust releases are preventable. See how differential pressure tracking and automated CMMS work orders stop them before they start.
How a Top-of-Silo Dust Release Actually Develops
A visible dust event at the silo vent is never a sudden failure. It is the last step in a chain that usually starts weeks earlier, inside the bag filter housing where nobody is looking.
Stage 1 — Weeks Before
Dust cake begins building on filter media
Normal cement dust loading forms a cake on the bag surface. This is expected, but if compressed air for the pulse-jet system is damp or under-pressured, the cake stops releasing cleanly and starts accumulating layer over layer.
Stage 2 — Days Before
Differential pressure trends upward
As the cake thickens, airflow resistance across the filter media rises steadily. A DP gauge or sensor logging this trend shows a clear upward slope well before any visible symptom appears at the vent.
Stage 3 — Hours Before
Pulse valves lose cleaning effectiveness
Once DP crosses into the warning band, pulse-jet cleaning can no longer keep pace with incoming dust load, especially during a fast tanker fill cycle that spikes airflow through the vent filter.
Stage 4 — The Event
Visible dust escapes at the silo top
Media blinding or a torn bag lets particulate pass straight through, producing a visible plume during filling — the point at which the incident becomes a compliance and community issue, not just a maintenance one.
Differential Pressure Bands Every Silo Filter Should Be Watched Against
Differential pressure is the single clearest early signal a bin-vent filter gives off. These are the three bands a monitoring program should classify every reading into.
Normal Range
Steady DP with a gentle upward slope between cleaning cycles is normal cake buildup. No action needed beyond routine logging.
Warning Band
A sustained rise beyond the normal cleaning range signals blinding or a compressed air supply issue. This should auto-trigger an inspection work order the same shift.
Critical Band
DP at or near the filter's rated maximum, or a sudden unexplained drop, both indicate imminent bag failure and call for an immediate offline check before the next fill cycle.
Still logging DP readings on a clipboard? OxMaint pulls differential pressure straight from your silo vent sensors and flags any compartment drifting into the warning band automatically.
What a Connected Silo Monitoring Setup Actually Tracks
Differential pressure alone tells only part of the story. A complete silo dust emission program pulls in four data streams, each catching a different failure path.
Differential Pressure Sensors
Continuous DP readings across the bin-vent filter housing, trended shift over shift, catching blinding and bag damage before either becomes visible at the vent.
High-Level Probes
Rotary paddle or capacitance probes inside the silo prevent overfilling, which forces excess air and dust straight into the vent filter faster than it can be cleaned.
Pulse-Jet Air Supply Monitoring
Pressure and moisture sensors on the compressed air line catch the damp or under-pressured supply that causes most premature cake buildup on filter media.
Discharge and Hopper Sensors
Bridging or blockage at the dust bin discharge point backs material up into the filter housing, so hopper-level sensors catch that failure path independently of DP.
Inspection Cadence That Keeps Silo Filters Out of the Warning Band
A structured inspection routine catches what sensors alone can miss — physical bag condition, cage integrity, and gasket wear. This is the cadence built into every silo filter work order template in OxMaint.
Every Shift
Log differential pressure and note any visible dust at the vent during active filling
Weekly
Verify pulse-jet solenoid timing and check compressed air supply pressure and moisture
Monthly
Inspect filter bag condition, cage integrity, and gasket seating inside the vent housing
Quarterly
Check high-level probe calibration and confirm hopper discharge mechanism runs freely
KPIs a Silo Dust Program Should Report Monthly
0
Visible top-of-silo dust events
The target for every actively monitored silo is zero visible release events during fill cycles.
100%
DP logging coverage across silos
Every silo vent filter should have continuous or shift-logged DP data with no coverage gaps.
<24 hr
Response time to a warning-band alert
A DP reading crossing into the warning band should have an inspection work order closed within one day.
>90%
Planned bag replacement rate
Most bag changes should come from condition-based scheduling rather than an emergency swap after a failure.
One missed DP reading is all it takes to miss a warning sign. OxMaint auto-generates the inspection work order the moment a silo filter crosses into the warning band — no manual monitoring required.
Frequently Asked Questions
What differential pressure signals a cement silo bag filter is about to fail?
A sustained upward trend beyond the filter's normal cleaning range signals blinding, while a sudden unexplained drop usually points to a torn or failed bag. Both should trigger an inspection the same shift.
Book a session to set your own DP thresholds.
Why does a silo dust release usually happen during tanker filling?
Fast fill cycles spike airflow through the bin-vent filter faster than pulse-jet cleaning can keep pace with, which is why filters already sitting in the warning band tend to fail visibly right when a tanker is loading.
Can moisture in the compressed air line really cause a dust event?
Yes. Damp compressed air stops the dust cake from releasing cleanly during each pulse cycle, so it builds up layer by layer until differential pressure climbs into the critical band and cleaning stops working entirely.
How often should silo filter bags be physically inspected?
Monthly physical checks of bag condition, cage integrity, and gasket seating catch problems that differential pressure trends alone can miss, such as early-stage tearing or seal wear.
See the full inspection template in OxMaint.
What role does the high-level probe play in preventing dust releases?
Overfilling forces excess air and dust into the vent filter faster than it can process, so a correctly calibrated high-level probe prevents the overload condition that often precedes a visible release.
Stop Top-of-Silo Releases Before They Start
OxMaint connects your differential pressure, high-level, and pulse-jet sensors into one CMMS that flags a drifting silo filter days before it becomes a compliance incident.