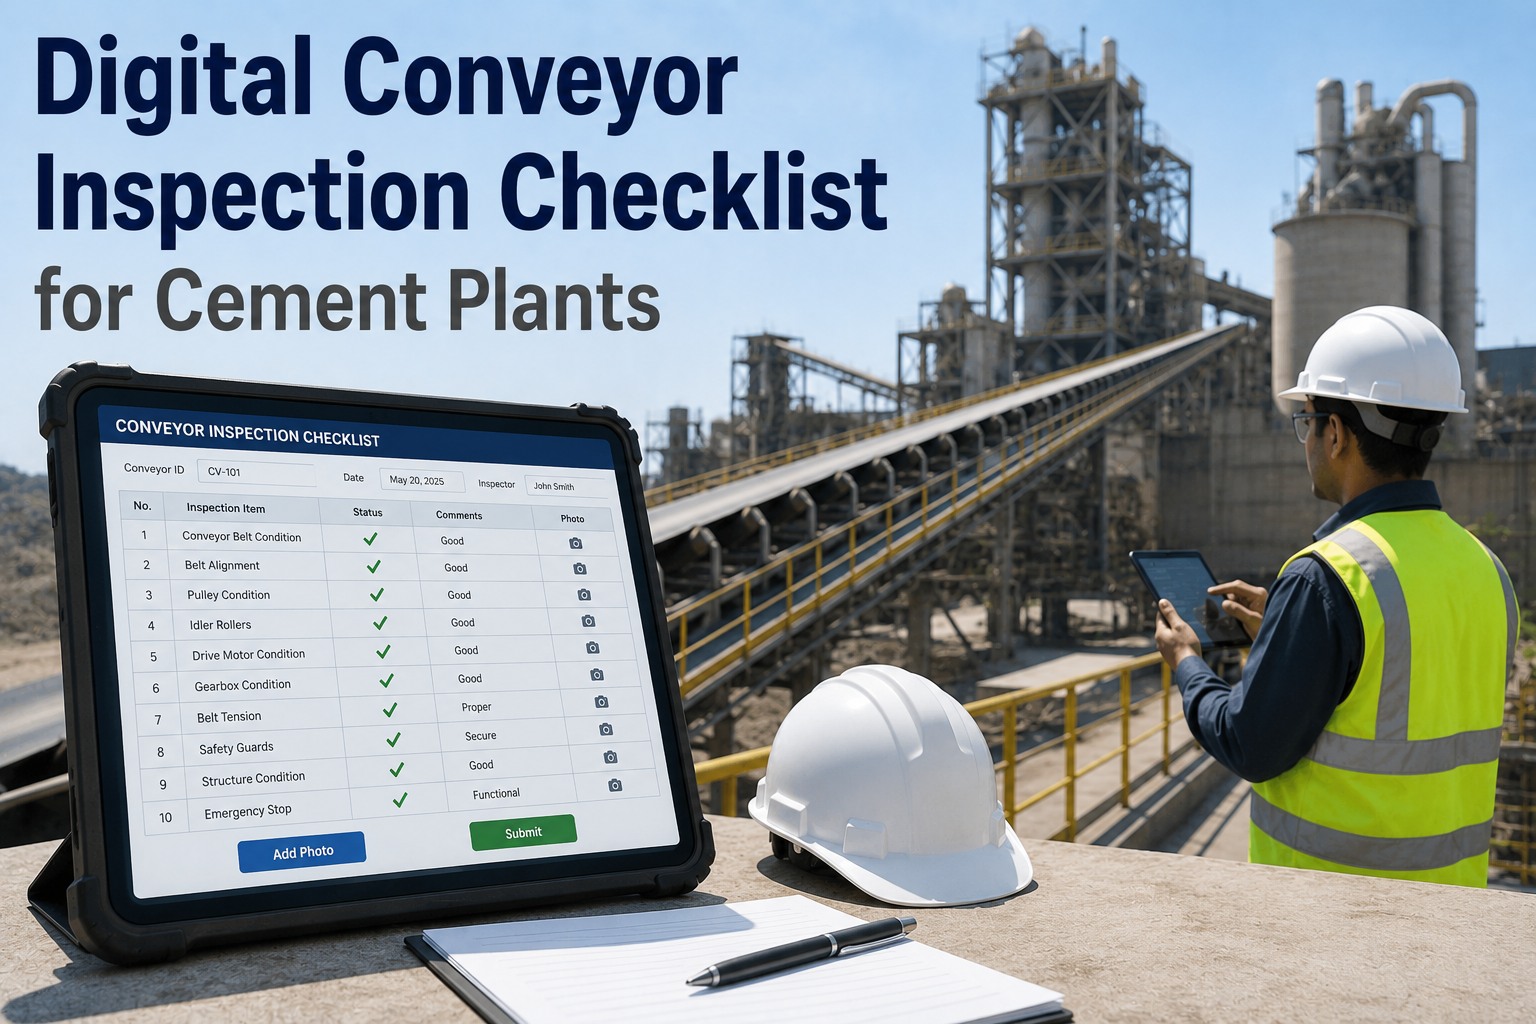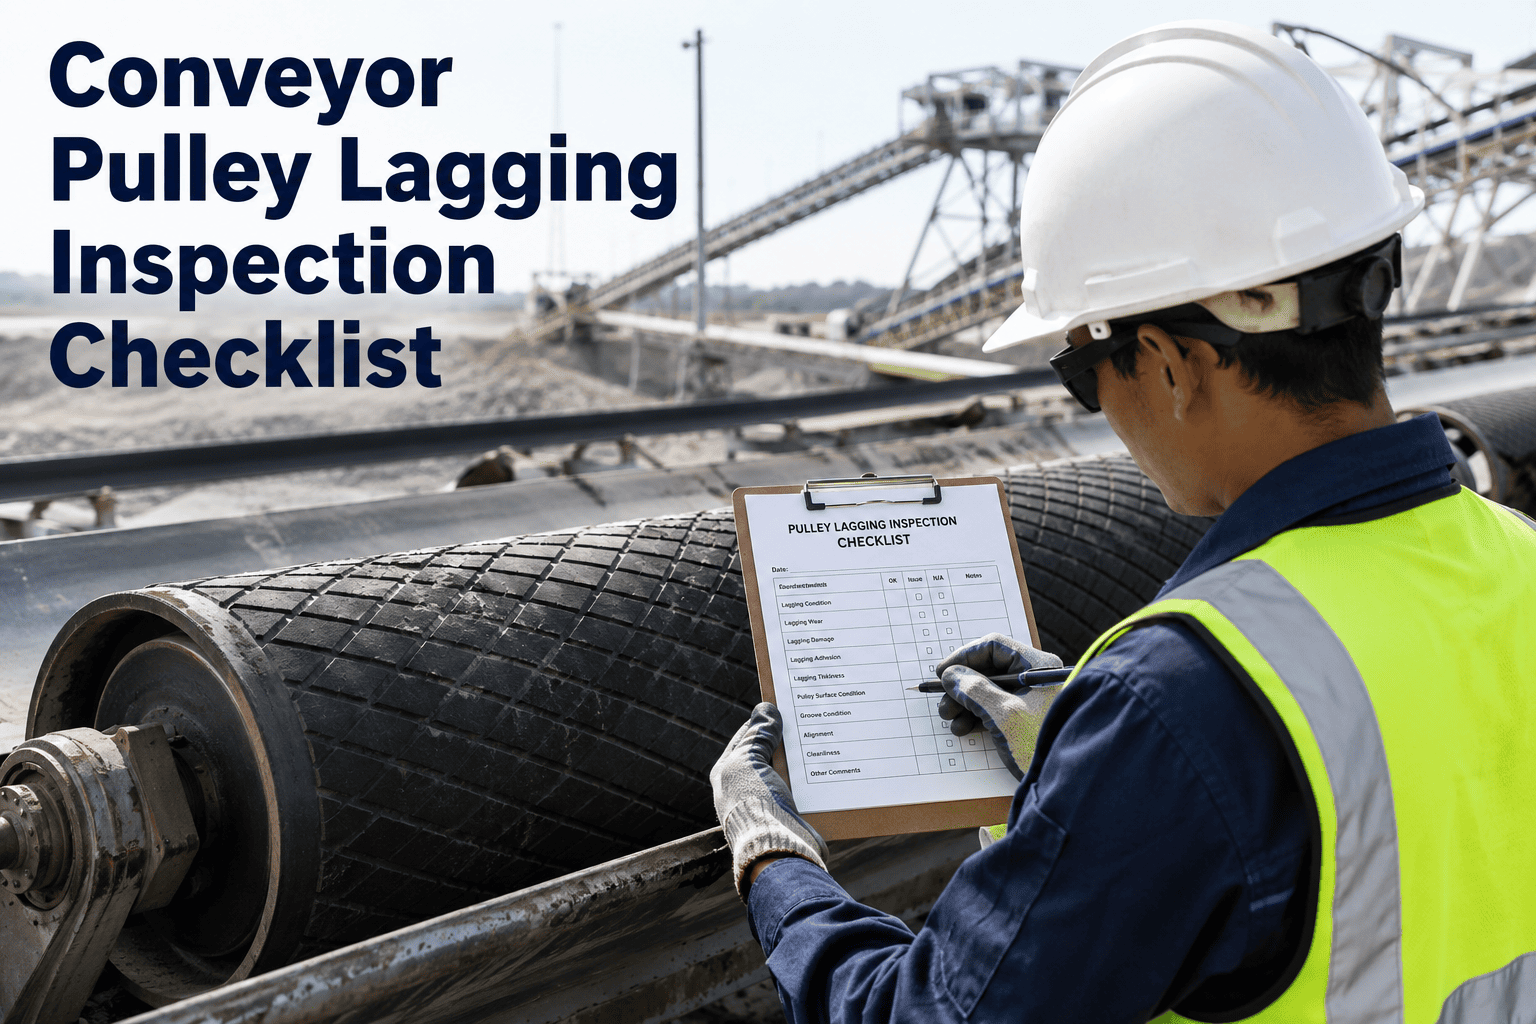
On a cement plant conveyor, the lagging is a thin protective skin bonded to the pulley shell — and when it fails, it rarely fails quietly. A drive pulley that loses its tread starts slipping, the belt begins to mistrack, edges fray, and a repair that could have been a scheduled lagging swap becomes an emergency belt-and-pulley replacement at four to five times the cost. Roughly three-quarters of failed pulleys fail because of wear, and nearly all of it is visible weeks before a shutdown. This checklist gives your crews an exact, tickable routine — safety, visual, measured, and wheel-interface — so glazing, gouging, delamination, and lost crown get caught early. Run it inside OxMaint Inspection Management and every checked item becomes a tracked work order instead of a note that gets lost.
Conveyor Pulley Lagging Inspection Checklist
A tick-by-tick lagging inspection for drive, head, tail, and bend pulleys — catch wear, glazing, and delamination before slippage takes the whole conveyor down.
Pre-Inspection Safety Checklist
Lagging inspection means working close to a pulley that must not move. Every item here is a lock before a look — clear all of them before anyone puts a hand near the shell.
Lagging Surface & Wear Checklist
This is the core of the round — the failure modes that end a pulley. Wipe and light each surface before you tick; a glazed pulley under a film of clinker dust reads as "fine" until the belt slips.
Crown, Alignment & Rotation Checklist
Even perfect lagging fails the belt if the pulley's shape or rotation is off. These checks catch the tracking and mechanical faults that wear lagging unevenly and mistrack the belt.
Score Each Pulley: Pass, Monitor, Act
A ticked item still needs a verdict. Sort every pulley into one band and let the band drive the work order — this is where the checklist turns into a plan.
Prioritize the Round by Pulley Type
Not all pulleys wear the same. Work them in priority order — drive pulleys carry the torque and glaze first; tail and bend pulleys collect material and gouge.
| Pulley | Priority | Watch For |
|---|---|---|
| Drive pulley | Highest | Glazing, delamination — highest torque and tension |
| Head pulley | High | Face gouging, one-sided wear from tracking drift |
| Tail pulley | Medium | Carryback buildup, uneven contact, hidden delamination |
| Bend & snub pulley | Medium | Material packing, localized wear on the dirty belt side |
Drive pulleys on cement lines are usually ceramic-lagged for the abrasion; give them the closest look and the tightest interval.
Why a Digital Checklist Wins
A clipboard checklist proves you looked; it doesn't prove you followed up. The gap between "inspected" and "fixed" is where lagging failures live. Running the round in OxMaint closes it.
What Reliability Leaders Say
The mistake I see everywhere is treating lagging as a consumable nobody watches until the belt slips. By then you're not swapping lagging — you're changing a belt and a pulley on an emergency callout. A structured checklist that names glazing and delamination, ticked and tracked per pulley, is the cheapest reliability spend in the plant.
Paper checklists told me a pulley was inspected. They never told me whether anyone acted on what they found. Once every failed item opened a work order automatically, our repeat lagging failures dropped and the audit stopped being a fire drill. The inspection finally connected to the fix.
Frequently Asked Questions
How often should this lagging checklist run?
For most cement plant conditions, run the full checklist every 6 to 12 months, with high-torque drive pulleys and hot clinker or kiln-feed lines inspected more often. Abrasive dust, moisture, and heat all shorten the interval, so the right cycle is the one your own wear history proves rather than a generic number. OxMaint schedules the round automatically and adjusts intervals from each pulley's tracked condition. Book a demo to set your inspection cadence.
Which checklist items mean replace the lagging now?
The Act-now triggers are delamination (lagging lifting off the shell), missing chunks or deep gouges, a glazed shiny surface that has lost its grip, and a lost crown profile that lets the belt mistrack. Any of these means the lagging is no longer doing its job and slippage or belt damage is close behind. Loose ceramic tiles and heat cracking are equally urgent on high-temperature lines. Start free to log findings against each pulley.
Why does lagging matter so much on cement conveyors?
Cement lines move abrasive limestone, clinker, and fine dust at volume, often with moisture and heat, which is the hardest possible environment for a pulley surface. Lagging provides the friction that stops the belt slipping and the barrier that stops the steel shell wearing out. When it fails you lose traction and expose the shell at the same time, turning a cheap re-lag into an expensive belt-and-pulley job. That is why a disciplined checklist pays for itself quickly. Book a demo to see it applied to your lines.
Can I run this checklist without shutting the conveyor down?
A proper hands-on lagging inspection requires the conveyor locked out and de-energized — you cannot safely judge tread, bond, or crown on a moving pulley. What you can do is reduce how often you open the machine by tracking condition trends, motor current, and slip indicators between rounds so you know which pulleys actually need a close look. OxMaint keeps that history in one place so planned access is targeted, not guesswork. Start free to build your pulley records.
How does a digital checklist help at an MSHA or OSHA review?
Because every inspection is timestamped, tied to a specific pulley, and stored with photos and the resulting work orders, the full trail is already assembled when a reviewer asks for it. Instead of hours reconstructing who inspected what and whether it was fixed, the records export in minutes. That same discipline that satisfies an auditor is what prevents the failure in the first place. Book a demo to see the export.
Turn Every Ticked Box Into a Tracked, Provable Result
OxMaint runs this lagging inspection as a scheduled digital checklist, opens work orders the moment a pulley fails an item, and keeps a per-pulley history that stops small wear from becoming an emergency belt change — inspection that actually connects to the fix.