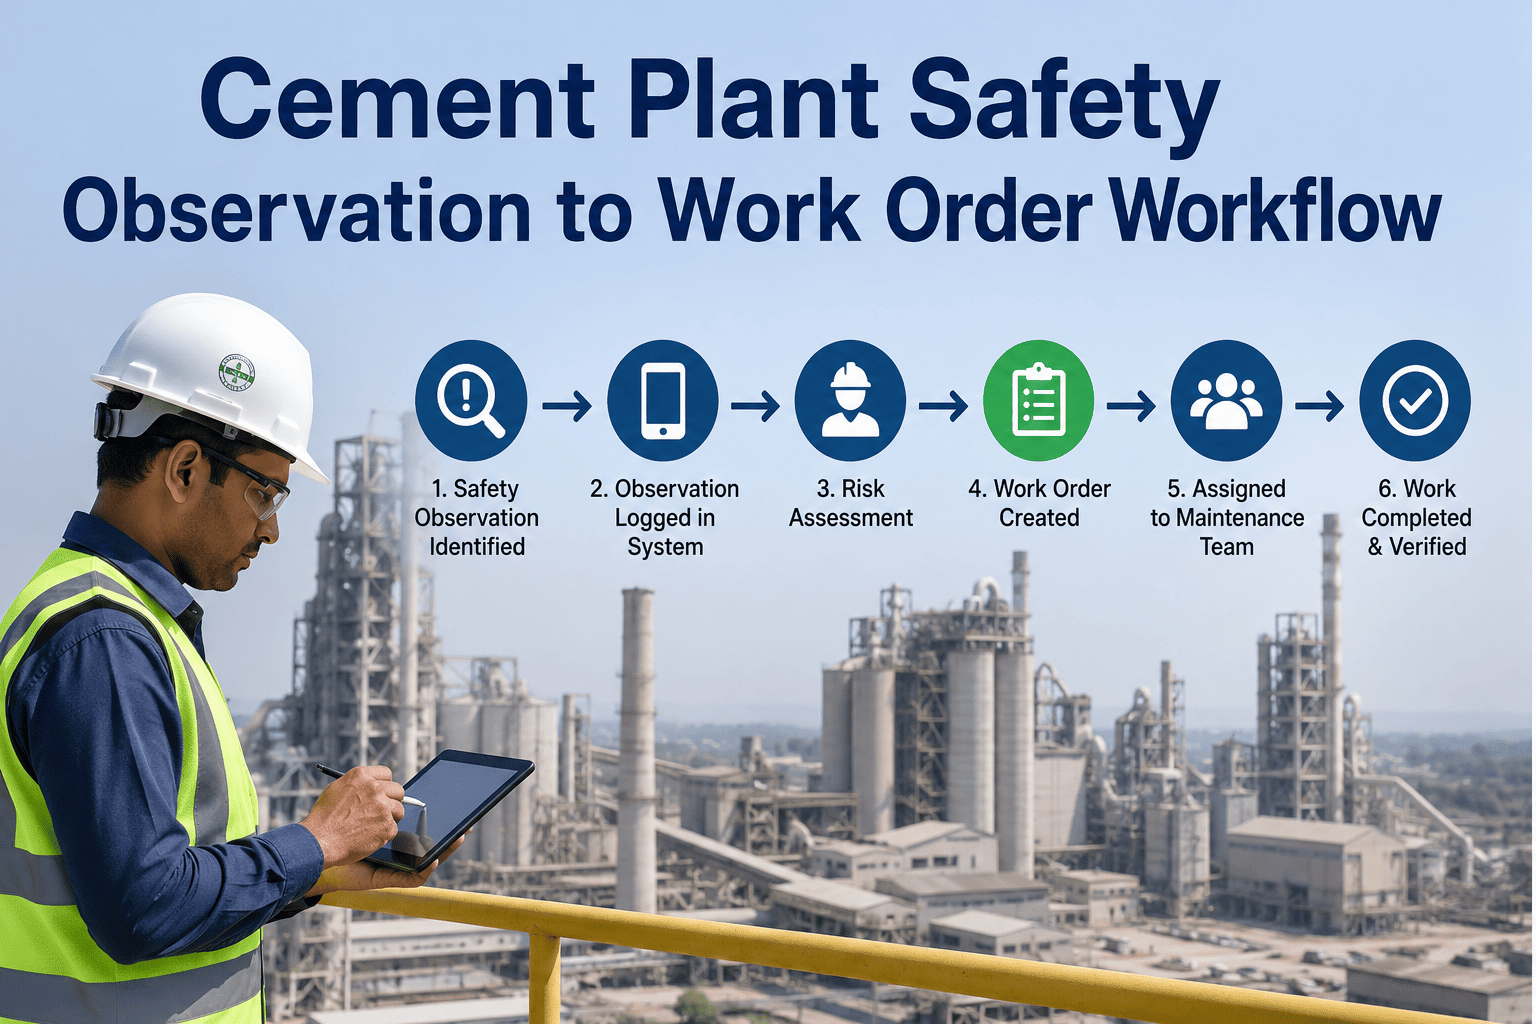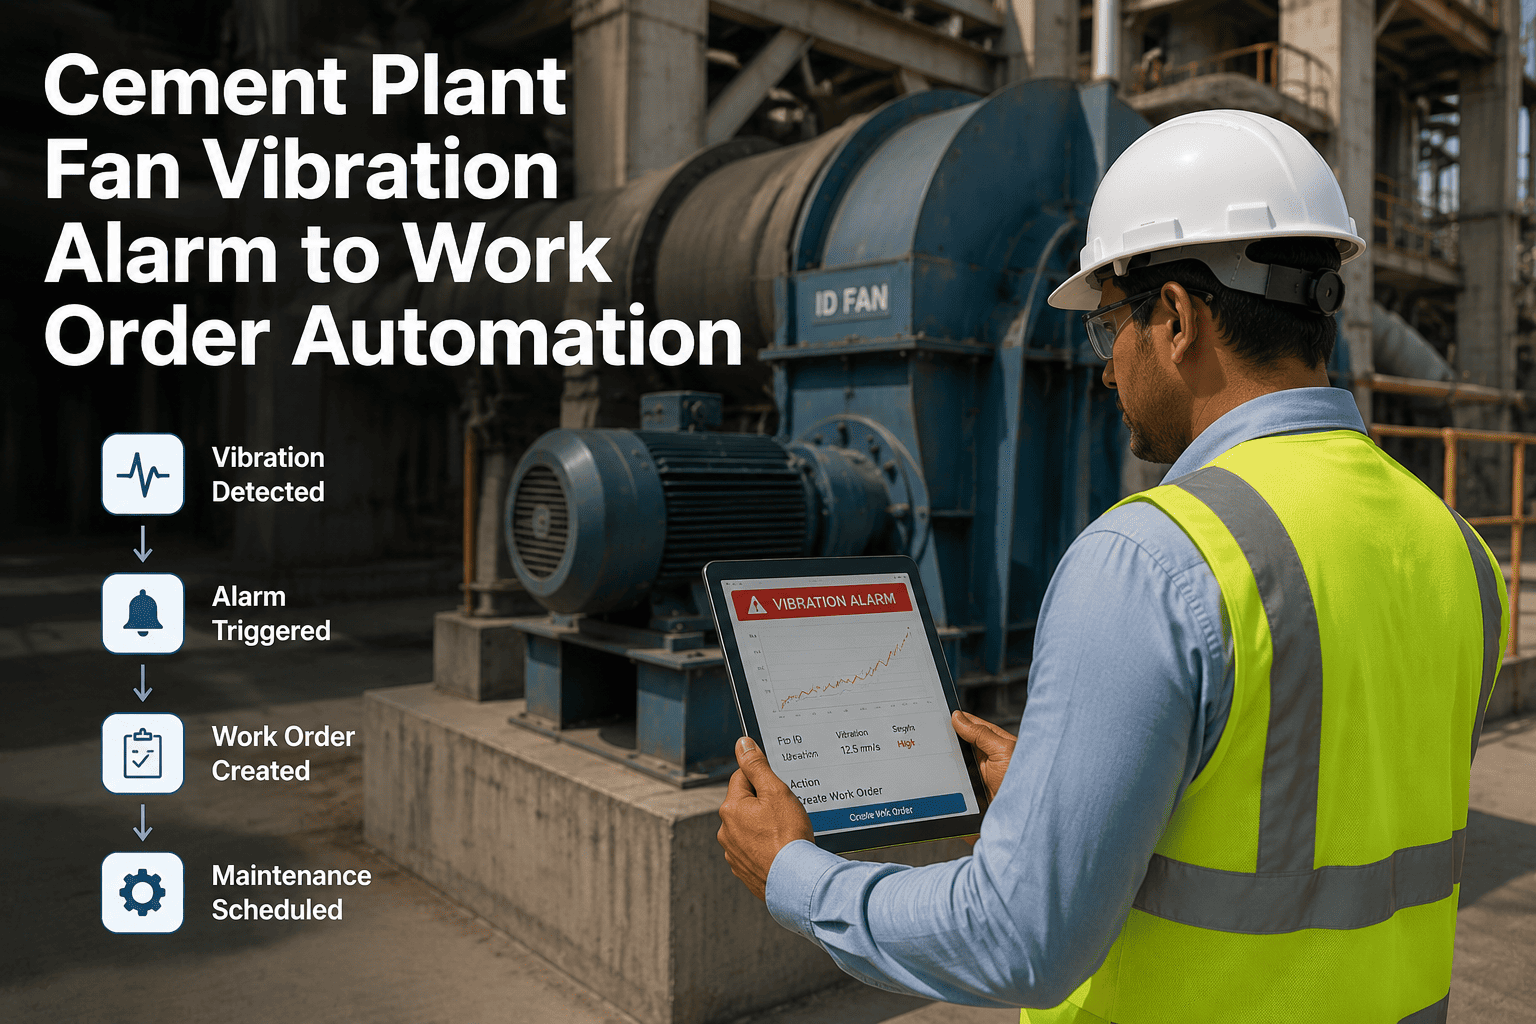
The first 72 hours after a cement plant restart are when a large proportion of shutdown maintenance failures surface — and they surface as unplanned stoppages, not as logged defects. A post-shutdown defect tracking workflow changes that outcome by treating start-up as an inspection phase, not just a production recovery phase. Every abnormal observation during commissioning becomes a work order before the observer walks away from the equipment. OxMaint's work order management makes this practical: mobile capture, automatic assignment to the responsible discipline, and real-time visibility for the shutdown coordinator so nothing falls through the shift boundary. This blog walks through why start-up defect tracking matters, how to structure the workflow, and what the handover checklist should capture at each system. Start free on OxMaint or book a demo to see how the workflow runs across your next planned shutdown.
Post-Shutdown Start-Up Defect Tracking Workflow
How to capture, assign, and resolve every defect surfaced during cement plant restart — before it becomes an unplanned stoppage that erases the maintenance work done during the shutdown.
Why Post-Shutdown Start-Up Creates a Defect Backlog
Shutdown maintenance is planned in detail. Start-up is often treated as a single event — flick the switch and watch the numbers. The reality is that restart is the highest-stress period for every system the shutdown touched, and it reveals defects that no pre-start inspection can find: misalignments that only show under load, connections that seat correctly cold but weep under process temperature, and clearances that were set correctly but not verified after final assembly. Without a formal defect capture workflow, every observation made during start-up commissioning lives in a technician's notebook, a verbal handover, or nowhere at all.
Post-Shutdown Start-Up Defect Tracking: Phase by Phase
The workflow has four distinct phases aligned to the start-up sequence. Each phase has a defined owner, a capture method, and a handover gate before the next phase begins. OxMaint runs each phase as a set of work order templates that activate when the shutdown coordinator moves the shutdown project to the start-up stage.
Discipline teams complete final commissioning inspections against OxMaint work order checklists — mechanical, electrical, instrumentation, and process each have their own template. All observations are logged as work order findings. Any item marked as a start-up blocker prevents the gate from clearing until it is resolved or formally accepted with a documented risk acknowledgment from the shutdown coordinator.
As systems come on load for the first time, roving observation rounds capture abnormal conditions. Each discipline assigns a walking technician whose only role during this window is observation and capture — not troubleshooting. Every observation goes into OxMaint as a work order, even if it appears minor. Priority is assigned at capture: P1 (stop immediately), P2 (resolve within 2 hours), P3 (resolve within the shift), P4 (schedule within 48 hours).
At every shift boundary during the first 72 hours, the outgoing coordinator runs the OxMaint defect dashboard with the incoming supervisor — live, on a screen. Every open defect is reviewed for status: resolved, in progress with a current owner, or overdue and needing escalation. The handover is documented as a work order comment so the record of what was communicated and to whom is preserved in the system, not just in someone's head.
At 72 hours post-start-up, the shutdown coordinator pulls the OxMaint start-up defect report: all defects captured, sorted by priority and resolution status. Every P1 and P2 must be closed. P3 closures are reviewed for completion quality. Open P4 items are converted to standard planned maintenance work orders and enter the regular schedule. The close-out report becomes the first document in the next shutdown's planning file — what failed at start-up informs what gets extra attention in the next preparation scope.
Never Lose a Start-Up Observation to a Verbal Handover Again
OxMaint gives every technician a mobile work order to capture defects in real time — logged, prioritized, assigned, and visible to the shutdown coordinator before they walk to the next system.
Start-Up Defect Capture Checklist by Discipline
These are the observation categories that each discipline team covers during first fire-up. Every item that does not pass becomes a work order before the team moves to the next system.
How to Triage Start-Up Defects in the First 4 Hours
| Priority | Definition | Response | Max Resolution Time | Example |
|---|---|---|---|---|
| P1 | Imminent safety hazard or equipment damage risk if operation continues | Stop affected system immediately; notify shutdown coordinator | Before restart | Gearbox temperature rising 15°C above normal after 30 minutes |
| P2 | Defect will escalate to P1 without intervention within 2–4 hours of operation | Assign technician immediately; assess while system continues running | 2 hours | Drive belt showing abnormal lateral drift at start-up tension |
| P3 | Defect is present but not escalating; will become P2 if unaddressed beyond the shift | Assign with current shift technician; resolve before shift end | End of shift | Minor oil weep at gearbox seal — not increasing rate |
| P4 | Observation noted; no immediate risk; should be addressed within 48 hours | Log and assign; convert to planned work order if not resolved at 72-hour review | 48 hours | Nameplate missing from motor; gasket cover slightly misaligned but sealed |
Frequently Asked Questions
Why do so many defects appear at start-up rather than during the shutdown itself?
Shutdown maintenance occurs under static conditions — equipment cold, no load, no process media. Many defects are only detectable under operating conditions: seal leaks that only appear at process temperature and pressure, misalignments that only manifest as vibration under motor load, and clearances that appear correct at assembly but change as components reach thermal equilibrium. This is why pre-start inspections, however thorough, cannot replace a structured observation protocol during the first hours of operation. The start-up phase is, in effect, the final quality check on every piece of work done during the shutdown — and it needs to be treated with the same rigor as the shutdown execution itself. Start free to set up your start-up observation work orders.
How should we handle a defect that is discovered but cannot be resolved before production restart?
Every unresolved defect at the time of restart must have three things before production begins: a named responsible technician, a resolution timeline, and a risk acknowledgment from the shutdown coordinator or site manager. In OxMaint, this is logged as a work order with a risk-accepted flag and a mandatory escalation if the resolution timeline is missed. This is not a workaround for poor maintenance practice — it is a formal risk management process that makes the acceptance decision explicit and auditable. The worst outcome is an undocumented verbal decision that accepts a risk no one can later identify who sanctioned. Book a demo to see the risk acceptance workflow.
What is the right observation period for post-shutdown monitoring?
The first 72 hours is the minimum structured observation window for most cement plant restarts. Within this window, the most common failure modes — thermal leaks, misalignment-driven vibration, and lubrication deficiencies — will have manifested if they are going to. For major shutdowns involving kiln refractory, drive train overhaul, or heat exchanger replacement, extending structured observation to 120 hours is prudent, particularly for the systems most directly affected by the shutdown work. The key principle is that structured observation — documented, with named observers and required capture of all anomalies — should not end before the most critical systems have completed at least two full load cycles. Start free to configure your observation window.
How does OxMaint help the shutdown coordinator manage defects across multiple disciplines in real time?
The shutdown coordinator sees a single dashboard that aggregates all open defects from all disciplines, sorted by priority and updated in real time as technicians log and close work orders from the floor. This eliminates the need for the coordinator to chase verbal updates from four or five discipline leads simultaneously while also managing process conditions. When a P1 or P2 defect is logged anywhere on site, the coordinator receives an automatic notification before the technician who logged it has moved to the next system. The dashboard also shows which defects are approaching their resolution deadline without a status update — a signal to escalate before the timeline is missed rather than after. Book a demo to see the coordinator dashboard.
How does the 72-hour close-out review improve the next shutdown?
The close-out report shows every defect that surfaced at start-up, sorted by system and type. Patterns in that data — multiple defects on the same system, repeated failure modes across shutdowns, or specific contractors whose work generates disproportionate start-up defects — are immediately visible when the data is aggregated across two or three shutdown cycles. OxMaint retains each close-out report linked to the shutdown project, so the planner preparing the next shutdown can pull the prior start-up defect history for each system and add targeted inspection or quality verification steps to the shutdown scope. This is the mechanism by which a structured start-up workflow produces continuous improvement in shutdown quality, not just in start-up performance. Start free to start building your shutdown history database.
Make Start-Up as Structured as the Shutdown That Preceded It
OxMaint gives every cement plant restart team a real-time defect capture workflow — mobile work orders, automatic priority escalation, shift handover documentation, and a 72-hour close-out report that feeds the next shutdown's planning scope.