A stockout rarely looks like a single failure. A customer sees a canceled order, a picker walks to an empty slot, a planner expedites freight, and the warehouse absorbs the cost of all three. Safety stock is the buffer meant to prevent that, yet many teams still set it with a flat rule such as two weeks of cover on every item. This guide explains how to size safety stock from real variability, where maintenance downtime quietly erodes availability, and how Oxmaint supports the equipment side of fulfillment reliability.
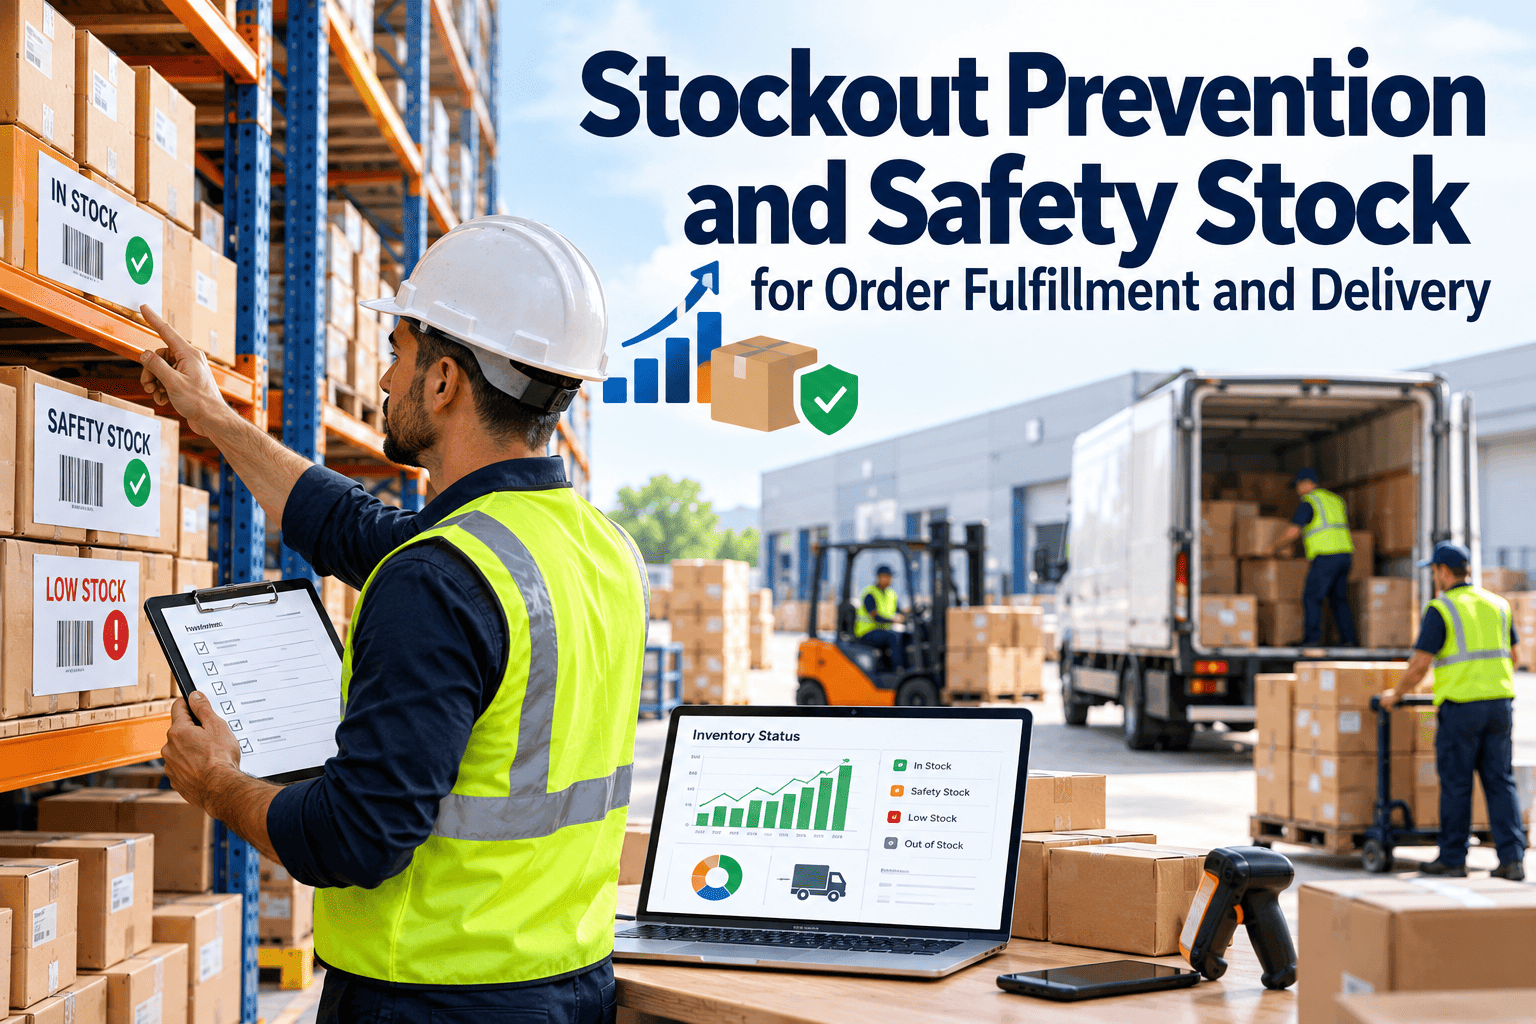
Stockout Prevention and Safety Stock for Order Fulfillment and Delivery
What a Stockout Really Costs
Many teams only count the first link. Pricing the whole chain justifies a more careful approach to buffers.
Why Safety Stock Rules of Thumb Fail
- A flat weeks-of-cover rule over-protects stable items and under-protects volatile ones.
- Supplier lead times change, but static settings stay the same for years.
- Promotions, seasonality, and new products distort demand history.
- Planners override system values after a stockout and rarely lower them afterward.
- No one connects service level targets to the inventory investment required.
The two sources of uncertainty
Safety stock exists to cover uncertainty in demand and uncertainty in replenishment lead time. Both must be measured separately before they are combined.
The Core Safety Stock Calculation
| Target cycle service level | Approximate z value | What it means |
|---|---|---|
| 90% | 1.28 | Roughly 1 replenishment cycle in 10 ends in a stockout |
| 95% | 1.65 | Roughly 1 cycle in 20 ends in a stockout |
| 97.5% | 1.96 | Roughly 1 cycle in 40 ends in a stockout |
| 99% | 2.33 | Roughly 1 cycle in 100 ends in a stockout |
Demand Variability: Getting the Inputs Right
- Measure forecast error rather than raw demand variation when a forecast drives replenishment.
- Use weekly or daily buckets that match your replenishment cycle.
- Remove one-time events such as a large one-off order before calculating variation, and track them separately.
- Treat intermittent demand differently, because standard formulas assume demand is reasonably continuous.
- Recalculate regularly, since demand patterns shift.
Lead Time Variability: The Overlooked Half
- Production delays and allocation limits.
- Transit variability and port or carrier delays.
- Order batching and minimum order quantities.
- Quality holds and rejected shipments.
- Receiving and put-away backlogs.
- Equipment downtime in dock, conveyor, and sortation areas.
- Labor shortages during peak periods.
- Inventory record errors that hide real availability.
Internal lead time counts. Stock that is physically received but not yet available to pick still behaves like a stockout.
Segment Before You Set Targets
Different items deserve different service levels
Setting one service level for the entire catalog wastes working capital on slow, low-impact items while leaving critical ones exposed.
A Stockout Prevention Workflow
Stockout Root Causes That Safety Stock Cannot Fix
| Root cause | Why a larger buffer does not solve it | Better response |
|---|---|---|
| Inaccurate inventory records | System shows stock that is not there | Cycle counting and location discipline |
| Slow receiving and put-away | Stock exists but cannot be picked | Dock scheduling and equipment reliability |
| Poor forecast inputs | Buffer is sized on bad history | Improve forecasts and flag promotions |
| Supplier unreliability | Lead time swings are too wide to buffer cheaply | Supplier performance management or alternatives |
| Unplanned equipment downtime | Throughput drops, so effective lead time grows | Preventive and condition-based maintenance |
Where Maintenance Meets Availability
- A dock leveler, conveyor, or sorter that stops during a receiving wave delays put-away and extends internal lead time.
- Forklift or reach-truck failures slow replenishment to pick faces, creating local stockouts even when inventory exists in the building.
- Packing and labeling equipment faults delay orders, which looks like a supply failure to the customer.
- Missing spare parts can turn a short repair into a long outage, so critical spares need their own stock policy.
- Delivery vehicle breakdowns delay replenishment to stores or customers, which can trigger downstream stockouts.
Apply safety stock thinking to spare parts
Critical maintenance spares can be classified by impact and lead time, just like sellable inventory. A belt or sensor with a long lead time and a high downtime cost deserves a deliberate buffer.
Metrics That Keep Availability Honest
How Oxmaint Supports Fulfillment Reliability
Oxmaint is maintenance management software. It does not forecast demand or set safety stock levels, but it protects the equipment that makes stock available.
- Preventive maintenance schedules for conveyors, sorters, dock equipment, forklifts, and packing lines.
- Work orders that prioritize repairs affecting receiving, put-away, and outbound flow.
- Asset history and downtime reports that show which equipment threatens throughput.
- Inventory management for spare parts, with reorder points and usage history.
- Mobile inspections so defects are logged at the point of work.
- Vehicle maintenance records that support reliable replenishment and delivery.
Worked Example: Sizing a Buffer Step by Step
Balancing Availability Against Carrying Cost
- Higher service levels raise safety stock at an increasing rate, so the last few percentage points cost the most.
- Carrying cost includes capital, storage space, handling, shrink, damage, and obsolescence.
- Space constraints can turn buffers into slotting problems, which hurts pick efficiency.
- Perishable or short-life items need smaller buffers and tighter replenishment cycles.
- Cheap items with high customer impact often justify larger buffers than their cost suggests.
Reduce variability before adding stock
Every reduction in lead time or demand variation lowers the buffer you need. Supplier agreements, faster receiving, and reliable equipment are often cheaper than carrying more inventory.
Ways to Reduce the Buffer You Need
| Lever | What it changes | Example action |
|---|---|---|
| Shorter lead time | Less demand exposure per cycle | Negotiate faster replenishment or closer sourcing |
| More reliable lead time | Lower lead time variance | Track supplier on-time performance and escalate repeat misses |
| Better forecasts | Lower forecast error | Share promotion calendars with planners |
| Faster receiving | Shorter internal lead time | Dock scheduling and reliable receiving equipment |
| Accurate records | Fewer phantom inventory events | Cycle counts targeted to fast movers |
| Pooling stock | Combines variability across locations | Centralize slow movers and hold fast movers locally |
Early Warning Signals for Stockout Risk
- Sales running above forecast for several periods in a row.
- Supplier confirmations slipping or partial shipments appearing.
- Receiving backlogs growing at the dock.
- Pick face replenishment tasks arriving late.
- Rising inventory adjustments on the same items.
- Repeated equipment faults in receiving or put-away zones.
Cross-Functional Ownership
- Own service level targets and parameters.
- Monitor supplier performance and lead time drift.
- Review exceptions and approve buffer changes.
- Keep receiving and put-away fast and predictable.
- Prevent equipment faults that extend internal lead time.
- Report recurring bottlenecks with downtime data.
Common Mistakes in Safety Stock Programs
- Using the same service level for every item.
- Calculating variability from stale or unadjusted history.
- Ignoring internal receiving delays when measuring lead time.
- Raising buffers after every stockout without checking the cause.
- Leaving obsolete or slow items with buffers set for past demand.
- Treating critical spare parts as an afterthought.
A 60-Day Starting Plan
Peak Season and Promotion Planning
Using Exception Reports Instead of Constant Review
- Flag items where on-hand plus on-order falls below the reorder point.
- Flag items where actual lead times exceed the planned value for several receipts.
- Flag items with large forecast misses over recent periods.
- Flag items with repeated adjustments or pick shorts.
- Review the flagged list in a short weekly meeting that includes warehouse and maintenance input.
Close the loop on every stockout
Record the cause, the cost, and the corrective action for each significant stockout. After a few months, the pattern shows whether the answer is more stock, a better supplier, faster receiving, or more reliable equipment.
Data Hygiene Checklist for Reliable Safety Stock
| Data element | Common problem | Fix |
|---|---|---|
| Demand history | Includes stockout periods, so true demand is understated | Adjust for lost sales and flag out-of-stock days |
| Lead time records | Uses order date to ship date, ignoring receipt and put-away | Measure to the point stock is pickable |
| Unit of measure | Mixed cases, eaches, and pallets across systems | Standardize conversions in the item master |
| Item status | Discontinued items still carry buffers | Review slow and obsolete items quarterly |
| Equipment downtime log | Outages recorded informally or not at all | Log downtime in a maintenance system with reasons and duration |
Questions to Ask in Your Next Inventory Review
- Which stockouts last quarter were caused by supply, which by forecasts, and which by internal flow?
- Which items hold large buffers but have not sold in months?
- Where did equipment downtime delay receiving, replenishment, or packing?
- Which critical spare parts have no stock policy at all?
- Who owns the decision to raise or lower a buffer, and how is the change recorded?
- Which service level targets were set years ago and never revisited?