Electrical failures are the second-largest cause of unplanned downtime in FMCG plants after mechanical breakdowns — and unlike most mechanical failures, they often give no warning before they occur. A motor winding that fails due to insulation breakdown, a panel bus bar that overheats due to a loose connection, or a VFD that trips on overtemperature because its cooling fins have never been cleaned: none of these announce themselves until the failure happens. The only defence is a structured electrical PM programme that tests insulation, inspects connections, monitors temperature, and catches degradation before it becomes a production event. This checklist covers every electrical and motor maintenance task in an FMCG plant — from daily panel visual checks to annual thermographic surveys and motor insulation testing — structured for deployment in OxMaint to auto-schedule every task and retain the compliance records required for insurance, statutory inspection, and electrical safety audits.
1. Electrical Panels and Distribution
Most electrical panel failures in food plants are caused by conditions that were visible and measurable weeks before the failure — loose terminations generating heat, moisture ingress creating tracking paths, and overcrowded panels with no ventilation. A monthly visual inspection and an annual thermographic scan together catch the vast majority of developing faults before they become unplanned outages.
2. Motor Condition Monitoring
Motor failures account for the majority of unplanned electrical downtime in FMCG plants. Bearing failure from inadequate lubrication, winding failure from contamination ingress, and overheating from blocked cooling passages are all detectable well in advance — but only if condition monitoring is performed consistently at the correct intervals.
3. Insulation Resistance Testing
Insulation resistance testing (Megger testing) is the only way to detect winding insulation degradation before it becomes a winding failure. A motor that meggers at 100 MΩ is in excellent condition. The same motor at 1 MΩ is approaching failure. At 0.1 MΩ it will fail under load within weeks. Testing costs 20 minutes per motor. A failed winding costs 3–10× the motor purchase price in rewind labour, lost production, and parts.
4. Variable Frequency Drives and Soft Starters
VFDs are the most failure-prone component in a modern electrical system — not because they are unreliable, but because they are almost never maintained. Blocked cooling fans, capacitor degradation, dirty heatsinks, and loose DC bus connections are the four most common VFD failure modes, and all four are preventable with a quarterly maintenance routine.
5. Thermographic Survey
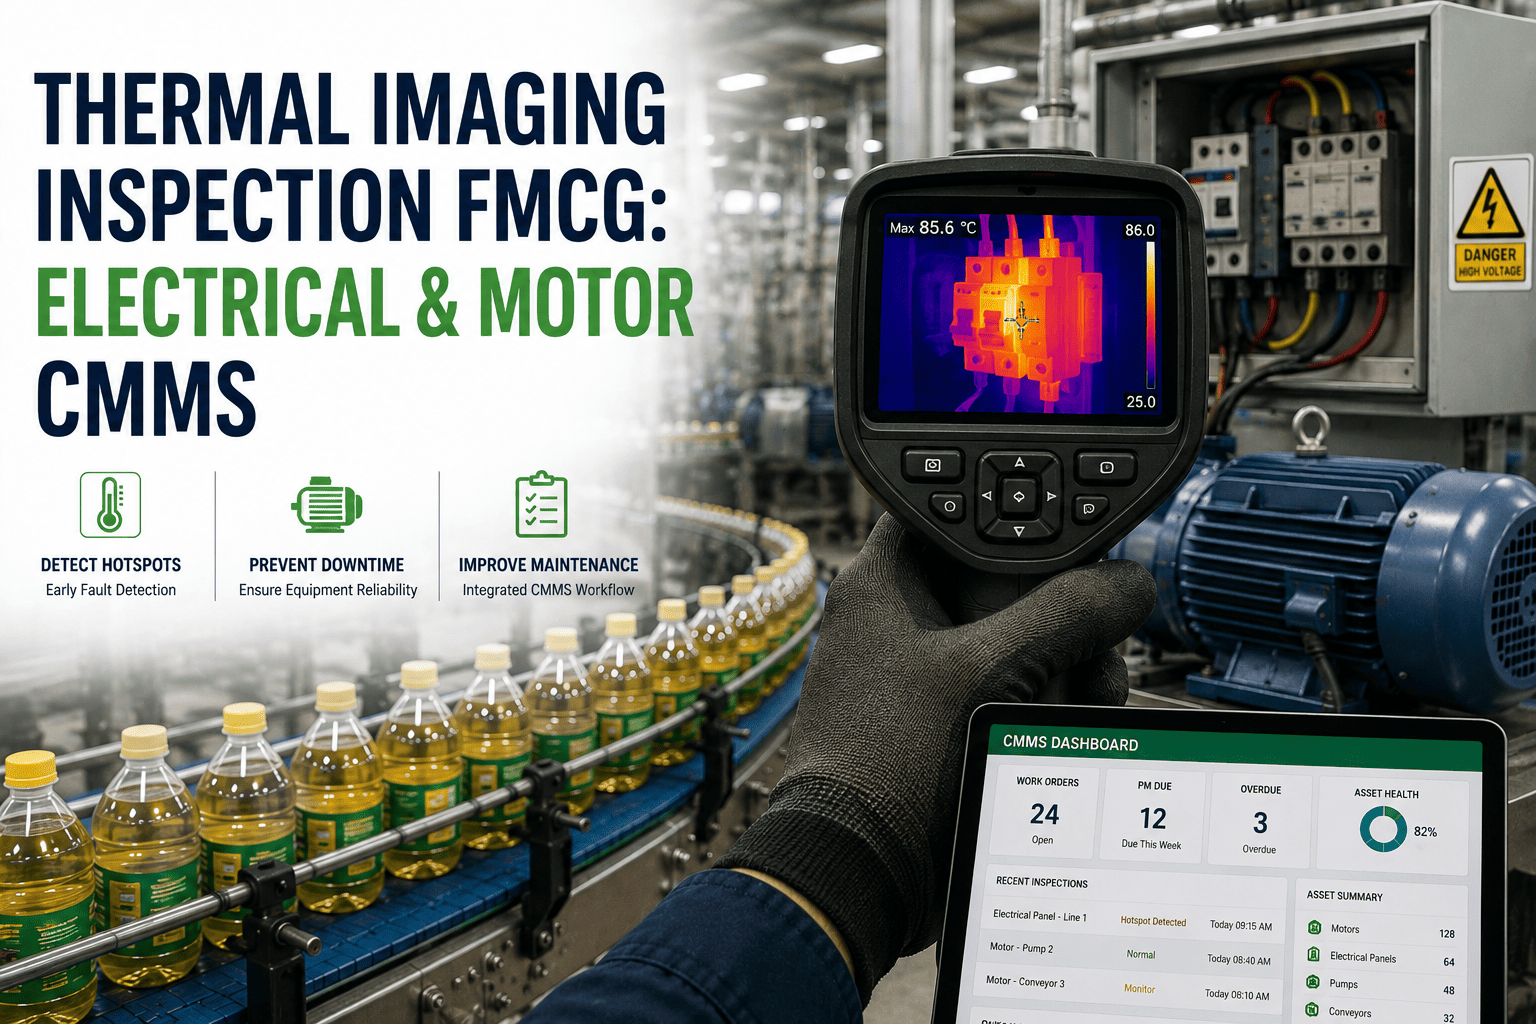
Thermographic (infrared) surveys of electrical systems are the most cost-effective maintenance activity available for detecting developing electrical faults. A qualified thermographer with a calibrated camera can survey an entire plant electrical system in a day and identify every hot spot above threshold — loose connections, overloaded circuits, phase imbalances, and failing components — all while the plant is running at full production load.
6. Statutory Compliance and Electrical Safety
Electrical compliance in FMCG plants covers both statutory requirements (periodic inspection and testing under NFPA 70B, BS 7671, or local equivalent) and food safety requirements (IP ratings, GFCI protection, and panel security in food production areas). Both must be documented and both must be current.