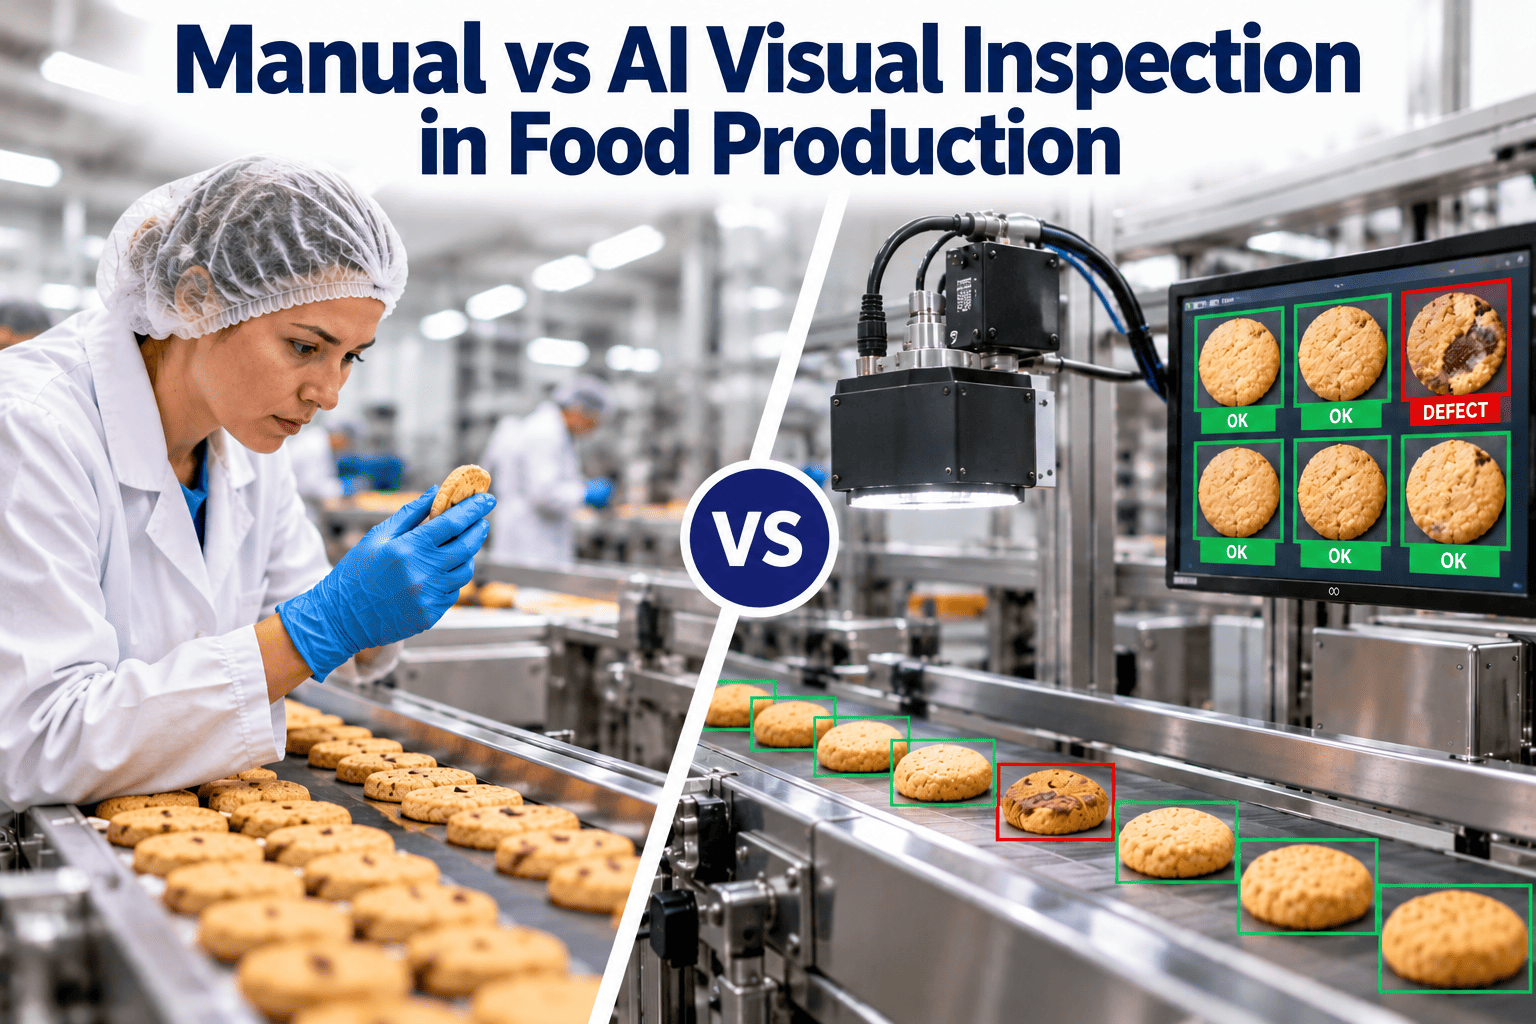
Every food plant relies on someone or something to decide whether product looks right before it ships. For decades that was a trained person at a conveyor; today it can also be a camera and a trained model. Neither option is simply better, because accuracy, speed, fatigue, and cost behave differently in each. This guide compares both methods honestly, shows where a hybrid approach performs best, and explains how to keep either one under control. Plants that want inspection tasks and equipment checks tracked together can organize them in Oxmaint.
Manual vs AI Visual Inspection in Food Production: Which Catches More, and When?
Compare human and machine inspection on accuracy, speed, fatigue, and cost, then decide where each one belongs on your line.
Why the Comparison Matters Now
Customers, retailers, and auditors expect documented control of visual defects and foreign material. Labour availability, line speeds, and complaint costs push plants to ask whether inspection can be more consistent.
- Visual defects drive complaints, downgrades, and rework
- Manual inspection results are rarely recorded in a usable form
- Machine vision has become more accessible, but it still needs data and upkeep
- Poorly chosen inspection methods add cost without reducing risk
Head-to-Head: Eight Factors Compared
| Factor | Manual Inspection | AI Visual Inspection |
|---|---|---|
| Consistency | Varies between people, shifts, and times of day | Applies the same rules to each image |
| Fatigue | Attention drops during repetitive, long tasks | Not affected by fatigue, but affected by dirty optics and drift |
| Speed | Limited by human viewing time per item | Matches line speed when hardware is sized correctly |
| New defect types | Inspectors can recognise something unusual immediately | May miss defects it was never trained or configured to see |
| Subtle colour | Influenced by lighting and individual perception | Measures colour consistently under controlled light |
| Records | Often limited to tick sheets and rejection counts | Stores images and results for traceability |
| Setup effort | Training and clear reference samples | Hardware, data collection, labelling, and validation |
| Ongoing cost | Wages, training, and turnover | Maintenance, retraining, support, and spare parts |
Where Manual Inspection Falls Short
Where AI Inspection Falls Short
Choosing by Defect Type
The best method depends on what you are trying to catch. Use this guide as a starting point, then validate against your own product.
| Defect Category | Better Suited To | Reason |
|---|---|---|
| Size, shape, count | AI or rule-based vision | Measurable and repetitive |
| Colour and browning | AI vision under fixed lighting | Consistent measurement beats perception |
| Unusual or unexpected items | Human review, supported by cameras | Context and judgement matter |
| Texture and smell | Human sensory evaluation | Not captured by a camera |
| Seal and label faults | AI or vision with rules | High volume and clear criteria |
Track Inspections and Equipment Checks in One Place
Whether your inspectors or your cameras do the looking, Oxmaint keeps schedules, checklists, and corrective actions organized.
The Hybrid Model That Works for Most Plants
Most plants get the best result by combining both. The machine handles volume and consistency, and people handle judgement and exceptions.
Benefits of the Hybrid Approach
- Inspectors focus on exceptions instead of staring at every unit
- Human corrections improve the model over time
- Inspection records cover the whole run, not samples only
- Manual checks continue as a verification layer against drift
Cost: What to Include in a Fair Comparison
Compare total cost over several years, not the purchase price. List every cost on both sides before deciding.
Manual Inspection Costs
- Wages and shift coverage
- Training and refresher sessions
- Turnover and onboarding
- Complaints from missed defects
- Waste from inconsistent rejection
AI Inspection Costs
- Cameras, lighting, and rejectors
- Integration with line controls
- Data labelling and validation
- Maintenance and spare parts
- Retraining when products change
Keeping Either Method Under Control
How Oxmaint Supports the Inspection Workflow
- Asset records for cameras, lights, sensors, and conveyors
- Preventive maintenance schedules for cleaning and function tests
- Mobile inspection checklists with pass or fail results
- Work orders for failed checks, with owners and due dates
- Reports that show recurring faults and completion history
Metrics to Compare Both Methods
Frequently Asked Questions
Is AI inspection more accurate than people?
Will AI remove the need for inspectors?
How do I measure inspector accuracy?
What breaks vision accuracy most often?
Where should a plant start?
What Accuracy Really Means in Inspection
Claims about accuracy are meaningless without a clear definition. Use the same terms to evaluate people and machines.
- Both sensitivity and specificity must be measured, because improving one often harms the other
- Test on samples that include borderline cases, not only obvious good and bad items
- Repeat the test regularly, because performance changes with fatigue, drift, and product variation
How to Run a Fair Side-by-Side Pilot
A pilot should answer a specific question: does this method reduce escapes or waste on our product at our line speed?
Pilot Design Tips
- Include multiple shifts and several inspectors, not only your best performer
- Seed known defects into the flow in a controlled way, with quality approval
- Record the reason for each disagreement, such as unclear standard, poor image, or human miss
- Decide success criteria before starting so results are not judged after the fact
Human Factors That Affect Manual Inspection
Manual inspection can be improved significantly with good work design. Many weaknesses attributed to people are really weaknesses in the setup.
Practical Improvements
- Provide consistent, glare-free lighting at the inspection station
- Rotate inspectors on a defined schedule to reduce monotony
- Build visual standards with photographs of acceptable, marginal, and rejected product
- Keep belt speed and product spacing within a range that allows reasonable viewing time
- Give inspectors clear authority to stop the line when they see a serious problem
Training and Verification
- Train new inspectors against the same reference set used for the machine
- Test inspectors periodically with known samples and record the results
- Share feedback, so inspectors see how their calls compare to the standard
- Refresh training when specifications or customers change requirements
Choosing the Method by Line Profile
| Line Profile | Suggested Starting Point | Watch For |
|---|---|---|
| Low speed, many product changes | Manual inspection with strong visual standards | Fatigue and inconsistent grading |
| High speed, few products | AI or machine vision with human verification | Drift and retraining after product changes |
| High risk of foreign material | Layered detection with dedicated equipment, plus visual checks | Over-reliance on one method |
| Premium appearance requirements | Hybrid, with machine grading and human final review | Subjective disagreements about grade |
| Seasonal or variable raw material | Human review supported by flexible vision rules | Model accuracy changing across seasons |
Common Objections and Honest Answers
Fallback and Contingency Planning
Every automated control needs a documented plan for the day it is unavailable.
- Define when the line may run with manual inspection only, and who approves it
- Increase sampling frequency while the system is offline
- Record the downtime period and the product made during it
- Verify the system with reference samples before returning to automatic control
- Review the root cause through a maintenance work order so the failure does not repeat
Data and Traceability: The Overlooked Difference
One of the biggest practical differences between the methods is what each leaves behind after the shift ends.
Manual Records Typically Show
- Tick sheets and hourly checks
- Rejected quantities by shift
- Handwritten comments
- Limited detail on the defect type
AI Records Can Show
- Image evidence for each rejection
- Defect type and time stamp
- Trends by product, line, and shift
- Results that can be reviewed later
Why This Matters During a Complaint
- Image records help show what the product looked like when it left the line
- Trend data helps identify when a problem began
- Reviewers can check whether a defect was seen and rejected or never detected
- Findings feed root cause analysis and corrective action instead of staying anecdotal
Food Safety Versus Appearance: Know What You Are Inspecting
Visual inspection serves two different purposes, and the standard for each is different.
- Do not rely on visual inspection alone for hazards that cannot be seen on the surface
- Use dedicated detection equipment such as metal detectors or X-ray for foreign material inside product
- Define which findings stop the line and which only trigger a grade change
- Document the role of visual inspection in your food safety plan so expectations are clear
A Staged Adoption Path
Few plants jump straight from manual to fully automated inspection. A staged path reduces risk and builds trust.
Maintenance Tasks Both Methods Depend On
Neither method works well on a poorly maintained line. Inspection quality is tied to equipment condition.
- Conveyor tracking and speed stability so product arrives consistently
- Oven and proofer performance, since inconsistent baking creates defects that inspection must then catch
- Lighting at manual stations and on cameras, including replacement before output fades
- Rejector and diverter function, including air supply and mechanical wear
- Sensors and encoders that time cameras and rejection
Using Work Orders to Close the Loop
- Raise a corrective work order whenever inspection shows a recurring equipment-related defect
- Assign it to the correct asset so history builds up
- Review defect trends after repair to confirm improvement
A Simple Decision Checklist
- Answer each question with evidence from your own line
- Involve quality, production, and maintenance in the decision
- Review the decision after six months of results
Build an Inspection Process You Can Prove
Connect inspection tasks, equipment care, and corrective actions so every method on your line stays reliable and documented.


