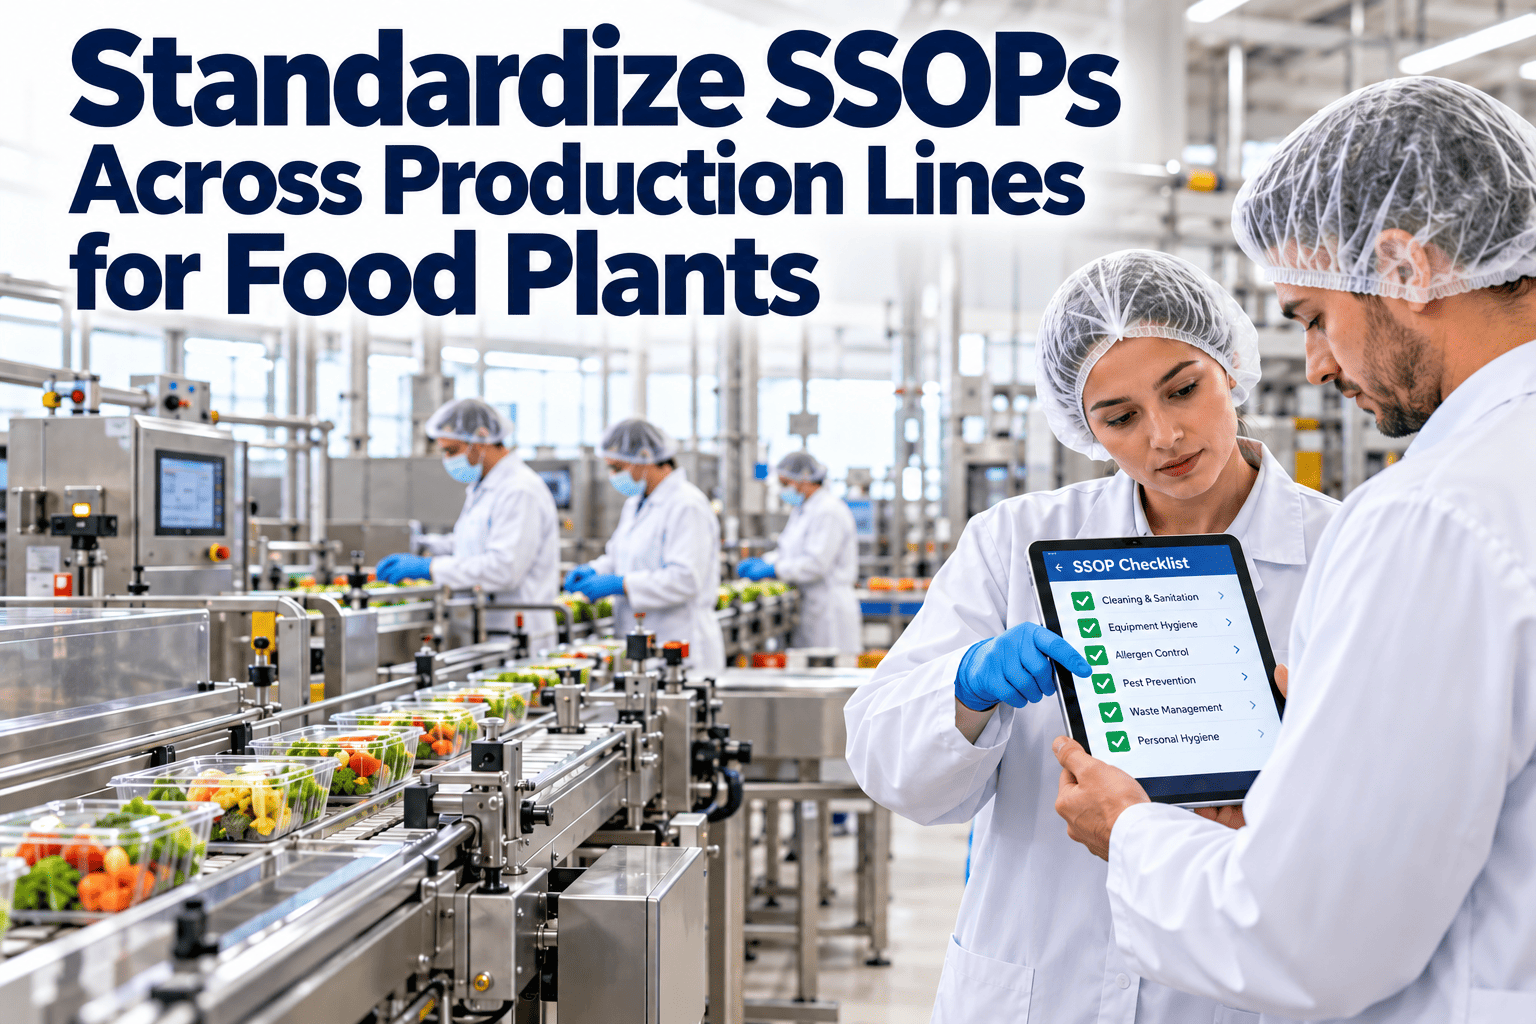
Walk through three lines in the same food plant and you may find three different ways to clean the same type of equipment. One crew rinses before foaming, another does not. One instruction lists a contact time, another leaves it out. Each version was written at a different time by a different person, and none of them is wrong on its own. Together they make training harder, verification inconsistent and audits uncomfortable. This guide explains how to align sanitation procedures across lines, keep what must stay specific and manage the library with maintenance management software.
Standardize SSOPs across production lines in food plants
Align cleaning instructions across lines with a common core, allow equipment-specific steps where they are needed and keep everything in one controlled library.
How a plant ends up with many versions of the same procedure
Inconsistency is rarely planned. It builds up over years of expansion, staff changes and fixes that were never shared.
Lines added at different times
Each new line brought its own supplier instructions and the habits of its first crew.
Local fixes that stayed local
A supervisor improves a step after a failure, but the change never reaches other lines.
Copy-and-edit documents
Procedures are copied from a similar line and edited by hand, leaving errors and old details behind.
Uncontrolled copies
Printed or saved versions sit in binders, shared drives and phones, and nobody knows which is current.
What different instructions cost you
Training burden
Staff who move between lines must relearn the basics, and trainers must explain why the lines differ.
Uneven results
Different steps, chemicals and contact times produce different cleaning outcomes, which makes verification results hard to compare.
Audit exposure
An auditor who finds different practices for the same hazard will ask which one is validated and why the others exist.
Standardize the principles, keep the machine details specific
The goal is not one identical document for every line. It is one consistent approach, with differences only where the equipment demands them.
- Document structure and headings
- Roles and responsibilities
- Cleaning stages and their order
- Approved chemicals, concentrations and contact times by surface type
- Verification methods and pass or fail criteria
- Corrective action rules and record formats
- Terms for zones, equipment states and risk levels
- Dismantling and reassembly sequence
- Special tools, brushes and access points
- Parts that need soaking or manual cleaning
- Hazards such as stored energy and lockout points
- Allergen and product changeover rules for that line
- Settings for cleaning-in-place systems
- Manufacturer instructions and photos
One template for every SSOP in the plant
A common template makes procedures easy to read, review and compare. Use the same sections in the same order on every line.
| Section | What it contains | Source |
|---|---|---|
| Purpose and scope | What area or equipment the procedure covers and when it is used | Layer 2 and 3 |
| Responsibilities | Who cleans, who verifies, who approves release | Layer 1 |
| Safety and PPE | Lockout, chemical handling, protective clothing and hazards | Layer 1 and 3 |
| Chemicals and tools | Approved products, concentration, temperature, contact time and tools | Layer 1 and 2 |
| Cleaning steps | Numbered steps in sequence, each with a single action | Layer 2 and 3 |
| Verification | Visual checks, swabs and pass or fail criteria | Layer 1 |
| Corrective action | What to do when a step fails, and who to inform | Layer 1 |
| Records | What is recorded, where and for how long | Layer 1 |
| Document control | Version number, owner, approval, effective date and review date | Layer 1 |
Keep one controlled sanitation library for every line
Attach current cleaning instructions to the equipment they cover, schedule the tasks and keep the records in one Oxmaint workspace.
See how a standard library looks for your lines
A practical way to align existing procedures
Start from what you have, not from a blank page. A structured review reveals the real differences and which ones matter.
Collect everything
Gather every current SSOP, work instruction, supplier guide and handwritten note used on each line.
Compare side by side
Group similar equipment, then lay the procedures next to each other and mark the differences in steps, chemicals, times and verification.
Sort the differences
Label each difference as equipment-driven, risk-driven or simply historical. Historical differences are candidates for removal.
Draft the core and modules
Write the plant-wide standard and the area modules, then reduce each line procedure to its specific steps.
Review with the floor
Walk each draft with the people who clean the equipment, and check that every step can be done as written.
Validate and approve
Quality confirms the effectiveness of changed procedures through verification results, then approves the release.
How a change flows through a standard library
With a layered library, a change is made once at the right layer and reaches every line that uses it. Compare that with editing each document separately.
Keep the library accurate once it is standardized
A standard library decays quickly without control. Set simple rules that make the current version obvious and the old version unavailable.
| Control | Rule | Why it matters |
|---|---|---|
| Single source | One approved version stored in one place, with no uncontrolled copies | Prevents crews using outdated instructions |
| Ownership | Each procedure has a named owner responsible for accuracy | Someone must keep it current |
| Version and effective date | Every change creates a new version with an effective date and summary | Shows what changed and when |
| Approval | Quality approves changes, with input from sanitation and maintenance | Maintains food safety review |
| Review cycle | Scheduled periodic review, plus review after equipment, chemical or product changes | Keeps instructions aligned with reality |
| Retirement | Withdrawn versions are removed from the floor and archived | Avoids mix-ups and supports traceability |
When a line really does need to be different
Some differences are legitimate. Handle them openly, so that exceptions are justified and recorded rather than accidental.
- Document the reason for each exception, such as a unique machine design, a different product risk or a manufacturer requirement.
- Show the exception inside the same template, in the equipment-specific layer, instead of creating a separate format.
- Have quality approve the exception and record the evidence that supports it, such as verification results.
- Review exceptions at each scheduled review, and remove them when the reason no longer applies.
- Link exceptions to the asset record, so they appear automatically whenever that equipment is cleaned.
Phase the change so the plant keeps running
Make the standard the easy way to work
- Put each procedure on the device or station where the task is done, so the crew uses the current version.
- Use photos and short step descriptions, since long paragraphs are rarely read during cleaning.
- Train supervisors first, so they can answer questions and spot deviations.
- Collect suggestions from the crew and show them what changed because of their input.
- Track which employees are trained on which procedure, and update training when a procedure changes.
Gaps you are likely to find when comparing procedures
When plants lay their SSOPs side by side, the same problems tend to appear. Use this list as a prompt for your own review.
Confirm that the standard cleans as well as the old way
Aligning steps should never reduce effectiveness. Treat each substantial change as something to be demonstrated, not assumed.
- Compare verification results before and after the change on the same equipment, using the same method and sites.
- Run the new procedure under normal conditions, with the actual crew, tools and time available.
- Pay extra attention to allergen changeovers and ready-to-eat areas, where the cost of failure is highest.
- Keep the evidence with the procedure so you can show an auditor why the standard was chosen.
- If results worsen on a line, find out why before extending the change, because equipment condition or layout may be the cause.
Extending the standard beyond a single plant
Groups with several plants face the same problem at a larger scale. The same layered model works, with one more level above the plant.
| Level | Owner | Content |
|---|---|---|
| Company standard | Corporate quality | Principles, documentation rules, verification approach and approval requirements |
| Plant core | Plant quality manager | Local regulatory needs, chemicals supplied, zones and risk assessment |
| Area and equipment modules | Sanitation and production leads | Procedures for each equipment family in that plant |
| Equipment steps | Line supervisors with maintenance | Specific dismantling, tools and settings for each machine |
Local legal requirements and customer rules may require differences between plants. Record them as documented exceptions.
Why standardization projects stall
- Writing the standard in an office without involving the people who clean the equipment.
- Making the core document so long that nobody reads it, instead of pushing detail into the modules.
- Skipping the pilot and discovering problems only after every line has changed.
- Leaving old versions on the floor, so crews keep using what they already know.
- Treating the project as finished at launch, with no owner for reviews and updates.
Standardize what the crew picks up, not only what they read
Instructions work better when the physical set-up supports them. A short list of approved chemicals and color-coded tools removes many decisions from the line.
- Limit the number of chemicals per plant, and assign each one to specific surface types and cleaning stages.
- Use color coding for brushes, scrapers and buckets by area and risk level, and display the key on the wall.
- Store tools in marked locations near the area where they are used, with a way to see when one is missing.
- Check dosing equipment and concentrations on a schedule, because a perfect procedure fails with a wrong dilution.
- Replace worn brushes and damaged tools on a planned cycle, and record the replacement.
Check that standardization is delivering results
Using Oxmaint to run the standard library
Oxmaint is maintenance management software. It does not replace your quality system, but it helps deliver procedures and records to the equipment and the people that need them.
- Asset management so each machine carries its current cleaning instructions, photos and manuals.
- Recurring cleaning and inspection tasks created from the same templates for every line.
- Mobile access to step lists and checklists at the point of use.
- Work orders for repairs that make a step difficult or impossible, tied to the same asset.
- Records and reports showing completion and failures by line, which supports comparison and audits.
- Preventive maintenance for spray systems, pumps, hoses and dosing equipment that cleaning depends on.
Standardizing SSOPs: common questions
Does standardizing mean identical SSOPs for every line?
No. Principles, structure and criteria are standard, while machine-specific steps stay in their own layer. The aim is consistency without ignoring real equipment differences.
Where should we start?
Pick one equipment family or line, compare its procedures and build the template there. You can get started by registering those assets first.
How do we handle manufacturer instructions?
Include the relevant parts in the equipment-specific layer and review them against your own risk assessment. Keep the source document linked to the asset.
Who approves changes?
Quality should approve, after input from sanitation, production and maintenance. Record the version, reason and effective date every time.
Can we see this set up for our plant?
Yes. A short session can map your lines and tasks into one library. Book a demo to see it.
One standard, every line, always current
Align cleaning instructions, keep equipment-specific steps where they belong and manage your sanitation library in one place.
Start with a single line and expand