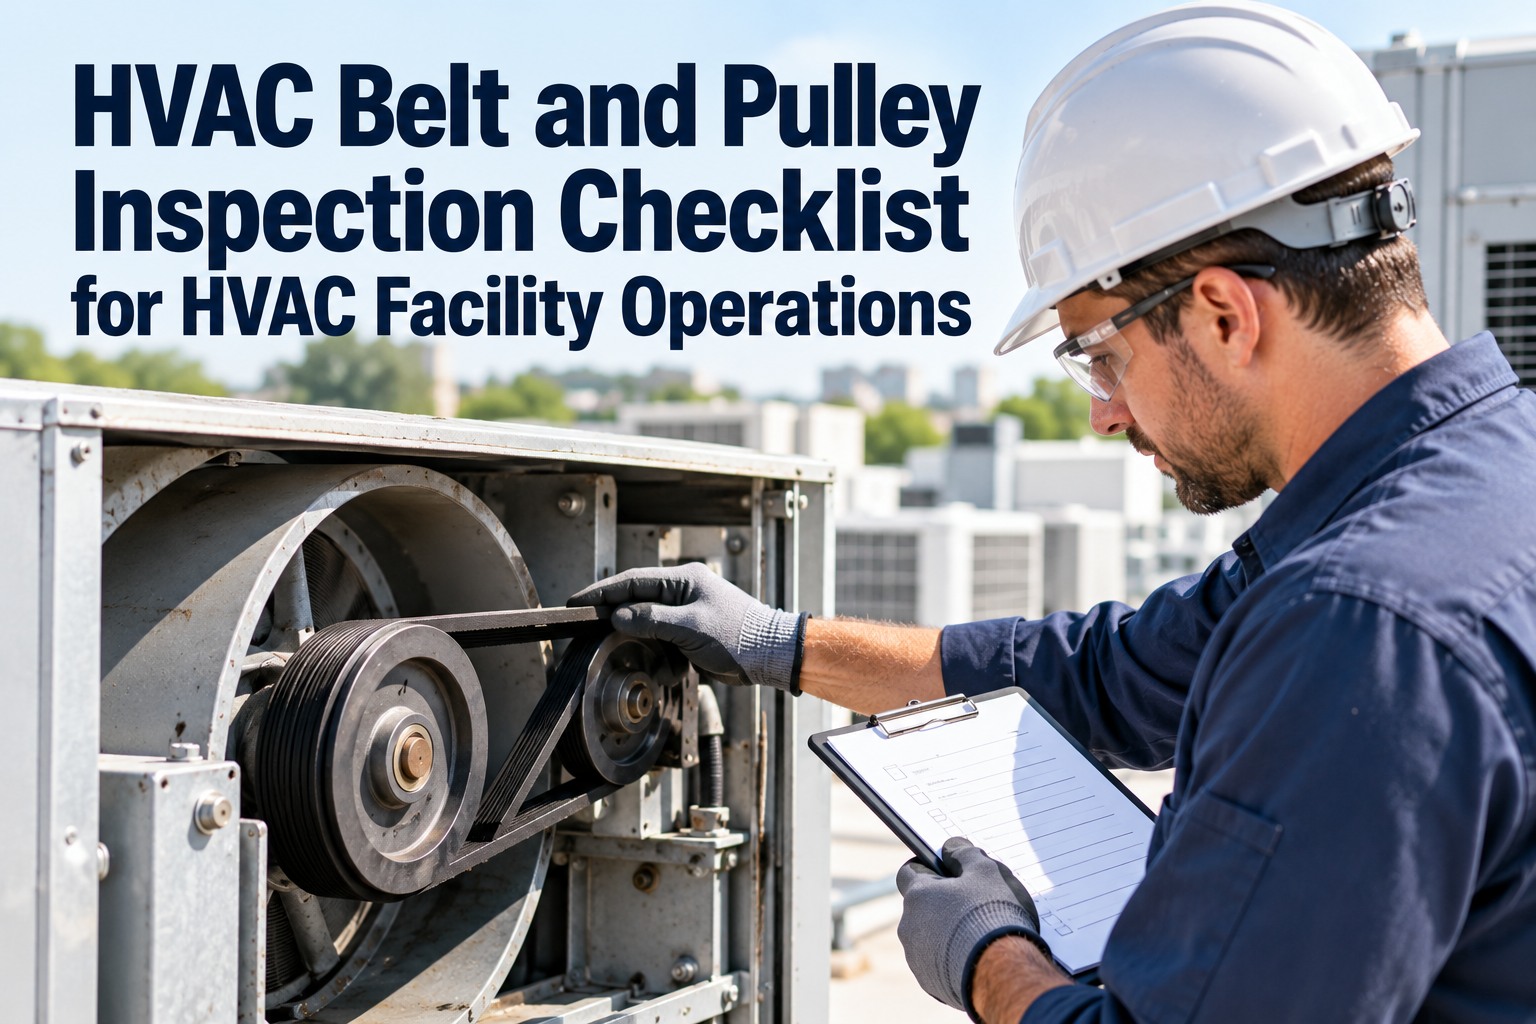
The squeal on start-up, the belt dust collecting in the guard, the airflow that has quietly dropped a notch — a slipping or misaligned HVAC belt wastes energy and burns itself out long before it snaps. A real inspection does not stop at "looks worn"; it takes a reading, picks the corrective action, and logs it so the next technician is not guessing. This checklist standardizes HVAC belt and pulley inspections — condition, tension, alignment, corrective action and documentation — using OXMAINT AI, the AI-powered CMMS that turns every check into a reading and every out-of-range result into a ranked work order.
A Tick-Box Says It Was Looked At. A Reading Says What To Do.
Standardize every HVAC belt and pulley inspection on one platform — condition, tension, sheave wear and alignment captured as readings, each out-of-range result raising a ranked corrective work order, every check logged per unit for audit and warranty.
Why Belt & Pulley Inspection Earns Its Own Checklist
The belt drive is the most adjustable wear point on an air handler — and the quietest. A belt three-quarters of a turn too loose slips, glazes, and steals airflow for weeks before anyone notices the energy bill or the warm zone. Sheave wear is worse: it is invisible until a brand-new belt fails in a fraction of its life because it was run on a worn groove. Catching both means a repeatable inspection with real readings behind every check. Sign up free and load your belt and pulley checklist into OXMAINT AI.
- No glazing or hard shine on the belt sidewalls
- No cracks, cuts, fraying or chunking
- No missing teeth on cogged or synchronous belts
- No belt dust or rubber debris building up in the guard
- No oil, coolant or heat damage on the belt surface
- Deflection measured by force/deflection method with a tester
- Deflection at 1/64" per inch of span length
- No squeal or slip on start-up or under load
- New belts re-tensioned after 24–48 hrs of run-in
- Tension re-checked whenever alignment is touched
- Groove checked with a sheave gauge — no dishing or gap
- Belt rides on the sidewalls, not bottomed in the groove
- No wobble or runout when the drive is turned by hand
- No cracks, chips or corrosion on the sheave
- Bore, bushing, set screws and keyway tight and secure
- Angular and parallel alignment checked, straightedge or laser
- Within 0.5° (V-belt) or 0.25° (synchronous / poly-V)
- Four points of contact across the drive when aligned
- Motor and fan sheaves sit on a common plane
- Alignment and tension iterated until neither needs adjusting
- Lockout / tagout applied before any contact with the drive
- Belt guard present, secure and undamaged
- No debris or nesting material packed against the drive
- Guard louvers clear for cooling airflow
- No exposed rotating parts once work is finished
- Belt profile and size match the sheave and the spec
- All belts on the drive are a matched set, same maker
- Correct spare belt stocked and labeled for the unit
- Drive and unit ID legible on the asset tag
- Inspection reading and photo captured for the record
From Tick-Box to Reading — What "Good" Looks Like
The difference between an inspection that prevents failures and one that just ages paper is the number written next to the check. Each line below pairs what you measure with the healthy range and the point where the reading tells you to act. Book a demo to see thresholds flag an out-of-range reading automatically.
When the Reading Says Act — Corrective Actions
A reading outside its range is only useful if it turns into the right fix, in the right order. These four cover almost every belt and pulley finding — and the escalation matters: never chase tension on a drive that is really misaligned, and never run a new belt on a worn sheave. Start free and auto-raise a corrective work order from any failed check.
Document It, or It Didn't Happen
An inspection nobody can find is an inspection you get to do twice — once in the field and once arguing with a warranty claim or an auditor. Capture the reading, a photo and the corrective action against the specific air handler, and the drive's whole history travels with the asset. Book a demo to see per-unit inspection history built automatically.
Stop Inspecting Belts With a Pen and a Hope.
Put the belt and pulley checklist, the readings, the thresholds and the corrective work orders on one platform — so every drive is inspected the same way, every time, and nothing worn slips through.
How OXMAINT AI Runs the Belt & Pulley Program
One platform behind the whole loop — the checklist, the readings, the thresholds, the corrective work orders and the history. This is the maintenance management software that keeps every air handler's drive inspected the same way and evidenced for life.
Belt checks used to be a line on a paper PM that everyone initialed and nobody read. The week we started logging the actual deflection and sheave readings, two drives that had passed on paper for a year turned out to be running on worn grooves — we were replacing belts every few months and blaming the belts. Fix the sheave, log the reading, and the belt lasts. The checklist did not change what we look at; it changed whether what we saw ever got written down.
Frequently Asked Questions
Every Drive. Every Reading. Every Correction, On the Record.
Move your HVAC belt and pulley inspections onto OXMAINT AI — a standard checklist, real readings against thresholds, corrective work orders raised on the spot, and a full history per air handler. Stop replacing belts in the dark and start inspecting with a number.