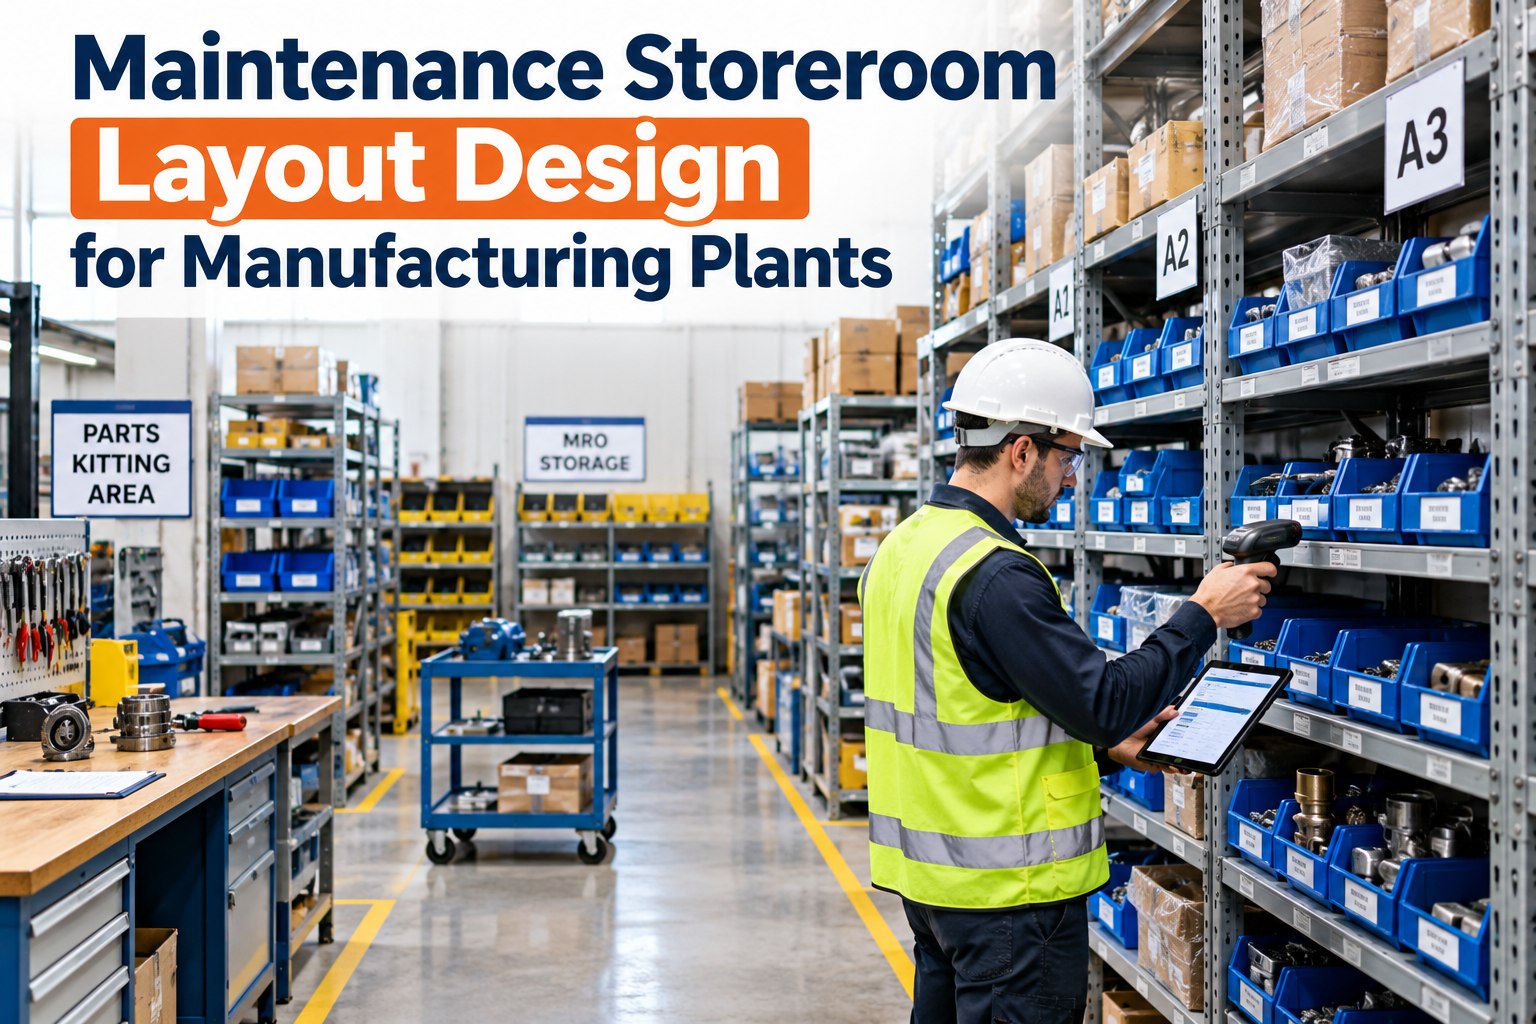
Walk into most plant storerooms and you can see the problem in thirty seconds: the part a technician needs is on the wrong shelf, under the wrong label or not in the system at all. The layout is the first maintenance task, because every breakdown runs through the storeroom door. OXMAINT AI is the maintenance management software whose bin locations, stock counts and QR scanning make a good layout stay good.
MRO STOREROOM · PLANT LAYOUT · BIN LOCATIONS · STOCK CONTROL · 2027
Maintenance Storeroom Layout Design for Manufacturing Plants
ABC slotting, bin locations, a kitting zone and labels that match your CMMS records, so a technician can find the right part in seconds instead of minutes. OXMAINT AI keeps every location, count and scan in step.
ABC slotting
Bin location codes
Kitting zone
QR scanning
18%
of a technician's time typically goes on looking for parts (Marshall Institute)
24–26%
more goes on walking to and from the job, in the same estimate
90 sec
a practical target from entering the storeroom to leaving with the right part
2 min
if finding a common bearing takes longer, fix the zoning before the labels
THE HIDDEN COST
Nobody budgets for the minutes lost between the work order and the part. Yet those minutes repeat on every job, every shift, in every plant. A better layout is one of the few fixes that pays back daily.
The Floor Plan: Closest to the Counter Is Fastest
Think of the storeroom as concentric rings around the issue counter. Fast movers sit within arm's reach, slow movers sit at the back and kits wait at the door. Sign up free and map your own zones.
RECEIVINGInspect and tag before put-away
C ZONESlow movers, back of the room
SECURED CAGEHigh-value and critical spares
B ZONEMedium movers, mid-room
SHELF-LIFESeals, adhesives, chemicals; first in, first out
KITTINGStaged jobs
A ZONEFast movers, nearest the counter
ISSUE COUNTERScan, issue, return
ENTRANCE
Illustrative layout. Your room shape will differ, but the order should not: counter, then A, then B, then C, with kitting and the cage close to the counter and receiving apart from the pick path.
One Code, Everywhere: Bin Location Labels
A bin code should read like an address and match the CMMS record exactly. If the shelf says one thing and the system says another, the technician stops trusting both. Book a demo to see labels and records stay in sync.
BIN LOCATION CODE · EXAMPLE
A3Aisle
-
S2Section
-
B14Bin
ON THE SHELF
A3-S2-B14
Bearing 6205-2RS
Scan to issue
=
IN THE CMMS
PartBearing 6205-2RS
LocationA3-S2-B14
On hand12
Min / Max4 / 16
Use labels rated for warehouse conditions so they do not fade or peel, and design them to scan reliably with a phone. Standardise part names and remove duplicates, or two bins will hold the same part.
Slot by Velocity, Not by Supplier
Group parts by how often they move and by the equipment they serve, not by who sold them. Then count the fast movers most often, because that is where drift costs the most. Start free and tag your A, B and C parts.
A
Fast movers
Closest to the counter, between knee and shoulder height.
Count monthly
B
Medium movers
Mid-room shelving, grouped by line or equipment.
Count quarterly
C
Slow movers
Back of the room or upper racking. Purge dead stock regularly.
Count twice a year
Count frequencies follow one storeroom framework from MPulse; set yours by criticality and by how often counts drift. Treat a $40 filter and a $4,000 gearbox differently: price matters less than lead time and downtime if it is missing.
Make the Storeroom the Fastest Stop in the Plant.
Load your bins into OXMAINT AI, print the labels and let technicians scan parts to the work order. You will see accuracy and speed improve within weeks.
The Kitting Zone: Pull Parts Before the Job
Kitting means preparing the materials and tools for a work order in advance. Start with preventive maintenance jobs, which are the easiest to plan. Book a demo to see kits tied to scheduled work orders.
1Find every part and tool the work order needs
2Place them in a marked staging bay
3Keep the bay secure and organised
4Move the kit to site before the job
5Return unused parts and close the order
KIT TAG
WO-2431 · Conveyor 4 gearbox PM
Gear oil, 2 L
Breather, 1
Output seal, 1
Torque wrench, 1
Ready for pick-up
Lock It Down Without Slowing It Down
Security should protect high-value stock and keep records honest, not make technicians queue. Start free and set access by role.
Secured cage
High-value and regulated items sit behind controlled access.
Issue against a work order
Every sign-out names the job, so usage is traceable.
Reserve parts
Reserved stock cannot be issued to another job.
Rotate shelf-life stock
First in, first out, segregated from other parts.
The 90-Second Walk Test
You do not need a consultant to know whether the layout works. Time a technician finding a common part and let the clock decide. Book a demo and we will show how to track it.
90seconds
Pick a common part, such as a bearing or a filter.
Start the clock when the technician walks in.
Stop it at the exit with the correct part.
Over two minutes? Fix zoning before touching the labels.
EXPERT REVIEWStoreroom and reliability view
Do the bin audit first. A 48-hour check of every location against the system record will show you where the layout and the data disagree, and that is where the lost minutes hide. Fix accuracy before you move a single shelf, or you will re-label a mess. Keep the first pilot small: one aisle, one line, then roll it out.
How OXMAINT AI Keeps the Layout Working
OXMAINT AI ties bin locations, stock control and mobile scanning to the same part record. Try it free on your busiest aisle.
BINSBin locations on every part
Aisle, section and bin recorded once and used everywhere.
QRScan to issue and return
A phone scan issues a part to a work order in seconds.
STOCKMin and max with reorder alerts
Set levels by usage, lead time and criticality.
KITSParts reserved to work orders
Planned jobs reserve their parts so kits are ready.
COUNTCycle count tasks
Counts scheduled by A, B and C class with variances logged.
VIEWAccuracy and usage history
See which parts move, which sit, and where counts drift.
Questions Storeroom and Maintenance Teams Ask
What is the best layout for a maintenance storeroom?
How should we label bins?
How often should we cycle count?
What is kitting and is it worth it?
Do we need special software for storeroom layout?
Find Every Part in Seconds — With OXMAINT AI.
Bin locations that match the shelf, QR scanning that issues to the work order and counts that stay accurate. Start with one aisle.