Dust Collection and Air Pollution Control System Maintenance in Steel Mills
By John Mark on March 13, 2026
Steel mills are among the largest industrial sources of particulate matter, heavy metal emissions, and gaseous pollutants in the world. Every tapping event, every scrap charge, every casting sequence, and every ton of material handled generates dust and fumes that must be captured, filtered, and disposed of in compliance with increasingly stringent regulatory requirements. The dust collection and air pollution control systems that make this possible — baghouses, electrostatic precipitators, scrubbers, ventilation hoods, and ducting networks — are among the most maintenance-intensive assets in the plant. When they fail, the consequences arrive simultaneously from two directions: production must slow or stop to avoid regulatory violations, and the maintenance team faces emergency repairs under the worst possible conditions. A dust collection system that is reactively maintained is not just an environmental liability — it is a production constraint waiting to materialize. Schedule a free air pollution control maintenance review with our team and find out where your current program has gaps before an EPA inspection or a baghouse failure makes the decision for you.
Regulatory Framework: What Steel Mills Must Control
Steel mill dust collection and air pollution control maintenance is not discretionary — it is legally mandated as a condition of the operating permits that allow production to continue. Understanding the regulatory drivers behind maintenance requirements establishes why consistent, documented maintenance programs are a business continuity requirement, not a cost center.
EPA 40 CFR Part 60
New Source Performance Standards (NSPS)
Prescribes emission limits for particulate matter from electric arc furnaces, basic oxygen furnaces, and sinter plants. NSPS Subpart AA covers EAF shops; Subpart N covers BOF facilities. Compliance requires continuous emission monitoring or periodic testing to demonstrate that control equipment is meeting required collection efficiency levels. Equipment maintenance records are subject to inspection at any time.
National Emission Standards for Hazardous Air Pollutants (NESHAP)
Steel major source facilities are subject to NESHAP Subpart FFFFF (integrated iron and steel) and Subpart YYYYY (secondary aluminum — also covering EAF with scrap input). NESHAP imposes maintenance, inspection, and monitoring requirements beyond NSPS, and requires facility-specific operating plans that specify how control equipment must be maintained to remain compliant.
Applies to: Major source facilities — typically all integrated steel and large EAF shops
Title V Operating Permits
Facility-Specific Emission Limits and Control Requirements
Every major steel facility operates under a Title V permit that specifies emission limits, required control equipment, minimum collection efficiency, inspection frequencies, monitoring protocols, and recordkeeping requirements. Permit conditions are legally enforceable — operating without meeting permit conditions, even temporarily during maintenance, requires advance notification to the regulatory authority.
Applies to: All major source steel facilities
OSHA 29 CFR 1910.1000
Workplace Air Contaminant Limits
Beyond environmental compliance, dust collection systems protect workers from exposure to iron oxide fumes, manganese, chromium, lead, and other hazardous air contaminants generated during steel production. Failure of dust collection equipment inside the plant creates OSHA exposure violations independent of any EPA permit issue — representing dual regulatory liability from a single equipment failure.
Applies to: All production areas with dust-generating operations
$70,117
Maximum daily EPA civil penalty per violation under CAA Section 113
$25,000+
Typical OSHA penalty for a serious dust exposure violation in a steel plant
Permit-based
Production shutdown authority granted to EPA when permit conditions are violated — no warning required
The Major Dust Control Systems in Steel Mills
Steel mills deploy multiple types of dust and pollution control equipment, each suited to different emission sources, particle characteristics, and gas volumes. Maintenance requirements differ substantially between system types — a baghouse maintenance program cannot simply be applied to an electrostatic precipitator, and scrubber systems require entirely different expertise. Understanding each system is the prerequisite for maintaining any of them effectively.
Baghouse Fabric Filter Systems
Most Common in EAF and BOF Shops
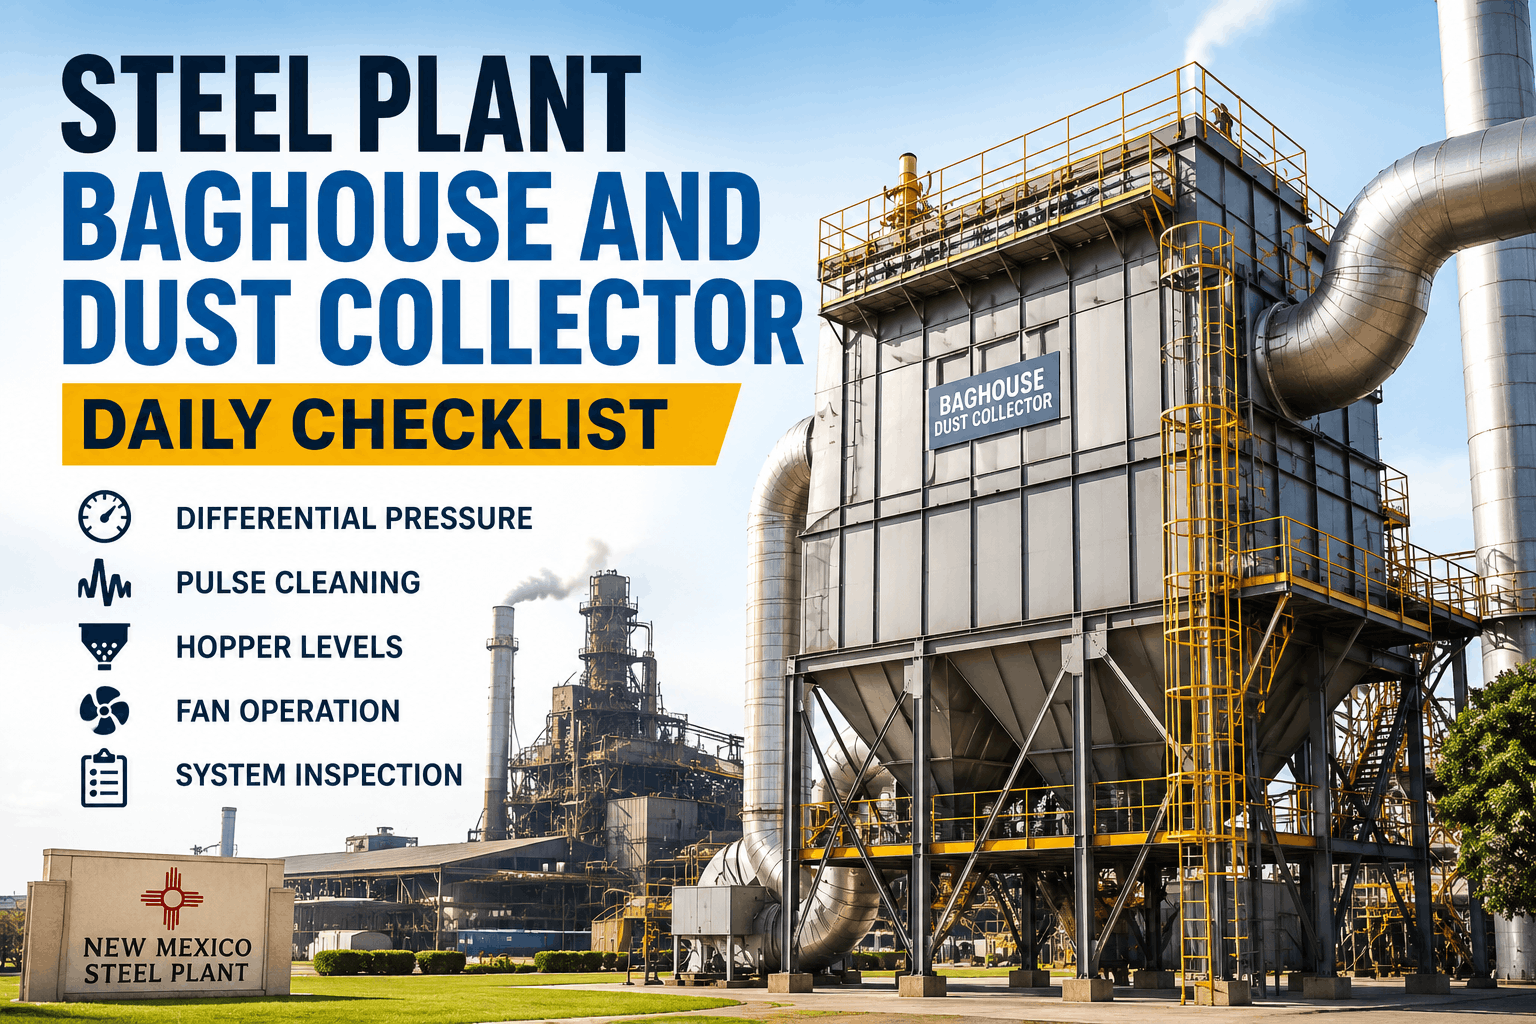
Baghouses use woven or felted filter bags to capture fine particulate matter from high-volume gas streams. They are the dominant dust collection technology in steel melt shops because they achieve high collection efficiency (99%+) across a wide particle size range. The filter bags are the primary consumable component — their condition directly determines emission performance, and their failure is the most common cause of permit exceedances. Pulse-jet baghouses clean bags continuously during operation; shaker and reverse-air designs require periodic offline cleaning cycles.
Collection Efficiency99–99.9%
Typical Bag Life2–5 years
Operating TemperatureUp to 260°C (standard)
Key Failure ModeBag rupture or bypass
Electrostatic Precipitators (ESPs)
Primary Technology for Coke Plants and Sinter Plants
ESPs use high-voltage electric fields to charge and collect particulate matter on collecting plates. They handle large gas volumes at high temperatures more reliably than fabric filters and are well suited to coke oven gas cleaning and sinter plant off-gas treatment where gas composition and temperature would damage filter bags. Collecting plate cleaning through mechanical rapping is continuous, and the collected dust is discharged through hoppers. ESP performance degrades gradually as plate spacing increases, electrodes corrode, or rapping systems fail — often without visible indication until emission testing reveals the decline.
Collection Efficiency95–99.5%
Equipment Life20–30+ years with maintenance
Operating TemperatureUp to 400°C
Key Failure ModePlate misalignment or rapping failure
Wet Scrubbers
Used for Gas Cooling and Simultaneous Acid Gas Control
Wet scrubbers contact contaminated gas streams with liquid — typically water — to remove both particulate matter and soluble gases simultaneously. They are commonly used downstream of EAF off-gas cooling systems and for sulfur dioxide removal from BOF and coke oven gas streams. Unlike dry systems, scrubbers generate contaminated wastewater that requires its own treatment and disposal program. The liquid distribution system, mist eliminators, and slurry handling components are the highest-maintenance elements in wet scrubber operation.
Operating TemperatureReduces gas to saturation temp
Key Failure ModeNozzle plugging or mist carryover
Ventilation Hoods and Canopy Systems
First Line of Capture at Process Sources
Ventilation hoods and canopy systems are the capture point for emissions at the process source — furnace roofs, tapping stations, casting platforms, and material handling transfer points. Their geometry, positioning, and air flow rates determine how much emission is captured before it escapes into the building and out through roof ventilators. Hood leaks, deformations from heat exposure, and deteriorated seals at duct connections reduce capture efficiency silently — the baghouse still operates, but an increasing fraction of emissions bypass capture entirely.
Capture Velocity Required0.3–1.0 m/s at hood face
Inspection FrequencyMonthly visual + annual flow test
Common DamageHeat distortion, weld failures
Key Failure ModeBypass capture — invisible to monitors
Your Dust Control Assets Deserve Better Than Reactive Maintenance
Oxmaint connects every baghouse, ESP, scrubber, and hood inspection to a single scheduled, tracked, and documented maintenance program — so compliance records are always current and failures are found before regulators do.
Baghouse Maintenance: The Most Critical Program in Steel Mill Air Control
Baghouse systems are the most prevalent air pollution control technology in steel mills and the one most frequently cited in regulatory violations. Most citations do not result from inadequate equipment — they result from inadequate maintenance programs. The following framework covers every element of a defensible, effective baghouse maintenance program.
Filter bags are the performance-critical component of every baghouse system. Bag failure — holes, blinding, or collapse — directly causes permit exceedances. An effective bag management program tracks individual bag age, monitors differential pressure trends as an early indicator of bag condition, conducts visual inspection during scheduled access, and uses opacity monitoring data to detect sudden bag failures in real time.
Healthy Bag Signs
Stable differential pressure within design rangeOpacity reading below permit thresholdUniform dust cake on visual inspectionNo visible holes or seam failures
Failure Warning Signs
Sudden drop in differential pressureOpacity exceedance during normal operationDust on clean-air side of tube sheetVisible pinhole light during internal inspection
02
Pulse-Jet Cleaning System Maintenance
Monthly inspection + annual overhaul
The pulse-jet cleaning system uses compressed air pulses to dislodge accumulated dust cake from filter bags. Solenoid valves, diaphragm valves, compressed air manifolds, and timers are all maintenance items that directly affect cleaning effectiveness. A partially failed cleaning system causes uneven bag loading, accelerated bag wear, and rising differential pressure that eventually forces offline cleaning cycles — creating unplanned production delays.
✓Solenoid valve actuation test — all compartments cycling
✓Diaphragm valve condition — no cracking or leak-by
✓Compressed air pressure at manifold — within design range
✓Timer sequence verified — pulse duration and interval correct
✓Air dryer operation — no moisture in pulse air supply
✓Blow tube alignment — centred in bag, no contact with fabric
03
Hopper and Dust Discharge System
Weekly inspection + condition monitoring
Collected dust must be discharged continuously to prevent hopper overflows that bury the bottom rows of filter bags — one of the most damaging conditions in baghouse operation. Rotary airlock valves, screw conveyors, and dust handling chain conveyors must operate reliably on every shift. Hopper level monitoring with high-level alarms prevents accumulation from going undetected across shift changes. In cold climates, hopper heating is critical to prevent dust bridging that blocks discharge.
✓Rotary airlock seal condition — no bypass leakage
✓Screw conveyor drive and auger wear inspection
✓Hopper level sensor calibration and alarm test
✓Hopper heater function in cold-weather operation
✓Dust bin or container level and emptying schedule
✓Dust disposal records — manifests for hazardous waste streams
04
Differential Pressure and Performance Monitoring
Continuous — recorded every shift
Differential pressure across the baghouse — the pressure drop from dirty to clean side — is the primary real-time performance indicator for any fabric filter system. It reflects the combined effect of dust loading, cleaning effectiveness, and bag condition. Trending ΔP data reveals system health over time: a gradual rise indicates cleaning system degradation or bag blinding; a sudden drop may indicate bag failure or bypass. Every permit inspection and CEMS audit will ask for ΔP records — these must be continuous, not spot-checked.
ΔP Reading
Interpretation
Required Action
Within design range
Normal operation — bags and cleaning system functioning
Log and continue monitoring
Rising above high limit
Bag blinding or cleaning system degradation
Inspect cleaning system; plan offline bag inspection
Sudden drop below normal
Possible bag failure, bypass, or compartment isolation
Opacity check immediately; inspect for bag failures
Near zero or erratic
Sensor failure, major compartment bypass, or hood duct problem
Shut down compartment; inspect and recalibrate sensor
ESP Maintenance: Keeping High-Voltage Collectors at Peak Efficiency
Electrostatic precipitators are low-frequency, high-consequence maintenance assets. They rarely fail suddenly — performance degrades gradually through identifiable mechanisms that can be managed if the right monitoring and maintenance program is in place. The challenge is that ESP performance decline often goes undetected because emission testing is infrequent and opacity monitors do not capture the full efficiency picture.
Discharge Electrode System
Annual inspection during planned outage
Discharge electrodes (wires or rigid frames) must maintain correct tension and spacing from collecting plates. Broken wires cause electrical sparking that reduces field strength across the entire section. Electrode alignment is checked during annual outage with the system de-energized.
Wire condition — no broken or sagging wires
Frame electrode alignment and connection integrity
Anti-sway baffles and alignment weights
Collecting Plates and Rapping System
Quarterly inspection + rapping system monthly
Collecting plates must be clean, flat, and uniformly spaced. The mechanical rapping system dislodges accumulated dust — rapping frequency and intensity must be optimized for the specific dust type. Under-rapping leads to dust buildup that reduces electrical field strength; over-rapping re-entrains collected dust back into the gas stream.
Plate alignment check — spacing uniform throughout
Rapper timing and impact force calibration
Plate corrosion assessment — particularly near hopper inlets
High-Voltage Power Supply
Monthly electrical checks + annual transformer service
The T-R (transformer-rectifier) sets that power ESP fields must maintain stable output voltage and current. Automatic voltage control systems maximize collection efficiency by running each section at the highest voltage without sparking. T-R set performance data — secondary voltage, current, and spark rate — provides direct operational condition information.
Secondary voltage and current readings per section
ESP hoppers accumulate highly resistive dusts that can bridge and block discharge — particularly common with high-resistivity dusts from coke and sinter plants. Hopper heaters prevent moisture condensation that causes caking. Full hoppers create back-ionization that severely reduces collection efficiency across adjacent sections.
Hopper level monitoring with high-level alarm test
Heater element function check
Discharge valve operation and dust removal rate
Track Every Inspection. Close Every Finding. Stay Compliant.
Oxmaint schedules baghouse and ESP inspections automatically, captures findings digitally in the field, generates corrective actions linked to the right technician, and produces the compliance records your permit requires — without chasing paperwork.
The ductwork, fans, dampers, and expansion joints that transport contaminated air from process sources to control equipment are the connective tissue of the dust collection system — and they are among the most neglected components in steel mill air pollution control programs. A baghouse or ESP operating perfectly cannot compensate for a ducting system that leaks 30% of its captured flow before it reaches the control equipment.
Component
Failure Mode
Inspection Frequency
Detection Method
Consequence of Failure
Main ductwork and transitions
Corrosion-through, abrasion wear at elbows, thermal distortion
Annual external + biennial internal
Ultrasonic wall thickness measurement, visual
Fugitive emissions bypass control equipment; production area contamination
Induced draft fans
Impeller erosion, bearing failure, shaft imbalance from dust buildup
Thermal imaging of shell exterior, internal visual
Shell burnthrough; gas leaks; fire risk in adjacent structures
Spark arrestors and ember traps
Buildup of combustible dust, screen plugging
Weekly inspection in high-spark operations
Visual inspection during production
Baghouse fire from burning embers — total system loss
Compliance Monitoring and Recordkeeping Requirements
The maintenance records your team creates every day are the legal evidence that your dust collection systems are being properly operated. When an EPA inspector arrives or a permit renewal is under review, maintenance records are reviewed as thoroughly as emission test data. A well-maintained system with poor records is treated the same as a poorly maintained system — because from a regulatory standpoint, what is not documented did not happen.
Continuous Monitoring Records
Opacity monitor readings — every 6-minute average
Differential pressure across each baghouse compartment
Fan amperage and flow rate where required by permit
ESP secondary voltage and current per field section
Retention: 2 years minimum; 5 years recommended
Inspection and Maintenance Logs
Scheduled inspection records with technician ID and date
Filter bag replacement records — date, compartment, quantity
Corrective action records for all identified deficiencies
Malfunction logs — every deviation from normal operation
Retention: 5 years; duration of permit for malfunction logs
Performance Testing Records
Stack emission test reports — particulate and HAP results
Collection efficiency calculations per control device
Capture efficiency test results for hooded sources
CEMS calibration and audit records
Retention: Life of permit plus 5 years
Deviation and Excess Emission Reports
All opacity exceedances — cause, duration, corrective action
Periods of control equipment unavailability during production
Startup, shutdown, and malfunction (SSM) event logs
Notification letters to regulatory agency where required
Retention: Life of facility — these records are permanent
Maintenance KPIs for Steel Mill Dust Collection Systems
Measuring dust collection system maintenance performance requires metrics that capture both regulatory compliance outcomes and system reliability. These KPIs give maintenance and environmental managers the leading indicators needed to manage performance before violations occur.
Opacity Exceedance Rate
Target: Zero
Number of opacity exceedances per quarter — each exceedance is a potential permit violation and a direct indicator of bag failure, duct bypass, or hood capture deficiency.
Scheduled Inspection Completion Rate
Target: 100%
All permit-required and internally scheduled inspections completed on time. Missed inspections are a standalone permit violation regardless of whether emissions are within limits.
Differential Pressure Within Range
Target: 100% of operating hours
Percentage of operating hours where baghouse differential pressure remains within permitted or design range — out-of-range readings indicate maintenance needs or operating exceedances.
Control Equipment Availability
Target: > 98%
Percentage of production hours during which each control device is fully operational. Downtime of a required control device during production hours is a permit violation in most Title V facilities.
Bag Life Achieved vs Target
Target: ≥ 100% of design life
Average bag life achieved in each baghouse compartment compared to design life. Premature bag failure indicates temperature spikes, moisture excursions, or chemical attack that must be investigated and controlled.
Corrective Action Closure Rate
Target: 100% within 30 days
All inspection findings and deficiencies closed within 30 days. Open corrective actions on air pollution control equipment are evidence of management failure during regulatory inspections — not just a maintenance gap.
From Compliance Risk to Compliance Confidence
Oxmaint gives steel mill environmental and maintenance teams a single platform to manage every inspection, every finding, every corrective action, and every regulatory record for all dust collection and air pollution control assets — so the next EPA inspection is something you look forward to, not dread.
How often must baghouse filter bags be replaced in a steel mill EAF shop?
Filter bag life in EAF baghouses typically ranges from 2 to 5 years, depending on gas temperature, moisture content, chemical composition of the dust, and cleaning system effectiveness. The variability is significant — a baghouse operating with temperature spikes above bag material limits or with moisture condensation during cold starts will see premature failures in as little as 12 to 18 months. Differential pressure trending, periodic internal visual inspection, and opacity monitoring are the most reliable tools for determining actual remaining bag life rather than relying on fixed calendar-based replacement schedules. Most environmental managers use a combination of annual visual inspection during planned outages and continuous ΔP monitoring to make bag replacement decisions based on actual condition rather than age alone.
What causes opacity exceedances in steel mill baghouses and how are they prevented?
The most common causes of opacity exceedances in steel mill baghouses are bag failures (holes or seam splits that allow unfiltered gas bypass), hopper overflow that buries lower bag rows and causes bypass flow, cleaning system failures that allow excessive dust cake buildup and eventual bag collapse, duct leaks or open access doors that admit uncontrolled emission, and temperature exceedances that harden the dust cake into an impenetrable mass. Prevention requires all four elements of a complete maintenance program: frequent bag inspection with replacement at first sign of degradation, cleaning system monitoring with immediate repair of failed valves or timers, hopper level monitoring with high-level alarms on every shift, and duct integrity inspections that find and seal leaks before they appear on the opacity monitor. Most opacity events are traceable to a specific missed maintenance action that, in retrospect, would have taken less than an hour to perform.
Can a steel mill legally operate during baghouse or ESP maintenance downtime?
Whether production can continue during control equipment downtime depends on the specific conditions of the facility's Title V operating permit and applicable NSPS or NESHAP requirements. Most permits include startup, shutdown, and malfunction (SSM) provisions that allow limited periods of control equipment unavailability, provided the facility follows a documented malfunction abatement plan and notifies the regulatory authority within the required timeframe — typically within 2 hours for significant events. Operating a production source without required control equipment outside of a permitted SSM condition is a permit violation. Steel mill environmental managers should know their permit's specific SSM provisions for every dust control device before any planned or unplanned maintenance event occurs, and should have written procedures for each scenario that include notification requirements and maximum allowable downtime.
How does a CMMS help manage air pollution control system compliance in steel mills?
A maintenance management system addresses the specific compliance documentation requirements that make dust collection maintenance auditable. It schedules all permit-required inspections with automatic reminders and overdue escalation — so missed inspections are flagged before they become violations. It creates permanent, timestamped maintenance records for every inspection, repair, and bag replacement that can be produced instantly during a regulatory inspection. It tracks corrective action closure with owner assignment and due dates, creating the evidence trail that demonstrates prompt response to identified deficiencies. It generates the maintenance summary reports required for annual compliance certification and Title V permit renewal. And it links equipment availability tracking to production scheduling, so the environmental team knows immediately when a control device goes offline during production hours and can initiate the permit notification process within the required window.