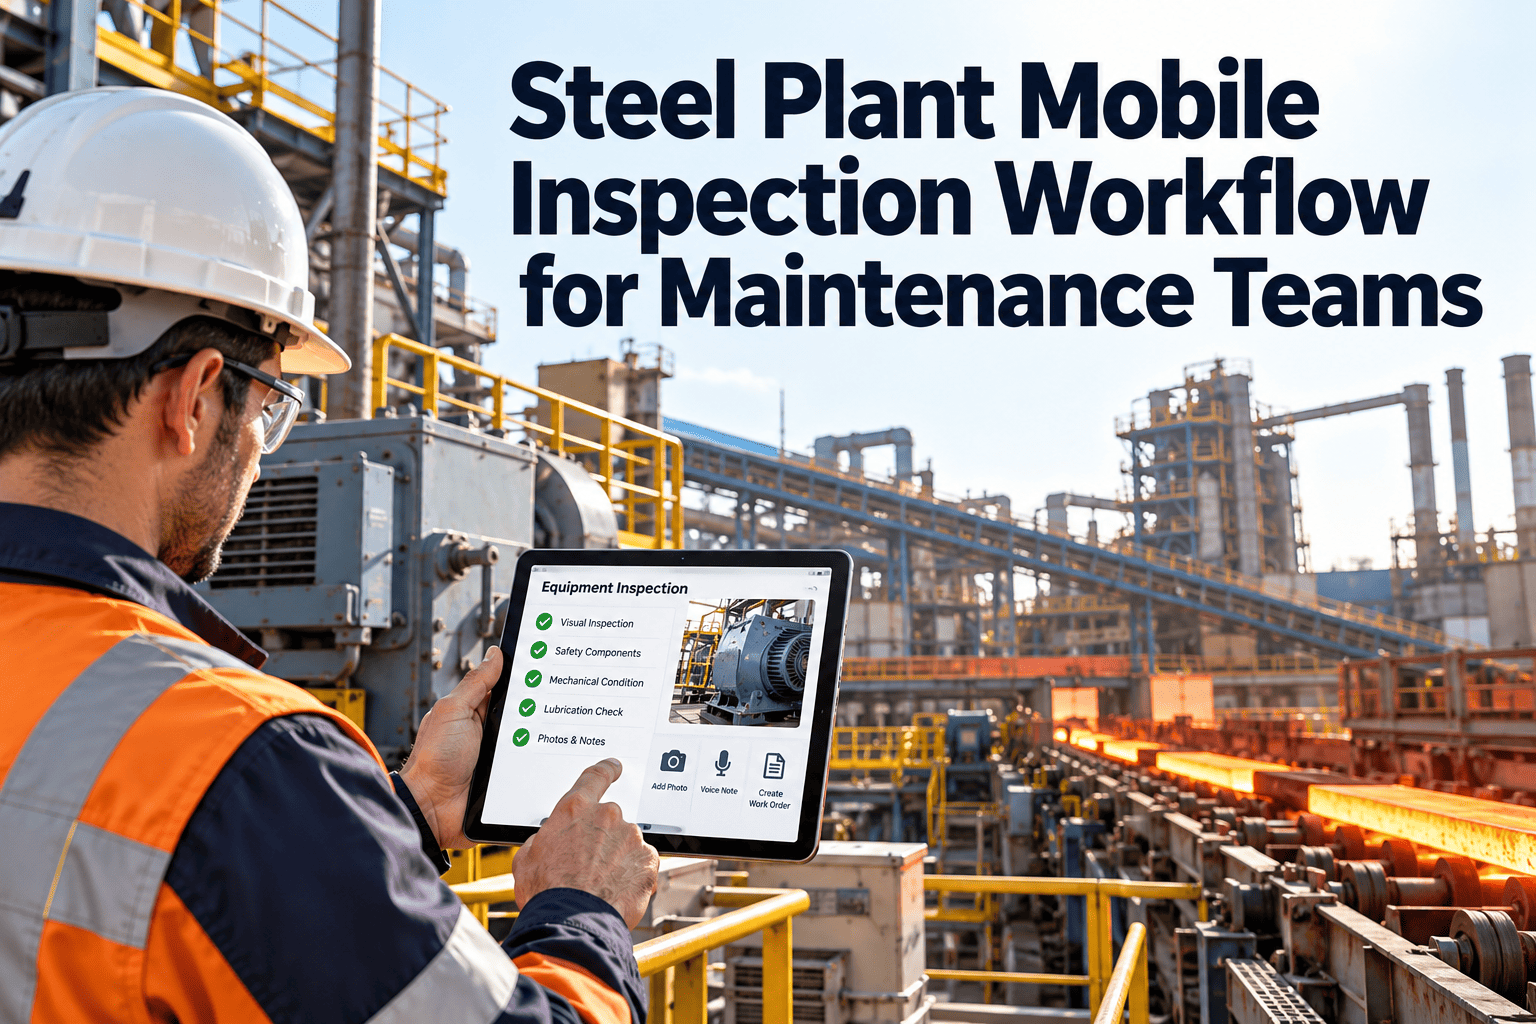
A steel plant never stops long enough for a clipboard to keep up. Furnaces, casters, mills, cranes and hydraulic systems run hot, loud and continuous, and the defects that stop them usually show up in small ways first: a warm bearing, a weeping hose, a loose guard. Mobile inspections turn those observations into records and work. This guide explains how to design the workflow, and how Oxmaint maintenance management software supports it.
Steel Plant Mobile Inspection Workflow for Maintenance Teams
Replace paper rounds with a route-based mobile workflow that captures findings, enforces lockout steps and sends every defect straight to a work order.
Why Paper Rounds Break Down in a Steel Mill
Steel plants cover enormous ground, from raw material yards to finishing lines. Paper rounds struggle across that footprint for predictable reasons.
- Findings written at the asset, typed in hours later
- Handwriting that planners cannot read
- Skipped checkpoints nobody notices until a failure
- Photos on personal phones, not on the asset record
- Lockout steps copied from memory or old binders
- Veteran knowledge that leaves with the person
- Findings entered once, at the asset, with a timestamp
- Structured answers that planners can filter and trend
- Required checkpoints that show as complete or missed
- Photos and readings attached to the equipment history
- Lockout procedures delivered step by step on the device
- Technician notes saved as reusable knowledge
Where the Inspection Route Should Go
A useful route follows the process, not the org chart. Group checkpoints by area so a technician walks logically and each finding lands on the right asset.
| Plant area | Typical checks | What a defect should trigger |
|---|---|---|
| Blast furnace and raw materials | Conveyor condition, cooling water flow, bleeder and valve leaks, dust accumulation | Corrective work order and cleaning task |
| Steelmaking (BOF or EAF) | Hydraulic hoses, electrode or lance equipment, cooling circuits, refractory wear notes | Priority inspection and planned repair |
| Continuous caster | Mold cooling, segment rolls, spray nozzles, oscillation, lubrication points | Same-shift work order for critical items |
| Rolling mills | Gearbox noise and temperature, roll chocks, couplings, guards, oil leaks | Condition-based task with readings attached |
| Cranes and handling | Wire ropes, hooks, brakes, limit switches, hoist lubrication | Safety-related hold until cleared |
| Utilities | Compressors, pumps, transformers, water treatment, gas lines | Preventive task adjustment or repair |
The Five-Stage Mobile Inspection Workflow
Digital rounds work when every stage has a clear owner and a clear output. This sequence fits most steel plants.
Designing Checklists Technicians Will Actually Use
Checklist quality decides whether a mobile program survives past the first month. Long, vague forms train people to tap through them.
Principles that hold up on the floor
- Ask what can be observed: leak present, guard secure, temperature in range.
- Use numeric fields for readings so trends can be charted later.
- Require a photo only for failures, not every pass.
- Keep each asset check short enough to finish while standing at the equipment.
- Write acceptance limits into the question so nobody guesses.
- Review questions quarterly and remove those that never find anything.
Examples of weak and strong questions
Built for Heat, Dust, Gas and Poor Signal
Steel plant conditions are hard on devices and networks. Plan for them before rollout rather than after complaints.
Lockout and Tagout Inside the Workflow
Inspections often reveal work that cannot start until energy is isolated. In the United States, OSHA's lockout/tagout standard (29 CFR 1910.147) expects documented, equipment-specific procedures, and steel plants have many energy sources to control.
A digital lockout sequence
Digital records also help audits, since the procedure version, the person and the time are saved against the work order. Final procedures remain the responsibility of your safety team.
See a Mobile Round Turn Into a Work Order
Walk through a route, a failed checkpoint and the resulting work order in a live session built around your equipment.
Capturing Knowledge Before It Walks Out the Gate
Many mills depend on a few experienced technicians who know which sound means trouble. Mobile inspections are a practical way to write that experience down.
Measuring Technician Productivity Without Gaming It
Productivity here means finding problems earlier and spending less time on paperwork, not rushing routes. Track measures that reward quality.
Deciding What a Finding Should Trigger
Not every defect deserves the same reaction. Agree on response rules in advance so supervisors do not negotiate each finding.
| Severity | Example finding | Standard response |
|---|---|---|
| Critical | Crane brake fault, major hydraulic leak near hot metal | Stop use, isolate and escalate immediately |
| Major | Rising gearbox temperature trend, damaged guard | Plan repair at the next available window |
| Minor | Minor seep, worn label, loose bracket | Bundle into routine corrective work |
| Watch | Slight noise change, borderline reading | Re-inspect with tighter frequency and track the trend |
Connecting Inspections to Condition-Based Maintenance
Handheld readings from vibration meters, thermal cameras and oil sampling can be logged on the same route. Over time, the numbers show which assets are drifting, supporting condition-based and predictive workflows without requiring a sensor on every machine.
- Log temperature, vibration and pressure as numeric values, not comments.
- Set alert thresholds so out-of-range readings create work automatically.
- Review trends by asset class, such as gearboxes or pumps, to spot patterns.
- Use inspection history to adjust preventive intervals up or down.
A 90-Day Rollout Path
Start small, prove value on a few critical areas, then expand. Wide rollouts across every unit at once tend to stall.
What to Look for in Steel Plant Inspection Software
When comparing a steel plant CMMS, test it against real routes rather than a sales script.
- Offline mobile use with reliable sync
- Asset hierarchy that mirrors plant areas and equipment
- Checklists with numeric limits, photos and required fields
- Automatic work orders from failed checkpoints
- Preventive scheduling tied to inspection results
- Lockout procedures and sign-off records on the work order
- Dashboards for completion, backlog and repeat failures
- Spare parts visibility from the work order
Frequently Asked Questions
Put Every Round, Finding and Lockout in One Workflow
Give steel plant technicians a mobile route that captures what they see, protects them during isolation and sends defects to planned work.