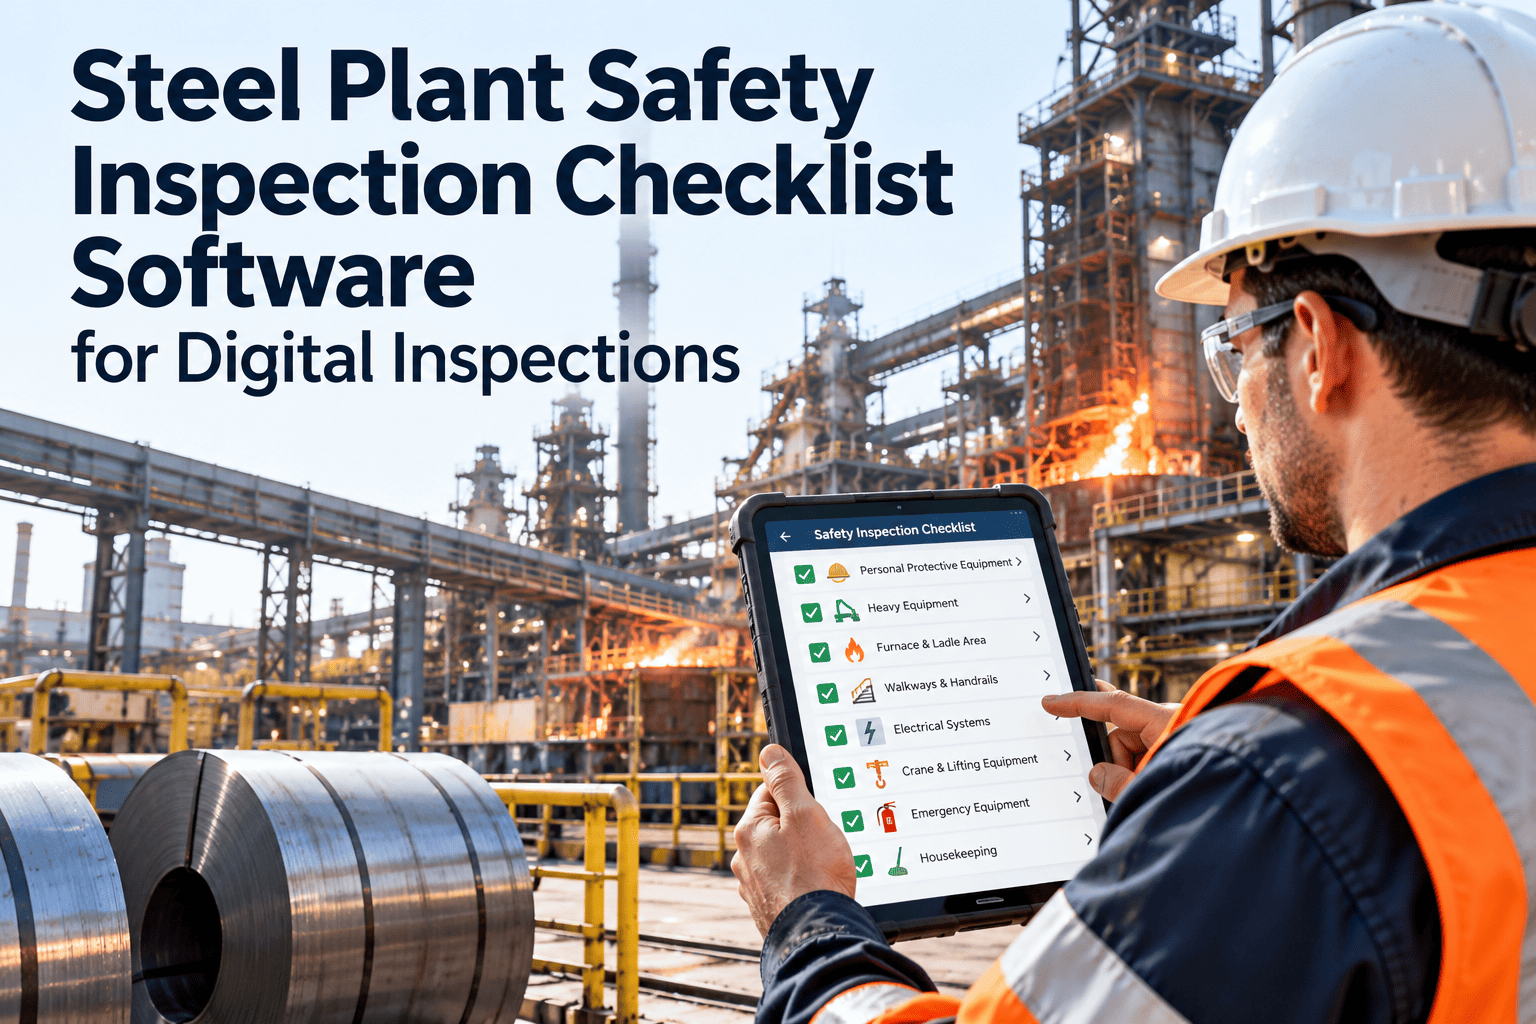
A steel plant combines molten metal, heavy lifting, high-pressure hydraulics, process gases and energised equipment in a single site, and every shift depends on inspections being done properly. When those inspections live on clipboards, hazards are noted late, isolation steps are hard to prove and experienced technicians take their knowledge home with them. A digital safety inspection checklist turns each round into a traceable record with owners, evidence and follow-up. This guide covers what to inspect, how to structure lockout/tagout, and how maintenance management software for steel plants keeps the whole workflow connected.
Steel Plant Safety Inspection Checklist Software for Digital Inspections
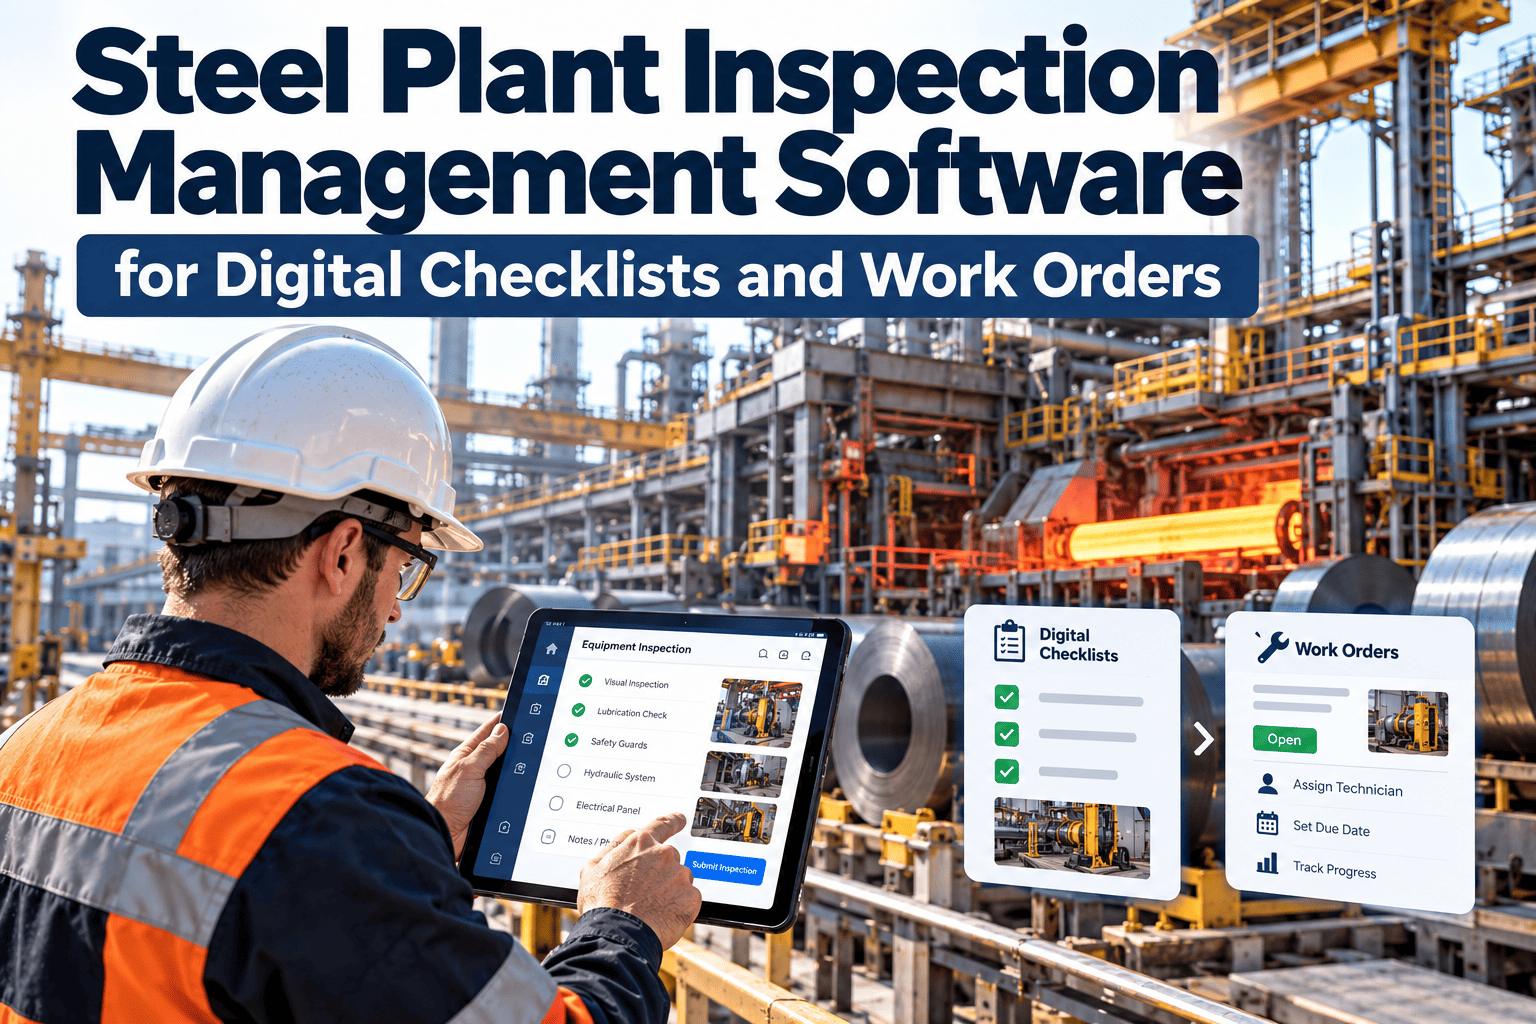
Replace paper rounds with mobile checklists that capture photos, readings, LOTO status and technician sign-off, then route every hazard straight into a work order for steel mills, melt shops and rolling lines.
Where Paper Safety Inspections Break Down in Steel Plants
Steel operations run continuously, in hot, noisy and dusty conditions where paperwork is the first thing to slip. The comparison below shows what changes when the same round is performed digitally.
Paper-based rounds
- Checklists filled at the end of the shift from memory
- Illegible handwriting and missing signatures
- Hazards reported verbally and never tracked
- No proof of who verified isolation, or when
- Audit preparation means searching through binders
- Contractors follow outdated procedure copies
Digital inspection workflow
- Time-stamped entries captured at the asset
- Mandatory fields that block incomplete submissions
- Failed checks create work orders with photos
- LOTO steps, locks and sign-offs stored per job
- Records retrieved by asset, date or inspector
- Current procedures attached to the task itself
Safety Inspection Checklist by Plant Area
Tick each point during the round. The frequency badge and owner show who checks it and how often, and each item can be configured as pass/fail, a reading or a photo. Use this as a starting framework and adapt it to your process route, whether electric arc furnace, basic oxygen furnace or integrated. Frequencies are typical starting points and should follow your own risk assessment and local regulations.
Melt shop and furnaces
Ladle and crane handling
Continuous casting
Rolling mill
Gas and utilities
Electrical rooms and MCCs
Hydraulic and lubrication systems
Conveyors and material handling
What Makes a Digital Inspection Point Usable
A checklist that technicians dislike gets skipped, so design matters as much as content. Well-built digital checklists share the following traits.
Clear pass or fail logic
- Binary questions where possible
- Numeric entry for pressures, temperatures and levels
- Acceptable limits shown beside the field
- Mandatory comment and photo on any failure
Asset-linked context
- QR or tag scan opens the correct checklist
- Last inspection result visible to the inspector
- Open work orders shown against the asset
- Reference photos of correct condition
Built-in escalation
- Stop-work flag for critical failures
- Automatic notification to the area supervisor
- Work order created from the failed point
- Re-inspection required before closure
Lockout/Tagout Workflow for Steel Plant Maintenance
Steel plants carry many energy types at once, so LOTO has to cover more than a single breaker. Attaching the procedure to the work order keeps every step visible and recorded.
Electrical, hydraulic and pneumatic pressure, gravity (suspended loads, rolls, ladle positions), process gas, steam, cooling water and thermal energy.
Operators, adjacent crews and contractors are informed before shutdown, with the notification logged on the job.
Equipment stopped using the machine-specific sequence, then isolation points opened, closed or blanked as listed.
Each authorised person applies a personal lock; lock IDs and names are recorded against each isolation point.
Accumulators bled, springs and suspended loads secured, then a try-start or zero-energy test confirmed before work begins.
Tools removed, guards refitted, locks removed by their owners and the area cleared before restart is authorised.
Under OSHA 1910.147, employers must also inspect energy control procedures at least annually. Storing each procedure, its revision history and the inspection record in one system makes this requirement far easier to evidence.
Risk Matrix: Turning a Finding into an Action
Not every failed check deserves the same response. Rows show likelihood and columns show consequence. A simple matrix lets inspectors classify findings consistently, so supervisors see what to address first. Response times shown are examples to adjust to your own policy.
Put Your Safety Rounds on a Single Platform
See how digital checklists, LOTO procedures and work orders connect in one maintenance workflow built for heavy industry.
Knowledge Management for the Maintenance Workforce
Many steel plants depend on a small group of veterans who know why a particular drive trips or which valve really isolates a line. Capturing that know-how protects safety as those people retire or move on.
Procedures at the point of work
- SOPs, drawings and isolation diagrams attached to the asset
- Version control so only the current revision is shown
- Required reading confirmed before a task is started
- Photos of correct set-up for tooling and guarding
Experience captured from the floor
- Technician notes recorded on every completed work order
- Failure causes tagged so repeat issues are visible
- Lessons from incidents linked to related checklists
- New hires and contractors guided by the same records
Compliance Records Your Inspections Should Produce
Regulations differ by country and site, so confirm requirements with your safety team. These are the records most steel plants are asked to produce during audits and after incidents.
Safety Inspection KPIs Worth Tracking
| KPI | How to calculate | What it tells you |
|---|---|---|
| Inspection completion rate | Completed rounds divided by scheduled rounds | Whether safety checks are really being performed |
| Finding closure time | Average time from failed check to verified close-out | How quickly hazards are removed |
| Overdue safety work orders | Open items past their due date by risk class | Where backlog is creating exposure |
| LOTO procedure currency | Procedures reviewed within the required period | Audit readiness for energy control |
| Repeat findings | Same asset and failure mode raised more than once | Root causes still unresolved |
| Near-miss reports per area | Count of reported near misses by location | Reporting culture and emerging risk zones |
How Oxmaint Supports Digital Safety Inspections
Oxmaint connects inspection results to the maintenance work that fixes them. Relevant capabilities for a steel plant include the following.
Inspections and mobile
- Configurable mobile checklists with photos, readings and signatures
- Scheduled rounds by area, shift and asset
- Failed points converted into work orders
Maintenance control
- Preventive maintenance schedules for safety-critical equipment
- Asset records with documents, history and spares
- Dashboards and reports for audits and reviews
Suggested rollout phases
Root Causes Behind Missed Safety Findings
When an incident investigation traces back to something an inspector could have seen, the cause is usually the process rather than the person. These are the patterns worth designing out.
| Root cause | How it shows up | Digital countermeasure |
|---|---|---|
| Inspection fatigue | Identical ticks on every shift, regardless of conditions | Numeric readings and photo prompts that make a blind tick impossible |
| Unclear acceptance limits | Inspectors disagree on what counts as worn or leaking | Reference photos and limits displayed beside each point |
| Delayed reporting | Hazards recorded hours later, with details lost | Entries time-stamped at the asset and sent instantly |
| Broken handover | Open defects not passed to the next shift | Open findings shown at the start of every round |
| Outdated procedures | Crews follow old isolation steps after a modification | Revision-controlled procedures attached to the work order |
| No feedback loop | Inspectors stop reporting because nothing happens | Status visible to the reporter until the finding is closed |
Shift Handover and Contractor Controls
Steel plants rely on outside crews for relines, crane repairs and shutdown work, and every handover is a chance for a safety assumption to be lost. Digital records make these transitions visible.
Shift-to-shift handover
- Open safety findings listed by area and severity
- Isolations still in force, with lock owners named
- Equipment running with temporary controls or bypasses
- Outstanding permits and their expiry times
- Notes from the outgoing supervisor attached to the round
Contractor management
- Site induction and competence confirmed before assignment
- Work orders issued with the exact procedure and permit
- Contractor locks recorded alongside plant personnel locks
- Completion photos and sign-off required before closure
- Performance and findings reviewed after the job
Moving from Routine Rounds to Condition-Based Safety
Once inspection data is digital, it can do more than prove that a round happened. Trends in the readings and findings help teams intervene before a hazard becomes an incident.
- Trend the readings. Hydraulic pressures, bearing temperatures and cooling water flows recorded every round reveal slow drift that a single reading would hide.
- Link findings to failure modes. Repeated hose abrasion or guard damage in the same area points to a design or layout issue worth fixing permanently.
- Prioritise by asset criticality. Cranes, ladles and gas systems deserve tighter inspection intervals than low-consequence equipment.
- Feed results into preventive maintenance. If an inspection regularly finds the same defect, adjust the interval or add a task rather than relying on the next round.
- Use condition data where available. Vibration, thermography and oil analysis results attached to the asset support predictive and condition-based decisions.
Common Mistakes When Digitising Safety Checklists
Audit Readiness: Questions Your Records Should Answer
After an incident or during an external audit, teams are asked to prove what was checked and what was done. A digital system should answer each of these without a search through folders.
- Who inspected this crane, ladle handling area or gas line last, and what did they record?
- Which findings were raised in the past quarter, and how long did each take to close?
- Who applied locks on a specific job, and when were they removed?
- Which version of the isolation procedure was in force on the day of the work?
- Were any overdue safety tasks active on the equipment involved?
Frequently Asked Questions
What should a steel plant safety inspection checklist include?
It should cover every hazard zone, from melt shop and cranes to gas lines and conveyors, with specific pass or fail points, numeric readings and photo evidence. Each point needs an owner, a frequency and a clear escalation path for critical findings, so a failed check becomes action rather than a note.
Can digital checklists support LOTO procedures?
Yes. Isolation points, lock owners, energy release steps and verification checks can be attached to the work order and stored as a permanent record. This helps demonstrate periodic procedure inspections and shows who applied and removed each lock. You can book a demo to see the workflow in practice.
Do technicians need connectivity to complete inspections?
Coverage in melt shops, basements and pits is often patchy, so confirm that a platform supports offline capture and later synchronisation before rollout. Inspectors should be able to complete a round, attach photos and save results on the device, then upload everything once they return to a covered area.
How do inspections link to corrective maintenance?
A failed checklist point can create a corrective work order that carries the photo, location, asset and severity from the inspection. Planners then see the defect with context, assign the right trade and schedule it, and the finding is only closed after the repair is verified, rather than relying on a verbal handover.
How can we start without disrupting production?
Begin with one area and your highest-risk assets, such as cranes or gas systems, and convert the paper checklists your crews already use. Run a short pilot, gather inspector feedback, then extend area by area. You can sign up and configure a first checklist quickly.
Make Every Safety Inspection Traceable
Move from paper rounds to digital inspections, linked LOTO records and faster hazard closure across your steel plant.