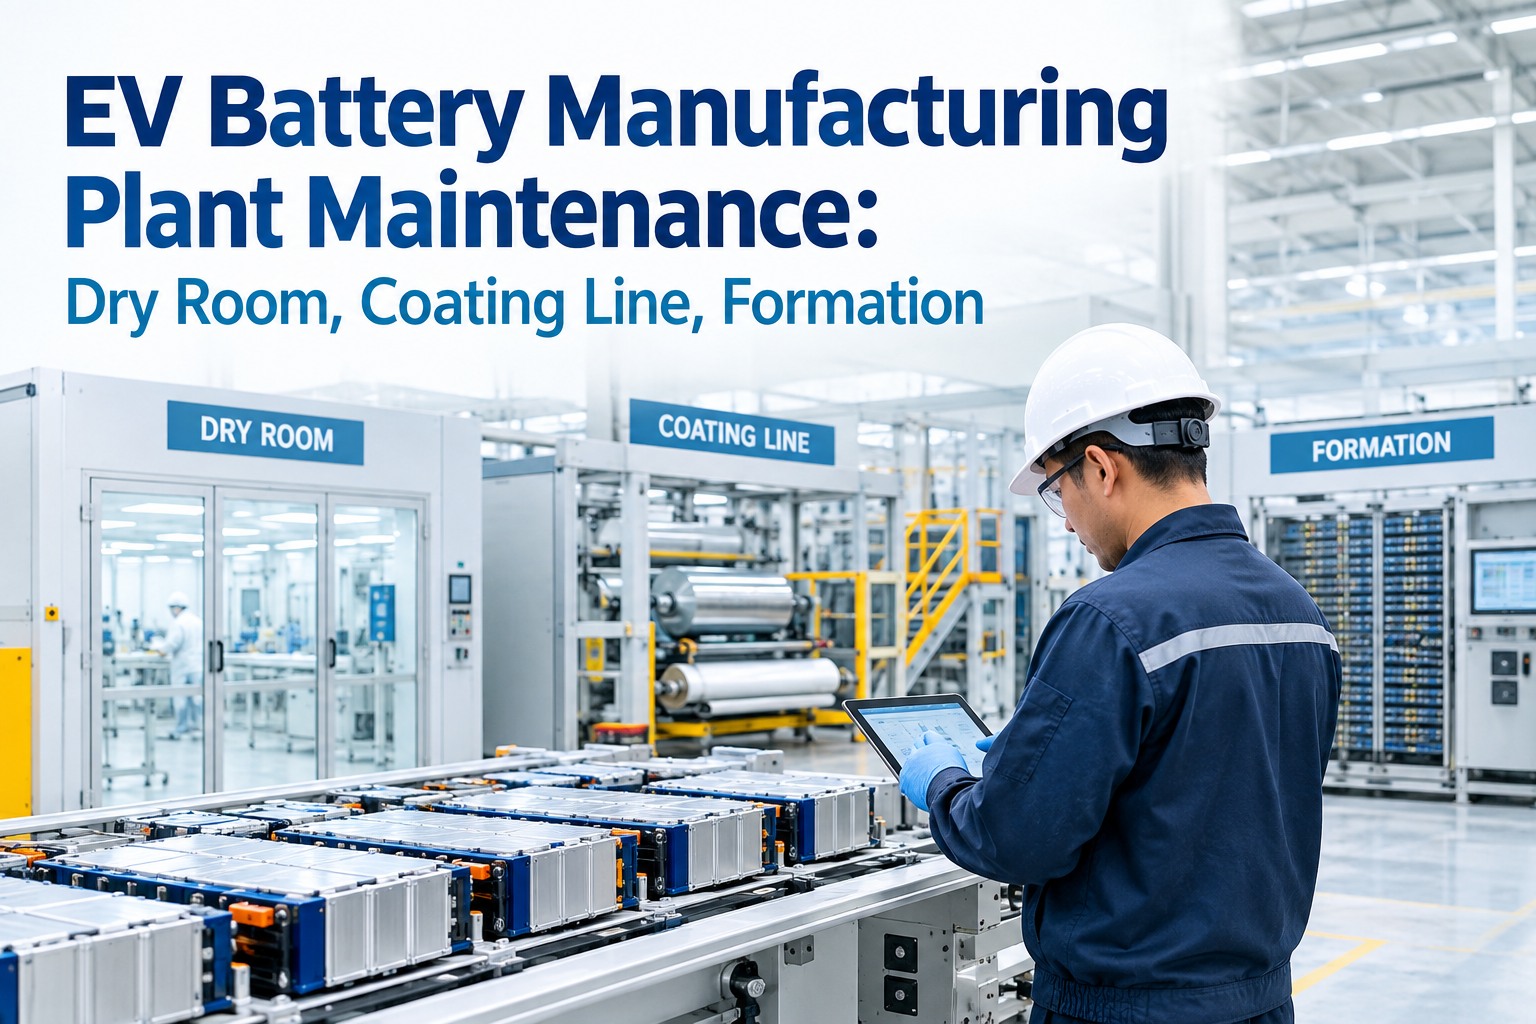
A gigafactory is not one factory — it's a chain of radically different environments, each hostile to equipment in its own way, and each capable of scrapping a batch the moment its conditions drift. The dry room holds air at a dewpoint below −40°C, drier than any desert, because lithium reacts violently with trace moisture. The coating line lays electrode slurry to micron tolerances at high speed. The formation area cycles thousands of cells for up to three weeks straight — the single most expensive step in the whole plant. Ordinary plant maintenance doesn't survive here; the failure modes and the cost of downtime are unlike anything in conventional manufacturing, which is why gigafactories run on purpose-built maintenance management software. This guide walks the maintenance profile of each critical zone, and how OxMaint's platform keeps a GWh-scale line running. Start free on OxMaint or book a demo.
Gigafactory · Dry Room · Coating · Formation
EV Battery Manufacturing Plant Maintenance: Dry Room, Coating Line, Formation
Three zones, three completely different maintenance regimes. Get any one wrong and cell chemistry, yield, or safety pays for it. Here's how each critical area actually fails — and stays running.
−40°C
Dry room dewpoint, down to −60°C for moisture-sensitive chemistries
32.6%
Of manufacturing cost sits in formation & aging alone
>75%
Of plant energy consumed by drying & the dry room
1.5–3wk
Formation cycling time — the longest, costliest step in the line
Why a Gigafactory Breaks the Maintenance Rulebook
In a normal plant, a machine fault stops one machine. In a gigafactory, an environmental drift ruins product that already passed through — silently, across an entire shift. Moisture that sneaks past a failing desiccant rotor doesn't trip an alarm; it shows up weeks later as capacity loss in formation, or worse, as a cell that fails safety testing. That inversion — where the utility systems are more production-critical than the production machines — is what makes gigafactory maintenance its own discipline, and why a purpose-built maintenance management platform like OxMaint matters here more than in a conventional plant: it holds every zone's assets, conditions, and PM in one system of record so an invisible drift becomes a tracked work order. The three zones below carry the bulk of that risk.
01
Dry Room & Dehumidification
The environment IS the product spec
Multi-stage desiccant dehumidification — twin-tower lithium chloride and silica gel rotors — holds the room below −40°C dewpoint and under 1% RH. This system, not any single machine, is the plant's most production-critical asset.
02
Coating & Calendering Line
Micron tolerances at speed
Electrode slurry coated and dried to precise thickness, then calendered. Coating-head alignment, tension control, and drying-oven stability decide electrode uniformity — and coating/drying is ~15% of manufacturing cost.
03
Formation & Aging
The most expensive step in the plant
Thousands of cells charge-discharge cycled over 1.5–3 weeks on formation cyclers, then aged. At 32.6% of manufacturing cost, cycler uptime and channel accuracy directly govern plant throughput and yield.
Zone 1 — Keeping the Dry Room Dry
The dry room is a utility system masquerading as a building, and its maintenance is relentless because failure is invisible until product is already compromised. Redundancy is designed in — N+1 desiccant configuration — but redundancy only helps if the standby is maintained and the monitoring is trusted, which is exactly the discipline OxMaint's maintenance management software enforces: dewpoint-linked PM on every rotor and a scheduled, logged test on the standby train so nothing is left to assumption.
Desiccant Rotor Health
Lithium chloride and silica gel rotor performance, reactivation-heater function, and seal integrity — the core of dewpoint control.
Continuous Dewpoint Monitoring
Real-time dewpoint and RH sensors with alarm thresholds — the early-warning system before moisture reaches product.
N+1 Redundancy Verification
The standby train tested and ready, not assumed. A failed rotor with an unmaintained backup is a whole-shift loss.
Make-Up Air & Chilled Water
Make-up air handling and the chilled-water plant feeding dehumidification — the supporting utilities the dewpoint depends on.
Make the Dry Room a Monitored Asset — Free Forever
Load every rotor, sensor, air handler, and chilled-water asset into OxMaint with dewpoint-linked PM and condition alarms. When a rotor trends toward failure or the standby train misses its test, a work order opens before moisture ever reaches a cell. No card, no time limit.
Zone 2 — Precision on the Coating Line
Coating is where microns become megawatt-hours. A drift in coat weight or a streak from a fouled die propagates into every downstream cell, and because the line runs fast and continuous, a small defect becomes a large scrap pile quickly. Maintenance here is about holding tolerance, not just preventing breakdown — the kind of condition-linked PM OxMaint triggers from coat-weight and tension data rather than a fixed calendar, so a drift is caught before it becomes a scrap pile.
Coating-Head & Die Precision
Slot-die cleanliness, alignment, and shim condition — the difference between uniform coat weight and streaked scrap.
Web Tension & Roller Alignment
Tension control and roller condition keep the foil web stable — wander and wrinkles are direct yield losses.
Drying-Oven Stability
Zone temperature uniformity and airflow balance in the drying tunnel — inconsistency changes solvent removal and adhesion.
Calender Roll Condition
Roll surface, gap control, and bearing health set final electrode density — a maintained calender protects capacity.
Zone 3 — Uptime Where It Costs Most
Formation ties up a cell for up to three weeks and consumes a third of the plant's manufacturing cost. Every hour a cycler channel is down, a paid-for cell sits idle in the most capital-intensive step of the line. This is where maintenance most directly converts into throughput — and where OxMaint's software earns its place, tracking cycler-channel uptime and calibration so the plant's most expensive step never quietly loses capacity to a down channel.
Cycler Channel Accuracy
Calibration of charge-discharge channels — drift here mis-forms cells and corrupts the data the whole step relies on.
Thermal & Cooling Management
Cooling that removes cycling heat — and heat-recovery systems that reclaim it — keep cells in spec and cut energy cost.
Power Electronics & Contacts
Cycler power stages and contact integrity across thousands of channels — the highest-count failure surface in the plant.
Safety & Fire Suppression
Thermal-runaway detection and suppression on the cycling floor — non-negotiable safety-critical PM, tested and logged.
The Cross-Plant Layer: Motors, VFDs, Utilities
Beneath all three zones runs the same backbone — VFD-driven motors on every load, chilled water, compressed dry air, and the substation. These are conventional assets, but at gigafactory scale their reliability sets the ceiling for everything above — so OxMaint runs them on the same maintenance management platform as the critical zones, calendar PM for the backbone alongside condition triggers for the product-critical systems.
VFDs & Motors
Variable-frequency drives across all motor loads — the efficiency layer that also carries single points of failure.
Chilled Water & CDA
The chilled-water plant and compressed dry air feeding dry rooms, coating, and formation alike.
Heat Recovery
Recovered formation heat feeding back into the plant — an energy asset that needs its own PM to keep paying off.
Substation & Power
HV substation and distribution — the whole plant's uptime rests on it, so its maintenance is plant-critical.
How OxMaint Runs Gigafactory Maintenance
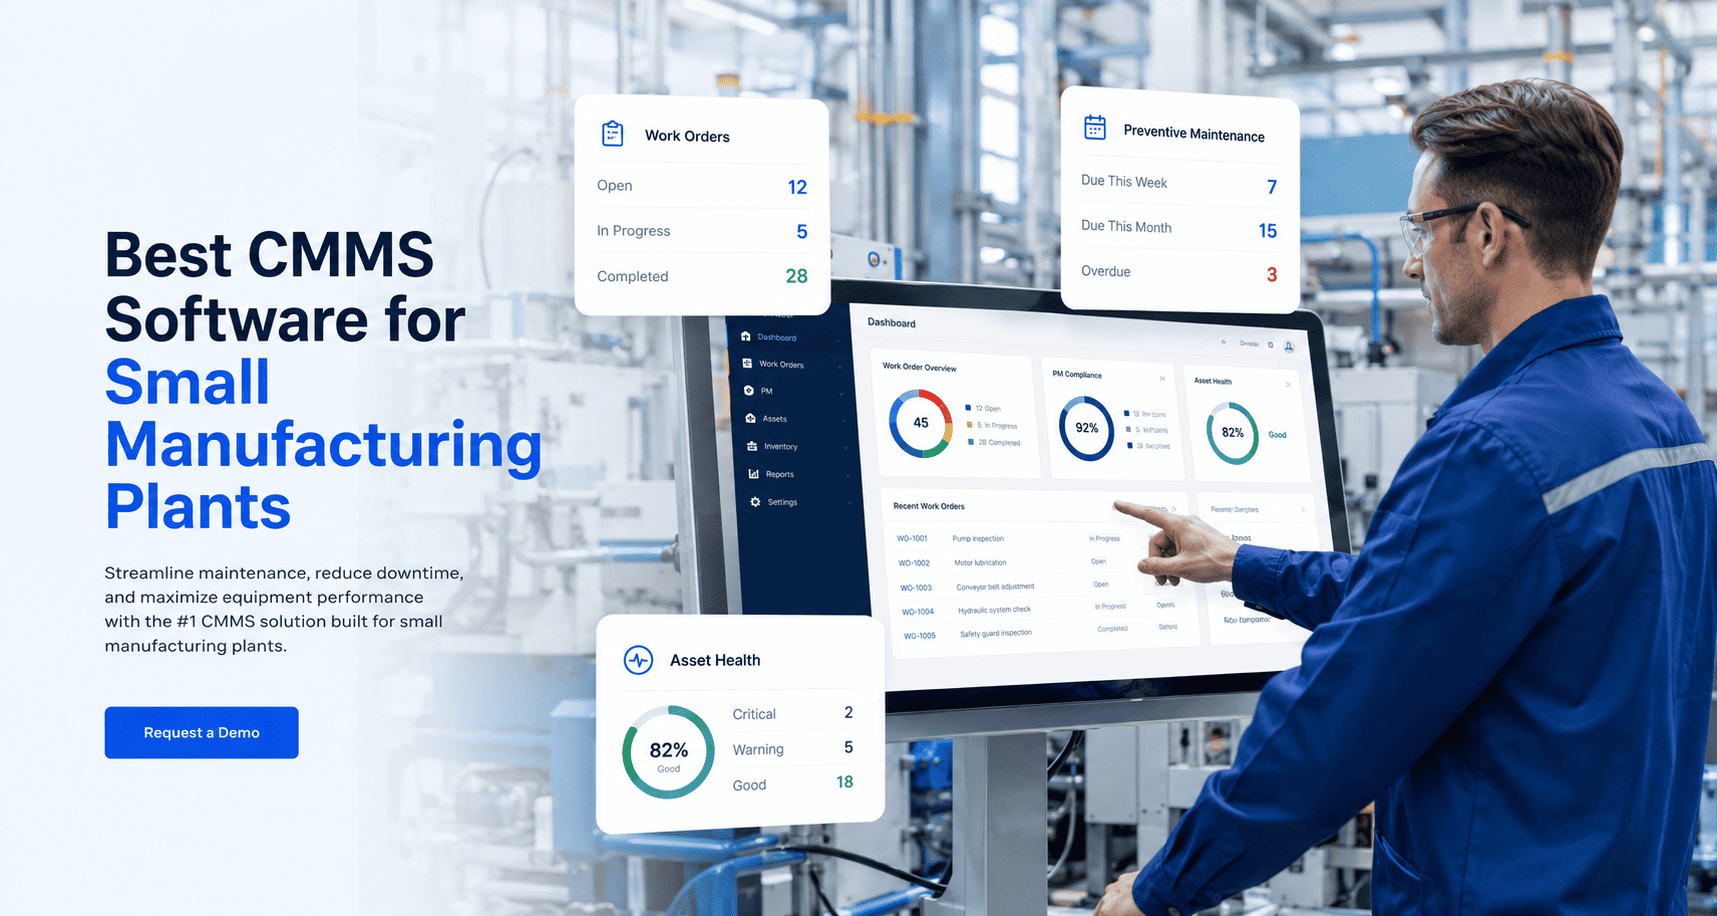
A structured asset hierarchy per zone, condition-linked PM, mobile execution, and audit-ready reliability records on one AI-native platform — so the dry room, coating line, and formation area each run to their own regime while leadership sees one plant-wide reliability picture.
Structure
Zone Asset Hierarchy
Every rotor, coating head, cycler channel, and utility mapped by zone — parent-child down to the component.
Trigger
Condition-Linked PM
Dewpoint, coat-weight, and cycler-calibration thresholds drive PM — maintenance fired by process data, not just calendar.
Monitor
IoT & Sensor Alarms
Real-time dewpoint, temperature, and vibration streamed in, alarming before a drift reaches product.
Execute
Mobile Work Orders
Technicians close jobs from the floor with full asset history — even inside gowned dry-room protocols.
Protect
Safety-Critical PM
Thermal-runaway and suppression checks scheduled, tested, and logged — never a missed safety inspection.
Report
Plant Reliability KPIs
Uptime, OEE, and energy trends by zone rolled up for plant and reliability leadership.
Give Every Zone the Regime It Needs
Free forever plan — no card, no time limit. Structure your dry room, coating line, and formation area as distinct maintenance regimes, trigger PM from process data, and keep safety-critical checks audit-ready. Or book 30 minutes and we'll map your gigafactory onto the platform end to end.
Frequently Asked Questions
Why is dry room maintenance so critical in a battery plant?
Because lithium reacts with trace moisture, and dry room failure is invisible until product is already ruined. The room holds a dewpoint below −40°C — under 1% RH — so a degrading desiccant rotor doesn't trip a machine alarm; it shows up weeks later as capacity loss or a cell that fails safety testing. That's why the dehumidification system, not any production machine, is the plant's most production-critical asset.
Start free to monitor it.
Which zone carries the most maintenance risk?
It depends how you measure it. The dry room is the most production-critical because its failure silently ruins product. Formation and aging carry the most cost — about 32.6% of manufacturing cost and up to three weeks per cell — so downtime there is the most expensive. Coating sits between: fast, continuous, and unforgiving of tolerance drift. A good program runs all three as distinct regimes, not one generic schedule.
How does formation maintenance affect plant throughput?
Directly. Formation cycling ties up each cell for 1.5–3 weeks in the most capital-intensive step, so every hour a cycler channel is down leaves a paid-for cell idle in the bottleneck. Channel calibration accuracy, power-electronics reliability, and cooling uptime govern how many cells the plant can form at once — which is the throughput ceiling for the whole line.
Book a demo to see cycler uptime tracked.
Can standard CMMS PM schedules work for a gigafactory?
Only partly. Calendar PM handles the conventional backbone — motors, VFDs, utilities — but the critical zones need condition-linked triggers tied to process data: dewpoint for the dry room, coat weight for coating, channel calibration for formation. The best programs blend both, so ordinary assets run on schedule while the product-critical systems respond to real conditions.
Why does energy monitoring belong in the maintenance program?
Because drying and the dry room alone consume over 75% of plant energy, and formation heat is often recovered and reused. That makes efficiency a maintenance outcome: a fouled coil, a drifting VFD, or an underperforming heat-recovery loop quietly raises energy cost. Tracking energy trends by zone alongside uptime turns maintenance into an energy-cost lever, not just a downtime one.