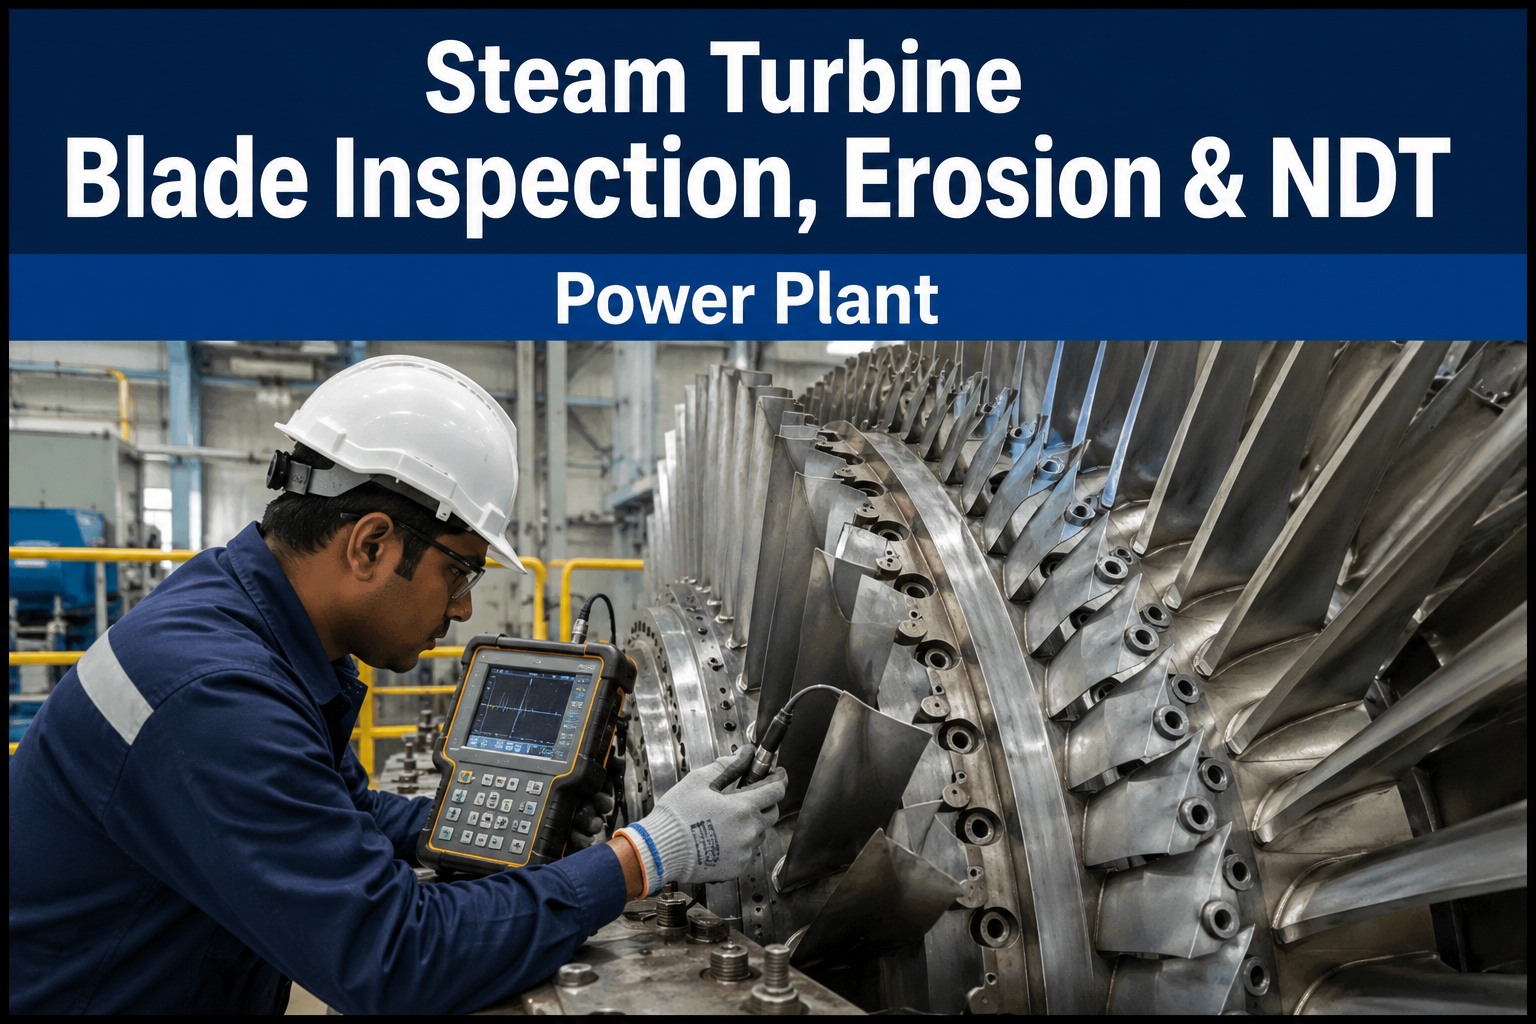
Steam turbine blade inspection is where outage planning either protects the machine or misses the crack that becomes a forced outage. This guide is written for power plant maintenance and reliability managers who own turbine blade NDT scope, erosion trending, and blade replacement decisions. It covers turbine blade erosion measurement, eddy current testing, LP blade cracking mechanisms, and practical repair-versus-replace criteria. If you want blade-level history and NDT results tied to asset records, start a free trial or book a demo to see how OxMaint supports turbine outage execution.
Steam Turbine Blade Inspection: Erosion, Cracking & NDT in Power Plants
A rigorous blade inspection program is not “visual checks during overhaul.” It is a measurable system: quantify leading-edge erosion, detect surface cracks early with eddy current testing, understand LP blade cracking drivers, and make replacement decisions before risk outruns the outage window.
What “good” looks like in a blade inspection program
A defensible program ties each inspection method to a specific failure mode and produces results you can trend by blade row, stage, and location. The output is not a report—it is decisions: run, monitor, repair, or replace.
- Turbine blade erosion (leading edge, moisture impingement, solid particle erosion where applicable)
- Turbine blade cracking (fatigue initiation, stress corrosion cracking in LP wet steam)
- Foreign object damage (FOD), rubbing, and tip shroud interactions
- Eddy current testing (ECT) for surface-breaking cracks in airfoils and root serrations (where geometry allows)
- Dimensional/erosion measurement for leading-edge loss and profile change
- Supplemental PT/MT/UT based on blade design and access
- Record by blade position and row (not “LP rotor checked”)
- Set acceptance criteria tied to OEM guidance and engineering evaluation
- Pre-plan repair/replace paths to protect the outage schedule
Turbine blade erosion: measurement techniques and acceptable wear limits
Erosion is a performance and integrity issue: it changes blade profile, reduces stage efficiency, and can accelerate local stress risers. The goal is consistent measurement locations and a repeatable method so the trend is meaningful.
Common erosion measurement methods
- Template/profile comparison against OEM blade profile gauges at defined chordwise stations
- Leading-edge thickness measurement using calibrated micrometers or dedicated blade gauges
- Blade-to-blade mapping for the worst quadrant (often where moisture concentration is highest)
- Photogrammetry/3D scanning where the plant has tooling and repeatable fixturing
Trend “loss per operating hour” and “loss per start” separately. Starts and load swings often correlate with moisture and shedding events that accelerate leading-edge wear.
Acceptable wear limits (practical approach)
Acceptable limits must come from the OEM and/or an engineering evaluation, but the decision logic is consistent:
- Run / monitor: erosion within OEM allowance, stable trend, no crack indications
- Repair: erosion approaching limit but restorable by approved weld/build-up and re-profiling
- Replace: beyond allowable material loss, distorted geometry, or repeated repair history with diminishing life
Where plants get hurt is “accepting” a single reading without a trend line or without tying it to the specific blade row and location.
Eddy current testing (ECT) for turbine blade NDT: procedure that holds up in an outage
ECT is the workhorse for surface crack detection on many blade designs, especially when you need fast screening with strong sensitivity to tight, surface-breaking flaws. The procedure must be controlled: probe selection, calibration, scan plan, and documentation.
Prioritize LP stages, known crack-susceptible rows, high-stress attachment features, and any blades with abnormal operating history (water induction, trips, overspeed events).
Use a reference standard with representative EDM notches in similar geometry/material. Confirm lift-off compensation and sensitivity at the tightest radius you must inspect.
Document scan direction, overlap, and indexing method (blade number, row, side). For airfoils, define zones (leading edge, trailing edge, suction/convex, pressure/concave).
Set rules for re-scan, confirmation with PT/MT where appropriate, and engineering disposition. Record signal amplitude/phase and location photos for traceability.
ECT fails as a “checkbox” when the crew is rushed, the blade numbering isn’t controlled, or results aren’t captured in a way that supports trending and follow-up. Treat data capture as part of the inspection method.
LP blade inspection: cracking mechanisms you must plan for
LP blades operate in wet steam where moisture droplets and corrosive chemistry can combine with cyclic stresses. The inspection plan should explicitly address the mechanisms that drive LP blade cracking.
Leading-edge erosion changes local geometry and can create stress risers. Under cyclic loading, small defects can transition into fatigue initiation sites.
Chlorides, caustic, or other contaminants (depending on cycle chemistry) plus tensile stress can drive SCC, especially in crevices, roots, and under deposits.
Corrosive environment reduces fatigue strength; cracks can initiate earlier and grow faster than “clean” fatigue predictions.
Where to focus LP blade inspection
- Last-stage and next-to-last-stage blades (highest moisture and largest annulus area)
- Blade root attachments and contact surfaces (fretting + stress concentration)
- Leading edges and any repaired zones (weld HAZ can be a crack initiator)
- Areas with deposit history or chemistry excursions (tie findings to water chemistry events)
Blade replacement vs repair: decision criteria that prevent forced outages
The best plants treat blade disposition as a controlled decision with thresholds, not a debate in the middle of the outage. Use a matrix that combines NDT results, erosion trend, repair history, and remaining life.
| Decision driver | Repair is reasonable when… | Replace is safer when… | Data you should have |
|---|---|---|---|
| Crack indication (ECT/PT) | Small, isolated, and OEM-approved blend/repair exists with proven success | Multiple indications, crack in high-stress zone, or uncertain sizing/depth | Indication map, photos, signal data, prior findings, engineering evaluation |
| Leading-edge erosion | Within allowable loss; profile restorable; trend stable | Beyond allowable loss, severe distortion, or repeated re-profiling | Station-by-station measurements, trend rate, OEM limits |
| Root / attachment condition | Fretting minor; no crack; contact restored within spec | Cracking, heavy fretting, or loss of fit that compromises damping/strength | Root NDT results, fit checks, torque/clamping records (as applicable) |
| Repair history | First repair, controlled process, good post-repair performance | Multiple repairs, recurring indications, or unknown weld procedure lineage | Blade-level repair log, procedure references, post-repair NDT |
| Outage constraints | Repair turnaround fits critical path with QA hold points | Repair risk threatens schedule; replacement parts available | Lead times, spares status, vendor capacity, lift plan |
Set “engineering review triggers” below the hard OEM limit (for example: % of allowable erosion consumed, or any new crack indication). That creates time to plan parts and labor before the next outage becomes an emergency.
Aligning blade inspection intervals with major outage planning
Blade NDT scope should be built backward from access and critical path. The right interval is the one that catches damage early enough to plan repairs without compressing the outage schedule.
Typical planning inputs
- OEM recommended inspection intervals by row/stage and duty cycle
- Operating profile: starts, hours, load swings, water chemistry excursions
- Known fleet issues for the blade design (service bulletins, fleet experience)
- Previous findings: erosion trend, crack history, repair locations
Outage-ready NDT scope checklist
- Blade numbering convention and mapping template locked before disassembly
- ECT procedure, calibration blocks, and qualified personnel confirmed
- Hold points defined: indication confirmation, engineering disposition, repair release
- Data capture plan: photos, measurements, and results stored to asset records
How OxMaint supports blade lifecycle decisions (blade-level CMMS records)
OxMaint helps reliability teams treat blades as trackable assets, not a single “turbine” work order. That means blade-level inspection history, NDT results, and thresholds that trigger action before risk becomes a forced outage.
Store blade row, position, serial/ID (where applicable), repair history, and inspection results as searchable records tied to the turbine asset hierarchy.
Attach ECT reports, indication maps, photos, and erosion measurements to the exact blade and outage—so trending is possible across cycles.
Plan eddy current and erosion checks against outage windows, assign tasks, and track completion with QA hold points and sign-offs.
Flag blades approaching replacement thresholds (erosion allowance consumed, recurring indications) so parts and engineering review happen early.
Keep dispositions, approvals, and vendor repair documentation linked to the blade record for defensible decisions and future planning.
Build a clear view of repeat findings, worst rows, and risk concentration to prioritize next outage scope and budget.
FAQ: steam turbine blade inspection & NDT
What is the best NDT method for steam turbine blade inspection?
For surface-breaking cracks, eddy current testing (ECT) is often the primary screening method because it is fast and sensitive on many blade geometries. Plants commonly supplement with PT/MT for confirmation and UT where geometry and access support volumetric examination.
How do you measure turbine blade erosion in a repeatable way?
Use fixed measurement stations (same chordwise locations each outage), calibrated gauges or templates, and consistent blade numbering. Record results by blade row and position so you can trend loss rate and identify localized moisture-driven wear patterns.
Why do LP blades crack more often than HP/IP blades?
LP blades see wet steam and higher moisture content, which increases erosion and can support corrosion-related mechanisms. Combined with high cyclic stresses and long blade lengths, LP stages are more susceptible to fatigue, corrosion fatigue, and stress corrosion cracking depending on chemistry and operating history.
When should a blade be repaired versus replaced?
Repair is typically reasonable when damage is within OEM allowances, the repair process is approved and proven, and the blade has limited prior repair history. Replacement is safer when cracks are in high-stress regions, erosion exceeds allowable limits, geometry is distorted, or repeated repairs indicate diminishing remaining life.
How does a CMMS help with turbine blade NDT and outage planning?
A CMMS like OxMaint keeps blade-level inspection history, NDT reports, photos, and measurements tied to the asset record, then schedules recurring eddy current and erosion checks against outage windows. It also supports threshold-based flags so blades approaching replacement criteria are identified early enough to plan parts, labor, and engineering review.
Make blade risk visible before the outage does
If your team owns turbine blade NDT scope, OxMaint gives you blade-level traceability: erosion trends, ECT results, dispositions, and replacement thresholds—organized for outage execution and long-term reliability.