On a Swiss-type lathe, precision does not live in the control — it lives in a spinning guide bushing a few millimetres from the cut. A bushing adjusted a hair too loose, a bar feeder a shade out of line, or neat cutting oil thick with tramp oil, and your medical and aerospace parts drift out of tolerance before anyone sees a scrap light. This guide lays out a preventive maintenance schedule built for the sliding-headstock machine — and shows how OxMaint AI maintenance management software turns it into live PM routes that fire before tolerance slips. Book a demo to see it on your machines.
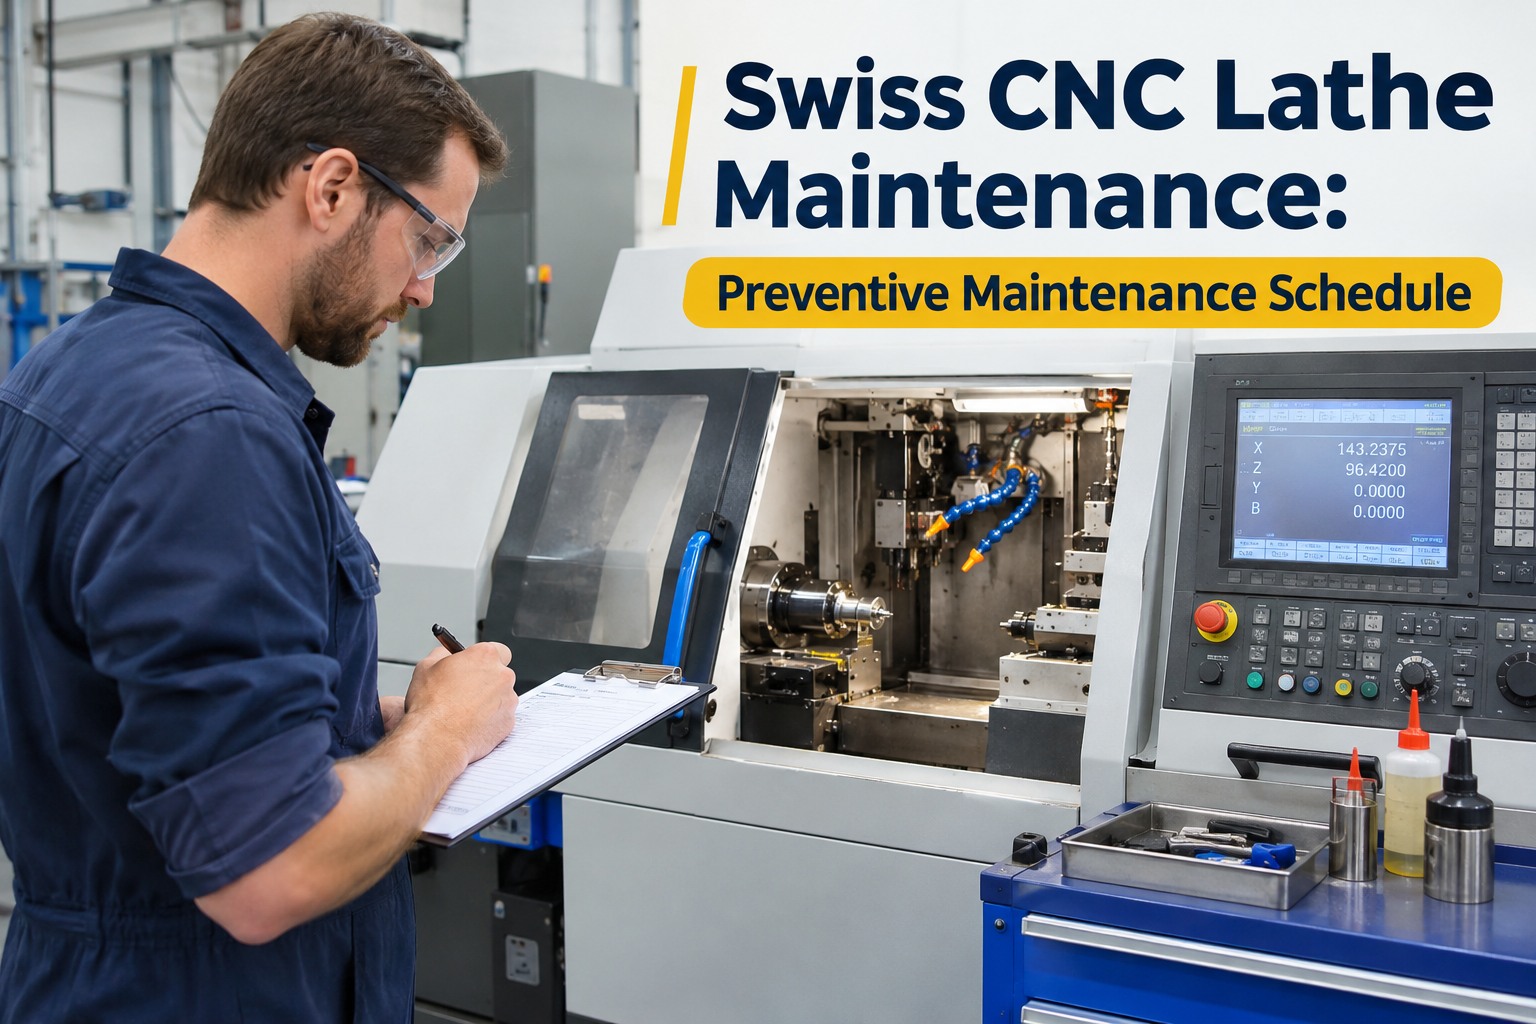
Swiss CNC Lathe Maintenance: The Preventive Maintenance Schedule
A Swiss lathe feeds rotating bar stock through a guide bushing right at the point of cut — so its wear points are nothing like a chucker's. OxMaint AI is the maintenance management software that follows that material path, from bar feeder to finished part, and turns every check into meter-and-time PM routes that fire before quality slips, not after.
A Swiss-type doesn't grip an overhung bar in a chuck — a sliding headstock pushes rotating stock through a guide bushing that supports it millimetres from the tool. That moves the wear onto parts a generic checklist skips: the bushing, the bar-feed channel, and the neat oil that lubricates both. OxMaint AI maps each to its own PM route, so the schedule gets done, not just posted.
Conventional Lathe
Bar clamped in a chuck, workpiece overhung
Collet and chuck are the main wear points
Usually runs water-soluble coolant
Length-to-diameter ratio is limited by deflection
Swiss-Type Lathe
Guide bushing supports stock at the point of cut
Bushing, bar feeder and sliding slides wear first
Typically runs neat (straight) cutting oil
Handles L:D ratios well beyond 3:1 without chatter
THE DEFINING COMPONENT
The Guide Bushing Is Where Your Tolerance Lives
The guide bushing's adjustment and condition are the biggest factors in holding size. Set it by feel — a light drag, not spin-free, not press-fit. Since ground bar stock varies bar to bar, operators reset it for each new bar, which is why "check guide bushing" is a daily line — and why OxMaint AI puts it on the daily route automatically.
TOO LOOSEOversize parts, dimensional drift, marring
CORRECT DRAGLight, even resistance — stock spins with the bushing
TOO TIGHTPress-fit, heat build-up, chatter, scored bars
Worn bushing bearings or a mismatched bushing-to-bar size will chatter no matter how it is set — log each adjustment in OxMaint AI and a recurring chatter becomes a wear trend you can see, not a surprise.
The Preventive Maintenance Schedule by Interval
Hit the right task at the right interval across the whole material path. Rows are the subsystems that fail; columns are how often each needs attention. OxMaint AI holds every cell as a scheduled route, so nothing slips at shift change. Start free and build these routes against every Swiss asset.
Subsystem
Daily
Weekly
Monthly
Quarterly
Annual
Guide bushing
Bar feeder & channel
Cutting oil (neat)
Spindle & collet
Slides & lubrication
Air & hydraulics
Mist collector & filters
Scheduled task Inspect / as-needed Not required
What Each Subsystem Needs — and How OxMaint AI Helps
The grid tells you when; these cards tell you what — plus the OxMaint AI feature that keeps each one on track.
Guide Bushing
Check clearance and drag on every new bar. Clean the mill grease off incoming stock, verify lubrication, and log bearing wear weekly. Match bushing size to bar — a mismatch chatters.
In OxMaint AI: a daily digital check plus a bushing adjustment and wear log per machine.
Bar Feeder & Channel
Keep the oil-filled channel clean and topped to spec viscosity so the bar rides a stable film. Confirm feeder-to-spindle alignment, check for scoring, and grease fittings on interval. Power off the lathe first.
In OxMaint AI: feeder PM routed with the lathe, with alignment and grease on their own intervals.
Cutting Oil (Neat)
Swiss machines run straight oil, not water-soluble coolant. Low-maintenance, not no-maintenance: skim tramp oil, filter metal fines, and watch oil temperature so viscosity holds. Keep flow steady at the cut.
In OxMaint AI: a dated oil log — skims, filtration and change-outs captured with readings.
Spindle & Collet
Clean and inspect collets weekly for grip and wear; check the spindle liner for debris and run-out. A tired collet shows as part-to-part size variation before it fails — trend it, don't wait for scrap.
In OxMaint AI: collet and spindle checks trended per asset, so wear is caught before scrap.
Slides & Lubrication
The sliding headstock and cross slides depend on clean way lube. Check reservoir level and pump flow, wipe and inspect ways for swarf, and refresh oil on schedule to protect positioning accuracy.
In OxMaint AI: lube checks and oil refreshes scheduled to protect positioning accuracy.
Air, Hydraulics & Mist
Check air and hydraulic pressure against set points daily, drain separators, and service the oil-mist collector and filter. A clogged mist collector on a straight-oil machine is a quality and fire risk — treat its filter as a safety item.
In OxMaint AI: the mist-filter service flagged as a recurring safety-critical PM.
The Warning Signs — Caught Early, Routed Fast
Most Swiss problems show at the part before they stop the spindle. Operators raise these from the floor in OxMaint AI with a photo, and each becomes a ranked work order routed to the right tech.
!
Chatter & Poor Finish
Worn bushing bearings, a loose bushing, or a bushing-to-bar mismatch vibrating at the cut.
!
Dimensional Drift
Diameters creeping out of size usually trace back to a too-loose bushing or a tired collet.
!
Bar Feed Stall or Noise
Low channel oil, misalignment, or scored channels breaking the bar's supporting oil film.
!
Short Tool Life
Degraded or contaminated cutting oil losing lubricity as tramp oil shifts its viscosity.
!
Oil Mist & Heat
A loaded mist collector smoking or overheating — a quality defect and a fire hazard at once.
!
Positioning Errors
Sticky slides or starved way lube showing up as step marks and lost repeatability.
Hold Microns, Not Hope.
A Swiss schedule only protects tolerance when every bushing check, oil skim and alignment lands on time, on the record. OxMaint AI maintenance management software runs the whole route off meter and time triggers, so the task fires before the part drifts — and the history is there when your medical or aerospace audit asks.
OxMaint AI is the AI-powered maintenance management software that carries a Swiss lathe from an operator squawk to a closed, recorded work order — with meter-based PM, per-machine checklists and asset history built into the workflow. Book a demo and see a Swiss PM route run end to end.
Meter & Time Triggers
PM routes fire on spindle hours or the calendar — daily bushing checks, weekly oil skims, annual overhauls — so nothing waits for memory.
Per-Machine Checklists
Each Swiss asset carries its own digital route with the exact bushing, feeder and oil tasks for that model, not a generic lathe list.
Guide-Bushing Log
Record adjustment, bearing wear and bushing changes against the asset, so recurring chatter becomes a trend you can see and act on.
Cutting-Oil Tracking
Log oil checks, skimming, filtration and change-outs with readings, turning "it smells off" into a dated maintenance record.
Squawk to Work Order
Operators raise chatter or a feed stall from the floor with a photo; it becomes a ranked work order routed to the right tech.
Audit-Ready History
Every task, part and sign-off kept per machine — the evidence trail a medical or aerospace quality audit asks for first.
EXPERT REVIEW
Written for machinists and maintenance leads running sliding-headstock Swiss-type lathes in precision work — medical, aerospace, micro-components. The intervals here are a general framework; your authoritative schedule is the machine builder's manual for your specific model and bar feeder, which sets the exact lubricants, viscosities and pressures. OxMaint AI structures and records the PM workflow — it doesn't replace your builder's manual, operator training, or your quality team's call on tolerance.
Frequently Asked Questions
How often should a Swiss lathe guide bushing be checked?
Daily, and in practice on every new bar. Ground bar stock varies slightly in diameter from bar to bar, so the bushing clearance that gave the right drag on the last bar may be too loose or too tight on the next. A quick feel-check at bar change, plus a weekly inspection of the bushing bearings for wear, keeps diameters in size and catches chatter before it scraps a run. Start free and put a daily bushing check on every Swiss asset in OxMaint AI.
Do Swiss lathes use coolant or cutting oil?
Most Swiss-type machines run neat (straight) cutting oil rather than water-soluble coolant, because the oil lubricates the guide bushing and bar-feed channel as well as the cut. Straight oil is relatively low-maintenance, but it still needs tramp-oil skimming, fine-chip filtration and temperature control to hold its viscosity and lubricity. Always follow your builder's fluid recommendation for your machine and materials. Book a demo and see how OxMaint AI logs oil condition against each machine.
What is the biggest cause of scrap on a Swiss-type lathe?
A worn or mis-adjusted guide bushing is the usual suspect for dimensional and finish problems, since it supports the workpiece right at the point of cut. Too loose and parts run oversize or mar; too tight and the bar press-fits, heats and chatters. Pair that with collet wear and degraded cutting oil and you have the three issues a Swiss PM schedule is built to catch early. Start free and trend bushing and collet wear per machine in OxMaint AI.
How do I keep a bar feeder running reliably?
Keep the oil-filled guide channel clean and topped to the specified viscosity so the bar rides on a stable, centering oil film, and verify feeder-to-spindle alignment on a regular interval. Inspect channels for scoring, grease the fittings on the builder's schedule, and always power the lathe off before any bar-feeder maintenance. Straight, in-spec bar stock matters as much as the feeder itself. Book a demo and route bar-feeder PM alongside the lathe in OxMaint AI.
Can maintenance software help with medical and aerospace audits?
Yes. OxMaint AI keeps every PM task, part replacement and sign-off tied to the specific machine, so when an auditor asks to see maintenance history for a line, it is a filter away instead of a hunt through binders. For precision Swiss work, that recorded history also helps connect a tolerance excursion back to the maintenance event behind it. Start free and build an audit-ready history for every Swiss lathe.
Run Every Swiss Lathe on a Schedule That Holds Size.
Put the guide-bushing checks, oil skims, bar-feed alignment and spindle routes on meter-and-time triggers in OxMaint AI maintenance management software — raised from the floor, ranked, scheduled before failure, and recorded for the audit. One platform that keeps the spindle turning and the parts in tolerance.