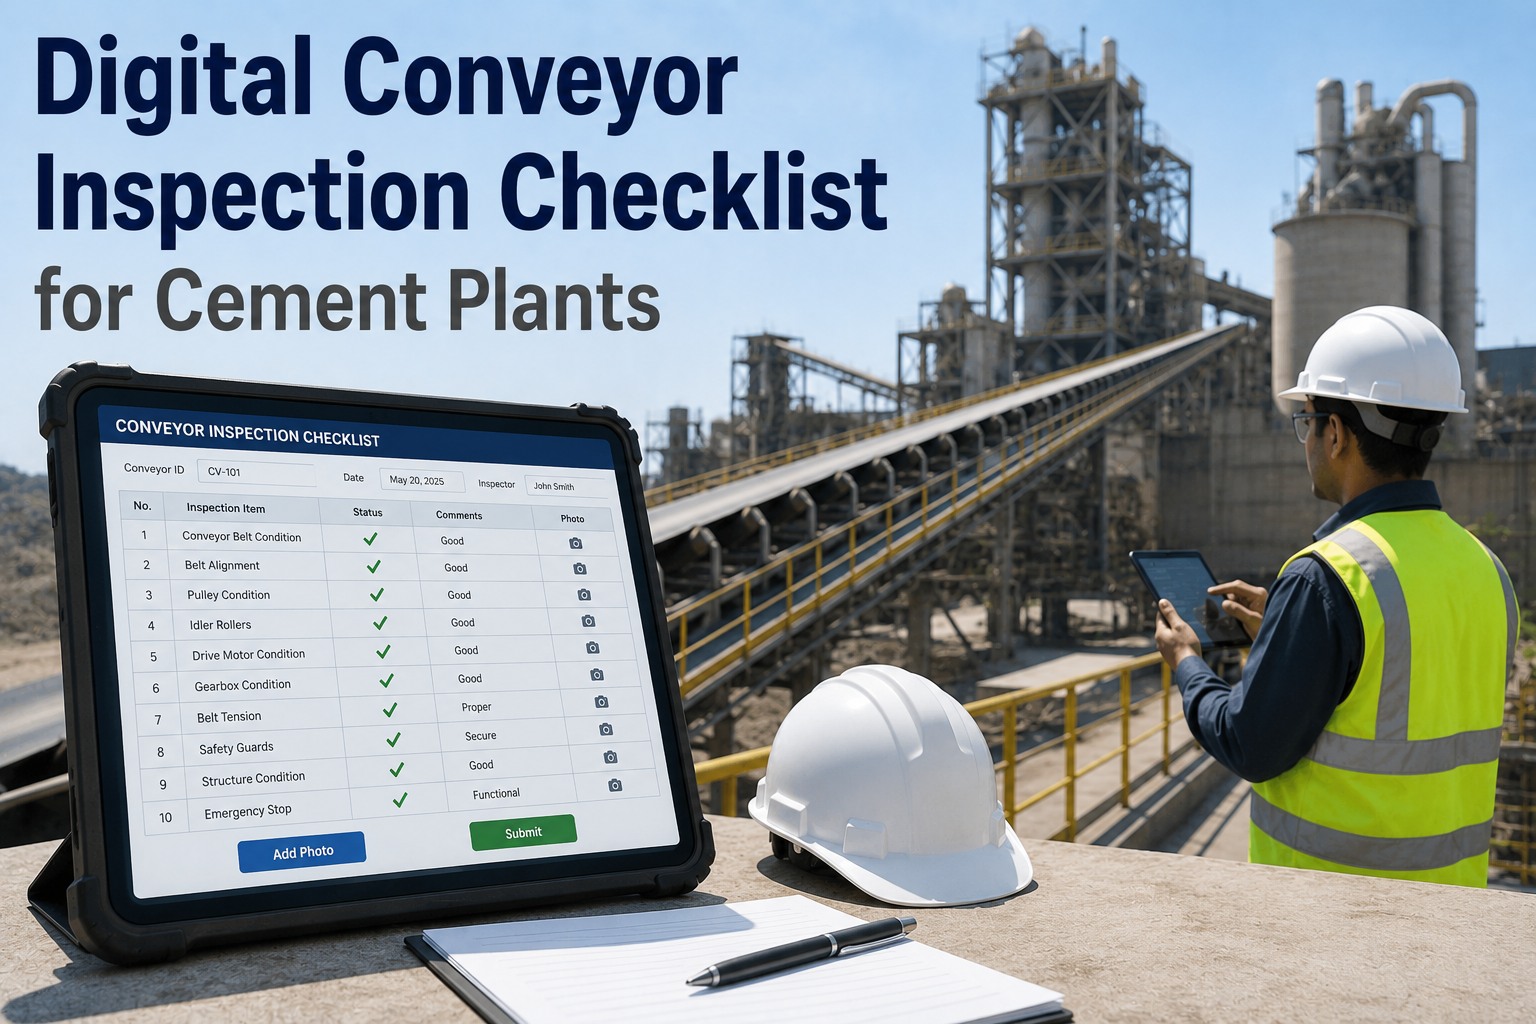
A belt conveyor in a cement plant rarely fails without warning. A seized idler runs hot for weeks, a worn skirt seal leaks fines for months, and a mistracking belt chews one edge until the splice gives way during a kiln feed run. Most of these signals are visible on a walk-round, but only when the inspection is structured, repeatable and linked to work orders. This checklist covers belts, pulleys, idlers, cleaners, drives and safety devices, and shows how Oxmaint maintenance software keeps every finding traceable.
Best Belt Conveyor Inspection and Maintenance Checklist for Cement Plants
A field-ready checklist for limestone, raw meal, coal, clinker and cement conveyors. It shows what to check, what a bad condition looks like, and when to raise a work order before the belt stops the kiln feed.
Inspection Record Header
Complete this block before starting the checklist, and tick each item as it is verified in the field.
Why One Neglected Conveyor Stops a Whole Cement Line
Cement plants run long chains of belts between the quarry, crusher, stacker, raw mill, kiln feed, coal mill, clinker storage and cement mills. A single stopped belt starves or chokes everything downstream.
Cement-specific conditions that accelerate wear
- Abrasive limestone, clinker and silica-rich additives wear covers, chutes and liners quickly.
- Fine raw meal and cement dust pack into bearings, seals and return rollers.
- Hot clinker and kiln-area ambient heat age belt covers and splices faster than a cool quarry belt.
- Coal and petcoke conveyors carry a dust and fire hazard that needs tighter housekeeping and heat checks.
- Wet or sticky material, such as clay or gypsum, builds up on pulleys and causes tracking trouble.
Inspection Zone Map: Where to Look on Every Conveyor
Splitting the conveyor into zones gives the inspector a fixed route. Each zone has its own failure modes and its own stop-and-report criteria.
- Chute liners and impact bed condition
- Skirt rubber gap and clamp tightness
- Material centred on belt at the load point
- Tail pulley lagging and wing wear
- Idler rotation, noise and surface temperature
- Belt edge damage and cover cracking
- Tracking drift over the full length
- Structure, walkway and guard integrity
- Head pulley lagging and slip signs
- Gearbox oil level, leaks and noise
- Coupling guard, alignment and bolts
- Motor current, temperature and vibration
- Primary and secondary cleaner blade life
- Return idler build-up and rubber discs
- Take-up travel, counterweight and guides
- Belt plough and snub pulley condition
The Checklist: Shift, Weekly, Monthly and Shutdown
Frequencies below are a starting point. Adjust them by criticality, material and operating hours, then record the adjusted plan against each conveyor asset.
- Belt is tracking centrally at head, tail and midpoints, with no edge rubbing on the structure.
- No unusual noise from idlers, pulleys, gearbox or motor, and no burning smell.
- Pull-cord switches, emergency stops and belt misalignment switches are accessible and unobstructed.
- Fixed guards are present at pulleys, drives and nip points.
- Spillage around the loading zone and under the return run is within the housekeeping limit.
- No glowing, smoking or visibly hot idlers, especially on coal, petcoke and clinker belts.
- Dust extraction or suppression at transfer points is operating.
- Idler rolls turn freely by hand where safe, and any seized or missing roll is tagged for replacement.
- Skirt seal rubber is in contact with the belt without grooving it, and the gap is consistent.
- Primary and secondary cleaner blades have remaining life and correct tension, and carryback on the return run is low.
- Belt cover shows no gouges, exposed fabric or steel cord, or longitudinal cuts.
- Splice area is flat, with no lifted edges, pulled fasteners or cracked rubber.
- Take-up is moving freely and sits within its normal travel range.
- Gearbox breathers are clear and oil level is within the sight-glass range.
- Head and tail pulley lagging thickness and pattern are measured, and loose or debonded sections are noted.
- Pulley bearings are checked for temperature and vibration, and grease points are serviced to the lubrication plan.
- Impact bed bars or slider rails are checked for wear and for correct support of the belt.
- Chute liners and wear plates are measured, with thin areas logged against remaining thickness.
- Coupling elements, fasteners and guards are checked, and motor and gearbox mounting bolts are verified.
- Thermography is carried out on motors, couplings, bearings and electrical terminations where available.
- Belt weigher or load cell readings are compared against known reference values.
- Full belt length is inspected on the stationary belt for cover wear, edge damage, ply separation and splice condition.
- Worn idlers are replaced as sets in critical sections rather than one at a time.
- Pulley shell, shaft and bearing housings are inspected, and lagging is replaced where worn.
- Gearbox oil is sampled or changed, and the coupling is realigned if readings have drifted.
- Take-up pulley, guides and counterweight are inspected, and rope or screw condition is verified.
- Safety devices are function-tested and the result recorded.
- Lockout and isolation points are confirmed for the next intervention.
Turn the Walk-Round Into Traceable Inspection Records
Load these checks into Oxmaint as mobile inspection templates, link each failed item to a work order, and keep the history by conveyor asset.
Condition Indicators, Likely Causes and Maintenance Actions
Use this table to decide what happens after a finding. It separates what the inspector sees from what maintenance should do next.
| Observation | Likely cause | Maintenance action | Escalate when |
|---|---|---|---|
| Belt runs to one side | Misaligned idler frames, uneven loading, material build-up | Clean rollers, check frame squareness, adjust training idlers | Edge touches structure or damage is visible |
| Hot or noisy idler | Bearing failure, seal damage, dust ingress | Replace roll and inspect neighbouring rolls | Roll is glowing, smoking or on a coal belt |
| Spillage at load point | Worn skirts, poor chute design, belt sag between idlers | Reset or replace skirt rubber, add impact support | Spillage buries rollers or blocks access |
| Carryback under head pulley | Worn cleaner blade, incorrect tension | Replace blade, set tension, inspect cleaner pole | Build-up reaches return rollers or tail |
| Belt slips at the drive | Worn lagging, low take-up tension, wet or sticky material | Inspect lagging, check take-up, review loading | Slip is recurring or motor current is abnormal |
| Splice lifting or fasteners pulled | Fatigue, incorrect splice, pulley diameter issue | Schedule re-splice or repair in the next stop | Splice opens or cord is exposed |
| Gearbox oil leak or heat | Seal wear, blocked breather, overload | Repair seal, clear breather, sample oil | Level drops quickly or temperature trends up |
Adjusting the Checklist by Material Carried
The same inspection form should not be applied to every conveyor. Add or tighten items based on what the belt carries.
From Paper Rounds to a Connected Inspection Workflow
- Findings are verbal or on a clipboard that is lost by the next shift.
- Repeat idler failures are not linked to a conveyor section.
- Replacement lagging, idlers and skirts are ordered after the failure.
- Shutdown scope is decided from memory a few days before the stop.
- Inspectors complete mobile checklists by conveyor and zone.
- A failed item opens a corrective work order with priority and photo.
- Parts such as idlers, cleaner blades and lagging are tracked in inventory.
- Shutdown work lists are built from open defects and trend history.
How Oxmaint supports the conveyor maintenance cycle
- Asset management to structure each conveyor into pulleys, drive, idlers, cleaners and safety devices.
- Preventive maintenance schedules for lubrication, idler checks, lagging measurement and cleaner changes.
- Work orders for corrective repairs, with assignment, due dates and completion notes.
- Inspection records and reports that show which conveyors have repeat defects.
- Inventory for spare idlers, belt splice kits and wear parts, to avoid waiting on a missing item during a stop.
- Condition-based triggers that can create work from vibration, temperature or run-hour readings where those inputs are captured.
Safe Inspection Sequence Before Anyone Touches the Belt
Many conveyor injuries happen during inspection and cleaning, not during production. Build the safety steps into the checklist so they are recorded, not assumed.
Root Causes Behind Repeat Conveyor Defects
If the same idler or skirt fails again and again, replacing it is only half the job. The inspection record should help maintenance find the cause.
- Off-centre loading from a worn or badly set chute, which pushes the belt to one side and overloads one wing of the idler set.
- Carryback that falls onto return idlers, builds up on the roller shell, and forces the belt out of line.
- Idler frames that have shifted after a shutdown or structural movement and were never re-surveyed.
- Skirt rubber installed too tight, which causes belt cover grooving, or too loose, which leaks fines.
- Lubrication carried out by habit rather than by the bearing type, duty and contamination level.
- Take-up systems that are seized or incorrectly weighted, which allow slip and high-tension cycles on the belt.
- Splices made under time pressure without the correct vulcanising or mechanical fastener procedure.
What to record so patterns become visible
- The exact conveyor, zone and position, such as carrying idler station number or return roller number.
- The failure mode: bearing seized, shell worn, seal failed, frame bent, or build-up.
- Run hours or date since the last replacement of the same component.
- Whether the failure was found on inspection or after a trip, so detection quality can be reviewed.
- Parts used and labour time, to compare repair cost against planned replacement.
Escalation Ladder for Conveyor Findings
Belt and Splice Condition: What to Measure and Record
The belt is the most expensive component on the conveyor, so its condition record deserves more than a note saying it looks fine.
- Record top cover thickness at fixed stations along the length, so wear rate per section can be calculated.
- Photograph each splice at every inspection and note fastener loss, lifted edges or rubber cracking.
- Log edge damage, longitudinal cuts and impact marks with their distance from the splice or a belt marker.
- Note belt age, rated type and any heat-resistant or fire-resistant specification, so replacement stock matches the duty.
- Record belt length changes after take-up adjustments, because repeated adjustment means stretch or a fault in the take-up.
- Capture any belt rip detection or tear sensor status, and test it as part of the safety device checks.
Typical inspection tools to place on the work order
- Thickness gauge for covers and lagging, plus a straight edge for pulley and idler alignment.
- Infrared thermometer or thermal camera for bearings, rollers, gearbox and motor.
- Vibration pen or portable analyser for critical drive and pulley bearings.
- Camera or phone for dated photographs attached to each finding.
KPIs to Prove the Checklist Is Working
Belt Conveyor Inspection FAQs
Keep Every Conveyor Running Between Shutdowns
Replace scattered notes with one inspection and maintenance record for every belt in the plant. Start with your critical conveyors and expand once the routine is working.