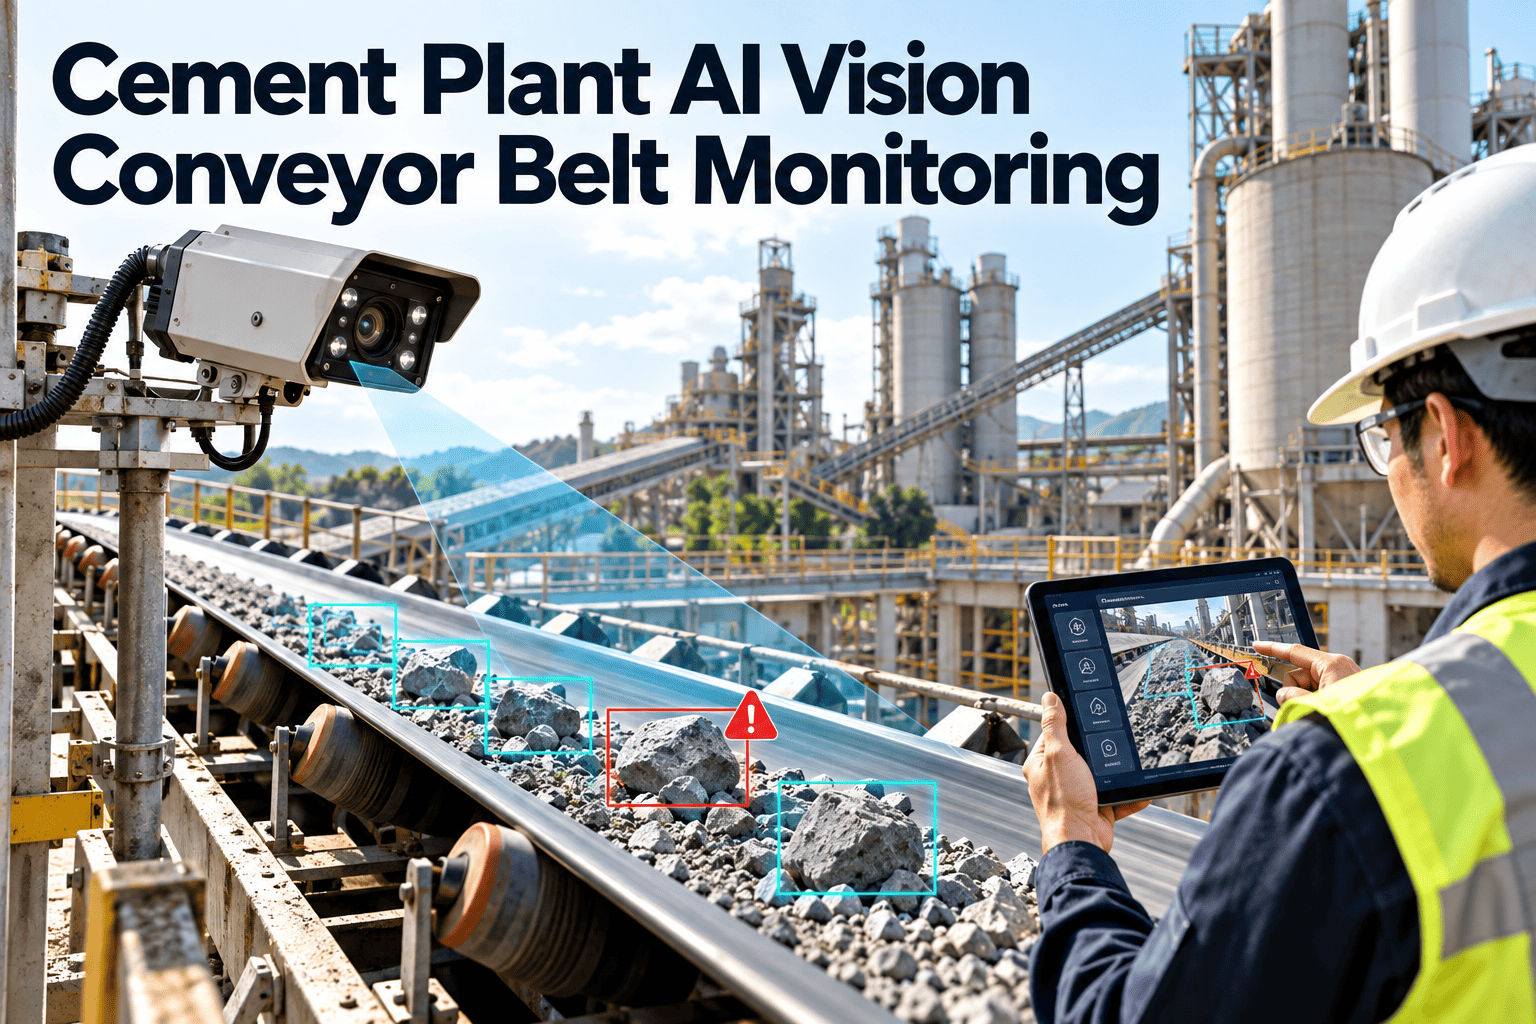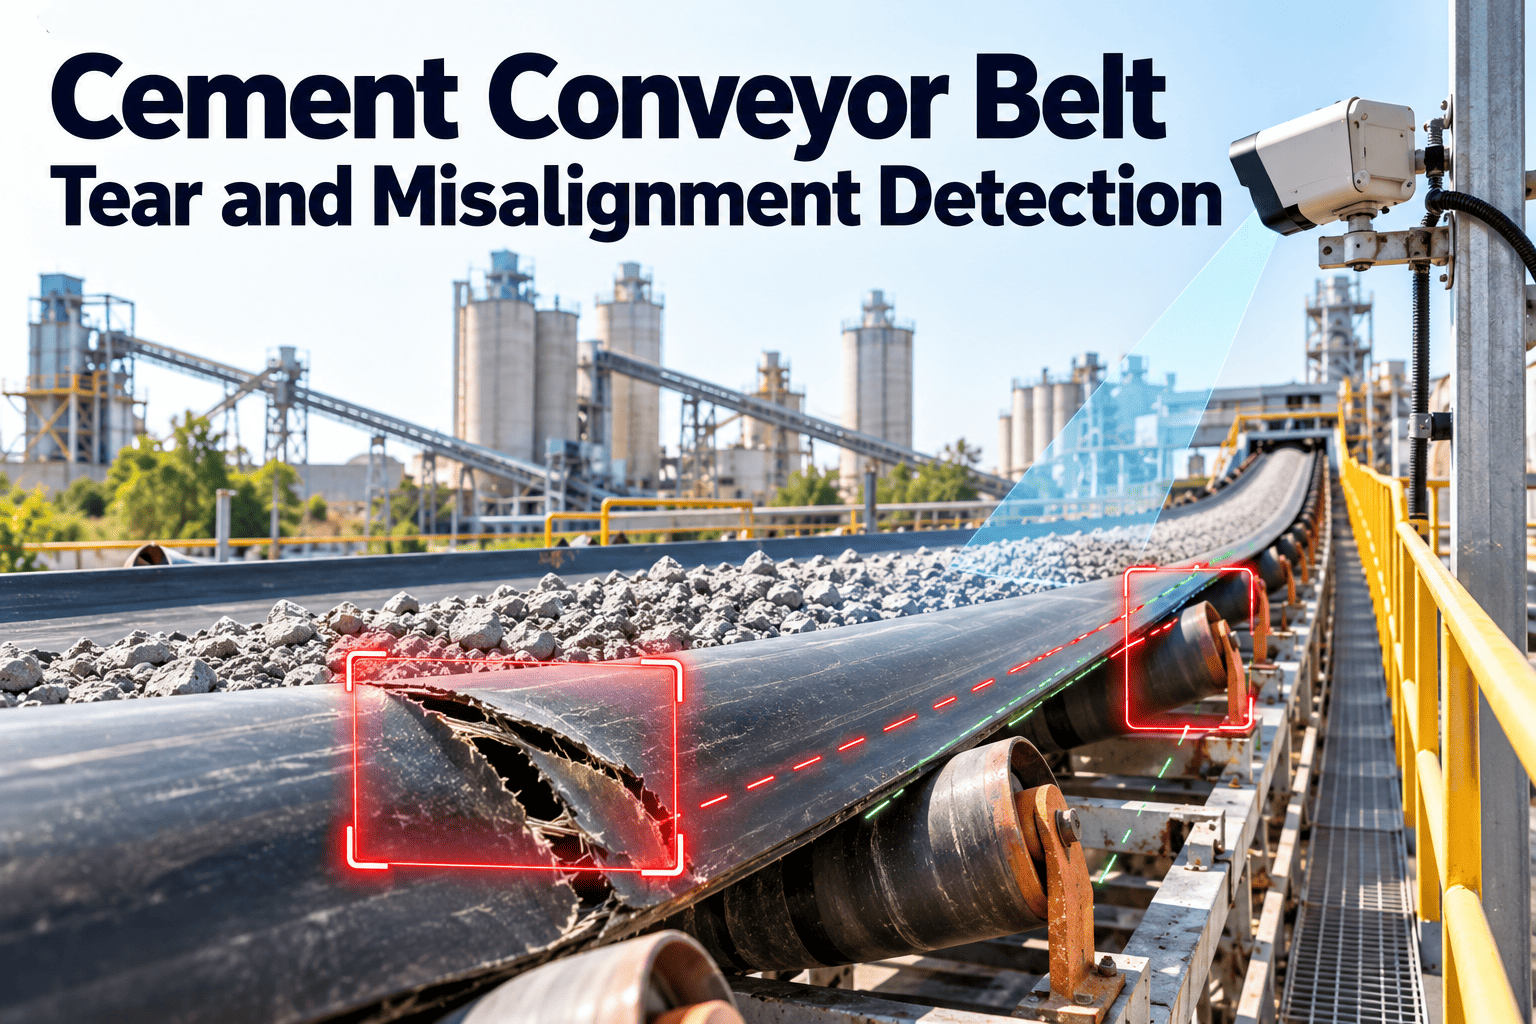
A conveyor belt rarely fails all at once. A tear starts with one impaled object or hung-up lump, and drift starts with a small mistrack that nobody notices until the edge rubs steel. On cement plant limestone, clinker, and coal belts that feed the kiln and mills, late detection turns a repairable fault into a long stoppage. This guide covers how tears and misalignment start, which detection layers work, and how crews should respond. When alarms and findings flow into Oxmaint maintenance management software, each event becomes a tracked job instead of a radio call.
Cement Conveyor Belt Tear and Misalignment Detection
Detect belt rips and tracking drift early, stop the belt before damage spreads, and turn every alarm into a planned repair.
Tear versus misalignment: two failures on different clocks
Both faults damage belts, but they develop differently. Detection and response need to match the speed of each one.
| Aspect | Belt tear or rip | Misalignment or mistracking |
|---|---|---|
| How it starts | Sharp object, wedged rock, or stuck component cuts the cover or carcass | Uneven loading, out-of-square idlers or pulleys, buildup, skewed splice |
| Speed of progression | Can lengthen quickly once started because the belt keeps running | Usually gradual, but accelerates once the edge meets structure |
| First sign | Gouge, slit, or sudden spillage at a transfer point | Edge creeping toward a guard, spillage on one side |
| Typical consequence | Long splice or section replacement, material loss | Frayed edges, damaged structure, heavy spillage, ignition risk |
| Best early detection | Rip sensors, tramp metal detection, chute blockage switches | Tracking switches, edge sensing, regular inspection trends |
| Typical repair | Patch, re-splice, or replace a belt section | Realign, clean, replace idlers or lagging, adjust loading |
Five layers of protection around a cement conveyor belt
No sensor catches everything. Reliable plants stack layers so that when one fails, the next one catches the fault.
Where belt tears come from in cement plants
Most longitudinal tears trace back to a few repeat causes. Each has a different prevention and warning sign.
| Cause | Typical location | Prevention | Warning sign |
|---|---|---|---|
| Tramp metal such as drill steel, liner bolts, or crusher teeth | Crusher discharge and first transfer | Magnets, metal detectors, controlled liner and bolt practice | Detector trips and scratches near the loading point |
| Rock wedged at chute or skirt | Transfer chutes and loading zones | Chute design, clearance checks, hung-up material control | Gouges on the cover and sudden spillage |
| Seized idler or stuck roller | Carrying and return runs | Idler inspection rounds | Hot or noisy rollers, flat-spotted shells |
| Damaged belt cleaner blade or fastener | Head pulley discharge | Blade inspection and secure fixings | Scoring on the belt cover |
| Splice failure | Splice joints | Splice inspection and quality repair practice | Lifted edges, cracking, or cover separation |
| Belt edge catching structure | Anywhere drift occurs | Tracking control and guards | Edge fraying and damaged guards |
Reading misalignment: symptom, likely cause, first check
Where and when the belt drifts is the best clue to why. Use the pattern to guide the first inspection instead of guessing.
| Observed pattern | Likely cause | First check |
|---|---|---|
| Drifts at one location only | Local idler or frame out of square, buildup on a roller | Idler frames, roller condition, nearby cleaning |
| Drifts the same way along the whole run | Pulley misalignment or skewed belt | Head and tail pulley alignment, take-up position |
| Drifts only when loaded | Off-center loading or worn chute liners | Feed position, chute liners, skirt condition |
| Drifts with wet or sticky material | Buildup on pulleys and idlers | Belt cleaners, pulley lagging, return rollers |
| Wanders near a splice | Crooked splice or belt skew | Splice squareness and edge alignment |
| Chronic damage on one edge | Training idlers not working or structure contact | Training idlers, guards, structure clearance |
Which detection method belongs where along the conveyor
Place each sensor where the fault is most likely to start or first show itself.
- Magnets and metal detectors upstream
- Plugged chute switches
- Rip detection sensors after the load zone
- Off-center loading checks
- Tracking switches at intervals
- Idler condition rounds
- Edge or camera-based sensing on long runs
- Spillage and cover wear checks
- Tracking switch near the pulley
- Belt cleaner blade inspection
- Pulley lagging and buildup checks
- Speed or zero-speed monitoring
- Take-up position and tension checks
- Return idler condition
- Splice inspection on the return side
- Buildup and spillage under the belt
Cut the time between a belt fault and a work order
Log trips, drift findings, and splice inspections against each conveyor so crews respond to the same facts.
Alarm philosophy: from information to trip
A clear alarm ladder avoids two common failures: ignored warnings and nuisance trips that tempt crews to bypass protection.
| Level | Example trigger | Response | Work order |
|---|---|---|---|
| Information | Small drift inside tolerance | Note and watch on the next round | Add to inspection list |
| Warning | First-stage drift or repeated chute blockage | Operator checks the location and reports the cause | Corrective job with priority |
| Trip | Rip detected, second-stage drift, plugged chute | Stop feed and belt, lock out, inspect before restart | Urgent job with cause recorded |
Rules for keeping protection trusted
- Set thresholds during commissioning and review them after any belt or structure change
- Record the cause of every trip, including false trips
- Require authorization and a record for any bypass
- Test switches and sensors on a defined schedule
- Review repeat trips by conveyor in the weekly reliability meeting
A tear event with and without layered detection
- Object impales the belt at the transfer chute
- Belt keeps running and the cut lengthens
- Spillage builds and the area is noticed later
- Operator calls for a stop and a crew is found
- Extended repair, parts search, restart pressure
- Metal detector or rip sensor flags the event
- Feed and belt stop in sequence
- Crew locks out and inspects the damage
- Repair method chosen: patch, splice, or section swap
- Restart after verification, cause logged in the system
Inspection routines that support detection hardware
Sensors catch events. Inspections catch the slow changes that cause them.
- Check edge position against guards
- Look for fresh spillage and cover damage
- Listen for noisy rollers or scraping
- Confirm cleaners are contacting the belt
- Inspect splices for lifted edges or cracks
- Measure cover wear at known points
- Check pulley lagging and chute liners
- Test tracking switches and pull cords
- Check pulley and idler alignment
- Review take-up travel and tension
- Replace worn cleaner blades and lagging
- Carry out planned splice repairs
The belt fault response loop in Oxmaint
The aim is a closed loop: every detection leads to a repair, a root cause, and a prevention step.
Oxmaint capabilities that fit belt maintenance
- Asset management for belts, splices, pulleys, idlers, chutes, cleaners, and sensors in a conveyor hierarchy
- Mobile inspection checklists for walk-downs, stopped-belt inspections, and switch tests
- Work orders created from alarms and findings, with priority and assigned crews
- Preventive maintenance scheduling for splice inspection, thickness checks, and cleaner blade replacement
- Inventory tracking for belt sections, splice kits, cleaner blades, and sensors
- Compliance records for lockout checks, switch tests, and inspection history
- Condition-based workflows using thresholds your team defines
- Dashboards for trips by conveyor and cause, overdue inspections, and backlog
KPIs that connect detection to results
| Metric | What it tells you | Action when it worsens |
|---|---|---|
| Belt trips by cause | Which faults repeat | Fix the top cause first |
| Time from alarm to work order | How fast findings enter planning | Simplify reporting at the conveyor |
| Time to restore after a tear | Repair readiness | Review spares, crews, and splice kits |
| Repeat misalignment by conveyor | Whether root causes are fixed | Audit alignment, loading, and cleaning |
| Inspections and switch tests completed | Discipline of the routine | Adjust routes and ownership |
| Planned versus emergency belt work | Reactive load on the team | Shift effort toward planned inspections |
Safety and compliance when working on belts
Belt tear and misalignment detection: common questions
How is a belt rip detected?
What causes cement conveyor belt misalignment?
Are tracking switches enough on their own?
Can tramp metal be fully prevented?
How does maintenance software help with belt faults?
Catch belt tears and drift before they stop the line
Bring alarms, inspections, spares, and repair history into one maintenance system for every cement conveyor.