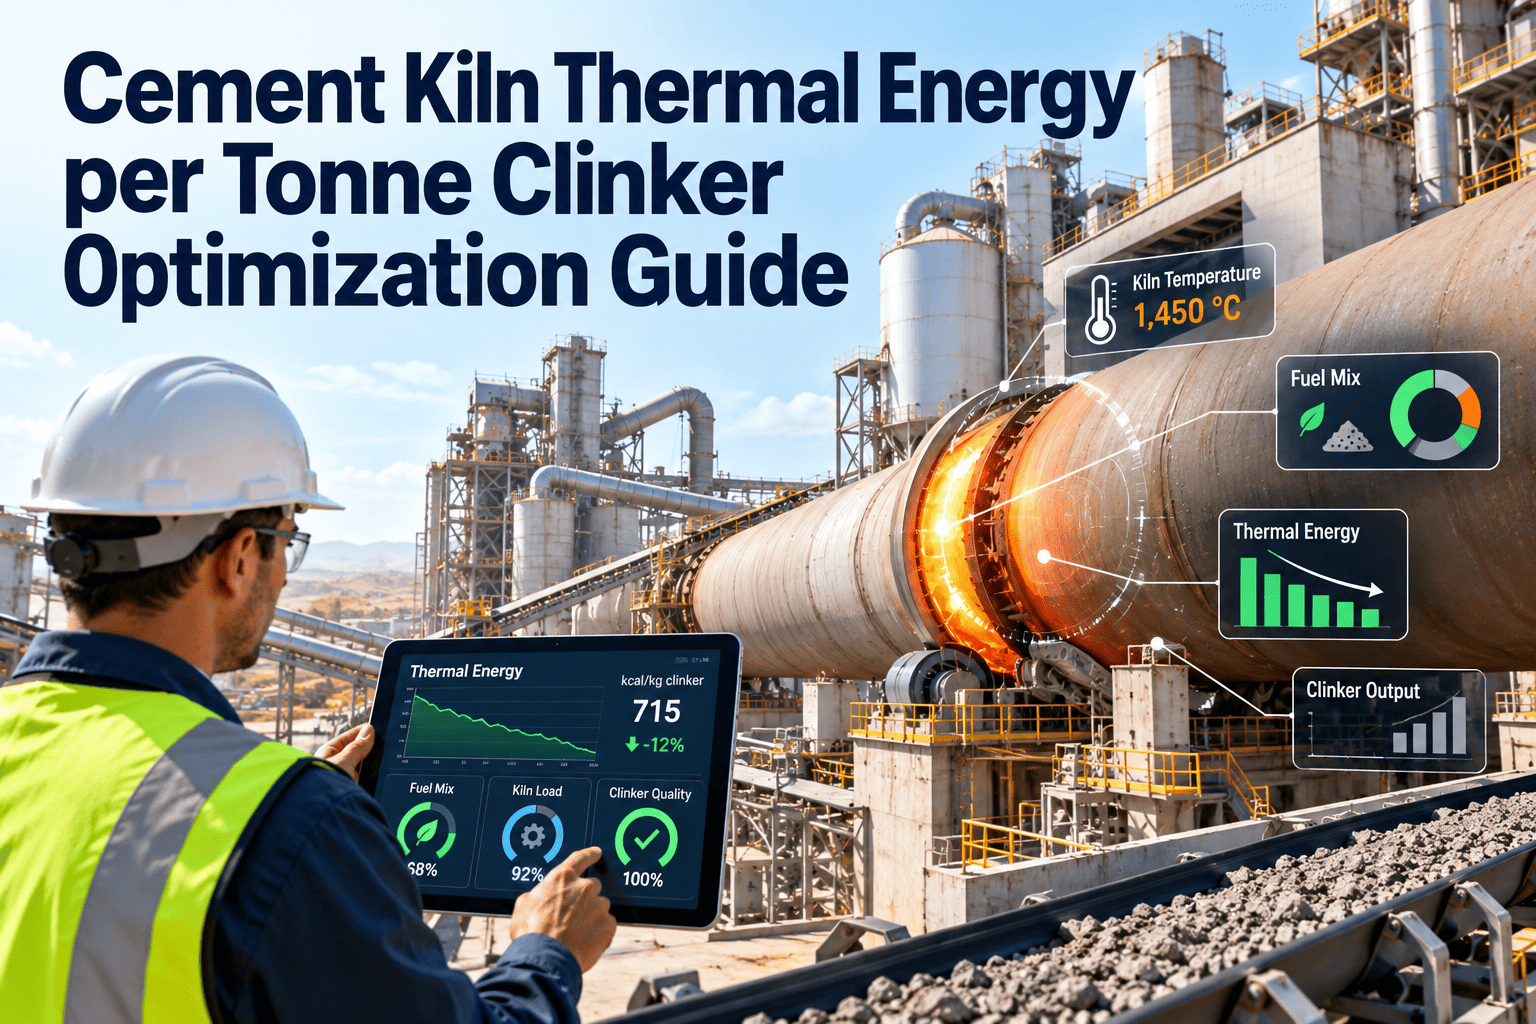
Fuel is one of the largest controllable costs in cement manufacturing, and the kiln is where almost all of it is spent. Thermal energy per tonne of clinker rises quietly when false air creeps in, cyclones build up, cooler grates wear and refractory thins. Process teams often chase set points while the real losses sit in equipment condition. This guide connects kiln heat consumption to maintenance practice, and shows how Oxmaint maintenance management software keeps those energy-critical tasks scheduled, recorded and closed.
Cement Kiln Thermal Energy per Tonne Clinker Optimization Guide
Find where heat is lost between the preheater and the cooler, and turn each loss into a planned maintenance action.
Why heat per tonne of clinker matters to cost and carbon
Every extra megajoule burned per tonne of clinker adds fuel cost and process emissions at the same time. That makes thermal efficiency a financial and a decarbonization topic.
The cost view
- Fuel is bought and burned continuously, so small inefficiencies repeat every hour.
- Unstable kiln operation wastes fuel during upsets, stops and restarts.
- Higher exhaust gas volumes increase fan power on top of fuel use.
The emissions view
- Calcination releases carbon dioxide from the raw material regardless of fuel choice.
- Fuel combustion adds further emissions, and reducing heat demand lowers them.
- Efficiency gains also make alternative fuel use easier to sustain.
Where the heat goes in a kiln heat balance
The chemistry of clinker formation sets a theoretical minimum, commonly cited at roughly 1.7 to 1.8 GJ per tonne. Everything above that is loss, and most losses have a maintenance link.
| Heat loss path | What increases it | Maintenance link |
|---|---|---|
| Preheater exhaust gas | False air, poor cyclone separation, build-ups, high gas volume | Seal inspections, cyclone cleaning, air-leak surveys |
| Clinker cooler | Poor air distribution, worn grate plates, fan problems | Grate plate condition, fan and damper checks |
| Kiln shell radiation | Missing coating, thin or failed refractory, hot spots | Shell scanning, refractory inspection and repair |
| Dust and bypass losses | Poor dust return, excessive bypass, leaking seals | Dust handling and bypass system reliability |
| Kiln inlet and outlet seals | Worn seal elements allowing cold air in or hot gas out | Seal replacement planned at the right condition |
| Combustion inefficiency | Burner wear, poor flame shape, unstable fuel feed | Burner tip condition, feeder calibration, dosing checks |
Follow the heat path from raw meal to clinker
Walking the process in order helps teams link each stage to a recurring maintenance check.
Raw meal feed
- Feed stability
- Raw mill fineness
- Moisture handling
Preheater
- Cyclone build-up
- Air-in leaks
- Pressure drop trend
Calciner
- Fuel feed control
- Tertiary air
- Refractory state
Rotary kiln
- Burner condition
- Shell temperature
- Seal condition
Cooler
- Grate plates
- Air fans
- Heat recovery
Make every energy-critical kiln task a scheduled job
Plan air-leak surveys, cooler checks, shell scans and burner work in one maintenance system with full history.
Six maintenance causes of rising heat consumption
These causes appear again and again in kiln lines. Treat each as a recurring inspection item, not a one-time project.
False air ingress
Leaks at kiln seals, inspection doors, expansion joints and cyclone flaps dilute process gas and raise fan load. Regular leak surveys and seal condition checks prevent slow drift.
Preheater build-up and blockages
Coating build-up restricts gas flow and separation efficiency. Tracking pressure drop trends and cleaning outcomes shows where recurring build-up starts.
Cooler wear and imbalance
Worn grate plates and poor air distribution reduce heat recovery and raise clinker temperature. Condition-based replacement keeps recuperation stable.
Refractory and shell losses
Thin lining and exposed shell zones radiate heat and risk unplanned stops. Shell temperature scans guide where repair is needed first.
Burner and fuel feeding issues
Worn burner components and unstable dosing distort flame shape and combustion. Feeder calibration and burner inspection belong in the PM plan.
Frequent stops and restarts
Each trip burns fuel for heating without producing saleable clinker. Reliability of fans, drives and feeders directly protects thermal efficiency.
From symptom to probable cause
Operators often notice the symptom first. This table helps maintenance and process teams agree on what to check.
| Observed symptom | Probable equipment cause | First check |
|---|---|---|
| Rising exit gas oxygen with higher fan load | False air at seals or ducts | Seal and joint leak survey |
| Higher preheater exit temperature | Build-up, poor cyclone separation, feed issues | Pressure profile and cyclone inspection |
| Hot clinker leaving the cooler | Grate wear, air imbalance, fan fault | Cooler air distribution and plate condition |
| New shell hot spots | Refractory loss or coating failure | Shell scan and planned repair review |
| Unstable flame and CO fluctuation | Burner wear or fuel feed variation | Burner inspection and feeder calibration |
| Frequent short stops | Drive, fan or feeder reliability problem | Work order history and root cause review |
Clinker cooler: the heat recovery stage that is easy to neglect
The cooler returns heat to the kiln and calciner as secondary and tertiary air. When it underperforms, that heat leaves with the clinker and exhaust instead.
- Grate plates: inspect for wear, warping and blocked air passages, and track replacement intervals by condition.
- Air distribution: check fan performance, dampers and compartment pressure so air reaches the clinker bed evenly.
- Snowman and red river events: record each event with its cause, because repeated incidents point to equipment or process drift.
- Hydraulic drives: monitor oil condition, leaks and cylinder health, since drive faults often force cooler reductions.
- Clinker breaker and conveyors: keep them reliable so cooler outlet problems do not limit kiln feed.
Refractory and shell: managing heat you can see
Shell temperature is one of the few heat losses that can be measured directly and acted on quickly.
- Shell scan results by kiln position
- Location and size of any hot spot
- Coating behavior in the burning zone
- Lining age and installed material type
- Monitor, cool locally or stop for repair
- Which zone to reline at the next outage
- Whether the cause is process or material
- Which spares and crews to prepare
Why kiln stability protects thermal efficiency
A steady kiln consumes less fuel per tonne than one that cycles through upsets, so equipment reliability is part of energy performance.
Feed variation
- Feeder wear
- Weigh system drift
- Raw mill outages
Draft disturbance
- ID fan faults
- Damper issues
- Build-up events
Fuel instability
- Dosing errors
- Blocked lines
- Burner damage
Unplanned stop
- Heat-up fuel use
- Lost clinker output
- Thermal stress on lining
Recovery
- Restart effort
- Quality variation
- Higher heat per tonne
Mistakes that keep heat consumption high
These habits show up often in plants that struggle to hold energy gains.
- Treating efficiency as a process-only topic: maintenance owns many of the loss sources, so the two teams must review data together.
- Fixing leaks once: seals and joints wear continuously, so surveys must repeat on a schedule.
- Deferring cooler repairs: small wear problems become large heat recovery losses before the next outage.
- Ignoring instrument drift: an uncalibrated analyzer or flow meter misdirects operators and engineers.
- Missing root cause analysis: repeat build-ups or trips need investigation, not only clearing and restarting.
A weekly kiln line energy walkdown
A short, recorded route keeps small losses from growing between shutdowns.
- Listen and feel for air leaks at doors and joints
- Check cyclone flap action and visible build-up
- Review shell temperature scan trends
- Inspect kiln seals for gaps and wear
- Check cooler fan current and damper position
- Note clinker temperature at the outlet
- Inspect hydraulic leaks at the grate drive
- Review vibration and bearing temperature on key fans
Measuring thermal energy consumption you can trust
An improvement program needs a baseline that engineers believe. Weak measurement hides both losses and gains.
- Fuel flow and calorific value: use calibrated metering and regular lab values, especially when fuel quality varies.
- Clinker production: use a consistent method, and record how it is derived so trends stay comparable.
- Operating state: separate stable running from heat-up, upset and restart periods before comparing results.
- Raw material moisture: note changes that affect drying heat demand upstream of the kiln.
- Instrument health: include flow meters, oxygen analyzers and thermocouples in the calibration schedule.
Reactive energy management versus reliability-driven
Plants that treat efficiency as a maintenance outcome behave differently from those that treat it only as a process target.
- Leaks found when fan load is already high
- Cooler plates replaced after clear failure
- Shell hot spots handled at the next breakdown
- Fuel use blamed on raw material alone
- Findings recorded in separate spreadsheets
- Leak surveys on a defined schedule
- Cooler wear tracked and parts planned
- Shell scans trigger planned refractory work
- Equipment and process data reviewed together
- All findings stored against the asset
How Oxmaint supports energy-focused kiln maintenance
Oxmaint does not replace process control. It makes sure the maintenance tasks behind thermal efficiency are planned, performed and visible.
- Asset management: structure the kiln line from preheater to cooler with documents, spares and history.
- Preventive maintenance: schedule seal checks, cooler inspections, burner service and instrument calibration.
- Inspection checklists: record shell temperature observations, leak findings and photos on mobile.
- Condition-based work orders: raise jobs when readings or inspection results cross set limits.
- Inventory: keep grate plates, seals, burner parts and sensors available before shutdowns.
- Reports and dashboards: review repeat defects, overdue tasks and kiln stop causes by asset.
Work order data that makes energy analysis possible
Maintenance records become useful for energy work only when they capture the right details at closure.
| Field to record | Example entry | Why it helps |
|---|---|---|
| Asset and location | Kiln inlet seal, drive side | Links repairs to a specific heat loss path |
| Failure or finding code | Seal wear, air leak found | Allows repeat issues to be counted and ranked |
| Condition before and after | Gap measurement or leak survey result | Shows whether the repair removed the loss |
| Downtime and stop type | Planned stop or unplanned trip | Separates restart fuel penalties from steady running |
| Parts used | Seal elements, grate plates, burner tip | Supports spares planning and wear analysis |
| Follow-up action | Re-survey after two weeks | Closes the loop on the energy benefit |
Alternative fuels and thermal efficiency
Many plants raise their use of alternative fuels while still controlling heat consumption. That puts extra demand on feeding and combustion equipment.
- Feeding stability: inconsistent dosing disturbs flame and calciner temperature, which can raise heat consumption.
- Moisture and calorific value: fuel quality changes should be reflected in feed rates and energy calculations.
- Equipment wear: abrasive or bulky fuels can accelerate wear on conveyors, airlocks and burner components.
- Build-up risk: chlorine, alkali and sulfur cycles may increase blockage risk, so preheater inspections matter more.
- Combustion monitoring: watch carbon monoxide, flame appearance and kiln torque trends so feed changes do not hide emerging equipment problems.
- Records: log fuel type, feed rate changes and related equipment findings together so energy effects can be explained later.
Shutdown scope checklist for energy recovery
Annual kiln outages are the best chance to remove heat losses that cannot be reached while running.
- Replace worn kiln inlet and outlet seal elements and verify the fit.
- Repair cyclone flaps, expansion joints and inspection door seals found leaking during the year.
- Inspect and renew cooler grate plates and check air compartment sealing.
- Reline the zones flagged by shell scans, using the recorded hot spot history.
- Service burner components and recalibrate fuel feeders and key analyzers.
KPIs that connect maintenance to heat consumption
Review these together with the process team each month so improvements are visible and attributable.
| KPI | What it tells you | Desired trend |
|---|---|---|
| Specific thermal energy per tonne clinker | Overall kiln fuel efficiency | Falling or stable at target |
| Kiln run factor | Share of time producing clinker | Rising |
| Number of unplanned kiln stops | Reliability of the kiln line | Falling |
| False air surveys completed | Discipline in preventing leaks | On schedule |
| Planned versus reactive work | Maturity of maintenance planning | Shifting toward planned |
| Open shell and refractory actions | Backlog of known heat loss sources | Falling |
A 90-day plan to start reducing heat losses
Start with a focused kiln line review rather than a plant-wide program.
Baseline
Confirm measurement quality, list heat loss paths and record current inspection routines.
Inspect and fix
Run leak surveys, review cooler and shell condition and plan the highest-value repairs.
Embed
Convert checks into recurring tasks and review KPIs in a monthly energy and reliability meeting.
Kiln thermal energy FAQs
What is thermal energy per tonne of clinker?
It is the fuel heat used to produce one tonne of clinker, usually expressed in megajoules or kilocalories.
Can maintenance really reduce kiln fuel use?
Yes. Fixing air leaks, cooler wear and refractory loss reduces avoidable heat loss. Get started to schedule those checks.
What should we inspect first?
Start with kiln seals, preheater air leaks, cooler grates and shell hot spots, since they affect heat losses directly.
Do alternative fuels change the picture?
They can, because fuel quality and feeding stability affect combustion, so feeder and burner reliability matter more.
How do we track improvements?
Link energy KPIs to work orders and findings. To see how, book a demo.
Lower kiln heat loss with maintenance you can prove
Give your cement plant a single workflow for energy-critical inspections, repairs and results.