A kiln drive gearbox bearing, a roller press stud set or a vertical mill grinding roller can sit on a supplier's lead time for months, while the plant it serves loses clinker output every hour. Spare parts shortages in cement rarely come from one bad purchase. They come from weak criticality ranking, stale reorder points and maintenance plans that never reach the storeroom. This guide shows how cement teams can find the parts that matter, size stock to real risk and tie inventory to planned work. Plants that want to see this in practice can review maintenance inventory and work order software built for this workflow.
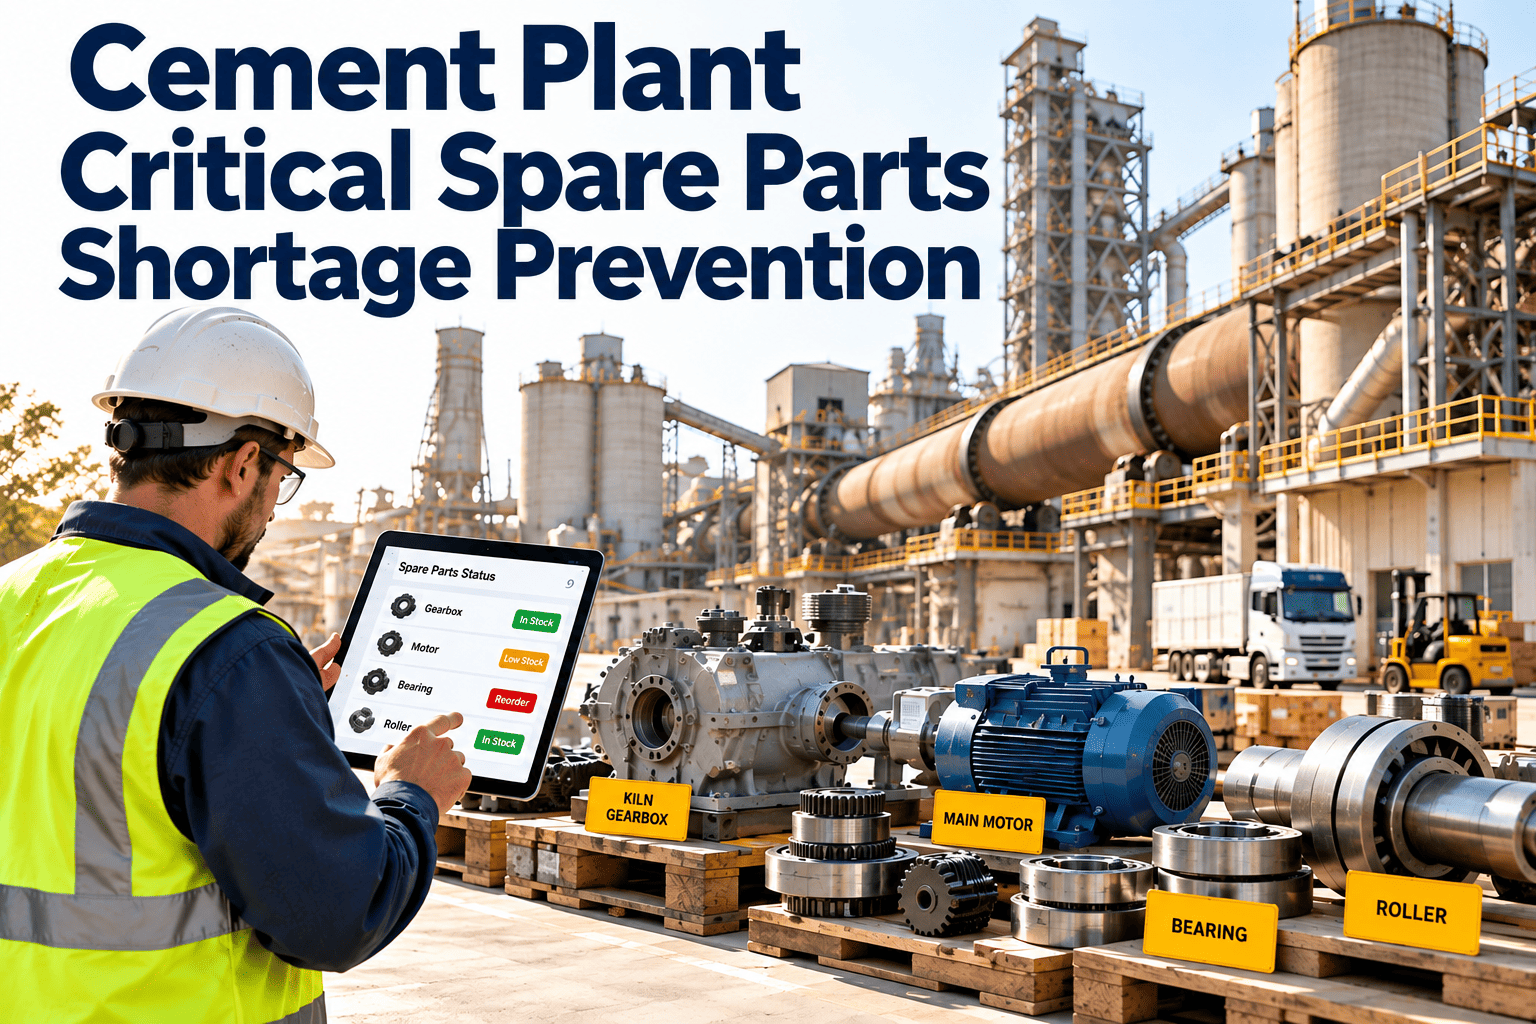
Cement Plant Critical Spare Parts Shortage Prevention
A shortage is a chain of small planning gaps that ends at a stopped kiln. Break the chain early, at the criticality ranking, the reorder rule and the work order, and the emergency freight bill never arrives.
1Wear signal ignored or unrecorded
2Part not reserved against a plan
3Lead time longer than the warning
4Kiln, mill or cooler stops
5Expedited freight and rushed repair
Why cement plants run short on the parts that matter most
Cement is a continuous, high-temperature, abrasive process. Equipment is large, often custom, and frequently sourced from a handful of manufacturers. That combination makes spare parts planning very different from a general factory storeroom.
- Long lead times on forged, cast and machined items such as kiln support roller shafts, girth gear segments, pinions and large gearbox components.
- Wear parts that fail on a curve rather than a date, so a fixed annual order never matches real consumption.
- Many plants hold thousands of low value items while the five parts that can stop the kiln sit unreserved or are missing from the system entirely.
- Shutdown scopes that grow late, so kits are incomplete on the first day of the stoppage.
- Part numbers that differ between the OEM manual, the storeroom and purchasing, which hides stock that actually exists.
Seven shortage patterns seen in cement maintenance
Most stockouts repeat the same few patterns. Naming them helps a planning team audit its own storeroom quickly.
The invisible critical spare
The part is critical in everyone's head but has no criticality flag, no minimum and no owner in the system.
The stale reorder point
The minimum was set years ago, before supplier lead times stretched or before an equipment upgrade changed consumption.
The phantom stock
The system says one is on the shelf. The shelf says otherwise, because issues were never booked or a part was cannibalised.
The unreserved kit
A planned job has no linked parts list, so the storeroom cannot reserve anything before the stoppage.
The single source trap
One supplier, one drawing, one country of origin, and no approved alternate or repair route.
The unrepaired rotable
A removed gearbox or motor is not sent for repair, so the pool of exchange units quietly shrinks.
The late approval
The requisition waits for budget sign-off while the lead time clock keeps running.
Rank spares by consequence and lead time, not by price
Purchase price is a poor guide to stocking priority. A cheap sensor can stop a mill, and an expensive spare may never be needed. A simple two-axis ranking separates the parts that deserve insurance stock from those that can be bought on demand.
Long lead time, high consequence Stock on site as an insurance spare with owner, location and inspection routine.
Long lead time, moderate consequence Hold one, or share through a sister plant or supplier agreement.
Long lead time, low consequence Plan the buy against the maintenance plan and watch the lead time.
Short lead time, high consequence Keep a small buffer with automatic reorder.
Short lead time, moderate consequence Standard minimum and maximum with periodic review.
Short lead time, low consequence Buy on demand or use vendor managed stock.
Scoring questions to ask for every critical candidate
- If this part fails today, which production unit stops and for how long?
- What is the real supplier lead time, including manufacturing, inspection and shipping?
- Does the failure give warning through vibration, temperature, wear measurement or inspection findings?
- Is there an approved alternate, a repair route or an exchange unit?
- Could a failure create a safety or environmental event, such as a fan or conveyor failure near people?
Critical spares by cement process area
The table below is a starting point for a criticality review. Every plant should confirm it against its own equipment list, supplier lead times and failure history.
| Process area | Typical critical spare | Why a shortage hurts | Common stocking approach |
|---|---|---|---|
| Crushing and raw milling | Mill rollers, grinding table segments, main gearbox bearings, classifier parts | Raw meal supply falls and kiln feed becomes unstable | Insurance spare for main drive items, planned wear part orders |
| Preheater and calciner | Cyclone dip tubes, flap valve parts, refractory anchors and shapes | Blockages and heat loss shorten run time | Kitted for planned stops, shapes ordered by campaign |
| Rotary kiln | Support roller bearings, girth gear and pinion parts, drive gearbox spares, kiln shell seal parts | Kiln stoppage is the most expensive outage in the plant | Insurance spare plus rotable repair programme |
| Clinker cooler | Grate plates, hydraulic cylinders, cooler fan bearings, drive components | Poor cooling limits kiln speed and clinker handling | Min and max for grate plates, spare cylinders on site |
| Fans and dust control | ID fan bearings, rotors, bag filter bags and cages, rotary valves | Emission limits and process draught are at risk | Min and max, with a documented replacement kit |
| Cement grinding and packing | Roller press rolls and studs, separator parts, packing machine components | Dispatch and cement availability suffer | Wear part forecasting and vendor agreements |
| Electrical and automation | Drives, motor spares, protection relays, PLC cards, instrument sensors | Small parts can stop a very large machine | Standardised spares and tested spare cards |
Audit your critical spares before the next shutdown
Bring your equipment list and spare parts register. See how criticality, lead time and reserved parts can sit in one place beside your work orders.
Size stock to lead time and risk, not to habit
Reorder logic for fast-moving wear parts can be built on demand during lead time. Insurance spares need a different logic, because they may never be used and the question is whether the plant can afford to be without them.
Reorder point for consumables
Average daily use multiplied by supplier lead time in days, plus safety stock for variation in use and delivery.
How the logic changes by part type
- Consumable wear parts: use consumption history, shutdown demand and supplier delivery reliability to set minimum and maximum levels.
- Insurance spares: justify by consequence of failure, lead time and the cost of downtime compared with carrying cost. Decide once, document the reasoning and review yearly.
- Rotables: track each serial number through removal, repair, test and return to stock so the pool is always known.
- Shared or pooled spares: agree access terms with sister plants or suppliers and record them in the register so planners know the option exists.
- Obsolete or low-use items: review regularly so storage cost and working capital do not hide the genuinely important items.
Include process and fuel changes in the forecast
Alternative fuels, changes in raw material hardness and output increases can shorten the life of liners, rollers, refractory and fan components. Reorder points that ignore these shifts will always lag. Reviewing wear rates after each campaign keeps forecasts honest.
A six-stage lifecycle for shortage prevention
01
Register
Link every critical spare to the equipment it protects, with part numbers, drawings and approved alternates in one record.
02
Rank
Score consequence, lead time, warning signs and alternates. Flag the top group as critical.
03
Set rules
Assign min, max, insurance or pooled status, and a named owner for each critical item.
04
Connect to work
Attach parts lists to preventive maintenance and shutdown work orders so demand is visible early.
05
Monitor
Watch stock, open requisitions, lead times and condition findings on a shared dashboard.
06
Review
After each outage and failure, update criticality, quantities and supplier notes from what actually happened.
Connect condition findings to purchasing
The best early warning is wasted if it stays in a vibration report or an inspector's notebook. Condition monitoring results, thickness readings, thermography findings and inspection notes should create a corrective work order with a parts requirement attached.
Before
- Findings sit in separate files.
- Purchasing hears about the part during the stoppage.
- Stock is checked by phone or by walking the shelves.
- Rush orders are placed with premium freight.
After
- Findings become work orders with a due window.
- Parts are reserved or requisitioned at the time of the finding.
- Stock and open orders are visible to planner and storekeeper.
- Orders are placed inside the lead time.
KPIs that show whether shortages are really falling
Critical spares availability
Share of critical items with stock at or above the agreed level on the day it is measured.
Stockout-related delay
Hours of work delayed or extended because a part was not available when planned.
Expedite spend share
Premium freight and rush purchases compared with total spare parts spend.
Kitting completeness
Percentage of planned jobs with every part reserved before the work start date.
Inventory record accuracy
Result of cycle counts comparing system quantity with physical quantity.
Lead time coverage
Open critical items where the planned need date falls inside the supplier lead time.
Where Oxmaint maintenance management software helps
Oxmaint brings assets, work orders, inventory and reporting into one maintenance workflow, which is where shortage prevention succeeds or fails.
Asset and inventory records
Link spare parts to the assets they protect, so a planner can see which kiln, mill or fan a part supports.
Work orders with parts
Attach parts to preventive and corrective work orders so demand shows up before the job starts.
Reorder levels and visibility
Set minimum and maximum levels, track usage and review items that sit below target.
Inspections and mobile use
Capture findings in the field so condition information reaches planning without delay.
Scheduling for shutdowns
Build outage task lists and check parts readiness against each task.
Reports and dashboards
Report on stock, usage and delays to support purchasing and budget discussions.
Shutdown parts readiness checklist
- Every task in the shutdown scope has a parts list reviewed by the planner and the storekeeper.
- All long lead items have a confirmed delivery date that falls well ahead of the stoppage.
- Refractory, wear liners and bearings are physically counted and checked for damage in storage.
- Special tools, lifting gear and consumables such as seals and fasteners are included in the kit.
- Rotables out for repair have a confirmed return date and a test record.
- Alternate parts have been approved by engineering before being used.
- Unused parts are returned and booked after the outage so records stay accurate.
Common mistakes when setting minimums and maximums
- Copying the OEM recommended spares list without checking it against the plant's own failure history, operating hours and raw material conditions.
- Setting the same minimum for every plant item, so low-risk fasteners and high-risk bearings receive equal attention.
- Ignoring delivery performance. A supplier quoting eight weeks but delivering in twelve makes every reorder point wrong.
- Counting stock that is reserved for another job as available, which makes coverage look healthier than it is.
- Failing to update the record after a part is repaired, substituted or consumed during emergency work.
Questions that improve supplier resilience
A storeroom alone cannot remove supply risk. Procurement and engineering should review sourcing for the highest-risk items at least once a year.
- Is there a second approved manufacturer, or an approved local fabricator who can work from drawings?
- Can the supplier hold consignment or call-off stock, and under what terms?
- Are repair and refurbishment services available, and what is their real turnaround?
- Does the drawing package exist in the plant records, so manufacture can start without delay?
Who should own shortage prevention
Shortages sit between departments, which is why they persist. Clear ownership turns a shared problem into a managed one.
- Maintenance planner: owns parts lists on planned work and confirms kit readiness before each job.
- Storekeeper: owns stock accuracy, cycle counts and reservations.
- Buyer: owns supplier lead time records and delivery follow-up.
- Reliability engineer: owns criticality ranking and approved alternates.
- Plant manager: owns the decision on insurance spares and the budget behind them.
Frequently asked questions
What is a critical spare part in a cement plant?
It is a part whose absence can stop a production unit or create a safety or environmental event, especially when lead time is long.
How often should criticality be reviewed?
Review yearly and after any major failure, equipment change or supplier change. Oxmaint can keep the history in the asset and inventory records.
Should every critical part be stocked on site?
No. Some are better pooled, repaired or covered by a supplier agreement. The decision should rest on consequence, lead time and cost.
How do work orders help prevent shortages?
Work orders with linked parts reveal demand early, so purchasing can order inside the lead time.
Can we see this on our own data?
Yes. You can book a demo and walk through your register.
Stop shopping for parts during the stoppage
Give planners, storekeepers and engineers one shared view of critical spares, open requisitions and planned work.