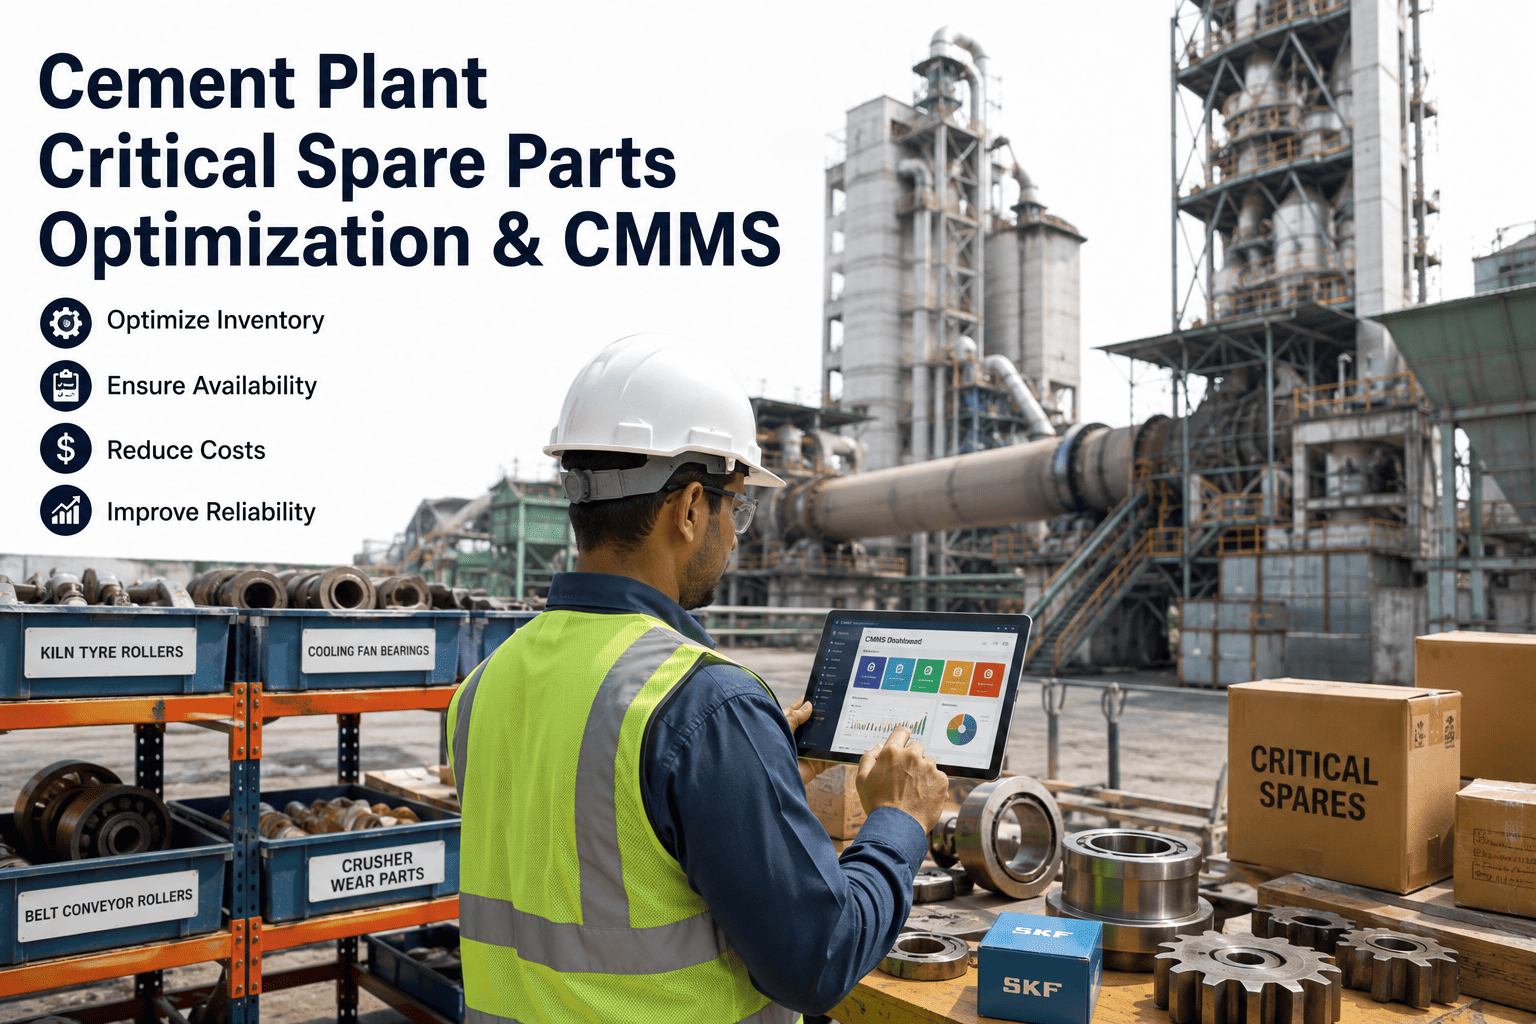
Critical spare parts optimization in a cement plant is where maintenance strategy meets working capital reality — a single missing girth gear pinion can idle a 5,000 TPD kiln for twelve weeks, while a warehouse full of rarely-used hydrator seals ties up cash that should be earning elsewhere. The plants that win this balance classify spares by true operational risk, set reorder points from lead-time data rather than gut feel, and let a CMMS enforce min/max logic so buyers and planners stop firefighting. This guide walks through criticality classification, stocking strategy, lead-time management, and the CMMS-driven inventory approach that keeps cement critical spares available without carrying dead stock. You can put it into practice today with a Start Free Trial of Oxmaint, or read on for the full framework.
Are your cement critical spares protecting uptime — or just sitting on the shelf?
For a typical 2 MTPA plant, the gap between a 14-day safety stock and a 90-day overstock on high-value items can mean $180K–$420K of frozen working capital per year. The right CMMS-driven strategy cuts that gap without adding outage risk.
Rank every spare by the cost of the hour it is missing
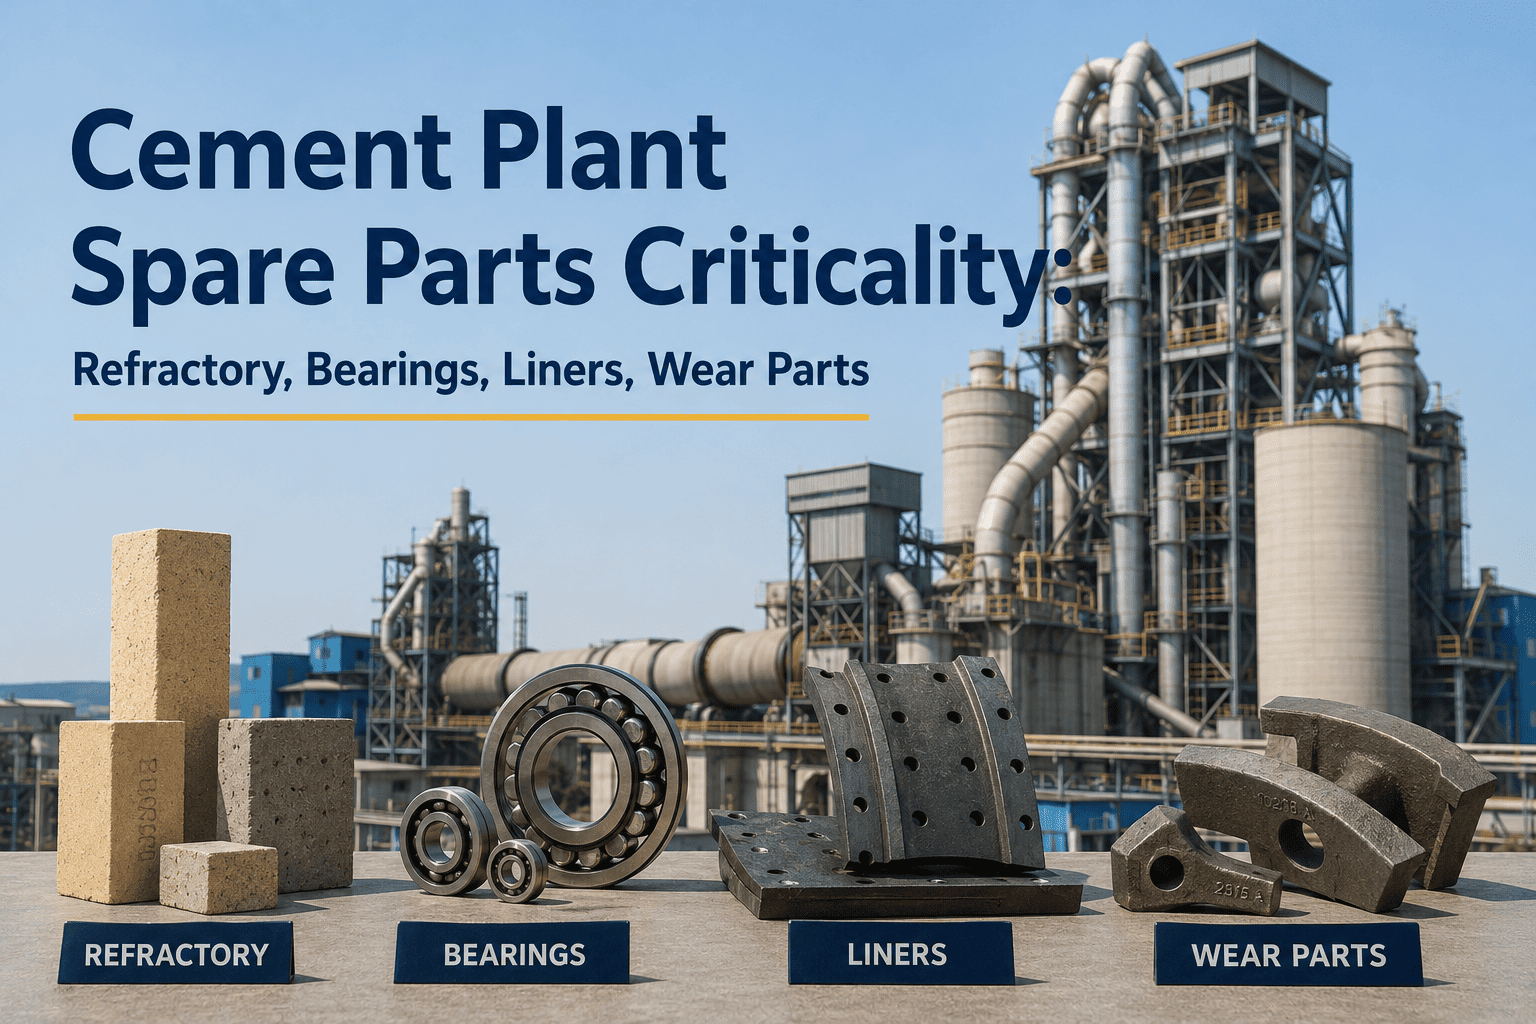
Criticality is not the same as price. A $400 kiln burner nozzle that takes six weeks to remanufacture is far more critical than a $4,000 hydraulic power unit kept in stock for a redundant conveyor. Classify each spare against four factors, then assign an ABC+Criticality tier that drives reorder behavior.
Does failure stop the kiln, mill, or finish mill? A spare on the critical path of a single-day 5,000 TPD line carries $180K–$260K of lost margin per day.
A forged kiln tyre runs 26–42 weeks; a girth gear pinion 16–24 weeks. Spares with lead times above 12 weeks that gate production must be stocked.
Single-source, import-dependent, or geographically remote suppliers raise effective lead time by 30–60%. Track on-time delivery rate per vendor in the CMMS.
Use MTBF and failure mode data from the CMMS work-order history. Items failing more than once per 18 months on the same asset belong on the critical list.
| Tier | Definition | Stock policy | Review cadence | Typical examples |
|---|---|---|---|---|
| A — Critical | Stops production, lead time > 12 weeks | Always-stocked, safety stock + 1 | Monthly | Kiln tyre, girth gear, pinion, mill trunnion |
| B — Essential | Reduces throughput or risk, lead time 4–12 weeks | Min/max with safety stock | Quarterly | Ball mill liners, fan impellers, slide shoe bearings |
| C — Routine | Standard wear parts, lead time < 4 weeks | Min/max, lean reorder | Half-yearly | Seals, bearings, filter bags, coupling elements |
| D — Insurance | Rare failure, catastrophic if it occurs | Single unit held, justify annually | Annual | Preheater fan shaft, ID fan rotor, gearbox |
Set reorder points from data, not from the last outage
Reorder point and safety stock should be calculated from historical consumption and supplier lead-time variance, then enforced automatically by the CMMS. Manual spreadsheets drift; planners forget to re-order; the plant pays for it at 2 a.m. on a Sunday.
Covers supplier variability and demand spikes. For a girth gear pinion averaging 18-week lead with a 6-week variance, and 0.02 units/day peak demand, SS ≈ 0.84 units — round up to 1.
When on-hand drops below ROP, the CMMS auto-generates a purchase request. For a ball mill liner consuming 0.04 units/day over a 10-week lead with SS of 2, ROP = 4.8 → reorder at 5.
A 2 MTPA plant holding 4,200 SKUs was carrying $2.9M in spares. After re-tiering 380 items from "always stocked" to "min/max" and applying CMMS-calculated ROP/SS to the top 120 critical items, inventory dropped to $2.1M within nine months — freeing $800K of working capital — while stockout incidents on critical assets fell from 11 per year to 2. The freed cash funded a clinker cooler grate replacement a full quarter ahead of schedule.
Long-lead castings are where cement plants actually bleed
The four asset classes below account for 60–75% of unplanned downtime days in most cement operations — not because the failure is unexpected, but because the spare is not on the floor when it happens. Build a written lead-time strategy for each.
Kiln tyre & riding ring
A forged tyre is a single-point-of-failure with no off-the-shelf substitute. Maintain one insurance spare for each active kiln, condition-monitor with periodic NDT crack inspection, and pre-stage the machining contractor so refit downtime stays under 14 days.
Girth gear & pinion set
Document gear geometry, tooth counts, and helix angle in the CMMS asset record so a replacement can be quoted immediately. Hold one pinion as a rotating spare; full gear sets are justified only when measured backlash exceeds 1.5× new-build tolerance.
Ball mill & vertical roller mill liners
Track wear rates by compartment via monthly thickness readings entered against the CMMS work order. Reorder at 60% of nominal wear life, not at failure. Pre-stage a full liner set one month before projected change-out to avoid premium freight from Europe.
Preheater & ID fan rotors
Vibration trend in the CMMS should trigger rotor replacement planning at ISO 10816 zone C, not zone D. Hold a balanced spare rotor for each critical fan and pre-book the crane slot — the rotor is cheap next to a 9-day kiln stop.
What the CMMS actually does that spreadsheets cannot
A purpose-built maintenance CMMS turns spare parts strategy into enforced process. The features below are the difference between a plant that knows its reorder points and a plant that acts on them automatically.
Auto reorder triggers
When on-hand crosses ROP, the CMMS generates a purchase request pre-filled with vendor, part number, and preferred quantity. No planner needs to remember.
Lead-time analytics
Actual supplier lead times are captured against every receipt, so safety stock recalculates from real data — not the supplier's promised date that was last updated in 2019.
BOM-linked spares
Each asset's bill of materials links critical spares directly to work orders, so a kiln stoppage automatically reserves and pulls the right pinion, liner, or seal from stores.
Criticality-based alerts
A-tier stockouts page the maintenance manager; B-tier trigger a daily digest; C-tier sit in the weekly review. Attention is routed by operational risk, not alphabet.
Dead-stock reports
Quarterly reports flag items with zero movement in 24 months, with original cost and current book value — the input for disposal, redeployment, or vendor return negotiations.
Multi-store visibility
For multi-site operators, the CMMS shows spare availability across all plants — so a sister plant's pinion can be transferred in days instead of waiting 22 weeks for a new casting.
How mature cement spare parts programs measure up
The table below aligns common CMMS inventory KPIs with ISO 55000 asset-management principles and TPM participation targets. Use it to benchmark your current program before scoping a CMMS rollout.
| KPI | Definition | Reactive plant | Industry average | Best-in-class |
|---|---|---|---|---|
| Spare parts availability | % of work orders fulfilled from stock on first request | 72% | 88% | 96%+ |
| Inventory turnover | Annual issue value ÷ average inventory value | 0.6× | 1.2× | 2.0×+ |
| Dead stock ratio | % of SKUs with zero movement in 24 months | 34% | 18% | Under 8% |
| Critical stockout days | Days per year A-tier spares unavailable | 22 days | 6 days | Under 1 day |
| Emergency purchase ratio | % of POs flagged emergency / expedite | 19% | 8% | Under 3% |
Stop guessing at reorder points. Let the CMMS enforce them.
Roll out criticality tiering, ROP/SS logic, and lead-time analytics across your plant in weeks, not quarters — with a CMMS built for cement maintenance teams.
Cement critical spares & CMMS — what plant teams ask
Put your cement critical spares on autopilot.
Criticality tiering, reorder-point logic, lead-time analytics, and multi-store visibility — purpose-built for cement maintenance teams.
Free 14-day trial · No credit card