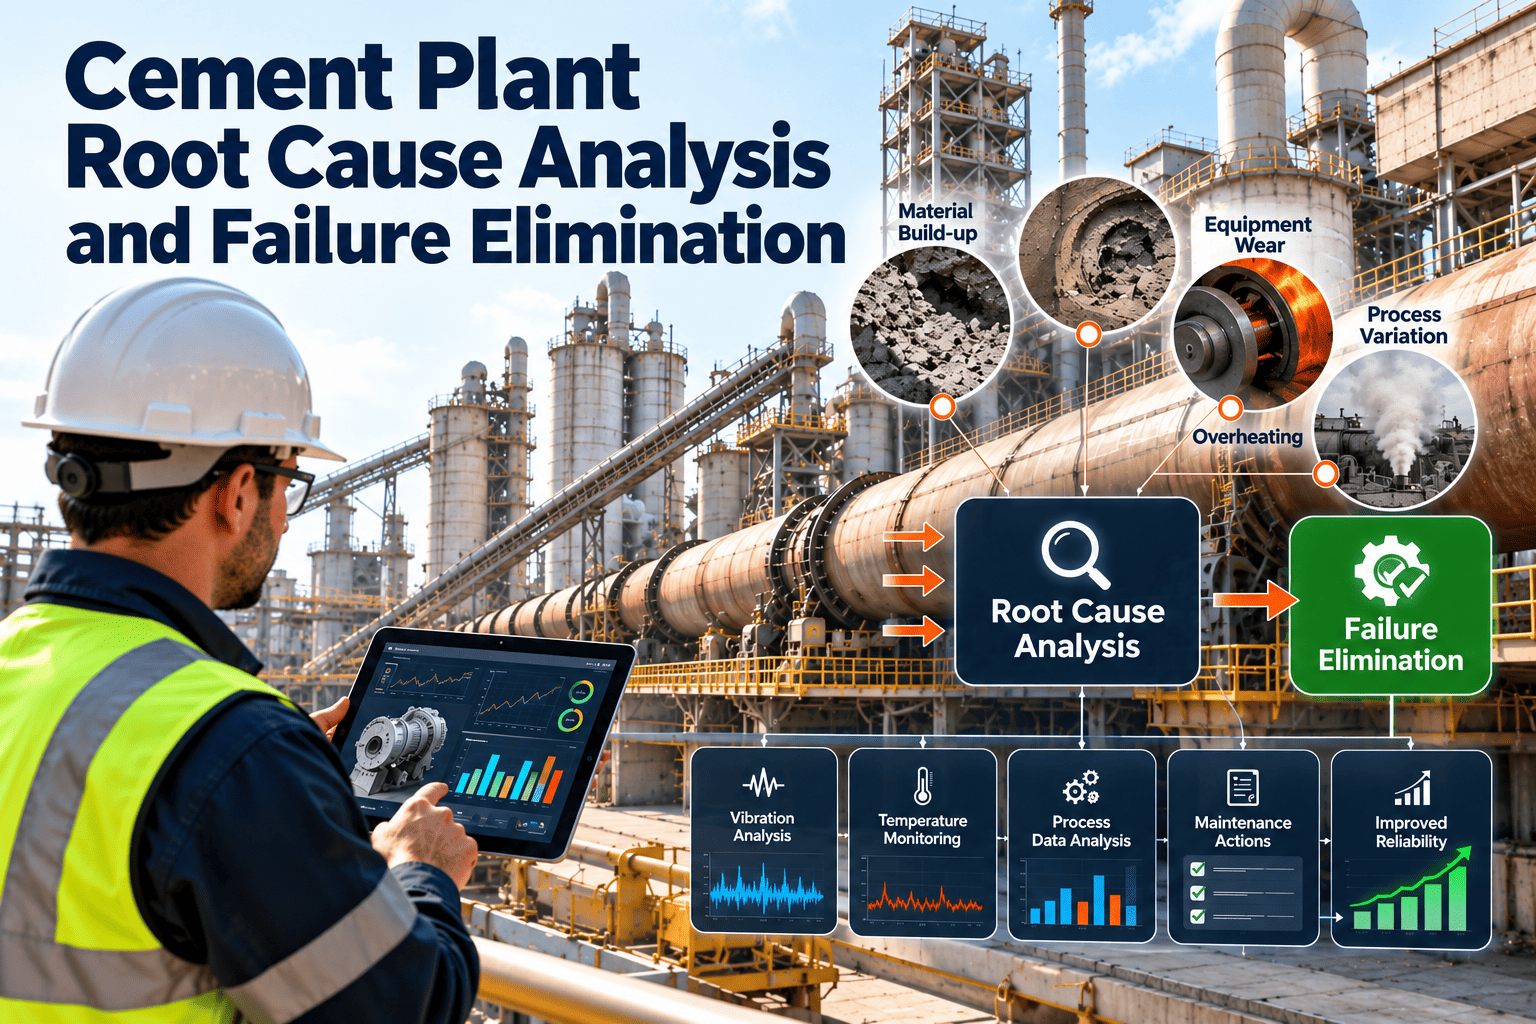
Every cement plant knows the failure that keeps coming back. A kiln support roller bearing overheats, a raw mill roller needs another weld repair, or an ID fan loses balance again after a restart. The team fixes the symptom, production resumes, and the same work order reappears months later. Real elimination needs disciplined root cause analysis, supported by clean failure records and tracked actions. This guide shows how to structure that work, and how a cement maintenance management platform keeps the evidence and follow-up in one place.
Cement Plant Root Cause Analysis and Failure Elimination
Five Reasons Cement Plants Keep Fixing the Same Failure
Pressure to restart
Vague failure codes
Split ownership
Actions without tracking
No effectiveness check
What Repeat Failures Really Cost
A repeat failure is more expensive than the first one because the plant already had the chance to learn from it. Costs also appear in places the work order never shows.
The First 24 Hours After an Unplanned Stop
Most useful evidence disappears quickly. Photos, oil samples, process trends and operator accounts should be captured before repairs begin.
Building a Failure-Coding Library That Supports RCA
Analysis is only as good as the failure history. A short, consistent set of codes lets the plant filter, count and compare events instead of reading free text.
Weak codes
- Breakdown
- Mechanical fault
- Motor problem
- Other
Useful codes
- Bearing overheating with lubrication starvation
- Gearbox oil contamination
- Roller hydraulic pressure loss
- Cyclone blockage from build-up
Fields every cement failure record should carry
- Asset and component, such as ID fan drive-end bearing
- Failure mode, cause category and how it was detected
- Process condition at the time and duration of the stop
- Parts consumed, labour hours and evidence attached
From Symptom to Root Cause: An Illustrative Why Chain
The example below is a generic illustration of method, not a claim about any specific plant. It shows how each answer must be supported by evidence before the next question.
What the example teaches
- The bearing was never the root cause, only the visible casualty
- Replacing the bearing again would have guaranteed a fourth failure
- The fix is a scheduled inspection task and a defined alarm response, both trackable
Deciding Which Failures Deserve a Full Analysis
Analysis capacity is limited. Use simple triggers so effort goes to events that matter most.
| Criterion | Question to ask | Example trigger |
|---|---|---|
| Safety or environment | Did the event put people or permits at risk? | Any incident or near miss involving the asset |
| Production impact | Did it stop the kiln or a main mill? | Stops longer than a plant-defined duration |
| Repeat frequency | Has the same failure mode occurred recently? | Second occurrence within a set period |
| Repair cost | Was the cost far above normal? | Spend above a plant-defined threshold |
| Spare risk | Was the part hard to source? | Long lead time or single-supplier item |
Matching the RCA Method to the Failure
Not every stop deserves a full investigation. Use a simple method for minor events and reserve deeper tools for costly or safety-relevant failures.
| Method | Best used for | Strength | Watch out for |
|---|---|---|---|
| Five whys | Single-path failures on one machine | Quick and easy to teach | Can stop early or follow opinion rather than evidence |
| Cause and effect diagram | Failures with several possible contributors | Organises ideas across people, method, machine, material and environment | Lists possibilities without proving them |
| Fault tree analysis | Major stops with multiple combined events | Shows how events combine logically | Needs time and facilitation |
| Failure mode and effects analysis | Preventing failures on critical assets before they happen | Prioritises risk across many failure modes | Becomes shelfware if not updated after real failures |
| Barrier analysis | Safety, environmental or quality incidents | Finds which protections failed or were absent | Requires clear definition of intended barriers |
Make Every Failure Investigation Leave a Permanent Record
Condition Data That Strengthens an Analysis
Condition monitoring tells the team how the asset behaved before it failed. That history separates a sudden event from a slow degradation that went unnoticed.
Recurring Failure Patterns Across the Cement Process
The causes below are common contributing factors worth testing, not conclusions. Every analysis must confirm cause with plant evidence.
| Area | Recurring failure | Causes to test |
|---|---|---|
| Crushing and conveying | Hammer and liner wear, bucket elevator chain or belt problems | Material hardness changes, mistracking, lack of tension checks, wrong wear part grade |
| Raw and cement mills | Roller and table wear, hydraulic faults, vibration trips | Feed variation, accumulator pressure loss, foreign metal, grinding bed instability |
| Rotary kiln | Support roller and tyre issues, refractory failures, shell hot spots | Alignment drift, lubrication condition, thermal cycling, unstable burning |
| Preheater | Cyclone blockages, build-up | Chlorine and sulphur cycles, false air, fuel quality, cleaning practice |
| Clinker cooler | Grate plate breakage, hydraulic drive faults, fan problems | Overloading, red river conditions, undersized spares, air distribution issues |
| Fans and drives | Imbalance, bearing failures, coupling wear | Dust build-up, soft foot, misalignment, lubrication errors |
Choosing Actions That Actually Remove the Cause
Not all actions are equal. Strong actions change the plant or the equipment, while weak ones rely on people remembering to be careful.
Eliminate the cause
Redesign or upgrade
Detect early
Standardise the procedure
What Changes When RCA Is Built Into the Work Order
Before: repair-only workflow
- Free-text failure descriptions that cannot be filtered
- Photos on personal phones, parts discarded
- Meeting notes with no action owners
- Repeat failures discovered through memory
After: RCA-linked workflow
- Standard problem, cause and remedy codes on every job
- Evidence attached directly to the asset record
- Corrective actions as tracked tasks with due dates
- Repeat failure reports by asset, component and cause
Who Does What in a Cement Plant RCA
Common RCA Mistakes in Cement Plants
- Stopping at the failed component instead of asking why it failed
- Naming human error as a root cause without examining training, tools, procedures or workload
- Skipping evidence because the repair was urgent
- Producing long reports that nobody turns into scheduled work
- Keeping each investigation in a separate file so patterns across assets are never seen
- Closing the case without checking, weeks later, that the failure has not returned
Building the habit over 90 days
How Oxmaint Supports Failure Elimination
Oxmaint structures the maintenance data that RCA relies on. The analysis still requires skilled people, but their time goes to thinking, not searching.
Feeding RCA Findings Back into Preventive Maintenance and Spares
An analysis that ends in a report changes nothing. The value comes when findings reshape routines, inspection points and the parts held in stores.
Update the maintenance plan
- Add inspection steps for the weakness found
- Adjust task frequency based on actual failure interval
- Add measurable acceptance limits to checklists
- Retire tasks that never catch real problems
Update stores and procedures
- Stock critical spares for long-lead components
- Specify the improved part grade or material
- Revise work instructions with the lesson learned
- Brief crews and record that the briefing happened
Capturing evidence on mobile
- Technicians attach photos, readings and notes to the work order at the equipment
- Required fields prompt for failure mode and suspected cause before closure
- Inspection rounds flag early signs, such as leaks, noise and hot spots, as corrective requests
- Supervisors review repeat requests by asset in the weekly planning meeting
KPIs That Show Whether Failures Are Disappearing
Checklist for a Complete RCA Close-Out
Before closing
- Evidence attached and root cause supported by it
- Contributing causes recorded separately
- Corrective and preventive actions assigned
- Spares and procedures updated if affected
After closing
- Effectiveness review scheduled at a fixed date
- Similar assets checked for the same weakness
- Lessons shared in the daily or weekly planning meeting
- FMEA or inspection plans revised