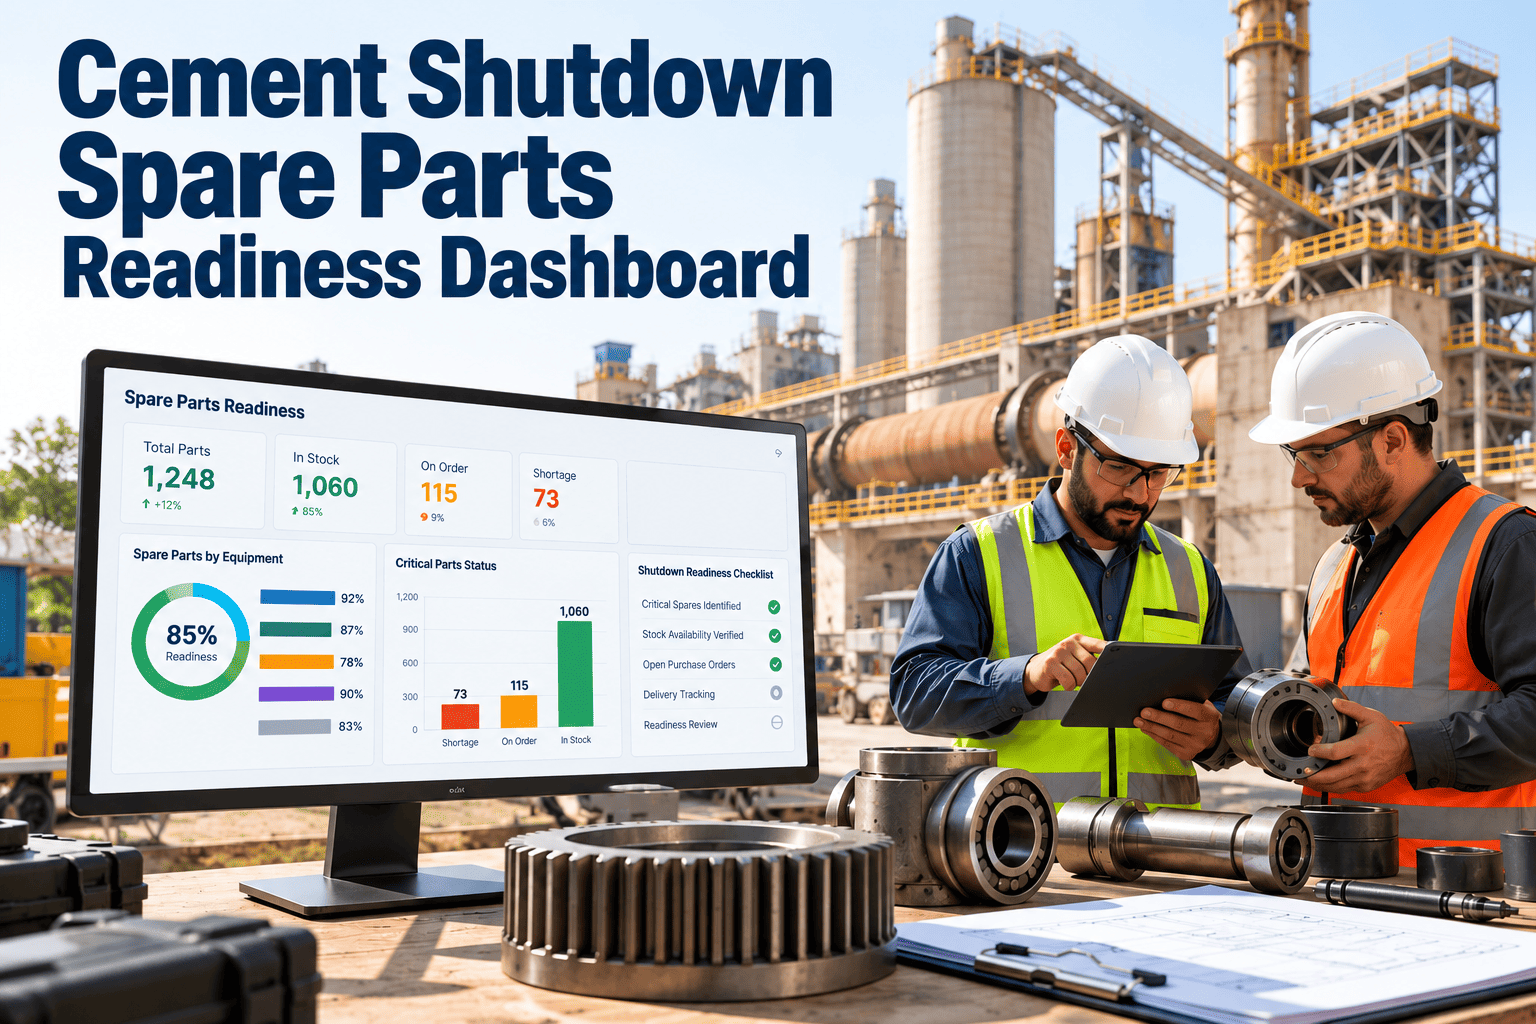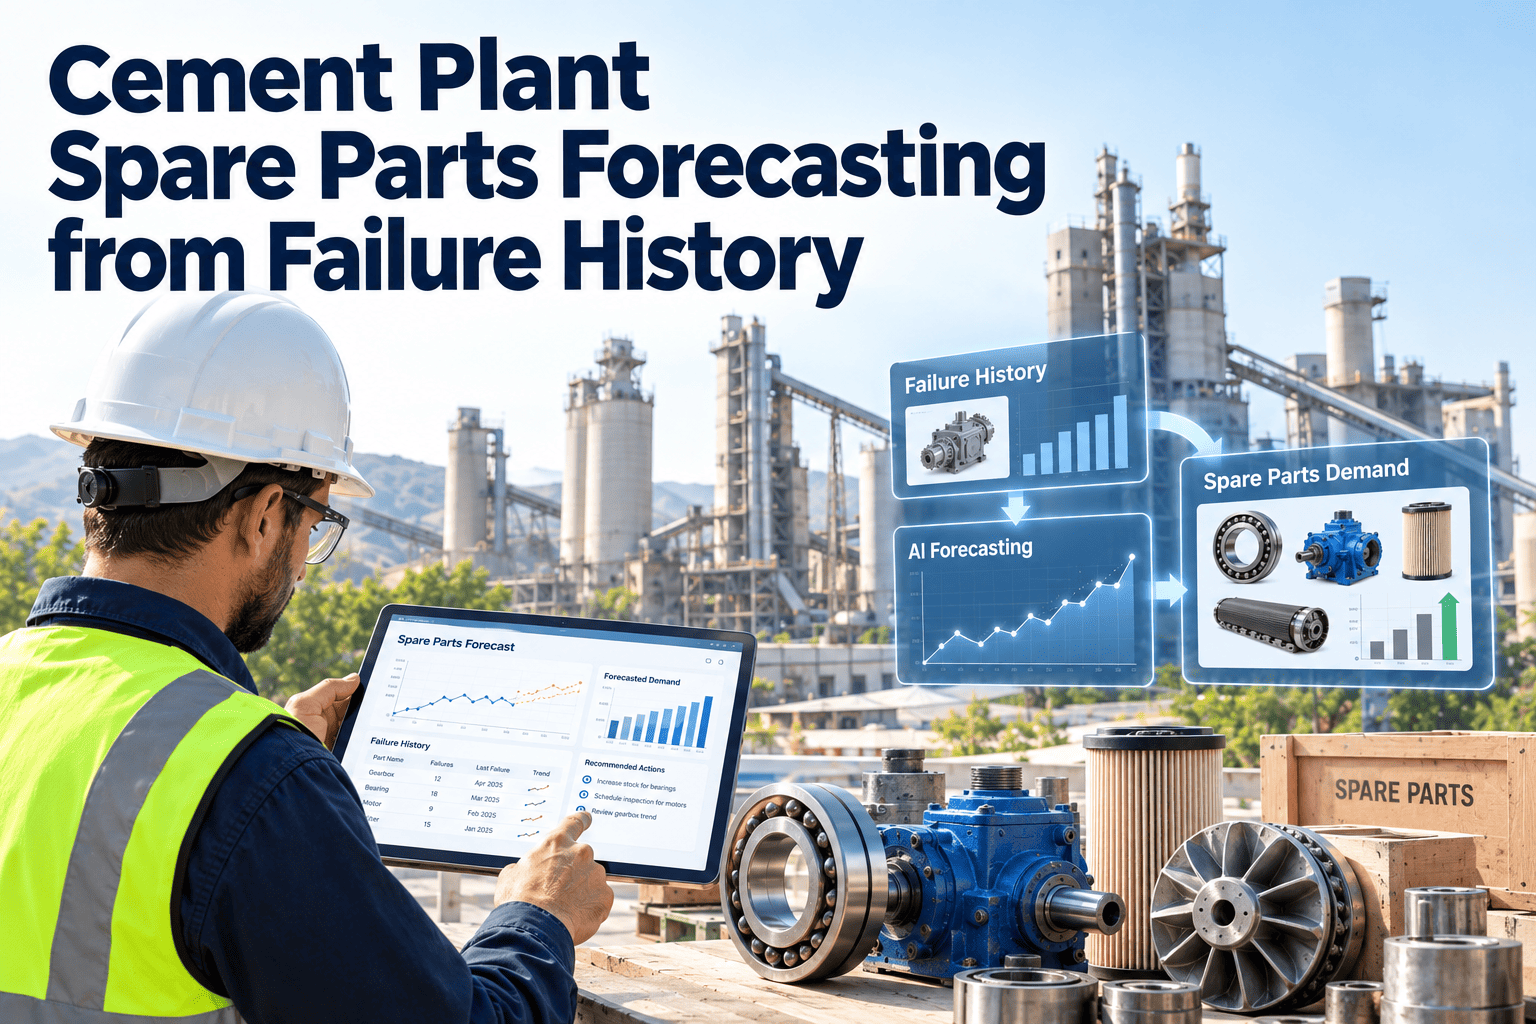
Cement plants carry thousands of spare parts, and most of them are used rarely. A kiln drive component may sit on a shelf for years and then be needed within hours, while a pulse valve diaphragm turns over every few months. Forecasting from last year's consumption alone fails for parts like these, because the demand is driven by failures, not by steady usage. This guide shows how to turn failure history into spare parts forecasts, reorder points, and stocking decisions, and how Oxmaint maintenance software keeps the underlying records in one place.
Cement Plant Spare Parts Forecasting from Failure History
Forecast what will fail, when it is likely to fail, and how long replacement takes. Stock the parts where that combination hurts most, and stop guessing on the rest.
Why usage-based forecasts fail for maintenance spares
Ordinary inventory methods assume steady, repeated demand. Spare parts demand is lumpy, tied to specific machines, and linked to how those machines age.
The failure history you need before forecasting
A forecast is only as good as the records beneath it. If work orders do not capture the right fields, fix that first. Better data beats a more complicated model.
From failure history to a reorder point
The method is short and can be done in a spreadsheet or inside a maintenance system. The work is in preparing clean inputs, not in the arithmetic.
A worked example with simple numbers
The figures below are illustrative. They show the logic only, so use your own failure counts, population, and lead times.
- A plant runs 10 identical drive units and history suggests each fails about once every 5 years on average.
- That gives about 2 expected failures per year across the population, or about 0.0055 per day.
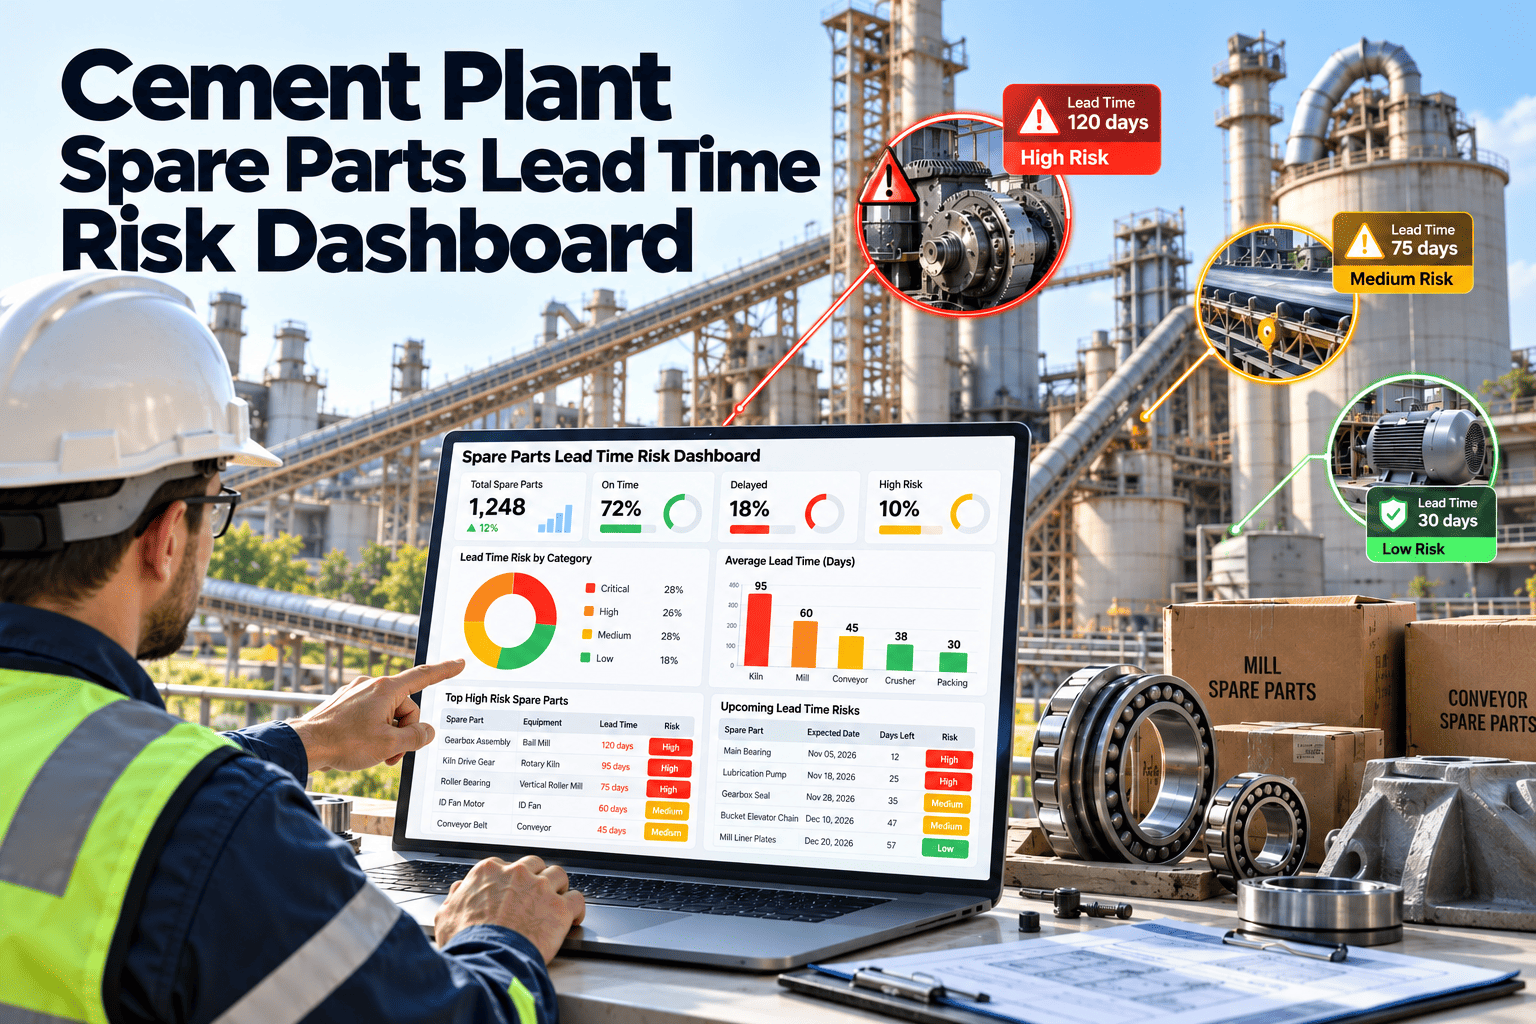
- The supplier quoted 20 weeks, but the last three orders arrived in 26 weeks, so planning lead time is 26 weeks, or 182 days.
- Expected demand during lead time is about 1 unit, so the base reorder point is 1.
- Because a missing drive stops a production line, the plant adds one unit of safety stock, giving a reorder point of 2.
Keep failure history where forecasts can use it
Record part, failure mode, run hours, and parts issued on every work order, and give planners a single view of stock, lead times, and demand.
Match the stocking approach to the failure pattern
Not every part fails in the same way. The pattern in your history tells you which forecasting approach fits.
Cement plant parts and what drives their demand
Use the table as a prompt for your own register. Demand drivers and lead times vary by plant, supplier, and equipment generation.
| Part group | Main demand driver | Forecast basis | Stocking note |
|---|---|---|---|
| Filter bags, cages, and pulse valve diaphragms | Operating hours and cleaning cycles | Age and condition trend per compartment | Plan bag sets for outages and hold valve parts for repeat failures |
| Clinker cooler grate plates and hydraulic parts | Wear and thermal cycling | Age, inspection findings, and failure history | Order ahead of planned stops, hold hydraulic critical items |
| Mill liners and grinding media | Wear rate per tonne ground | Throughput-based wear model | Align orders with scheduled relining |
| Gearboxes and kiln drive components | Wear-out and lubrication condition | Condition monitoring plus failure history | Insurance spare or access to a repair pool |
| Fan bearings and couplings | Vibration and temperature condition | Condition trend and past failures | Hold for critical fans, standardise where possible |
| Weigh feeder load cells and belts | Wear and drift | Calibration history and failure count | Keep a small buffer for key feeders |
| Drives, control cards, and sensors | Random failures | Population failure rate | Hold critical cards and standardise across lines |
Scoring criticality before you forecast
Forecast effort should follow consequence. A simple score applied to each part group tells you where to spend analysis time and where basic rules are enough.
Questions to ask for each part
- Does failure stop the kiln, a mill, or a packing line?
- Is there a standby unit or a workaround while waiting?
- How long does the supplier take, including shipping and customs?
- Can the part be repaired locally, and how quickly?
- Is the part shared with other machines that raise the odds of need?
How to use the answers
- Score each answer on a short scale and add the results.
- Treat the highest scores as the critical list for forecasting.
- Give mid-range parts min and max rules with periodic review.
- Leave low scores to simple reorder rules or on-demand purchase.
- Re-score after major failures or equipment changes.
Parts with little or no failure history
Some of the most critical parts have rarely or never failed on site. A forecast cannot come from your own data alone, so combine other sources with judgement.
Repair, pool, or buy: choosing the response to a rare failure
Holding a full new spare is only one answer. Compare the alternatives on cost and time before committing capital to stock.
| Option | Works best when | Main risk | What to record |
|---|---|---|---|
| Hold a new spare | Failure is costly and lead time is long | Capital tied up and ageing in storage | Storage condition, shelf life, and inspection dates |
| Hold a repairable spare | The part can be refurbished by a trusted workshop | Repair time and quality variation | Repair history, turnaround time, and test results |
| Share a pool across plants | Several sites use the same part | Transport time and unclear ownership | Location, owner, and transfer records |
| Supplier agreement | Supplier can guarantee fast delivery | Agreement not honoured under pressure | Delivery performance against the agreement |
| Buy on demand | Low impact and short lead time | Delay if the supplier is unexpectedly slow | Actual delivery times for each order |
Data problems that distort spare parts forecasts
Most forecasting disappointment traces back to a few record-keeping issues. Fix these before blaming the method.
- Duplicate part numbersThe same bearing held under three codes splits its demand and hides true usage.
- Free-text failure descriptionsWithout standard failure modes, similar failures cannot be grouped and counted.
- Parts issued to the wrong jobStores issues recorded against a general account break the link between failure and part.
- Stale lead timesA lead time copied from an old order may no longer match what suppliers deliver today.
- Mixing planned and failure demandOverhaul orders can inflate the apparent failure rate. Tag replacement type on every job.
A quarterly review cycle that keeps forecasts honest
Forecasts drift as equipment ages and suppliers change. A fixed cycle keeps the numbers close to reality without constant manual effort.
Pulling planned demand forward from the shutdown scope
Planned stops are the most predictable source of demand. Treat the scope list as a forecast and the parts list as an order that must be placed early.
- Months beforeFreeze the scope, identify long lead items, and place orders with confirmed delivery dates.
- Weeks beforeCheck receipt, inspect delivered parts, and reserve them against the planned work orders.
- During the stopRecord parts actually used and any extra needs found when equipment is opened.
- After the stopReturn unused items, update stock records, and feed findings into the next forecast.
Standardising parts across lines to cut stock
Every extra part variant needs its own stock, forecast, and reorder point. Reducing variants is often the cheapest way to improve coverage.
Measures that show whether forecasting is working
Track both service and cost. A good program reduces stockouts without simply adding stock.
How Oxmaint supports spare parts forecasting
Oxmaint is maintenance management software. It holds the work order, asset, and inventory records that failure-based forecasting depends on, so planners work from facts instead of memory.
Spare parts forecasting FAQs
Why not forecast spares from past usage?
Spares demand is driven by failures and planned work, not steady consumption. Averages hide long gaps followed by sudden need.
How much failure history is enough?
More is better, but even a few years of clean records for identical parts across a population is useful. Start with the critical list.
Should we stock every critical part?
No. Weigh consequence, lead time, and repair options. Some parts suit shared pools or supplier agreements, and Oxmaint tracks stock and demand for each choice.
How often should reorder points be reviewed?
Quarterly for critical parts is a common starting point, with extra reviews after major failures or supplier changes.
What is a good first step?
Clean the failure records for your top critical parts. Book a demo to plan the data fields and reorder logic.
Stock for the failures you can actually predict
Give maintenance, stores, and purchasing one shared record of failures, parts, and lead times so the right spares are on the shelf before they are needed.