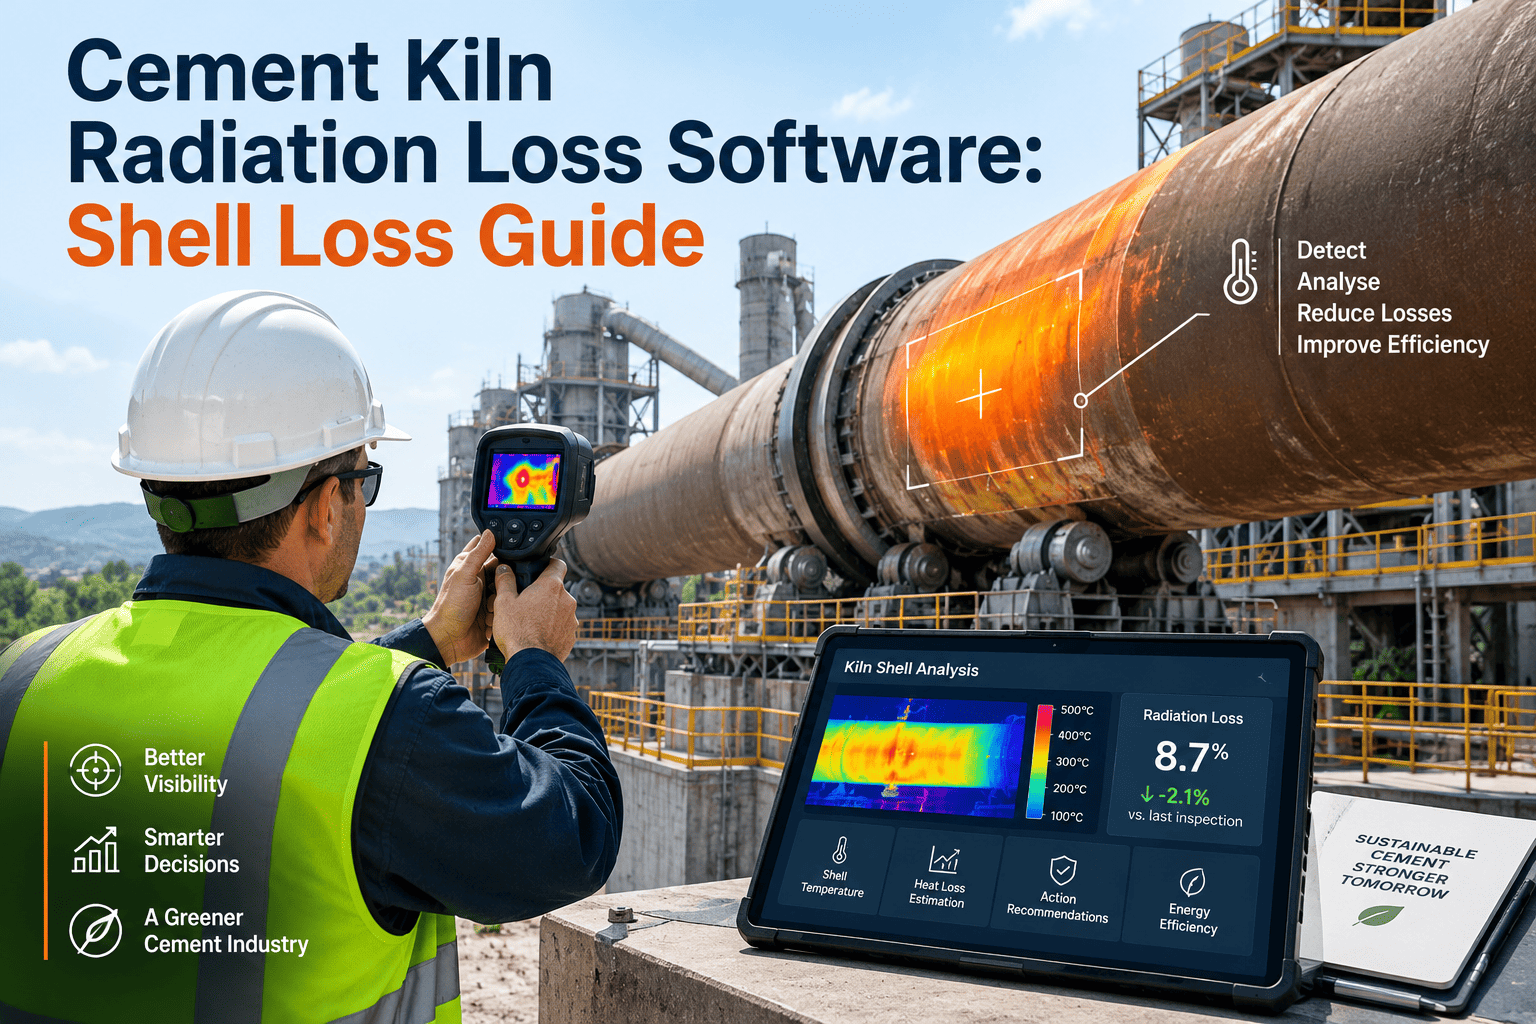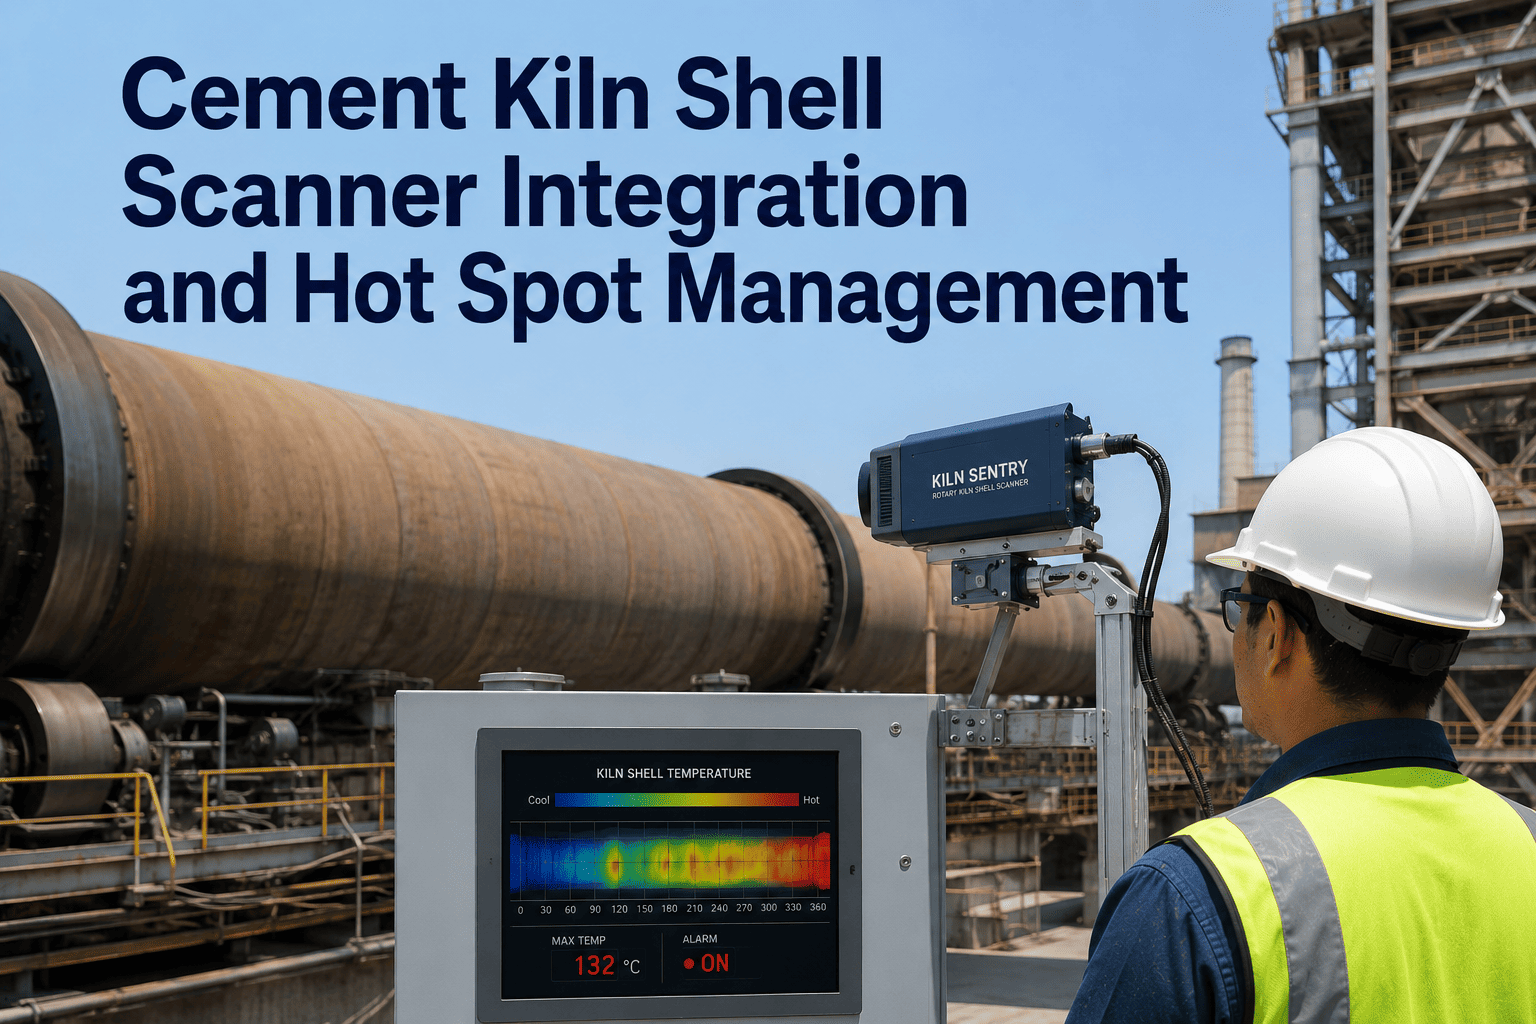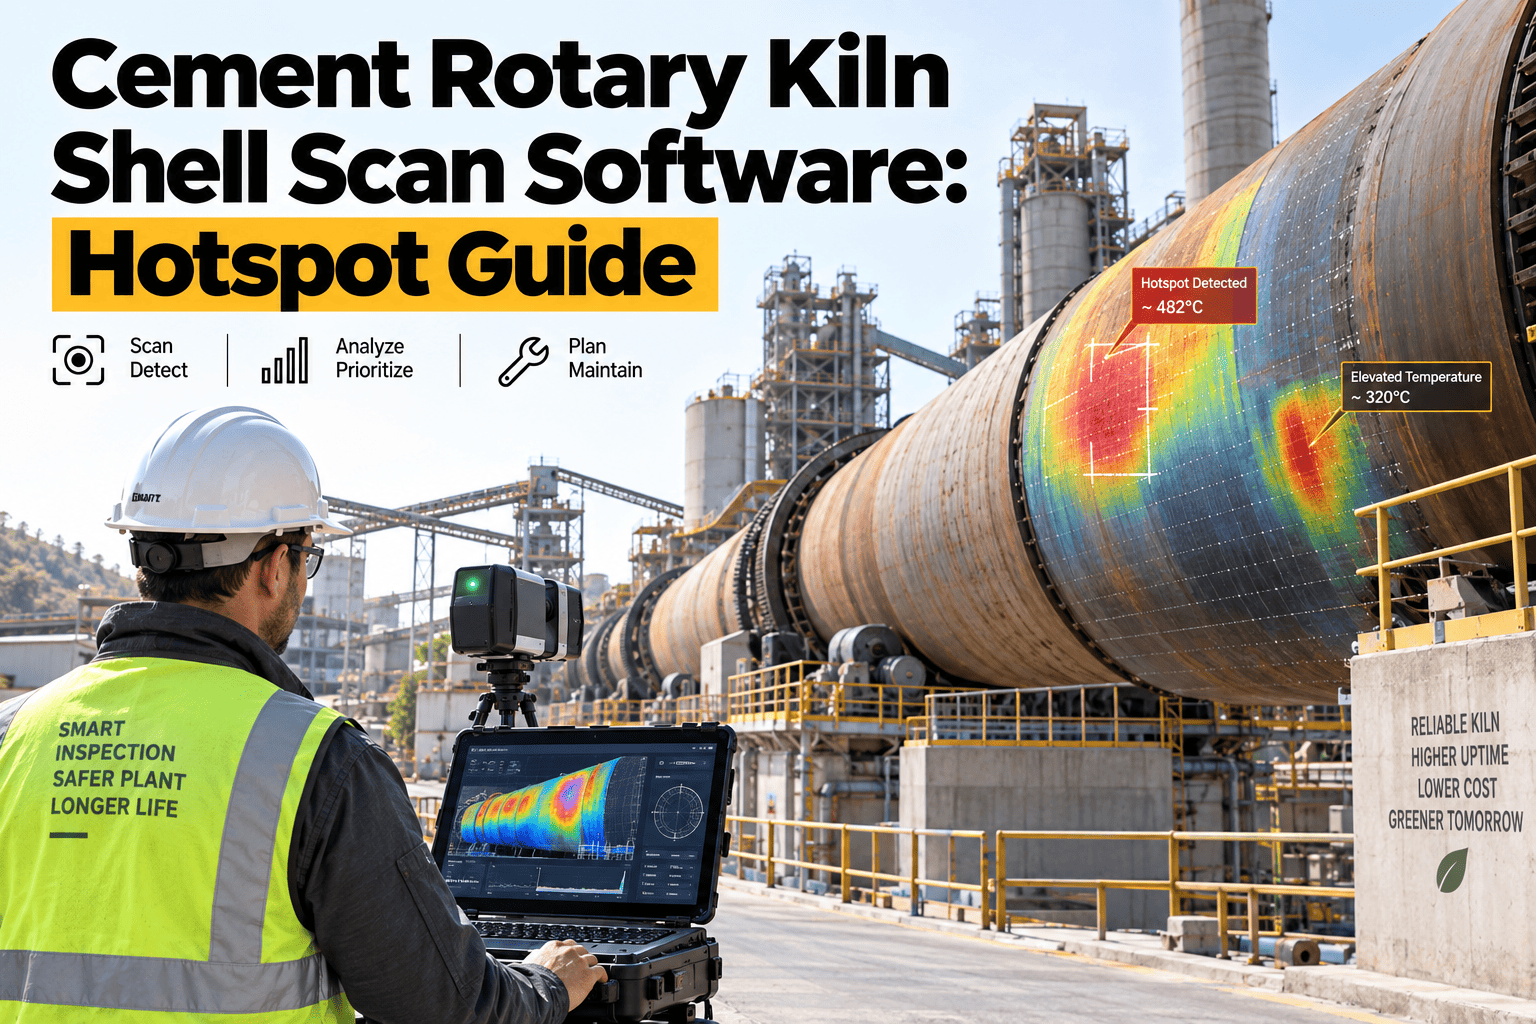
A cement rotary kiln shell is steel wrapped around fire — a nine to fifteen foot diameter tube holding a 1,450°C flame back with nothing but refractory brick and a clinker coating a few inches thick. When that lining wears through in one spot, the shell underneath can go from 250°C to over 400°C in a matter of hours, and once steel crosses that line it starts to warp permanently. Cement plant reliability teams that still rely on a handheld thermal gun and a whiteboard find out about that failure days after it started — this guide covers how a structured, CMMS-tracked shell scan program catches it while there is still time to schedule a repair instead of an emergency shutdown.
Kiln Shell Scanning & Hot Spot Management
Is your kiln shell telling you something before it breaks?
Refractory wear doesn't announce itself — it shows up first as a slow rise in shell surface temperature. A structured scanning program, logged and trended in a CMMS, turns that rise into weeks of warning instead of a 3 AM red-kiln call.
The Cost Of Not Knowing
Why kiln shell temperature is the number reliability teams can't afford to guess at
Inside the burning zone, the flame runs above 1,450°C while the refractory brick and clinker coating hold the shell surface down to a normal operating band. That coating is not static — feed rate swings, fuel changes, kiln speed adjustments, and ring formation all cause it to thin, spall, and rebuild constantly through a campaign.
The plants that get caught out are almost never the ones without a thermal camera — they're the ones where the readings never made it into a system that could trend them, flag a deviation, and turn that flag into a scheduled work order before the next shift forgot about it.
A pattern reliability teams recognize
A once-per-shift manual reading missed an overnight temperature climb that would have been obvious on a trend chart — by the time the day shift caught it visually, the shell had already discolored and a planned repair turned into a multi-week emergency reline. The scanning hardware wasn't the gap; the missing piece was a system trending every reading against the last one instead of judging each in isolation.
Root Cause
How a hot spot actually forms — the refractory failure pathway
A hot spot is rarely a single event. It's the visible end point of a chain that usually starts weeks earlier, inside the kiln, where nobody can see it directly.
Coating instability
Feed chemistry shifts, fuel changes, or kiln speed variation cause the protective clinker coating to thin unevenly in the burning zone.
Brick exposure and spalling
Once coating loss exposes the brick face directly to flame radiation, thermal cycling accelerates spalling and cracking of the refractory.
Shell surface heating
With brick thickness reduced, heat transfers through to the steel shell far faster — surface temperature begins climbing 2–3°C per day.
Localized hot spot
A patch of shell reads 40–60°C or more above the surrounding average — the visible signature that a scan is designed to catch.
Warp or breakthrough
Left unaddressed, sustained heat above 400°C weakens the steel — the shell can warp permanently or, in the worst case, breach entirely.
Reference Data
Kiln zone temperature reference: what normal looks like, and what a scan should flag
Different zones of a rotary kiln run at different baseline temperatures — a single plant-wide alarm threshold misses hot spots in cooler zones and over-alarms in the burning zone. A useful shell scan program sets zone-specific baselines.
| Kiln Zone | Typical Shell Temp | Watch Threshold | Alert / Emergency Threshold |
|---|---|---|---|
| Burning Zone | 200–280°C | 300–320°C | >340°C or +50°C differential |
| Upper Transition Zone | 180–240°C | 260–280°C | >300°C or +40°C differential |
| Safety / Nose Ring Zone | 150–200°C | 220–240°C | >260°C or +40°C differential |
| Calcining Zone | 140–190°C | 210–230°C | >250°C or +35°C differential |
| Chain / Feed End | 100–150°C | 170–190°C | >210°C or +30°C differential |
These bands are a starting reference, not a substitute for plant-specific data — every kiln's baseline should be established from its own thickness survey and shell scan history, then loaded into whatever system is tracking the trend.
Why generic thresholds fall short
Kiln diameter, feed chemistry, fuel type, and even ambient conditions at the plant site all shift these numbers slightly, which is why a scan program built around one kiln's own history tends to catch problems that a generic industry threshold would miss or flag too late.
Hardware Options
Handheld gun, fixed pan-tilt scanner, or continuous line scanner — which fits your kiln?
The scanning hardware matters less than what happens to the data afterward, but the choice still shapes how early a hot spot gets caught and how much manual effort a round takes.
| Method | Coverage | Typical Frequency | Best Fit |
|---|---|---|---|
| Handheld infrared gun | Operator-selected points, inconsistent between rounds | Once or twice per shift | Smaller plants, single-kiln operations building a scanning habit |
| Fixed pan-tilt scanner | Full circumference on a programmed sweep | Every 15–30 minutes | Kilns with a history of ring formation or repeat hot spots |
| Continuous line scanner | Full circumference every rotation | Continuous, real-time | Large single-kiln lines where downtime cost justifies the investment |
Whichever hardware a plant runs, the value only shows up once every reading lands in the same place, against the same zone baseline, where a trend line can be drawn through it — that's the role a CMMS plays regardless of which scanner feeds it.
See what your last twelve months of shell scans would have flagged
OxMaint can model your kiln's zone thresholds and show you where a trending alert would have caught a hot spot before it reached the alarm stage.
Manual vs Managed Scanning
Handheld thermal gun rounds vs a CMMS-tracked scanning program
Most plants already own an infrared thermal gun. The gap is rarely the hardware — it's what happens to the reading after it's taken.
- Readings logged on paper or a shared spreadsheet, reviewed only when someone remembers to look
- No consistent scan point map — different operators check different spots each round
- Hot spot discovered visually or by smell, often after the shell has already discolored
- No link between a bad reading and a scheduled work order — it becomes a verbal note
- Every reading logged against a fixed 16–24 point circumference map, tied to the kiln asset record
- Zone-specific thresholds trigger an automatic alert the moment a reading crosses the watch band
- Trend chart shows the 2–3°C/day rise that signals thinning coating — visible days before a visual hot spot
- Alert converts directly into a work order for refractory inspection, gunning, or a planned stop
Program Setup
Building a kiln shell scan program inside your CMMS
A scanning program is only as useful as the structure behind it. These are the pieces that turn a thermal gun reading into a working early-warning system — none of them require new hardware, since most plants already own a thermal gun and already run scans of some kind.
Establish a baseline map
After a reline, record shell temperature at 16–24 fixed circumferential points per zone in the CMMS — this becomes the reference every future scan is compared against.
Set a scan cadence
Weekly scans are a practical minimum for most kilns; plants with continuous infrared line scanners can log a full circumference reading every rotation instead.
Configure zone thresholds
Load watch and alert bands per zone into the CMMS so a reading is judged against the right baseline, not a single plant-wide number.
Automate the work order
A reading in the watch band opens a refractory inspection task; a reading in the alert band should generate a priority work order automatically, with no manual re-entry.
Review the trend, not just the point
A single high reading matters less than a sustained rise — the CMMS dashboard should plot each scan point over time so a 2–3°C/day climb is visible at a glance.
Common Pitfalls
Where kiln shell scan programs quietly fail
Most plants don't skip scanning altogether — the program exists on paper, but a few gaps in execution quietly erode its value until it stops functioning as an early-warning system.
- Inconsistent scan points. If each operator picks their own spots on the shell, no two rounds are directly comparable, and a genuine trend gets buried in point-to-point noise.
- No baseline after a reline. Without a fresh reference reading taken right after a reline, every later scan is being compared against an outdated or estimated starting point.
- Readings that stop at the logbook. A temperature entered on paper or in a spreadsheet with no automatic threshold check relies entirely on someone remembering to review it — the exact failure mode a scan program exists to remove.
- Plant-wide thresholds. A single alarm value applied to every zone either misses hot spots in cooler zones or generates so many false alerts in the burning zone that operators start ignoring them.
- No link to a work order. An alert that doesn't automatically create a task for refractory inspection or gunning depends on a verbal handoff surviving a shift change — which is exactly where early warnings tend to get lost.
OxMaint For Kiln Reliability
How OxMaint supports kiln shell scanning and hot spot response
OxMaint gives kiln reliability teams one place to log scans, watch trends, and act on them — instead of splitting the workflow across a thermal gun, a spreadsheet, and a radio call to the shift supervisor.
Zone-based scan logging
Log readings against a fixed circumferential point map per kiln zone, either manually from a handheld gun or via integration with a continuous infrared line scanner.
Outcome: consistent, comparable scan data every roundAutomatic trend alerts
OxMaint plots every scan point over time and flags a sustained rise rate or a differential versus neighboring points, well before a reading crosses an absolute alarm value.
Outcome: earlier warning, not just a louder alarmWork orders on threshold breach
A watch-band reading opens an inspection task; an alert-band reading auto-generates a priority work order with the zone, reading, and history attached.
Outcome: no dropped handoffs between shiftsCampaign-level reporting
Export scan history and refractory intervention records for the full campaign — useful for reline planning, refractory vendor reviews, and reliability audits.
Outcome: audit-ready records without manual compilationFAQ
Kiln shell scanning: frequently asked questions
How often should a cement kiln shell be thermally scanned?
Weekly scanning at 16–24 points per zone is a practical minimum for most kilns. Plants running continuous infrared line scanners can capture a full circumference reading every rotation, giving near real-time hot spot detection rather than a once-a-week snapshot.
What shell temperature counts as a hot spot?
There's no single universal number — it depends on the zone. As a general guide, a reading more than 40–50°C above the surrounding shell average, or above roughly 320–340°C in the burning zone, warrants inspection. Zone-specific thresholds configured in a CMMS give a more accurate call than a flat plant-wide value.
Can a hot spot be repaired without stopping the kiln?
Early-stage hot spots are often managed with external gunning or cooling air while the kiln keeps running, buying time until a planned stop. Once shell temperature sustains above roughly 400°C, the risk of permanent warp usually forces an emergency shutdown regardless of production schedule.
Does OxMaint integrate with infrared kiln shell scanners?
Yes. OxMaint can receive scan data from fixed or pan-tilt infrared line scanners via standard integrations, logging every reading against the kiln asset and applying the same zone-based alerting used for manual gun readings. Book a demo at calendly.com/oxmaintapp/30min to see your scanner connected.
What's the difference between a red kiln event and a routine hot spot?
A routine hot spot is a localized, moderate temperature rise caught early and managed with gunning or a planned repair. A red kiln event is shell temperature sustained high enough that steel is visibly glowing or deforming — a full emergency shutdown and, usually, weeks of reline work follow, along with the lost production that comes with an unscheduled stop of that length.
Stop finding out about hot spots from the color of the shell
Move your kiln shell scans into OxMaint and get zone-based thresholds, trend alerts, and automatic work orders — so refractory problems get caught while they're still a gunning job, not a reline.
Free 14-day trial · No credit card