Cement manufacturing consumes 3–4 GJ of thermal energy and 90–130 kWh of electricity per tonne of clinker — making it the most energy-intensive industry on the planet after aluminum smelting. Energy costs represent 30–40% of total cement production costs, and in 2026, with coal prices still elevated and electricity tariffs rising across Asia, the Middle East, and Europe, every percentage point of energy efficiency directly translates into millions of dollars in annual savings. The plants pulling ahead are not the ones with newer kilns — they are the ones deploying AI-driven energy management systems that optimize fuel blends, mill loading, and demand profiles in real time, 24 hours a day. Start your free Oxmaint trial and connect your energy meters to a live CMMS dashboard in under 48 hours.
Where Energy Goes in a Cement Plant
Before optimizing, you must understand the energy map. A 3,000 TPD integrated cement plant consumes roughly 280–320 MW of thermal and electrical energy combined. The distribution below reveals exactly where AI optimization delivers the highest return — and why kiln and grinding dominate every energy reduction strategy.
AI Energy Optimization: How It Actually Works
AI energy optimization in cement plants is not a black box. It is a model-predictive control system that ingests hundreds of process variables — kiln inlet/outlet temperatures, raw mix chemistry, draft profiles, fuel calorific values, mill feed rates, separator speeds — and calculates the mathematically optimal set points every 30–60 seconds. Manual operators, even expert ones, can manage 5–8 variables simultaneously. AI manages 200–500 simultaneously without fatigue. Book a demo with Oxmaint to see how energy data feeds directly into maintenance work orders when anomalies are detected.
Real-Time Data Ingestion
Every sensor reading — temperature, pressure, flow rate, power draw, vibration — is streamed into the AI engine at 1–5 second intervals. The data pipeline normalizes units, detects outliers, and fills gaps from sensor failures before feeding the optimization model.
Predictive Modeling
Machine learning models trained on historical plant data — typically 2–5 years — predict the energy impact of each possible set-point change 15–60 minutes into the future. This forward-looking view prevents optimization decisions that improve one metric while degrading another.
Constraint-Aware Optimization
Optimization runs within hard constraints: minimum clinker quality targets (LSF, SM, AM), equipment operating limits, environmental permit thresholds for NOx and SO₂, and shift-specific production targets. AI optimizes within the feasible solution space, not in theoretical ideal conditions.
CMMS-Linked Anomaly Detection
When energy consumption deviates from the AI model's predicted baseline — indicating equipment degradation, fouling, or failure — an automated alert triggers a maintenance work order in the CMMS. Energy anomalies are often the earliest detectable indicator of mechanical problems.
Oxmaint Turns Energy Anomalies Into Maintenance Work Orders — Automatically
When a ball mill draws 8% more power than the AI baseline at the same feed rate, Oxmaint creates a Priority 2 work order and assigns it to the right technician before the shift supervisor even notices. See it live.
Kiln Energy Optimization: The Highest-Value Target
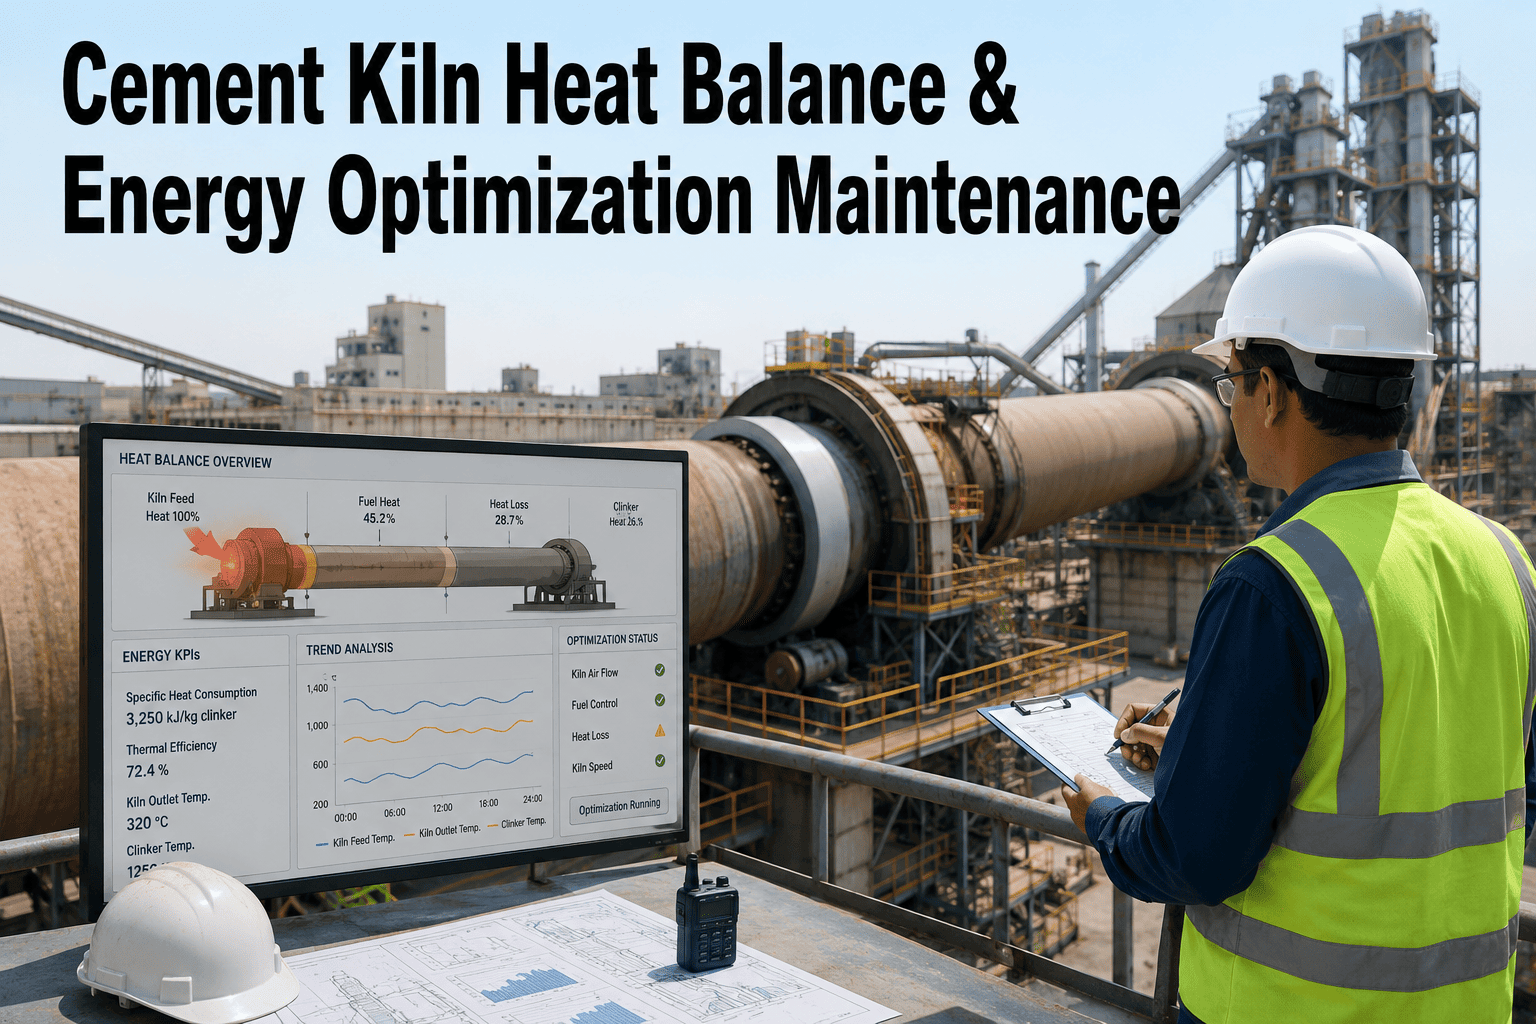
The rotary kiln consumes over half of a cement plant's total energy and offers the largest single optimization opportunity in the industry. A 1 GJ/tonne improvement in specific heat consumption at a 3,000 TPD plant saves approximately $3–5 million annually at current fuel prices. AI kiln optimization systems achieve this through simultaneous control of variables that no human operator can manage at the required frequency.
What AI Controls in the Kiln
Kiln Energy Benchmarks
Grinding Energy Optimization: The Electricity Cost Battleground
Cement grinding consumes 24–40 kWh per tonne of finished cement — the largest single component of electrical energy costs. At $0.07–0.12/kWh, a 3,000 TPD plant spends $15–25 million annually on grinding electricity alone. AI optimization of mill loading, separator speed, and water injection can recover 8–12 kWh/tonne, saving $4–8M per year at this scale. Sign up for Oxmaint to start tracking specific energy consumption per mill on a live dashboard today.
Sound-based estimation leads to under/overloading — both waste energy
Single set point ignores feed chemistry changes — forces overgrinding to hit strength targets
Temperature control by exception — mill frequently runs too hot or too cold
No demand management — peak tariff periods treated identically to off-peak
AI holds mill at exact optimal loading point — maximizes throughput per kWh continuously
Fineness target maintained with minimum energy by adjusting to real-time clinker reactivity
Mill outlet temperature held within ±2°C of target — prevents wasted cooling energy
AI shifts discretionary throughput to off-peak tariff windows — same output, lower bill
Energy Monitoring Infrastructure: Building the Data Foundation
AI optimization is only as good as the data feeding it. Before deploying any optimization algorithm, cement plants must establish a metering and monitoring infrastructure that provides accurate, real-time energy data at equipment level. Book a demo to see how Oxmaint's energy monitoring dashboard integrates with your existing meters and DCS historian.
Utility feed power meter with 1-minute interval data logging, demand trending, and tariff period flagging
Dedicated power transducers on kiln main drive and ID fan — two largest single consumers
Mass flow meters on all fuel lines (coal, petcoke, gas, alternative fuels) with calorific value integration
Separate meters for ball mill, separator, mill fan, and bucket elevator — isolates energy per circuit component
Flow meters at compressor output and at major consumption points — identifies leak losses and pressure drop
Real-time linkage of energy meters to production rate (t/hr) for specific energy consumption calculation
All process variables (temperatures, pressures, flows) linked to energy data via OPC-UA for AI model training
Non-invasive clamp-on power meters on individual motors for granular equipment-level energy profiling
Ambient temperature and electricity tariff schedule inputs allow AI to predict optimal demand-shifting windows
Oxmaint Connects to Your Existing Meters and DCS Historian in Days
Most cement plants already have 80% of the metering infrastructure they need. Oxmaint's integration layer pulls from your existing OPC-UA historian, creates live energy dashboards, and starts flagging anomalies before your first AI optimization cycle. Start seeing your energy data in real time — not in next month's report.
Energy Audit Framework: Finding Hidden Losses
Before any AI system can optimize, a structured energy audit establishes the current baseline and identifies the highest-priority loss points. Most cement plants that conduct their first rigorous energy audit discover 8–15% of energy consumption in losses that are not visible on standard production reports. Sign up for Oxmaint to run continuous automated energy audits rather than annual point-in-time snapshots.
Establish Specific Energy Consumption Baselines
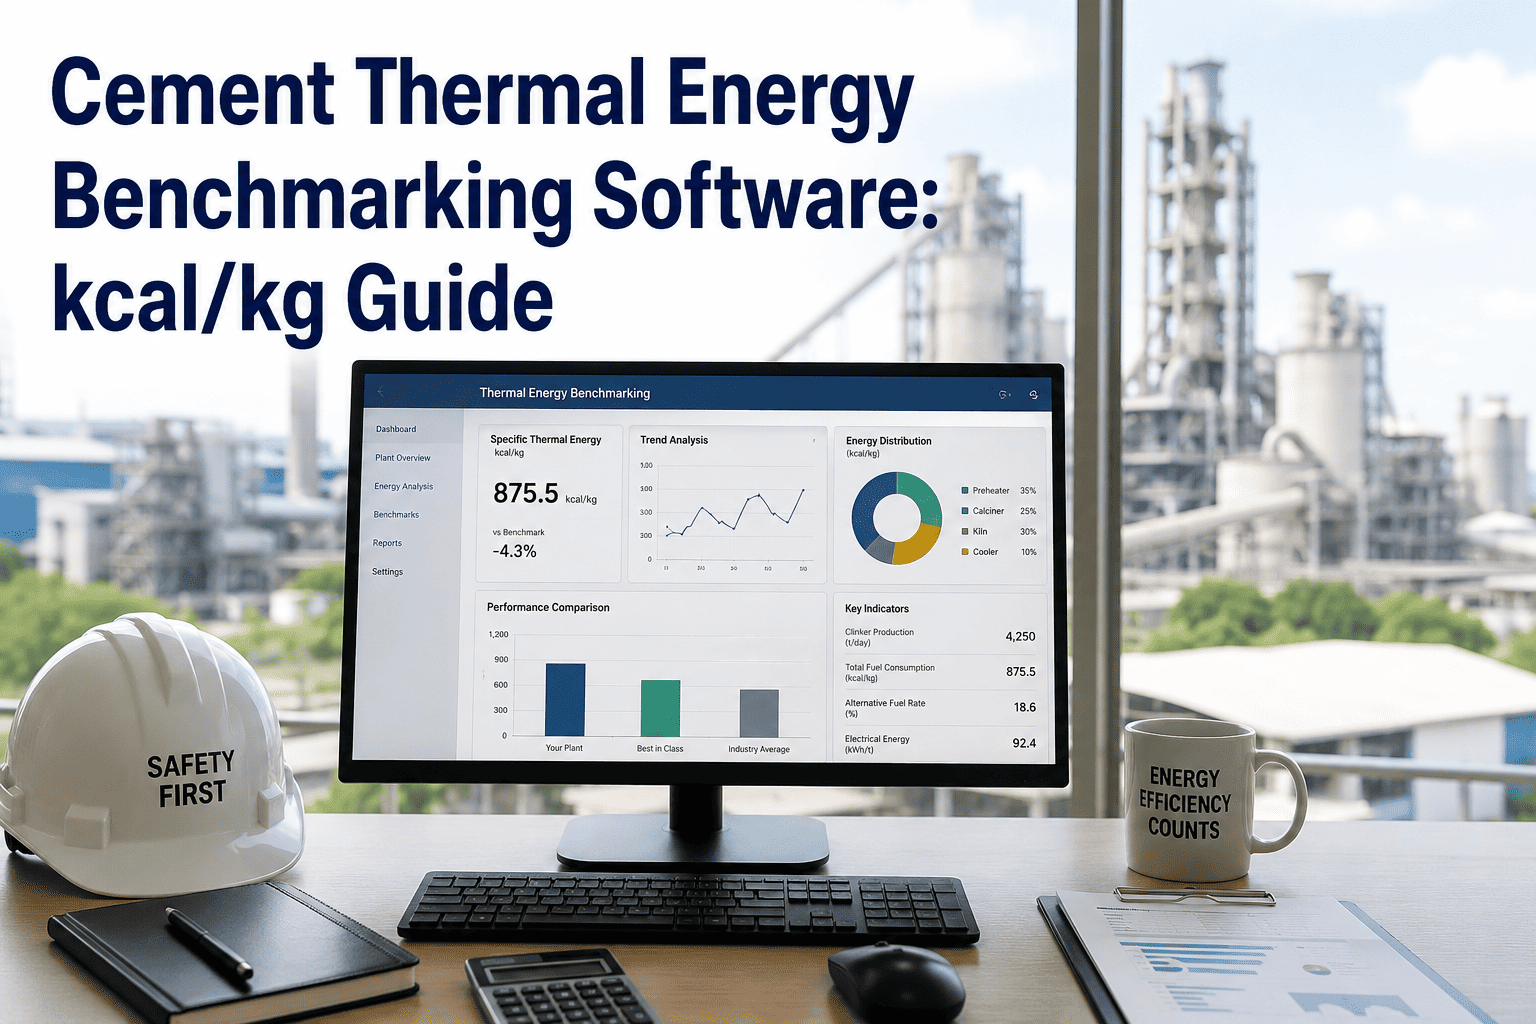
Calculate thermal energy (GJ/tonne clinker) and electrical energy (kWh/tonne cement) for each production unit. Compare against world best practice, regional benchmarks, and your own 3-year trend. This comparison immediately identifies which units are underperforming and by how much.
Map False Air Infiltration Points
False air in the kiln preheater string is one of the most common and costly energy losses in cement — each percentage point of false air adds approximately 0.03 GJ/tonne to heat consumption. Systematic smoke stick testing and O₂ balance calculations across each preheater stage locate infiltration points worth $200,000–$800,000 in annual fuel savings.
Compressed Air Leak Survey
Ultrasonic leak detection across the compressed air distribution network typically finds 15–30% of generated compressed air lost through leaks — at an electricity cost of $0.02–0.04/Nm³. A 3,000 TPD plant can recover $150,000–$400,000 annually from compressed air leak sealing alone, often with repair costs under $30,000.
Motor and Drive Efficiency Survey
Survey all motors above 30 kW for power factor, harmonics, and operating load fraction. Motors running below 40% of rated load are candidates for downsizing or VFD installation. A single oversized 500 kW fan running at 45% load with no VFD wastes $40,000–$80,000 per year compared to a VFD-controlled equivalent.
Heat Recovery Opportunity Assessment
Kiln exhaust gases at 300–350°C and cooler vent air at 200–250°C represent recoverable thermal energy equivalent to 8–12% of kiln fuel input. Waste heat recovery systems generating electricity (ORC or steam cycle) or preheating raw materials have payback periods of 3–6 years at current energy prices — increasingly viable in 2026 as tariffs rise.
Frequently Asked Questions
How much does AI energy optimization cost for a cement plant, and what is the payback period?
AI energy optimization systems for cement plants typically cost $300,000–$1,200,000 for full deployment covering kiln and grinding circuits, including sensors, software licensing, integration, and commissioning. For a 3,000 TPD plant with a heat consumption improvement of 0.2 GJ/tonne and grinding energy reduction of 5 kWh/tonne, annual savings typically reach $2–5M. This yields payback periods of 3–8 months for kiln optimization and 12–18 months for comprehensive grinding optimization. Entry-level energy monitoring and anomaly detection systems — which connect to existing meters and DCS — cost $30,000–$80,000 and typically pay back within 2–4 months through loss identification alone.
What is specific heat consumption and what is the world best practice for modern cement kilns?
Specific heat consumption (SHC) is the thermal energy required to produce one tonne of clinker, expressed in GJ/tonne or kcal/kg. It is the single most important thermal efficiency KPI for cement kiln operations. World best practice for a modern 5-stage preheater precalciner kiln is approximately 2.85 GJ/tonne (680 kcal/kg). The global industry average is approximately 3.3–3.5 GJ/tonne. Wet process kilns can run 5.0–6.0 GJ/tonne — the reason dry process conversion has been the largest energy initiative in cement history. AI kiln optimization systems typically achieve 0.1–0.3 GJ/tonne improvement from baseline, moving plants from average to top-quartile performance.
Can AI energy optimization be deployed without replacing existing DCS systems?
Yes — this is the standard deployment model. AI energy optimization systems operate as a supervisory layer above the existing DCS, communicating via OPC-UA or OPC-DA protocols. The AI calculates optimal set points and sends them to the DCS, which executes them through existing control loops. The DCS hardware, PLCs, and field instruments do not change. This architecture also allows the AI to be disabled and operators to revert to manual control instantly — an important requirement for operator trust during the initial validation period. The only hardware additions are typically additional sensors where existing instrumentation has gaps.
How does demand management reduce electricity costs without reducing production?
Cement plant electricity tariffs in most markets include both a consumption component (per kWh) and a peak demand component (per kW of maximum 15-minute demand). The demand component often represents 20–35% of the electricity bill. AI demand management reduces peak demand by coordinating load sequencing: when multiple large motors (mill start-ups, compressor load-ups) would simultaneously draw peak current, the AI staggers their starts by 2–5 minutes to reduce the coincident peak without affecting production. Plants also use AI to shift discretionary grinding throughput (cement storage buffer grinding) from peak tariff periods (typically 6–9 AM and 6–9 PM) to off-peak night hours, achieving identical weekly production at 8–15% lower electricity cost.
What role does a CMMS play in energy management for cement plants?
A CMMS connects energy management to maintenance execution in three critical ways. First, energy anomaly detection: when a piece of equipment draws more energy than its AI-modeled baseline, the CMMS automatically generates a maintenance work order — catching bearing degradation, fouling, or mechanical issues before they cause failure. Second, maintenance-energy correlation: by linking energy trend data to equipment work order history, reliability engineers can see exactly how energy consumption changes before, during, and after maintenance interventions — quantifying the energy ROI of each PM activity. Third, ISO 50001 documentation: the CMMS provides the audit-trail records required for energy management system certification, linking maintenance actions to energy performance improvements with timestamps and sign-offs.
How much energy can be saved by fixing compressed air leaks in a cement plant?
Compressed air leak losses in unmanaged cement plant systems typically range from 20–35% of total compressed air generated. At an energy cost of 0.12–0.15 kWh per Nm³ of compressed air produced, and typical cement plant compressed air consumption of 1,500–3,000 Nm³/hour, leak losses represent 180–630 kW of wasted electrical power — equivalent to $130,000–$500,000 per year at $0.08/kWh. Ultrasonic leak surveys (cost $5,000–$15,000 per survey) combined with a systematic repair program typically recover 60–80% of leak losses within 6 months. Additionally, reducing system pressure by 0.1 bar (often feasible after leak elimination) saves approximately 0.5% of compressor energy — a further $15,000–$40,000 annually for typical cement plant compressed air systems.
What KPIs should a cement plant track to measure energy management performance?
The seven essential energy KPIs for cement plant management are: (1) Specific heat consumption (GJ/tonne clinker) — primary kiln thermal efficiency indicator; (2) Specific electrical energy (kWh/tonne cement) — overall electrical efficiency; (3) Clinker-to-cement ratio — lower clinker factor means less kiln energy per tonne cement; (4) Mill specific power (kWh/tonne) per circuit — isolates grinding efficiency by mill; (5) Compressed air specific consumption (Nm³/tonne cement) — tracks system efficiency; (6) Peak demand factor (kW peak / kW average) — measures demand management effectiveness; and (7) Energy cost per tonne cement ($) — the financial integration of all efficiency metrics. All seven should be tracked in real time on a CMMS energy dashboard, with weekly trend reviews and monthly variance analysis against production mix changes.
Oxmaint Connects Your Energy Data, Maintenance Workflows, and Compliance Records Into One Platform
From basic energy anomaly detection to full AI optimization integration — Oxmaint scales with your program. Cement-specific dashboards. DCS integration in days. Live energy-to-maintenance correlation. No lengthy implementation projects.