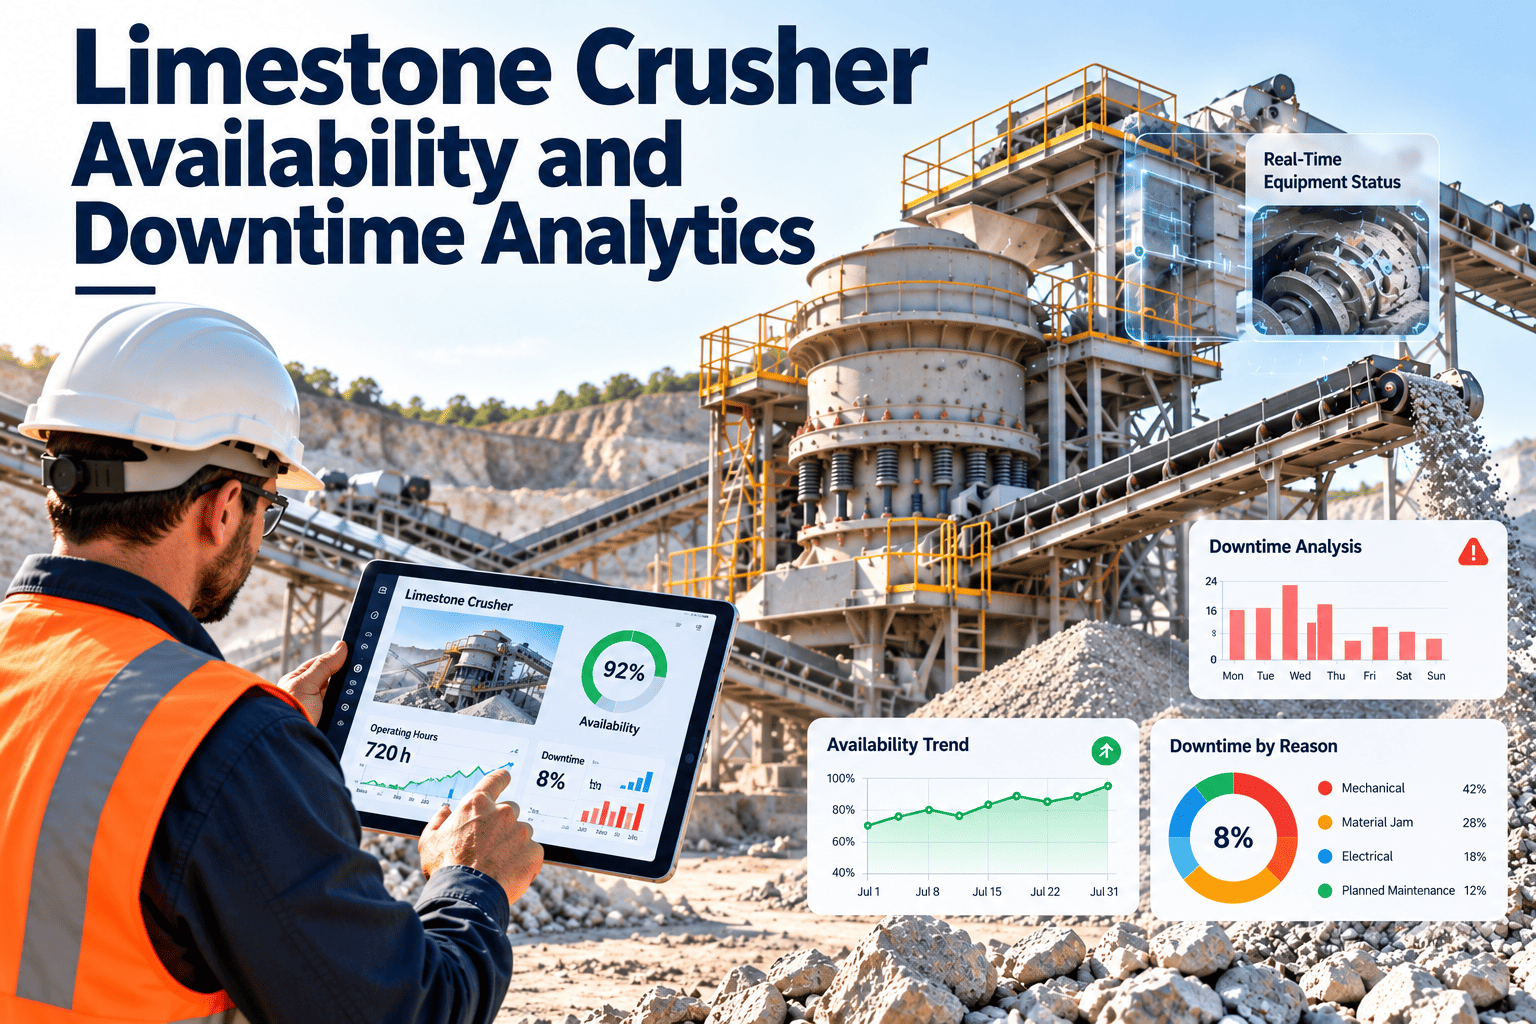
Limestone crusher availability sets the pace for the whole cement plant, because every tonne of kiln feed starts at the quarry. When the primary crusher stops, stockpiles drain, raw mill feed becomes inconsistent, and the cost shows up far from the cause. Most sites log stoppages but rarely analyze them by cause, duration, and repeat pattern. Availability and downtime analytics turn those logs into decisions on wear parts, inspections, and spares. This guide shows how to build that analysis and run it with Oxmaint maintenance management software.
Limestone Crusher Availability and Downtime Analytics
Measure every minute the crusher is not feeding the plant, find the repeat causes, and fix them before they cost you stockpile days.
Why crusher downtime spreads through the whole plant
The crusher is the first link in a chain with little slack. A stoppage that looks minor at the quarry reaches the kiln through buffers that only last so long.
The hidden cost is the repeat stop
One long overhaul is visible and planned. Dozens of ten-minute stops are scattered across shift reports and never added up, yet together they often remove more feed than the overhaul.
Define availability before you measure it
Arguments about availability usually come from different definitions. Fix the time model first, then apply it to every stop.
Classify every minute of lost time
| Loss class | Examples at a limestone crusher | Counts against availability? |
|---|---|---|
| Planned maintenance | Liner or blow bar change, scheduled inspection, lubrication round | Usually reported separately |
| Unplanned mechanical | Bearing failure, shaft or hammer damage, hydraulic leak | Yes |
| Unplanned electrical | Motor trip, drive fault, sensor or interlock failure | Yes |
| Process and material | Oversize rock, clay or wet feed, chute blockage | Plant-specific rule, agree it |
| Upstream or downstream | No trucks, apron feeder trip, full conveyor, full stockpile | Usually idle, not downtime |
| Operational | Shift change delay, waiting for rock breaker, missing permit | Track as delay |
Whatever rules you choose, write them down and apply them identically across shifts. Trend lines only mean something when the definition never moves.
Prioritize losses with a frequency and duration matrix
Not every stop deserves a root cause study. Plot each cause by how often it happens and how long it lasts, then pick the response that fits the quadrant.
Capture the data that makes analysis possible
Analytics fails when stop records say only "crusher down". Each event needs a few structured fields, entered at the time of the stop.
Record on every stop
- Start time, end time, and duration
- Equipment and sub-assembly affected
- Loss class from the table above
- Failure mode, such as wear, fatigue, blockage, or overload
- Immediate cause and suspected root cause
- Work order number and parts used
Link to production context
- Throughput in tonnes per hour before the stop
- Feed size and moisture observations
- Tonnes crushed since the last liner or blow bar change
- Operator and maintenance comments
- Photos of the failed part or blocked area
The KPI set for crusher reliability
Keep the scorecard short enough to review in a weekly meeting. These indicators cover uptime, repair speed, and discipline.
| KPI | What it tells you | Typical action when it worsens |
|---|---|---|
| Availability | Share of scheduled time the crusher could run | Review the top loss causes |
| MTBF | How long it runs between failures | Tighten inspections on weak assemblies |
| MTTR | How fast the team restores it | Check spares, tools, and crew readiness |
| Planned to unplanned ratio | Whether work is controlled or reactive | Move repeat repairs into PM tasks |
| Repeat failure rate | Same failure mode recurring on the same asset | Open a root cause study |
| Wear life per tonne | Liner or blow bar life against material crushed | Adjust replacement trigger and settings |
| PM compliance | Share of scheduled tasks completed on time | Rebalance workload and scheduling |
A six-step downtime analysis workflow
Run this loop monthly. It takes raw stop records to a reliability action list.
- Clean the stop log. Merge duplicates, correct impossible durations, and assign missing loss classes.
- Rank causes. Sort by total lost hours and by event count, since the two lists often differ.
- Find repeats. Group by asset and failure mode to separate chronic problems from one-offs.
- Dig into the top three. Use five whys or a fault tree, and check for wear, setting, or feed causes.
- Assign actions. Create corrective work orders, PM changes, or design requests with owners and dates.
- Verify results. Compare the next month against the baseline and close or reopen the action.
Crusher type changes the failure picture
Limestone is relatively soft and less abrasive than many ores, but contamination, clay, and oversize feed still drive wear and blockages. Match analysis to your machine.
| Crusher type | Common wear and failure points | Analytics focus |
|---|---|---|
| Impact crusher | Blow bars, impact aprons, rotor bearings, drive belts | Blow bar wear per tonne, vibration, imbalance |
| Hammer crusher | Hammers, grate bars, shaft and bearings | Hammer wear, grate blockage, motor current |
| Jaw crusher | Jaw plates, toggle, bearings, hydraulic setting system | Plate wear, setting drift, bearing temperature |
| Gyratory crusher | Mantle and concave liners, spider bearing, lubrication system | Liner profile, oil condition, power draw |
| Sizer | Teeth, shafts, gearboxes, hydraulic couplings | Tooth wear, torque peaks, gearbox temperature |
Stop guessing why the crusher stopped
Log stops, link them to work orders, and see your availability trend in one place.
Condition signals that warn before the stop
Downtime analytics looks backward. Condition signals look forward. Together they shift repairs from emergency to planned.
You do not need every sensor on day one. Start with manual readings captured on inspection routes, then add online signals where failures cost the most.
From reactive stops to planned work
Before structured analytics
- Stops logged as free text in shift reports
- Liners replaced when they fail or by habit
- Same blockage fixed repeatedly without review
- Spares ordered after the breakdown
- Availability debated, never trended
With structured analytics
- Every stop coded by class, asset, and failure mode
- Replacement timed from wear per tonne and measurements
- Repeat causes escalated into corrective actions
- Critical spares tied to failure history
- Availability and MTBF reviewed weekly
How Oxmaint supports crusher reliability work
The value of software is that analysis and action live in the same system. These capabilities map directly to the workflow above.
A 90-day rollout path
Common mistakes that weaken the numbers
- Mixing idle and down time. A full stockpile is not a failure, and counting it hides real problems.
- Changing definitions mid-year. Trends become useless when the rules shift.
- Coding everything as "other". If a third of stops have no cause, the analysis has no direction.
- Ignoring short stops. Small repeating events add up and are usually the cheapest to eliminate.
- Not closing the loop. A root cause finding without an owned work order changes nothing.
Wear parts and spares: where availability is won or lost
Liners, blow bars, hammers, and bearings are consumed on a predictable path. When replacement is planned around tonnes crushed and measured wear, the crusher stops once, on your terms, instead of several times on the machine's terms.
Plan the change-out
- Track tonnes crushed since the last replacement
- Measure wear at fixed intervals and store the readings
- Pre-stage parts, lifting gear, and tools before the stop
- Write a step-by-step task list with expected duration
- Record actual duration to improve the next plan
Stock the right spares
- Rank spares by failure history and downtime impact
- Include supplier lead time in every reorder point
- Keep a spare rotor, shaft, or bearing set where failure would be long
- Review slow-moving stock against actual failure causes
- Link parts used to work orders for accurate cost history
Match the strategy to the loss pattern
| Pattern in the data | Likely meaning | Maintenance response |
|---|---|---|
| Stops cluster late in a liner life | Wear limit is exceeded before replacement | Shorten the interval or add a wear check trigger |
| Blockages rise with wet weather | Clay or moisture in feed is the driver | Adjust feed control and add a standard clearing procedure |
| Bearing faults repeat on one shaft end | Lubrication, alignment, or seal problem | Review the lube task and inspect alignment and seals |
| Long repairs despite few failures | Poor spares readiness or planning | Pre-stage parts and write repair job plans |
| Electrical trips without mechanical cause | Overload, setting, or protection issue | Check current trends, interlocks, and drive settings |
Running the weekly reliability review
Analytics only pays off when someone reviews it on a fixed rhythm. A short weekly meeting with quarry operations and maintenance keeps actions moving.
- Last week's numbers. Availability, unplanned hours, and PM compliance against the target.
- Top three stops. Duration, cause code, and whether the work order is closed.
- Repeat offenders. Any asset with the same failure mode twice in the review window.
- Wear and condition watch list. Components approaching their replacement trigger.
- Actions and owners. Each item gets a person, a date, and a work order.
Availability alone can hide a throughput problem
A crusher can show healthy availability while quietly running below rated capacity. Read availability together with rate and product quality, or the quarry will look better on paper than it feels at the mill.
Reviewing all three levels lets maintenance defend work that improves rate and size control, even when the stop count looks acceptable. It also stops teams from celebrating uptime that produced poor feed.
Frequently asked questions
What is a good availability target for a limestone crusher?
It depends on design, feed, and redundancy, so set the target from your own baseline. Improve against it quarterly rather than copying an outside figure.
Should planned liner changes count as downtime?
Report them separately from unplanned stops, and track their duration too. Long planned stops still reduce output. Book a demo to see this split in practice.
How do I set up reliable downtime codes?
Keep the list short, around 15 to 25 codes, tied to loss class and failure mode. Review unused and overused codes every quarter.
Can I analyze downtime without online sensors?
Yes. Coded stop records, work orders, and inspection readings already support strong analysis. Add sensors where the data shows the greatest loss.
How soon can I see results in a CMMS?
A baseline is possible within weeks once stops are coded. You can sign up and start logging right away.
Turn crusher stops into a reliability plan
Give your quarry team one system for stop analysis, wear tracking, and planned maintenance.