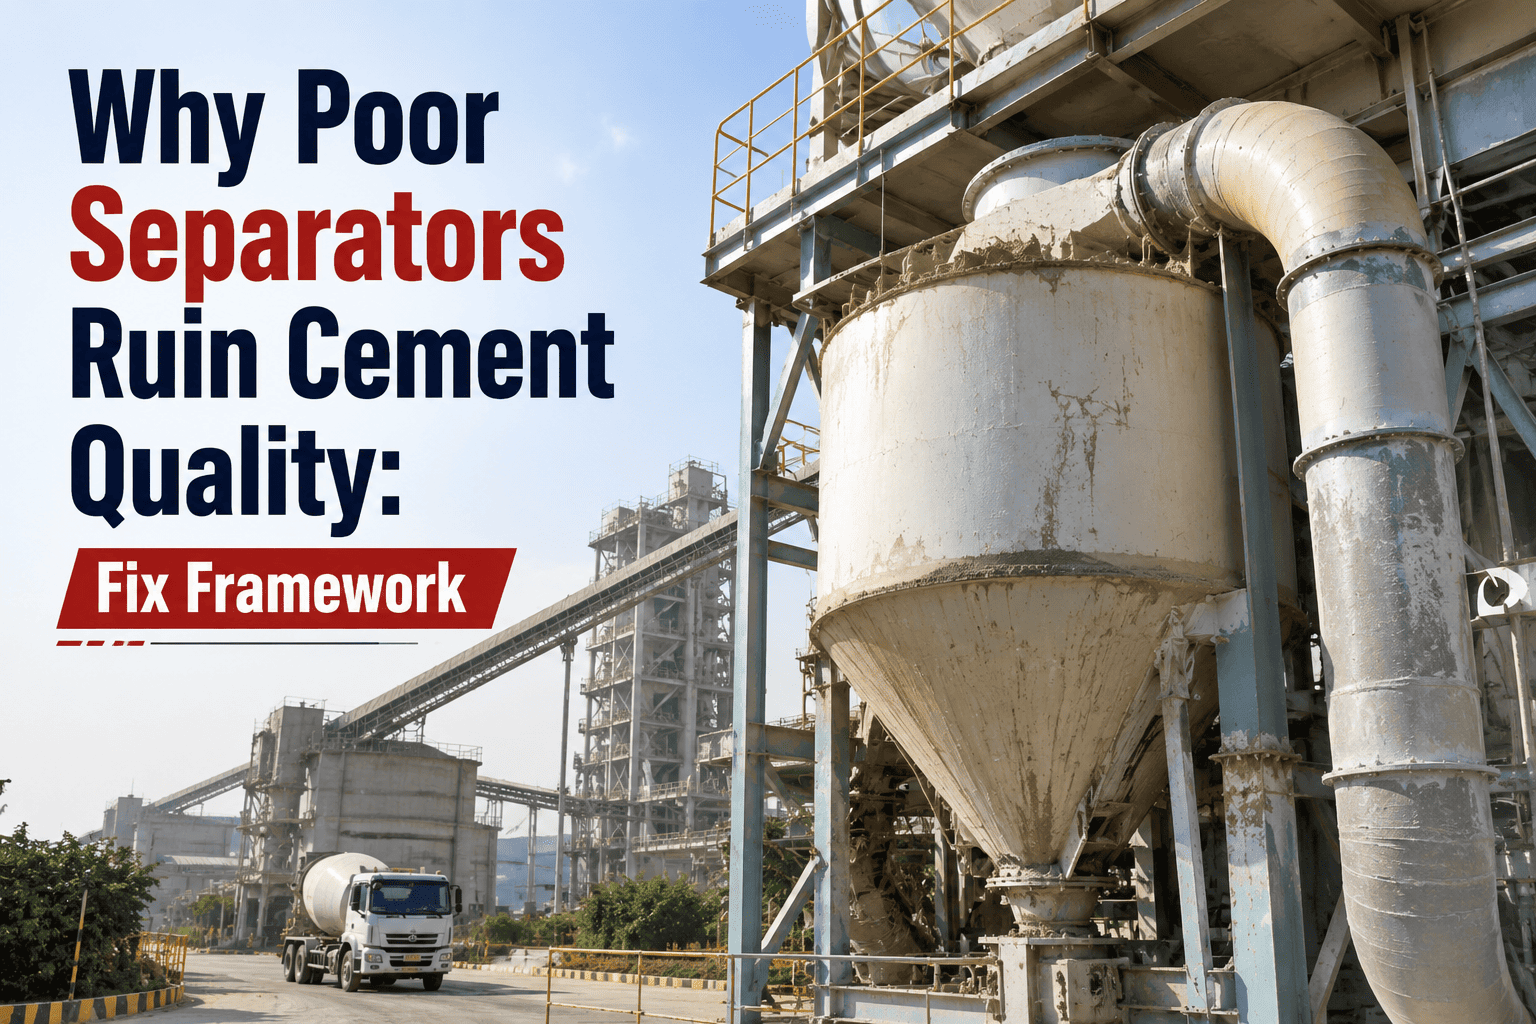
Poor separator performance is one of the few failure modes in a cement plant that can ruin product quality while every gauge on the control room screen still reads normal. A dynamic separator does not fail loudly — it drifts. Bypass creeps up a few points a month, a blade edge wears past its cut-sharpness threshold, a seal starts leaking a little false air, and none of it shows up as an alarm. What it does show up as is inconsistent 28-day strength, a fineness target the mill suddenly cannot hit without running harder, and a customer complaint that reaches your desk long after the batch has shipped. This guide breaks down the three separator failure modes that quietly erode cement quality, why your QC lab panel is structurally blind to them, and the CMMS-based fix framework that catches separator drift before it becomes a strength complaint. Start Free Trial and start trending your separator's cut performance instead of waiting for the next quality hold.
CEMENT SEPARATOR PERFORMANCE · QUALITY FIX FRAMEWORK
Your lab report says the cement passed. Your separator says otherwise.
Improving separator cut sharpness by just 8 to 10 percentage points typically cuts specific power consumption by 1.5 to 2.5 kWh/t with zero capital spend — and the same drift that wastes that energy is quietly widening your particle size distribution and destabilizing strength development batch to batch.
THE DISCONNECT
Why your QC lab clears a batch that your separator already ruined
A standard cement QC panel was built to catch chemistry and gross fineness problems, not slow mechanical drift inside a rotating separator. That gap is exactly where separator wear hides in plain sight, batch after batch, until strength variability finally forces someone to ask why.
The daily QC panel
- Blaine fineness on a composite sample
- Residue on the 45 micron sieve
- Compressive strength cubes at 1, 7, and 28 days
- Bulk chemical and mineralogical composition
All of this is measured after the separator has already done its job — it tells you the outcome, never the mechanical cause.
Inside the separator, right now
- Bypass percentage creeping upward week over week
- Rotor blade edge wear past the 3mm cut-sharpness threshold
- False air leaking in above 10% of total separator flow
- Guide vane angle drifting out of spec against the rotor
None of these four show up on a lab certificate. They only show up as the strength variability the lab certificate can't explain.
THREE FAILURE MODES
The wear patterns hiding inside a normal-looking separator
A separator can run for months looking mechanically fine — spinning smoothly, no unusual noise, no vibration alarm — while these three patterns quietly widen the particle size distribution leaving the mill.
Bypass creep
Bypass is the fraction of feed that passes straight to the coarse reject stream without ever being classified. It is a function of separator ventilation and feed rate, and it climbs quietly whenever airflow or feed balance drifts from design — sending coarse, under-ground particles straight into the finished cement stream.
Rotor blade edge wear
Worn blades reduce the centrifugal force that drives an accurate cut, softening the separation curve even when rotor speed is turned up to compensate. The standard rebuild trigger is 3mm of edge wear — past that point, no amount of speed adjustment restores the original cut sharpness.
Seal and false air leakage
Cold air leaking in at the rotor shaft, guide vane housing, or discharge cone above 10 percent of total separator flow is enough to destroy cut efficiency on its own. It is also one of the easiest failure modes to miss, since nothing about a leaking seal looks abnormal from the control room.
Stop finding out about separator drift from a strength complaint
See how bypass, blade wear, and seal condition get trended inside a CMMS instead of discovered after the batch has already shipped.
READING THE CUT WITHOUT A LAB REPORT
Four numbers that tell you the separator's condition before strength does
Process engineers already track these figures on a Tromp curve during commissioning. Very few plants keep trending them afterward — which is exactly the gap this framework closes.
The particle size with an equal chance of ending up in the fine or coarse stream. When d50 drifts from its design point without a deliberate setpoint change, something mechanical has moved.
The lowest point on the Tromp curve — feed that skips classification entirely. Rising bypass is one of the earliest, most reliable signs that ventilation or feed balance has drifted.
How steep the separation curve is around the cut point. A sharpness reading that slides below roughly 65 percent means the separator is over-grinding fines and recycling them instead of releasing them.
Very fine particles getting recaptured into the coarse stream near the tail of the curve. A worsening fishhook is a classic signature of guide vane misalignment or rotor wear.
FAILURE MODE TO FIX
Matching the quality symptom to the mechanical cause
Once a quality symptom shows up in the lab, the diagnostic path back to the separator is usually fast if you know which mechanical cause to check first. Here is the map most reliability teams end up building the hard way.
| Failure Mode | Quality Symptom | Detection Method | Fix |
|---|---|---|---|
| Bypass creep | Coarse grains in finished cement, strength variability | Trend bypass % from mill mass balance | Retune ventilation and feed rate to design |
| Blade edge wear | Cannot hit fineness target even at high rotor speed | Blade profile check at 3mm edge wear | Rebuild or replace blades on schedule |
| Seal / false air leakage | Erratic residue results, elevated power draw | Quarterly smoke test at shaft, vanes, cone | Reseal and replace worn gaskets |
| Guide vane misalignment | Uneven particle size distribution, fishhook effect | Vane angle check against rotor exit angle | Realign vanes to within 2 degrees of spec |
CMMS CONFIGURATION
How a CMMS turns separator drift into a trend line, not a mystery
The plants that catch separator drift early are not running better lab tests — they are trending mechanical condition against quality outcomes in one place instead of two separate, disconnected systems.
Bypass and cut sharpness trending
Log bypass percentage and cut sharpness from every mass balance calculation against the separator's own asset record, so a slow upward drift becomes visible weeks before it shows up in a strength result.
Blade wear PM scheduling
Schedule blade profile inspections on a fixed interval and trigger a rebuild work order automatically once edge wear crosses the 3mm threshold, instead of waiting for a fineness complaint to prompt an inspection.
Seal smoke-test tracking
Track quarterly smoke tests at the rotor shaft, guide vane housing, and discharge cone against each separator's maintenance history, so false air leakage gets caught on schedule rather than discovered during a power audit.
Quality complaint to work order linkage
When a strength or fineness complaint comes in, link it directly to the separator's maintenance and trend history from the same batch window, cutting root cause investigation from days down to minutes.
Vane alignment records
Log guide vane angle checks against the rotor blade exit angle at every inspection, keeping a documented alignment history that separates a genuine mechanical fault from a legitimate process setpoint change.
Energy and quality on one dashboard
Because separator condition drives both specific power consumption and product quality, trending them on the same dashboard turns a quality investigation and an energy audit into the same conversation.
"
We had three strength holds in one quarter and every one traced back to the same separator, but nobody connected the dots because maintenance records and QC results lived in different systems. Once we started trending bypass and blade wear against our quality data in the CMMS, we caught the next drift two weeks before it reached a customer.
FREQUENTLY ASKED
Poor separator performance and cement quality — straight answers
How can separator wear affect strength if fineness still looks fine?
Bulk Blaine fineness can look normal even while the particle size distribution has widened, since a rising bypass or a softer cut spreads particles across a broader range without necessarily changing the average. Strength development is sensitive to that spread, not just the average fineness number.
What exactly is separator bypass and why does it matter?
Bypass is the portion of separator feed that passes directly into the coarse reject stream without being classified at all. It is driven by ventilation and feed balance, and a rising bypass percentage is one of the earliest reliable signs of separator drift.
How often should separator blades be inspected?
Most plants set a fixed inspection interval and a rebuild trigger at 3mm of blade edge wear, whichever comes first. Book a Demo to see how that threshold gets scheduled and tracked automatically.
Can false air really affect finished cement quality?
Yes. False air above roughly 10 percent of total separator flow is enough to destroy cut efficiency on its own, widening the particle size distribution and driving up specific power consumption at the same time.
How does a CMMS catch separator problems before QC does?
By trending bypass, blade wear, and seal condition against the separator's own maintenance history in the same place quality data lives, so mechanical drift is visible weeks before it shows up as a strength or fineness complaint. Start Free Trial to set up separator trending on your own mills.
Give your separator the same scrutiny your lab gives every batch
Bypass trending, blade wear PM, and seal smoke-test schedules, linked directly to your quality data.
Free 14-day trial · No credit card