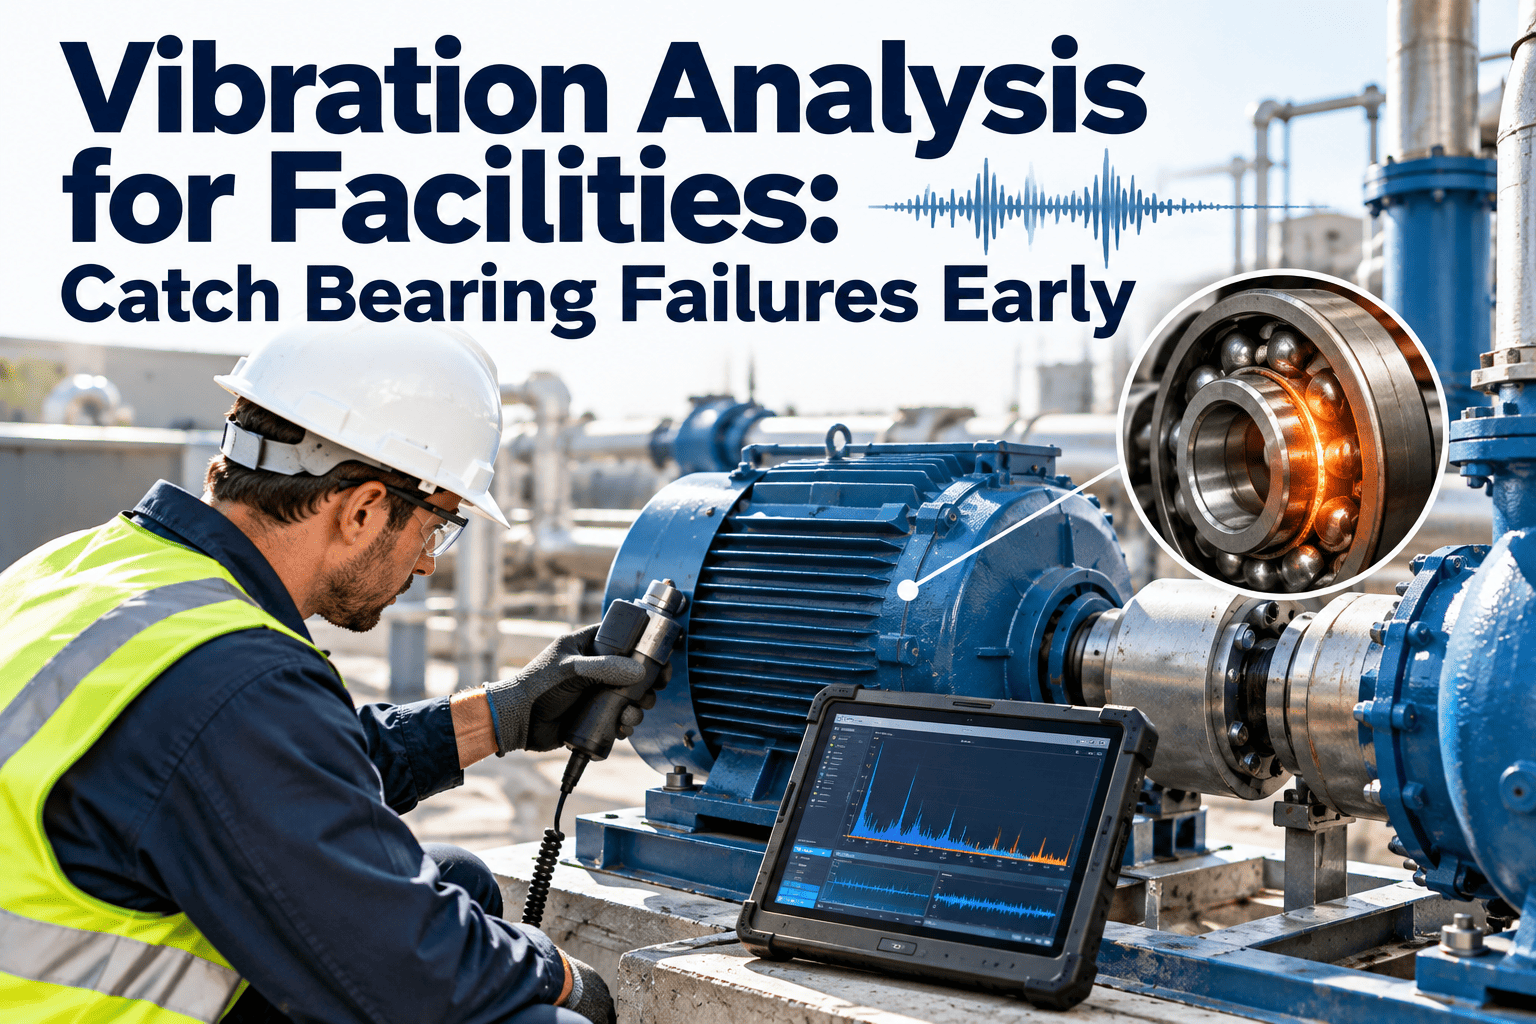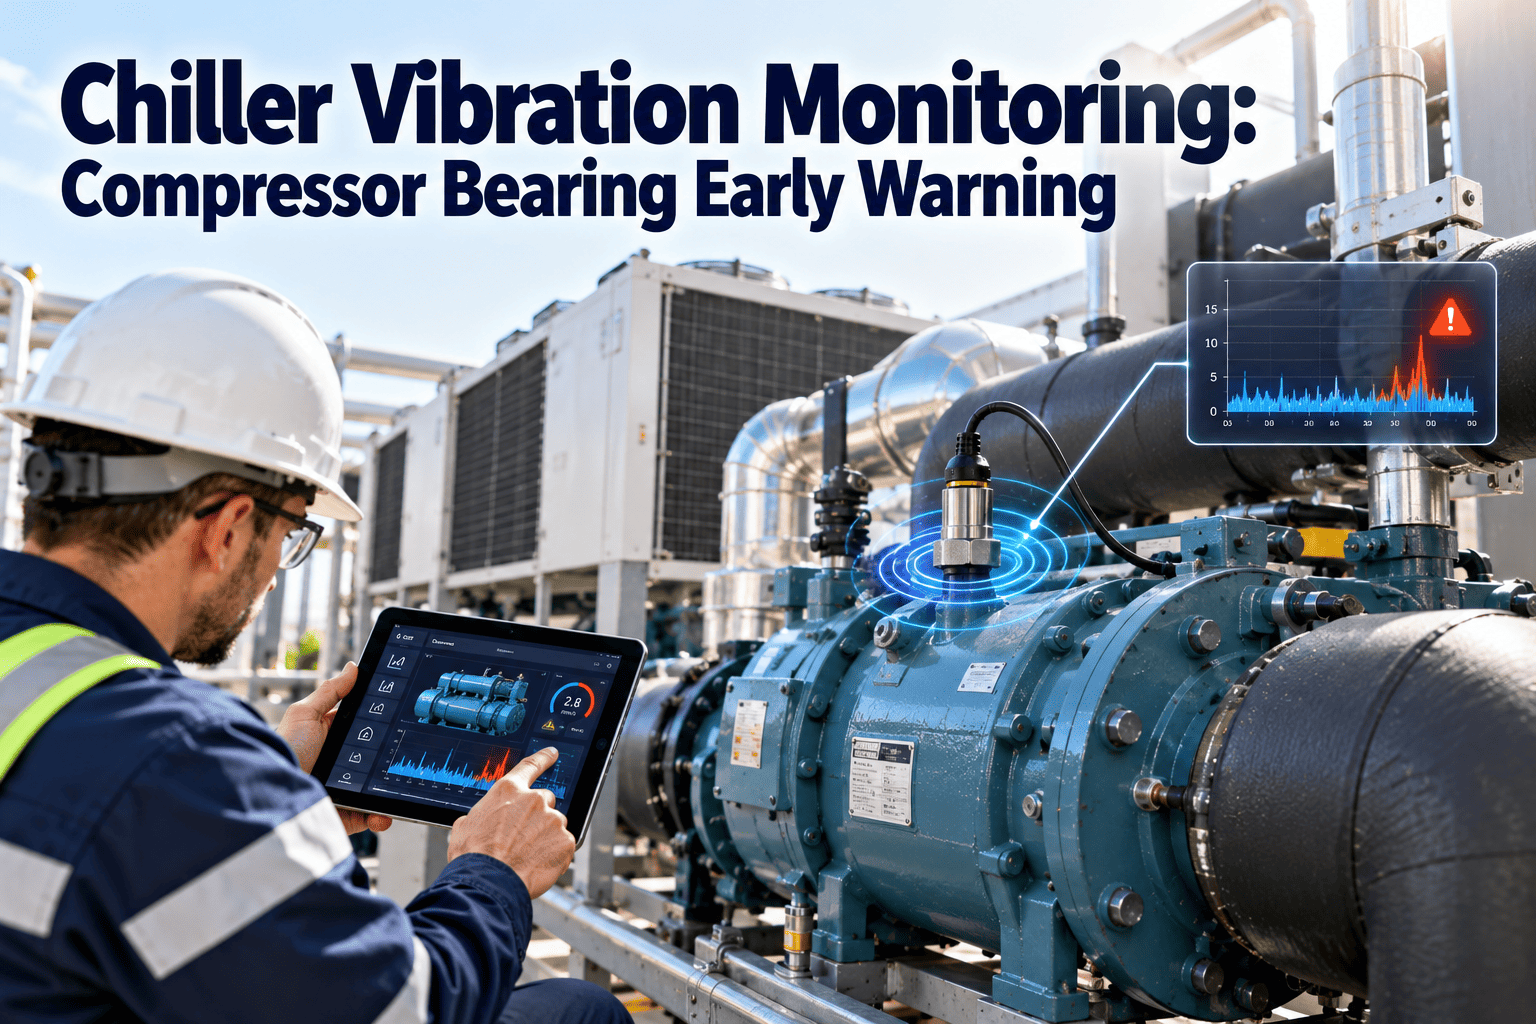
A chiller compressor rarely fails without warning. Weeks or months earlier, a failing bearing leaves a signature in the vibration data: faint high-frequency energy first, then distinct defect frequencies, and finally a visible rise in overall levels. Teams that watch only temperature and amps tend to see the problem after the damage is done. This guide covers sensor placement, thresholds, and alert routing, and shows how a condition-based maintenance platform turns an alarm into a planned repair.
Chiller Vibration Monitoring: Compressor Bearing Early Warning
Catch compressor bearing wear while there is still time to order parts, schedule an outage, and avoid a mid-season shutdown. Learn where to mount sensors, how to set alarm levels, and who should receive each alert.
The compressor is the costliest, slowest part of a chiller to recover
Bearing damage spreads. A worn bearing allows shaft movement, which strains seals, gears, and in turn the rotating assembly.
Operational impact
- Unplanned outage during peak cooling demand
- Extended lead time for major compressor components
- Collateral damage to rotors, impellers, or gears
- Temporary cooling rental and added energy cost
What early warning gives you
- Time to confirm the fault and order parts
- A repair scheduled in a low-load season
- Repair at bearing level rather than full rebuild
- A documented basis for capital and spares decisions
What to monitor depends on the compressor design
Vibration signatures differ by design, so tune your monitoring plan to what is installed.
| Compressor type | Typical bearing concern | Monitoring focus |
|---|---|---|
| Centrifugal, geared | High-speed shaft bearings and gear mesh | Bearing housing vibration, gear mesh orders, shaft position where available |
| Screw | Rotor bearings under axial and radial loading | Axial and radial vibration, lobe pass frequencies, oil condition |
| Scroll and reciprocating | Crank and main bearings, valve events | Overall levels and shock events, supported by amps and temperature |
| Magnetic bearing | No oil film, so contact bearings act as backup | Use controller data for bearing position and touchdown events |
Put the sensor where the vibration path is shortest
A sensor mounted on a thin cover tells you about the cover. Mount on a rigid area close to the bearing load zone.
- 1
Mount on the bearing housing
Use stud or adhesive mounting on a clean, flat, rigid surface. Avoid painted or flexible panels. - 2
Measure radial and axial
Radial data shows unbalance and misalignment. Axial data helps expose thrust and alignment problems. - 3
Choose sensor range for the fault
Accelerometers capture the high-frequency content where early bearing defects first appear. - 4
Keep placement repeatable
Mark each point with the asset ID, point name, and axis so readings stay comparable over years. - 5
Protect cabling and housings
Route cables away from heat and moving parts, and use sealed connectors in damp plant rooms.
Four stages from first defect to functional failure
Bearing faults tend to move through recognizable stages. Different analysis methods work best at each one.
Very early
Faint high-frequency energy shows in envelope or demodulated spectra. Overall vibration is unchanged.Defect visible
Bearing defect frequencies emerge in the spectrum. Plan inspection and parts.Advanced wear
Harmonics, sidebands, and a raised noise floor appear. Bearing temperature may start to rise.Imminent failure
Overall vibration climbs sharply and audible noise appears. Prepare for a controlled stop.Route every chiller vibration alarm to a planned work order
Connect condition data, alert rules, and maintenance tasks so warnings turn into scheduled repairs.
How ISO vibration severity guidance fits chiller programs
ISO 10816 established the familiar severity zones for machine vibration. It has since been superseded by the ISO 20816 series, so check which edition your policy cites.
Setting alarms in practice
- Use the manufacturer's limits first, then the standard's zones as a cross-check
- Record a healthy baseline right after commissioning or overhaul
- Set alert levels relative to that baseline, plus a fixed upper limit
- Alarm on trend and on defect-frequency energy, not only overall velocity
- Review levels after every repair, load change, or equipment change
Defect frequencies that point to the failing component
Each bearing part produces a characteristic frequency tied to its geometry and running speed.
| Frequency | Meaning | What it suggests |
|---|---|---|
| BPFO | Ball pass frequency, outer race | Outer race defect, often the first to develop |
| BPFI | Ball pass frequency, inner race | Inner race defect, often with running-speed sidebands |
| BSF | Ball spin frequency | Rolling element damage |
| FTF | Fundamental train frequency | Cage problem or looseness |
Where to find the numbers
Use the bearing manufacturer's data or the OEM service manual for exact frequencies, since they depend on the installed bearing.
Define who acts, and how fast, at each alert level
An alarm nobody owns is only noise. Link each level to a role and a standard response.
Detect
Sensor or portable route reading crosses a trend or limit rule.Verify
Analyst checks spectra, load, and recent changes to rule out false alarms.Corroborate
Compare with oil condition, bearing temperature, and motor current.Plan
Create a work order, reserve parts, and pick an outage window.Repair and reset
Fix, record findings, and set a new baseline.| Alert level | Typical trigger | Owner | Expected response |
|---|---|---|---|
| Watch | Upward trend or early defect energy | Reliability technician | Increase measurement frequency |
| Warning | Defect frequency confirmed | Maintenance planner | Corrective work order and parts check |
| Alarm | Severity limit exceeded | Maintenance supervisor | Inspect promptly, decide on load reduction |
| Critical | Rapid rise or protective trip | Chief engineer | Controlled shutdown and emergency repair |
Cross-check vibration with other chiller signals
Vibration is strongest when confirmed by a second indicator.
Connect condition data to maintenance execution
Detection only matters when work follows. These Oxmaint capabilities close that loop.
- Asset managementHold each chiller, compressor, and motor with nameplate data, baseline spectra, and repair history.
- Condition-based triggersCreate work orders when readings cross defined rules, instead of waiting for a calendar date.
- Work orders and inspectionsAssign confirmation checks and repairs with checklists, notes, and photos from the plant room.
- InventoryLink bearings, seals, and oil to the compressor so parts are on hand before the outage.
- Dashboards and reportingShow alert counts, open repairs, and repeat failures to guide reliability decisions.
Before you switch on vibration alerts
Confirm each item so alarms are trusted from the first week.
- Compressor and motor nameplate data recorded, including bearing designations
- Sensor points named, labeled, and photographed
- Healthy baseline captured at normal load
- Manufacturer limits and ISO zone references documented
- Alert levels mapped to named roles and response times
- Spare bearings and seals identified, with supplier lead time noted
- Seasonal outage windows agreed with operations
- Review cycle set for thresholds after repairs
Chiller vibration monitoring questions
How early can vibration detect a chiller bearing fault?
Envelope analysis can show early defects well before overall vibration rises. Lead time varies widely by machine and load.Do I need continuous sensors or routine routes?
Critical chillers benefit from continuous monitoring. Routes suit lower-risk units. A quick demo can help you decide.Is ISO 10816 still the right reference?
It has been replaced by the ISO 20816 series. Always apply OEM limits alongside the standard.Can an alarm create a work order automatically?
Yes, condition rules can open tasks with the right priority. You can sign up and test a rule.Does this apply to magnetic bearing chillers?
Partly. Those compressors report bearing data through their own controllers, so use that data and watch backup bearing events.Match the measurement type to the fault you want to see
Different vibration quantities reveal different problems. Using only one can hide an early fault.
| Measurement | Best for | Limitation |
|---|---|---|
| Velocity (overall) | General machine health, unbalance, misalignment, looseness | Slow to reflect early bearing defects |
| Acceleration | High-frequency events, early bearing and gear faults | Sensitive to mounting quality and noise |
| Envelope or demodulated spectrum | Repetitive impacts from bearing surface defects | Needs correct filter bands and known bearing geometry |
| Time waveform | Impacting, looseness, and transient events | Requires analyst interpretation |
| Spectrum with orders | Linking peaks to running speed and gear mesh | Speed must be known and stable |
Speed and load matter
Take comparison readings at similar load and speed. A chiller at part load can show very different vibration from the same machine at full load.
Build the baseline before you need it
Alarms mean little without a record of what healthy looks like for this specific machine.
- 1
Capture at stable operation
Record readings once the chiller has reached steady load, ideally after commissioning or a verified overhaul. - 2
Save spectra and waveforms
Keep full data, not only overall values, so future changes can be compared in detail. - 3
Record operating context
Note load, speed, inlet and outlet temperatures, and the number of units running. - 4
Repeat across load points
Build baselines for typical part-load and full-load operation so alarms are not triggered by normal changes. - 5
Refresh after major work
Capture a new baseline whenever bearings, couplings, or alignment are changed.
How an early bearing warning might unfold
This is a generic sequence to show how data and work connect, not a record of a specific site. Timing varies greatly between machines.
Trend rises
Envelope energy at a compressor bearing point climbs above its baseline band. A watch alert is raised.Analyst confirms
A defect frequency matches the installed bearing, and oil results are checked for wear particles.Work is planned
A corrective work order is created, parts are reserved, and an outage window is agreed with operations.Repair and reset
The bearing is replaced, findings are recorded, and new baseline readings are saved.Plan around lead times and cooling demand
Early warning is only valuable if the repair can actually happen before failure.
Before the cooling season
- Review all chiller trends and open watch items
- Confirm bearing and seal spares for critical compressors
- Agree repair windows and contractor availability
- Check that alert contacts and on-call lists are current
During peak demand
- Increase review frequency for units with active warnings
- Decide in advance when load will be reduced or shared
- Keep temporary cooling options identified
- Log every alarm decision for later review
Factors to include when justifying chiller monitoring
Build the case from your own plant data rather than generic figures. These are the inputs finance will ask about.
- The consequence of losing each chiller, including cooling capacity and dependent areas
- Historical bearing and compressor repair costs and the downtime that came with them
- Rental or temporary cooling cost per day and how long it is typically needed
- Lead time for compressor parts and for specialist contractors
- The cost of sensors, installation, analysis, and ongoing review
- Insurance, warranty, and contractual conditions tied to condition records
Start with the critical units
Begin with chillers that have no standby capacity or that serve critical spaces. Extend to the rest of the fleet once alert handling is proven.
Mistakes that undermine chiller vibration programs
Most failed programs have good sensors and weak habits. These are the patterns to avoid.
- Setting one fixed alarm for every chiller, regardless of size, speed, or design
- Ignoring operating mode, so start-ups and surge events trigger false alarms
- Collecting overall values only and never reviewing spectra
- Moving sensors between visits, which breaks trend comparison
- Failing to update baselines after a repair, so healthy readings look abnormal
- Sending alerts to a mailbox rather than a named role with a response time
- Treating a cleared alarm as closed without recording what was found
- Skipping analyst review, so every alarm is either trusted blindly or ignored
- Leaving sensor cables and mounts unchecked until a reading suddenly drops to zero
- Installing monitoring on the compressor but not on the motor and gearbox that feed it
Close the loop
After every repair, record the failure mode, the bearing condition, and whether the earlier warning matched the finding. That history is what improves your thresholds over time.
Who does what in a chiller condition program
Clear roles stop alarms falling between operations, maintenance, and contractors.
Fix the bearing before it stops the building
Bring chiller condition data and maintenance work together so early warnings become planned, parts-ready repairs.