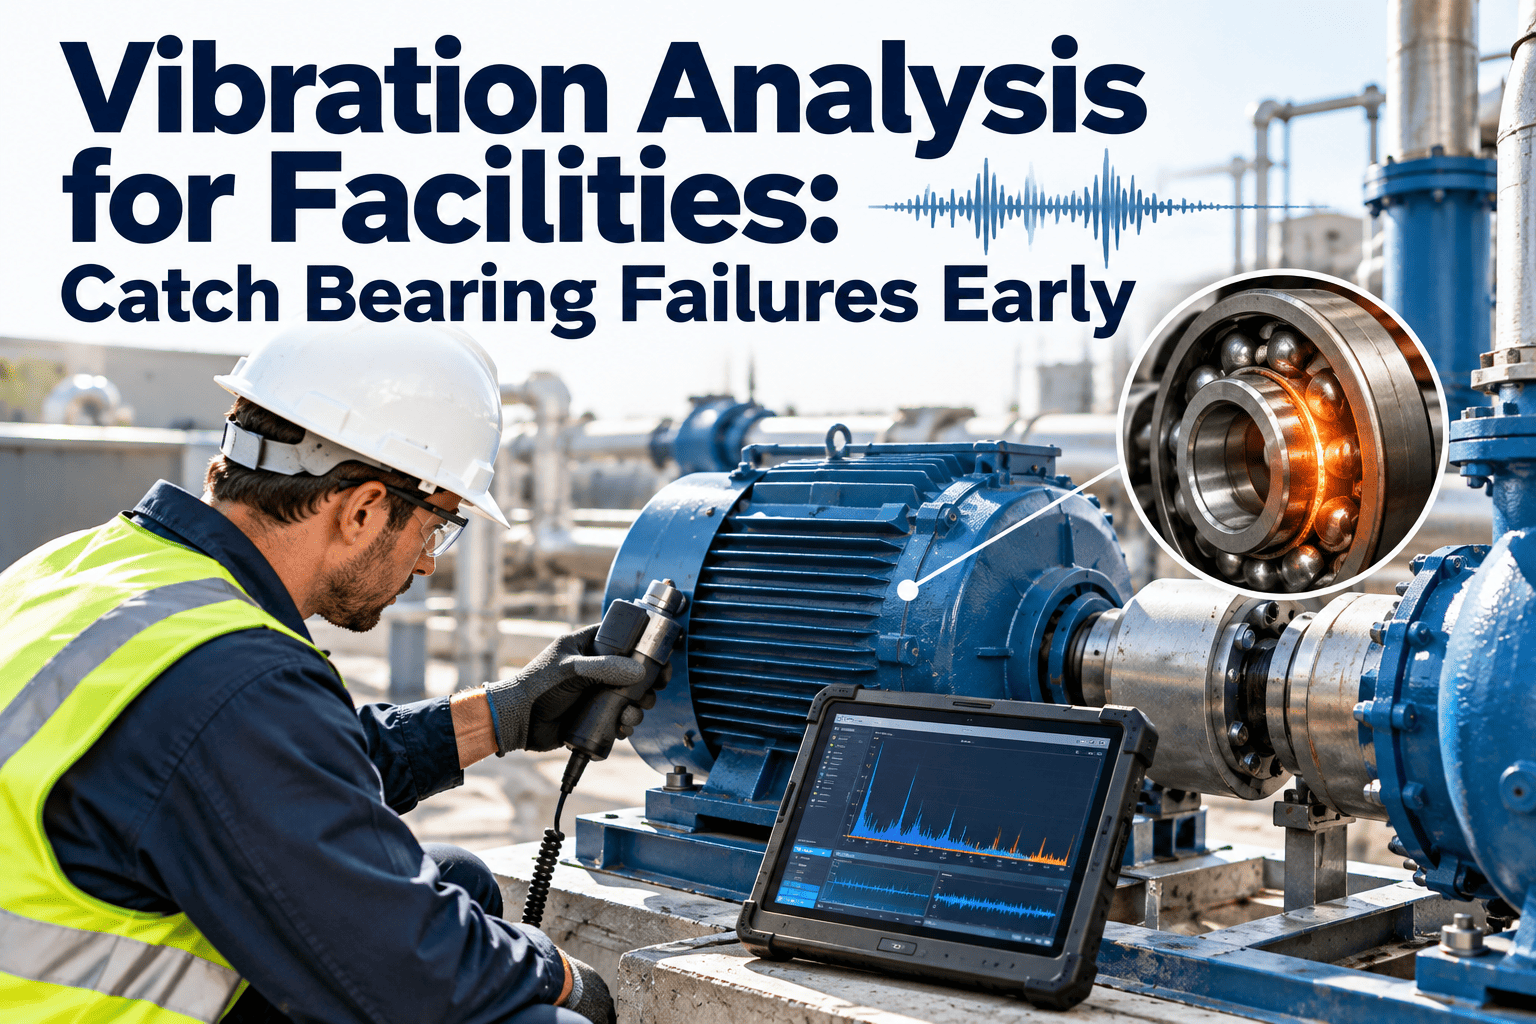
Bearing failure is one of the most common ways rotating equipment stops in commercial buildings, and it rarely happens without warning. Fans, pumps, and motors begin to vibrate differently weeks or months before they seize, but only teams that measure vibration routinely will see the change. This guide explains how facility teams apply ISO 20816 severity zones, choose sensors, build baselines, and set trusted alarms, and you can book a demo to see readings become work orders.
Condition Monitoring · Rotating Equipment
Vibration Analysis for Facilities: Catch Bearing Failures While They Are Still Cheap to Fix
Vibration analysis reads the mechanical signature of motors, fans, and pumps, so facility teams can replace a worn bearing in a planned window instead of after a breakdown.
Typical bearing degradation path
Stage 1
Very high-frequency energy
Micro-defects seen only by ultrasound or acceleration sensors
Stage 2
Bearing defect frequencies
Distinct peaks appear in the spectrum
Stage 3
Harmonics and sidebands
Peaks multiply and overall velocity begins to climb
Stage 4
Noise and heat
Symptoms people can hear and feel
Stage 5
Failure
Seizure, breakage, secondary damage
The warning window from first detectable defect to failure ranges from days to many months, depending on speed, load, and lubrication.
Failure Physics
What Each Degradation Stage Means for Your Team
Bearings do not fail suddenly. A defect starts small, grows through the raceway or rolling elements, and produces signals that change in a predictable order.
Stage
What the data shows
Response
Stage 1
Raised high-frequency energy in acceleration or ultrasound readings, with normal overall velocity.
Verify lubrication, confirm sensor mounting, and shorten the interval between readings.
Stage 2
Discrete peaks at calculated bearing defect frequencies appear in the spectrum or envelope.
Create a planned work order and order the bearing while the asset is still stable.
Stage 3
Harmonics and sidebands multiply, and overall velocity trends upward across readings.
Schedule replacement within the next available window and stage the crew and parts.
Stage 4
Noise floor rises and bearing temperature climbs. Damage may be spreading to the shaft or housing.
Replace urgently. Delay risks a seized bearing and a far larger repair.
Standards
ISO 20816-3 Severity Zones Explained for Facility Teams
ISO 20816 is the current series for evaluating machine vibration measured on non-rotating parts. Part 3 replaced ISO 10816-3 for industrial machines above 15 kW running between 120 and 30,000 rpm, and the zone letters carry over, so older reports citing ISO 10816 remain usable.
Zone A
Newly commissioned condition. Use it as the healthy baseline.
Zone B
Acceptable for unrestricted long-term operation.
Zone C
Unsatisfactory for continuous running. Plan remedial work.
Zone D
Severe enough to cause damage. Stop or restrict the machine.
Zone boundaries in RMS velocity (mm/s)
| Machine group and support | A/B boundary | B/C boundary | C/D boundary |
|---|
| Group 1 (above 300 kW to 50 MW), rigid support | 2.3 | 4.5 | 7.1 |
| Group 1, flexible support | 3.5 | 7.1 | 11.0 |
| Group 2 (15 to 300 kW), rigid support | 1.4 | 2.8 | 4.5 |
| Group 2, flexible support | 2.3 | 4.5 | 7.1 |
Worked example: same reading, different verdict
A 150 kW motor reading 3.0 mm/s RMS sits in Zone C on a rigid foundation but in Zone B on a flexible one. Support stiffness changes the verdict, so record it for every asset. To convert, 1 in/s equals 25.4 mm/s, which makes 4.5 mm/s about 0.18 in/s. Always confirm limits against the current standard and the equipment manufacturer.
Applicability
Which Facility Equipment Falls Under the Standard
Many building fans are smaller than the standard covers, so a mixed portfolio needs a mixed approach.
| Equipment | Typical size | Guidance | Practical approach |
|---|
| Air handler and exhaust fan motors | Often below 15 kW | Outside ISO 20816-3 scope | Use manufacturer limits plus your own baseline trend |
| Chilled and condenser water pump motors | Commonly 15 to 300 kW | Group 2 style limits, with pump-specific groups for multivane pumps | Use zone limits as starting alarms and refine per asset |
| Large chiller compressor motors and boiler feed pumps | Above 300 kW | Group 1 style limits | Combine zone limits with manufacturer guidance |
| Cooling tower fan drives | Varies, often slow speed | Below 120 rpm falls outside the range | Trend against baseline and monitor gearbox and motor separately |
| Standby generator engines | Varies | Reciprocating machines have a separate part of the series | Trend under test load and follow the engine maker |
Measurement Points
Where to Put the Sensor on a Motor-Pump Train
Motor non-drive end
Horizontal, vertical, axial
Motor drive end
Horizontal, vertical, axial
Coupling
Pump drive end
Horizontal, vertical, axial
Pump non-drive end
Horizontal, vertical, axial
Mount as close to the bearing housing as possible, on solid metal rather than a thin guard or fan cowl. Mark each point so every technician measures in exactly the same place.
Hardware
Choosing Sensors: Route, Wireless, or Online
Sensor choice should follow asset criticality and physical access, not the other way around. Most facilities end up with a blend of approaches rather than a single method.
| Approach | How it works | Best for | Limitation |
|---|
| Handheld route collector | A technician measures fixed points on a route, monthly or quarterly | Large populations of medium-priority assets | Can miss fast-developing faults between routes |
| Wireless triaxial sensor | Battery sensors send readings on a schedule through a gateway | Hard-to-reach fans, rooftop units, and critical pumps | Battery life and signal coverage need planning |
| Wired online accelerometer | Fixed sensor streams continuously to a monitoring system | Chillers and other high-consequence machines | Highest installation effort |
| Portable ultrasound | Listens for high-frequency friction and leaks | Early lubrication problems and slow-speed bearings | Needs trained interpretation |
Diagnosis
Fault Signatures a Facility Team Can Learn First
You do not need to be a certified analyst to use these patterns. They tell a technician where to look first, and a specialist can confirm the diagnosis on the assets that matter most.
| Fault | Spectrum signature | Common facility cause | First check |
|---|
| Imbalance | Dominant peak at running speed (1x) | Dirty or damaged fan blades | Clean and inspect the wheel |
| Misalignment | Peaks at 1x and 2x, high axial vibration | Poor coupling alignment after service | Laser align and check soft foot |
| Mechanical looseness | Harmonics of running speed, sometimes subharmonics | Loose base bolts or worn mounts | Torque check on baseplate and housing |
| Rolling element bearing defect | Non-synchronous peaks at defect frequencies, best seen in envelope analysis | Lubrication failure or contamination | Inspect lubricant and plan replacement |
| Electrical motor fault | Peaks at twice line frequency, sidebands near running speed | Rotor or stator issues, unbalanced supply | Check current balance and connections |
| Pump cavitation | Broadband high-frequency noise | Low suction pressure or blocked strainer | Check suction conditions |
Baseline
Set a Vibration Baseline in Six Steps
A baseline is the reference every later reading is judged against, so it deserves more care than a routine measurement. An extra hour spent on the first reading of each critical asset pays back every month afterward.
1
Confirm a healthy machine
Verify lubrication, alignment, and mounting before measuring. A baseline taken on a faulty machine locks in the fault.
2
Fix the points
Mark each measurement point and direction and record it in the asset record.
3
Match operating state
Measure at normal speed and load. Drive-controlled machines need a baseline for each speed band.
4
Capture more than one number
Store overall velocity, acceleration, and the spectrum so later readings can be compared properly.
5
Save it against the asset
Attach the baseline to the asset record with date, operating state, and the technician who took it.
6
Set the reading interval
Read often for the first quarter, then set frequency by criticality and observed rate of change.
Give every bearing a documented history
Store baselines on the asset record, schedule vibration routes as recurring tasks, and keep every finding where the next technician can see it.
Alarm Design
Alarm Levels That Technicians Will Trust
Alarms that fire constantly get ignored. Build three levels tied to the baseline and the ISO zone, and require two or three consecutive readings before escalating.
Alert: watch
Reading rises above baseline by a set margin, or the trend slope climbs across readings. Many programs start near double the baseline velocity and tune from there.
Response: read more often, check lubrication and mounting.
Alarm: plan
Reading approaches Zone C, or bearing defect peaks keep growing.
Response: raise a planned work order, stage parts, schedule the repair.
Action: act now
Reading enters Zone D or rises rapidly between readings.
Response: inspect immediately and consider shutting the machine down.
Route Design
Reading Frequency by Asset Criticality
Not every machine deserves the same attention. Use these starting intervals, then tighten or relax them based on how quickly each asset actually changes.
| Criticality | Example assets | Starting interval | Notes |
|---|
| Critical | Chiller motors, main chilled water pumps, air handlers serving data or sterile spaces | Continuous or weekly | Justifies permanent wireless or online sensors |
| Important | Condenser water pumps, cooling tower drives, boiler feed pumps | Monthly | Shorten the interval after any alert |
| Standard | Supply and return fans, secondary pumps | Quarterly | Route-based collection is usually enough |
| Low | Small exhaust fans and utility pumps | Annual check or run to failure | Keep a spare on the shelf |
Trend Reading
What the Shape of the Trend Tells You
A single reading is a snapshot. The direction and speed of change tell you how much time you have.
Rate of rise
A slow, steady climb suggests gradual wear. A steep climb across a few readings suggests an advancing defect and should shorten the response window.
Step change
A sudden jump after maintenance or a load change often points to alignment, mounting, or installation rather than bearing wear.
Load or seasonal pattern
Readings that follow occupancy or outdoor temperature reflect operating conditions, so normalize by load before raising an alarm.
Flat but high
A stable elevated reading may be a fixed problem such as misalignment or a soft foot, and it is still worth correcting.
Workflow
Turning a Vibration Reading Into a Work Order
ReadSensor or technician records velocity, acceleration, and spectrum.
RuleThreshold and trend rules compare the reading with the asset baseline.
AlertA confirmed exceedance notifies the maintenance planner.
OrderA work order is created with the asset, reading, zone, and priority.
PlanThe job plan lists steps, safety requirements, and bearings from inventory.
CloseFindings and a fresh baseline are recorded on the asset history.
Oxmaint keeps asset records, recurring inspection routes, work orders, spare parts inventory, mobile completion, and reporting in one system. That lets a reading taken in the plant room reach a planner and a technician without retyping. You can
create a free account and set up a vibration route this week.
Work Order Content
What a Good Vibration Work Order Contains
- Asset ID, location, and the measurement point that triggered the alert
- Reading, zone, and baseline values with the date each was taken
- Operating state at the time of the reading
- Suspected fault and the evidence behind it
- Job plan with lockout and safety steps
- Bearing and lubricant part numbers reserved from inventory
- Completion date tied to the alarm level
- Findings fields for the technician, including photographs of the removed part
Lubrication
Vibration and Lubrication Work Best Together
Lubrication is the most controllable cause of early bearing distress, so schedule vibration readings and lubrication tasks in the same route.
- Read vibration before greasing so the value reflects true bearing condition, then read again afterward to see the effect.
- Record grease type and quantity, because mixing incompatible greases can damage bearings.
- Use ultrasound while greasing and stop when the friction signal drops, rather than adding a fixed number of shots.
- Flag any bearing that needs frequent regreasing as a possible seal or contamination problem.
Avoidable Errors
Common Vibration Program Mistakes and Their Fixes
Most vibration programs fail through habit, not technology. These six patterns account for a large share of the false alarms and missed faults teams report.
Relying only on overall velocity
Add acceleration and envelope data, because early bearing defects hide below the velocity threshold.
Measuring in different spots each time
Mark points permanently and photograph them in the asset record.
Ignoring speed and load changes
Log operating state with every reading and build baselines per speed band.
Over-greasing after an alert
Follow the lubrication procedure and quantity. Excess grease can raise temperature and cause damage.
Alarms with no owner
Route every alarm to a named planner through a work order.
No closed-loop learning
Record what the technician found so thresholds improve with each repair.
Documentation
Records That Support Warranty, Insurance, and Audits
Vibration data does more than trigger repairs. A dated history of readings, zones, and corrective actions shows that equipment was maintained against a recognized standard.
Warranty support
A documented baseline and reading history helps show that equipment ran and was maintained within manufacturer expectations.
Insurance and risk reviews
Condition records give risk engineers evidence of an active monitoring program on critical equipment.
Repair or replace decisions
Trend history supports capital planning with real condition data instead of equipment age alone.
Technician handover
New technicians inherit years of findings on each asset rather than starting from zero.
Common Questions
Facility Vibration Analysis: Frequently Asked Questions
How early can vibration analysis detect a bearing problem?
Often weeks to months before failure, though the window depends on speed, load, and lubrication. Treat any fixed number as an average.
Is ISO 10816 still used?
ISO 20816 is the current series and its part 3 replaced ISO 10816-3. The zone letters and limits carry over.
Which facility equipment should be monitored first?
Start with high-consequence rotating assets such as chilled water pumps, chiller motors, and critical air handler fans.
Do wireless sensors replace route-based readings?
They complement them. Use wireless on critical or hard-to-reach assets and routes for the wider population.
How does a CMMS support vibration monitoring?
It stores baselines, schedules routes, and turns alarms into work orders.
Book a demo to see the flow.
Catch the next bearing failure before it stops a building system
Connect vibration readings, baselines, inspection routes, and work orders in one maintenance platform your whole team can use.